

Most foam-line problems do not start with a bad machine. They start upstream, when a specification is written around a single number — density, hardness, or cycle time — without deciding which type of polyurethane foam the process actually needs. Once that question is settled, the required mixing energy, mold temperature, component ratio control, and demold logic become much easier to specify.
A Working Classification: Function Before Chemistry
Polyurethane foam is easier to compare through cell structure, skin formation, and load response than through raw-material family alone. From a processing and equipment-selection standpoint, five practical categories matter most: flexible slabstock, high-resilience molded foam, rigid closed-cell foam, semi-rigid/integral skin foam, and microcellular structural foam.
| Foam category | Typical cell structure | Primary property target | Key equipment implication |
|---|---|---|---|
| Flexible slabstock | Mostly open cell | Resilience, airflow, comfort | Low-pressure continuous pour; surfactant and catalyst balance |
| High-resilience molded | Partly open cell | Ball rebound, support factor | High-pressure impingement mixing; mold fill and venting control |
| Rigid insulation | Mostly closed cell | Low thermal conductivity, compressive strength | Fast cream, high output, closed-cell formation control |
| Semi-rigid/integral skin | Dense skin with cellular core | Skin quality, low compression set | Tight mold temperature control and shorter cream-to-gel window |
| Microcellular/RIM structural | Microcellular | Density, hardness, fatigue resistance | Precision metering, nucleation control, mold-pressure management |
Flexible Foam: Open Cells, Resilience, and Support Factor
Flexible foam is usually built from polyether or polyester polyol with water, catalysts, and surfactants. The formulator controls water content, isocyanate index, and the balance between amine and tin catalysts so that the blowing reaction and the gelling reaction stay aligned. When that balance is correct, the cells open at the right time and the foam becomes breathable and recoverable.
The main properties are usually checked with standardized methods. Apparent density is measured according to ISO 845 [1], indentation hardness according to ISO 2439 [2], and ball rebound resilience according to ISO 8307 [3]. A plant should separate these three values instead of treating “firmness” as a single specification.
For production, flexible foam is demanding in a different way from rigid foam. The system tolerates a wider density band, but the metering ratio still has to stay stable because water content and isocyanate index drive the reaction profile. A small ratio drift can move the cream time, rise time, and final cell structure together.
Resilience testing is one of the fastest ways to confirm that cell opening and cure are repeatable after demold. Measuring Polyurethane Foam Resilience A Practical Test Guide covers the test method and how to read the result against cell structure and gel reaction.
Rigid Foam: Closed Cells and Thermal Performance
Rigid polyurethane foam is formulated for a different outcome: high closed-cell content, compressive strength, and low thermal conductivity. The raw-material side typically uses higher-functionality polyols and polymeric MDI, while the blowing package may combine water, physical blowing agents, or both.
For insulation panels, cold-storage panels, pipe insulation, and refrigeration, the meaningful specification is steady-state thermal performance rather than resilience. Closed-cell content can be measured by methods such as ASTM D6226 [5], while thermal resistance is evaluated with apparatus following ISO 8301 [4]. High closed-cell content also improves moisture resistance and long-term dimensional behavior, but it requires the mixing head and metering system to hold a more aggressive reaction profile.
Rigid foam often moves from cream to tack-free quickly, so mold filling and injection timing become critical. High-output panel lines need a large, repeatable shot delivered quickly, with enough mixing pressure to homogenize the components before the reaction locks the structure. This is where high-pressure impingement mixing tends to earn its cost.
Semi-Rigid, Integral Skin, and Microcellular Foam
Semi-rigid foam sits between soft cushioning and dense elastomer behavior. Automotive interior parts, rail pads, damping blocks, and many structural components use this class. The challenge is controlling the skin formation and the cream-to-gel window: too fast and the mold may not fill completely; too slow and the surface can sink or show flow marks.
Integral skin foam uses the same logic in a more visible way. A colder mold surface slows the reaction near the skin and lets it densify, while the core remains cellular. Keeping mold temperature stable is not optional here; it directly changes surface quality, demold time, and part consistency.
Semi-rigid foams create a processing window that is different from both slabstock and dense elastomer casting, so viscosity, fill rate, and mold venting all shift. What Is Semi Rigid Polyurethane Foam covers the formulation and processing range behind that class.
Microcellular foam goes one step further. It is used in rail pads, automotive buffers, and other parts where a small, uniform cell structure must carry repeated load without becoming a full elastomer. On a rail-pad line, moving from manual open pouring to a compact rotary-disc line with a precision pouring nozzle raised first-pass qualification from below 80% to more than 99% while daily output went from roughly 80 pads to more than 200 pads.
How Foam Type Drives Equipment Selection
The same general-purpose machine cannot handle every foam type equally well. The decision usually comes down to three questions: how fast the reaction moves, how much mixing energy the formulation needs, and whether the part is molded, slabstock, or sprayed.
Flexible slabstock tends to suit low-pressure continuous pouring with careful surfactant and catalyst balance. High-resilience molded parts and rigid closed-cell panels normally benefit from high-pressure impingement mixing because the reaction is faster and the shot must be homogenized quickly. Microcellular RIM and structural parts add another requirement: nucleation control and predictable shot weight, because the part density and mold fill are directly linked.
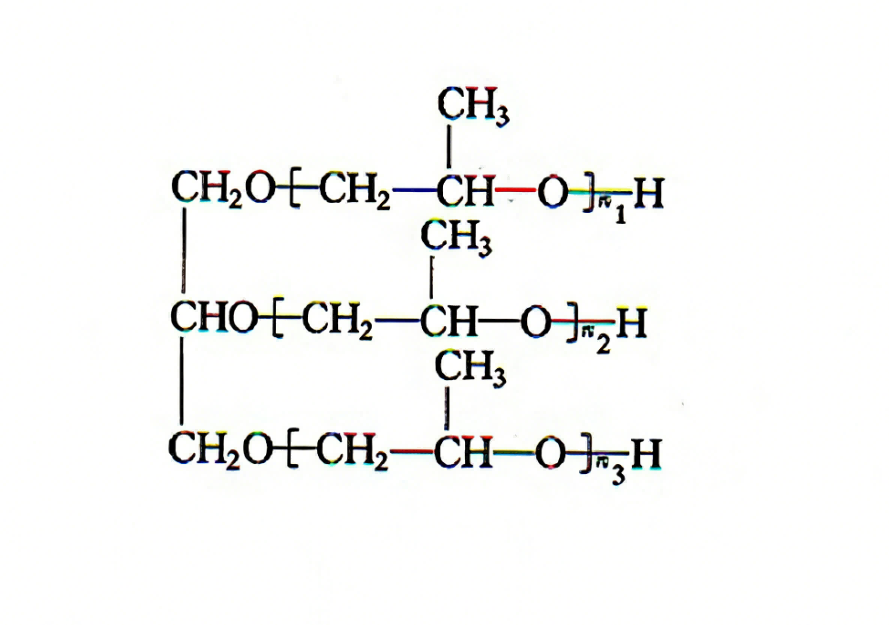
Shot weight deserves special attention. It defines the metering pump range, the mixing head cycle, and the mold carrier timing. If the shot is too small for a large mold, the mix may not fill the cavity before gel; if it is too large, overflow and flash become daily problems.
Shot weight has to be calculated before a molding line is specified, not after trial parts begin. How To Calculate Shot Weight In Polyurethane covers the calculation method and the processing factors that change the number.
Specification Checks Before You Buy
Before comparing machine models, fix the material and process requirements in writing.
- Confirm apparent core density and tolerance using ISO 845 [1].
- Separate hardness from density; use ISO 2439 [2] for flexible foam indentation hardness.
- Define cream time, gel time, rise time, tack-free time, and demold time at your actual mold temperature and line speed.
- Decide whether the part needs open cells, closed cells, or a dense skin. Test closed-cell content with a method such as ASTM D6226 [5].
- Specify resilience for comfort or rebound applications using ISO 8307 [3].
- For insulation parts, state the thermal performance target and test method, such as ISO 8301 [4].
- Verify metering accuracy, ratio control, material recirculation, and the ability to hold process temperature.
The goal is to make the foam type drive the machine decision, not the reverse. When the classification is clear, most of the downstream equipment choices stop being subjective.
Mapping foam type to equipment is a payback decision, not just a chemistry question. If you need to confirm output, mold carrier layout, or whether a low-pressure or high-pressure metering line fits your formulation, write to the engineering team at Info@chinahaifeng.com or reach us on WhatsApp at +86 135 6629 6633 with your part drawing, target cycle, and material system. We will respond with a line configuration and the parameters that matter first.
FAQ
What is the difference between open-cell and closed-cell polyurethane foam?
Open-cell foam has broken cell walls, so air and moisture can move through the structure. It is soft, breathable, and good for cushioning and sound absorption. Closed-cell foam retains gas inside discrete cells, which improves thermal insulation, moisture resistance, and compressive strength. The choice depends on whether the part must breathe or insulate.
Which foam type is easiest to run on a low-pressure pouring line?
Flexible slabstock and many semi-rigid molded parts are the most forgiving for low-pressure pouring because the reaction allows a broader fill window and lower mixing energy demand. Fast rigid systems, very high-resilience molded parts, and dense microcellular parts usually need higher mixing pressure and stricter shot-weight control.
Is higher density always better?
No. Higher density often improves durability and load-bearing capacity, but it also costs more and can hurt weight-sensitive or comfort-driven designs. The correct approach is to specify density, hardness, resilience, and cell structure separately. Density alone does not guarantee the part will perform.
How do I choose between a low-pressure and high-pressure foaming machine?
Look at the reaction speed, the required mixing quality, and the part geometry. Low-pressure equipment suits slower, less demanding fills and can be easier to maintain. High-pressure impingement mixing is preferred for fast formulations, high-output molded lines, and parts that require rapid homogenization before the reaction locks.
What happens if cream time or gel time shifts between batches?
The mold may not fill completely, density may drift, and surface defects can increase. Common causes include raw-material temperature variation, metering ratio drift, moisture contamination, or poor recirculation. The first response is to check component temperature, ratio calibration, and material condition before adjusting the formula.
References
[1] ISO 845:2006, Cellular plastics and rubbers — Determination of apparent density.
[2] ISO 2439:2008, Flexible cellular polymeric materials — Determination of hardness (indentation technique).
[3] ISO 8307:2007, Flexible cellular polymeric materials — Determination of resilience by ball rebound.
[4] ISO 8301:1991, Thermal insulation — Determination of steady-state thermal resistance and related properties — Heat flow meter apparatus.
[5] ASTM D6226, Standard Test Method for Open Cell Content of Rigid Cellular Plastics.
If you’re interested, check out these related articles:
What Is Semi Rigid Polyurethane Foam
How Polyurethane Rollers Are Made From Casting To Cure
SRIM Explained Structural Reaction Injection Molding Basics





