MDI—methylene diphenyl diisocyanate—is not a single material. It is a family of aromatic diisocyanates that includes low-viscosity monomeric grades, high-functionality polymeric MDI (PMDI), and reactive prepolymers. Choosing the wrong member of that family usually does not show up at purchase. It shows up later as unstable ratio control, a foam that drifts off target density, or an elastomer that misses its demold hardness. This guide breaks down where each MDI type earns its place, and what the change means for metering, mixing, and cure control.
Why MDI Shapes the Polyurethane System
MDI contains two isocyanate (NCO) groups on an aromatic backbone. Those NCO groups react with polyol hydroxyl groups to form urethane links and with water to form urea plus carbon dioxide. The aromatic structure brings rigidity, thermal stability, and a fast response in molded parts [1][2].
The important difference between MDI grades is functionality. Pure 4,4′-MDI is close to 2.0, meaning each molecule offers roughly two reactive sites and builds a mainly linear or lightly crosslinked polymer. Polymeric MDI has a functionality closer to 2.6–2.9, which creates the dense, highly crosslinked network needed in rigid foam. MDI prepolymers sit between those extremes: the isocyanate is partly reacted with polyol to reduce NCO content, lower viscosity, and prebuild part of the final structure.
| MDI type | Typical NCO content | Approximate functionality | Common role |
|---|---|---|---|
| Monomeric 4,4′-MDI | ~33.5% | ~2.0–2.1 | Cast elastomers, TPU, coatings |
| Polymeric MDI (PMDI) | ~30–32% | ~2.6–2.9 | Rigid foam, wood binders |
| MDI prepolymer | ~5–28% | ~2.0–2.5 | Elastomers, adhesives, microcellular parts |
Compared with TDI, MDI has a lower vapor pressure at ambient temperature, which reduces the immediate airborne exposure risk during handling. Its reactivity is also generally higher in many foam and elastomer systems, so the process window around mixing, injection, and cure is tighter. Ventilation and skin protection remain non-negotiable.
Rigid Foam Insulation: PMDI Builds the Closed-Cell Matrix
The largest MDI application is rigid polyurethane foam. This covers appliance insulation, continuous sandwich panels, pipe insulation, cold-storage panels, and spray-applied roofing or building insulation. In these products, polymeric MDI is the workhorse because its higher functionality gives the crosslink density needed for compressive strength and dimensional stability.
Two reactions run side by side. The polyol reaction builds urethane links, while the water reaction generates carbon dioxide and urea. Physical blowing agents and surfactants then shape the cell structure. A well-controlled MDI rigid foam system produces small, closed cells that lock in low thermal conductivity. Manufacturers frequently evaluate the result with steady-state thermal transmission testing [3][4][5].
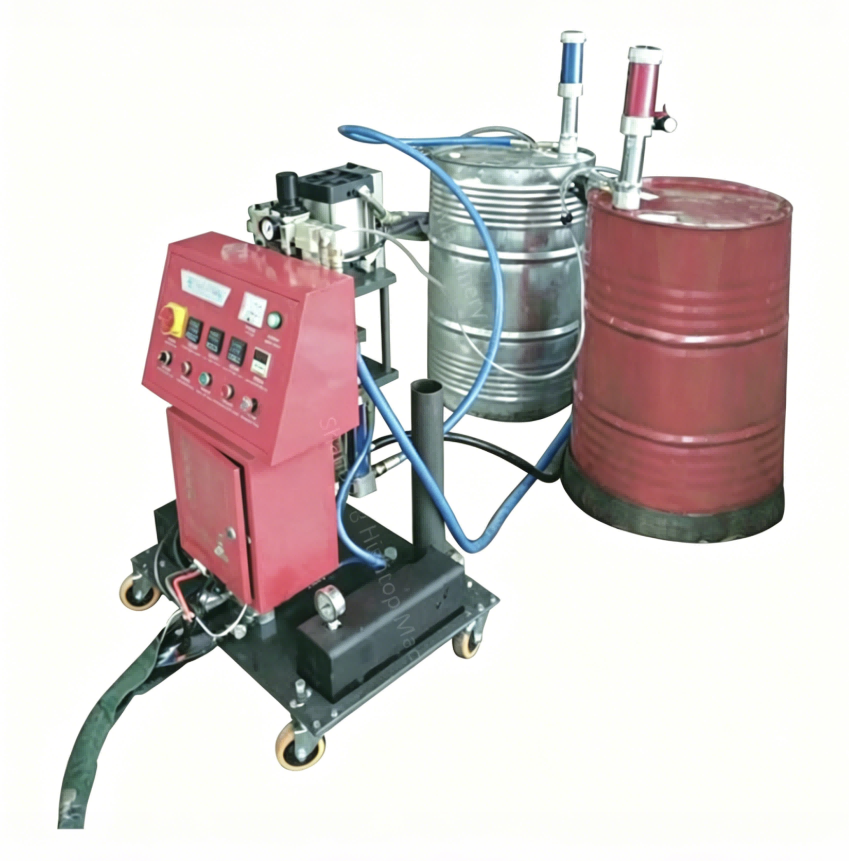
From an equipment view, PMDI viscosity rises fast as temperature drops. That is why day tanks, supply lines, and metering circuits are heated and recirculated. If the A-side is too cold, the metering pump sees higher viscosity and the component ratio can drift before the machine even reaches full output.
MDI-based spray foam is formulated as a two-component system with a fast ambient reaction. What Is Spray Polyurethane Foam Composition And Application covers how the A/B reaction and foam composition are controlled for insulation layers.
Structural and Composite Molding: RIM, SRIM, and RRIM
MDI systems also serve reaction injection molding (RIM), structural reaction injection molding (SRIM), and reinforced reaction injection molding (RRIM). In these processes, a low-viscosity MDI side and a formulated polyol side are injected into a closed mold at high pressure. The materials react quickly, fill thin or complex cavities, and demold as a rigid or semi-rigid part.
SRIM adds a continuous glass mat or structural preform; RRIM adds milled fiber to one component stream. MDI is useful here because the impingement-mixed liquid must wet the reinforcement quickly before viscosity builds. The machine has to keep the ratio accurate under high flow, because a short shot or a lean isocyanate feed creates weak spots that are difficult to detect until the part fails in service.
The difference between standard RIM and SRIM is not just chemistry. Mold clamping force, mixing pressure, and injection rate all change when a reinforcement mat is present. Equipment that worked for an unfilled fascia will not automatically transfer to a structural preform.
MDI-based structural RIM depends on high-pressure impingement mixing to wet the reinforcement. SRIM Explained Structural Reaction Injection Molding Basics covers the process differences that affect fiber wet-out and cavity fill.
Cast Polyurethane Elastomers: MDI Prepolymers and Curative Control
For rollers, wheels, mining screens, seals, and industrial components, MDI prepolymers are often reacted with a chain extender such as MOCA or BDO. The prepolymer route keeps initial viscosity manageable and allows the processor to shift hardness and resilience by changing curative ratio and type.
The final property set depends on stoichiometry. A higher curative fraction can raise hardness while changing tear and compression-set behavior. That is why a cast MDI elastomer line is judged less by nominal pour rate and more by how repeatably it meters the prepolymer and curative over a full shift. Vacuum degassing helps remove trapped air, while a dynamic mixing head must produce a uniform clear or near-clear mix within a short pot life.
Hardness is the first property many plants measure. But hardness alone does not tell you whether the part will survive flexing, oil contact, or wet service. It is only the quickest confirmation that the ratio and cure schedule are on target.
Once a cast MDI part leaves the mold, hardness is the fastest quality check. Shore A Vs Shore D Hardness In Polyurethane covers how to choose the right scale and what the reading does not tell you about tear or compression-set performance.
Microcellular Foam and Footwear
MDI-based microcellular elastomers bridge foam and solid rubber. They are used in shoe soles, midsole components, vibration mounts, and some automotive suspension buffers. The part has a dense skin and a fine internal cell structure, which gives it a different feel and compression behavior than either solid polyurethane or open-cell flexible foam.
The process window is narrow because the material must fill a mold, form a skin, and cure enough to demold without collapsing the cells. Small changes in shot weight or mix ratio become visible as density variation, surface defects, or hardness drift. For a new mold, the plant should verify both fill time and shot weight before committing to a cycle time.
Changing an MDI-system shot weight shifts fill time and cure profile. How To Calculate Shot Weight In Polyurethane covers the variables to lock before you change molds or raise output.
Binders, Adhesives, Coatings, and Sealants
PMDI also functions as a binder. In engineered wood products such as OSB and MDF, the isocyanate reacts with both wood moisture and hydroxyl groups, forming strong bonds without the formaldehyde release associated with some older binder systems. The same chemistry shows up in rubber-crumb binders, construction adhesives, and some foundry or composite applications.
In adhesives and sealants, MDI prepolymers can be formulated as one-component moisture-cure systems or two-component fast-cure systems. Pot life and humidity become critical variables. A one-component MDI sealant cures by reacting with ambient moisture, so application thickness and environmental conditions directly affect the cure front.
Processing Considerations for MDI Systems
MDI is not simply a drop-in replacement for another isocyanate. The machine must be configured around the actual grade being run.
Temperature affects viscosity and reactivity. MDI can dimerize if stored incorrectly, so heated storage must be controlled rather than simply warmed. Recirculation keeps the material homogeneous, but it must not expose the isocyanate repeatedly to moisture-laden air. Dry air or nitrogen blanketing is common on larger tanks.
Metering accuracy matters most in the first seconds of a shot and at the end of a pour. Piston and gear-pump designs both appear in MDI lines, but the selection depends on viscosity, flow range, and whether the stream is filled with abrasive reinforcement. Static mixers are reserved for low-viscosity, low-output jobs; dynamic or high-pressure impingement mixing is needed when the system has a short cream time or a wide ratio.
Need an engineering check for an MDI line? Send the target density, mix ratio, and cycle time to Info@chinahaifeng.com or WhatsApp 86 13566296633, and the team can review whether the metering and mixing circuit matches the grade you are running.
Selecting an MDI Grade: A Short Decision Framework
Before switching MDI grades or launching a new application, four checks remove most surprises.
- Define the end-use property. Closed-cell insulation, hardness, tear strength, and surface skin are different targets that point to different MDI types.
- Check NCO content and functionality. NCO content drives stoichiometry and cure speed; functionality drives crosslink density and heat resistance.
- Measure viscosity at process temperature. The value on the datasheet at 25 °C is not the viscosity inside a heated meter.
- Match pot life to the equipment. A fast MDI system needs a mixing circuit that can deliver a complete, uniform shot before viscosity locks the flow.
- Validate the A/B ratio across the full output range. Calibration at one flow rate does not prove behavior at low shot weights or maximum throughput.
When those five items align, the machine can hold the process window. When one is ignored, MDI’s reactivity turns small errors into large, visible defects.
Talk to a Polyurethane Equipment Engineer
Haifeng Polyurethane Machinery builds bespoke polyurethane processing lines for MDI and TDI systems, from low-pressure foaming machines and high-pressure RIM equipment to elastomer casting and continuous panel lines. If you are changing an MDI grade, qualifying a new formulation, or starting a new application, send your process requirements to:
Email: Info@chinahaifeng.com
WhatsApp: 86 13566296633
FAQ
Does MDI have a lower vapor pressure than TDI?
Yes, MDI has a substantially lower vapor pressure at ambient temperature. This does not remove the need for ventilation and skin protection, but it reduces the airborne exposure risk relative to TDI under normal plant conditions.
What is the difference between monomeric MDI and polymeric MDI?
Monomeric MDI is mainly 4,4′-MDI with functionality near 2.0, making it suitable for elastomers, TPU, and coatings. Polymeric MDI has a mix of higher-functionality oligomers, typically 2.6–2.9, which builds the highly crosslinked structure required in rigid foam and binders.
Can I use the same mixing head for MDI and TDI?
Not automatically. Mixing pressure, temperature, viscosity, and reactivity can all differ. A head sized for one system may run the other, but it must be verified for the grade, ratio, and output range rather than assumed to be interchangeable.
What is the correct storage temperature for MDI?
Storage temperature should follow the supplier’s recommendation for the specific grade. Many MDI products require warmed, moisture-protected storage, but overheating can accelerate dimerization. Controlled heating, dry-air or nitrogen blanketing, and gentle recirculation are more important than a single ideal temperature.
References
[1] M. F. Sonnenschein, Polyurethanes: Science, Technology, Markets, and Trends, 2nd ed., Hoboken, NJ: Wiley, 2021.
[2] M. Ionescu, Chemistry and Technology of Polyols for Polyurethanes, 2nd ed., Smithers Rapra, 2016.
[3] ASTM C518-21, Standard Test Method for Steady-State Thermal Transmission Properties by Means of the Heat Flow Meter Apparatus, ASTM International, 2021.
[4] European Committee for Standardization, EN 13165, Thermal insulation products for buildings — Factory made rigid polyurethane foam (PU) products, CEN.
[5] U.S. Department of Energy, Insulation Materials, Energy Saver, Washington, DC: U.S. DOE.
If you’re interested, check out these related articles:
What Is Semi Rigid Polyurethane Foam
What Is Spray Polyurethane Foam Composition And Application
RRIM Vs RIM Which Process Suits Your Structural Part