Most polyurethane buyers treat Shore A and Shore D as two separate material boxes. In production, a 70 Shore A part and a 70 Shore D part differ less by the number on a gauge than by the formulation, mixing, and cure path used to reach that number. That is the blind spot in most hardness discussions. Shore A vs. Shore D Hardness in Polyurethane is not only a measurement choice; it is a process specification problem. The scale should follow the load, impact, and recovery the part actually sees. The equipment and chemistry then need to be confirmed to hold that value through every shift.
What the Two Shore Scales Measure
Shore A and Shore D both measure resistance to indentation, but they use different indenter geometries and spring forces. Shore A suits softer polyurethane elastomers, gaskets, cushioning, and most molded flexible parts. Shore D suits harder urethanes, wheels, rollers, and rigid engineering parts where a Shore A reading would sit above 90 and lose resolution.
The two scales overlap around 90 Shore A to 40 Shore D, but the relationship is not linear. A two-point difference on Shore A near 60 is not the same as a two-point difference on Shore D near 60. That is why a part should be measured on the scale that gives usable resolution in its working range, not on whichever scale the lab has on hand.
Where Hardness Specifications Go Wrong
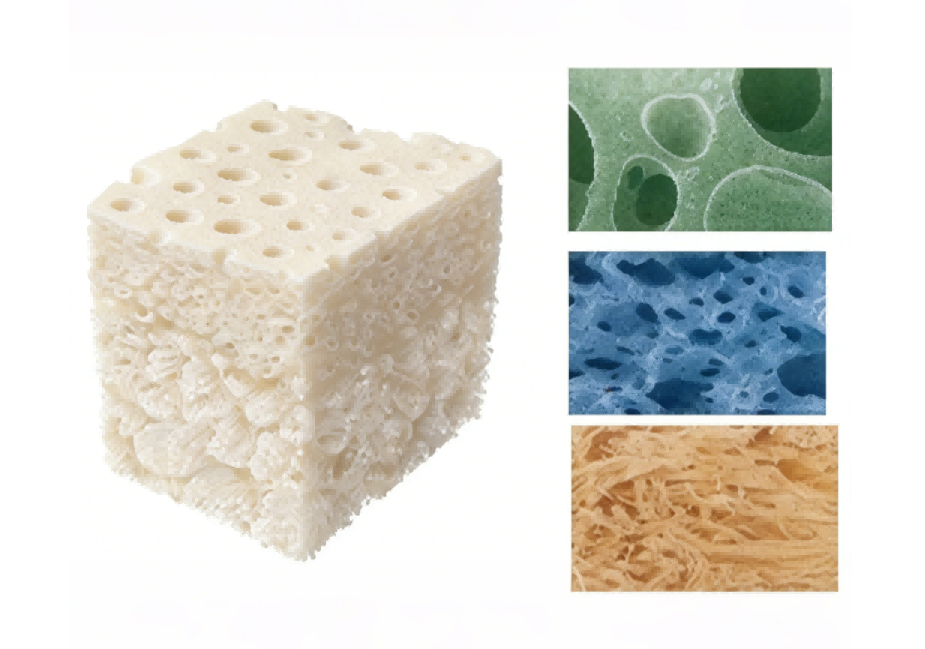
Hardness is the easiest polyurethane property to specify and the easiest to misuse. A drawing may call out Shore A 80 plus a color and a thickness, but say nothing about compression set, rebound, tear strength, or recovery after repeated load. Two materials can read the same on a durometer and behave differently in service because hardness is a surface indentation test, not a full description of the polymer network.
The biggest avoidable error is selecting a scale before understanding the part’s failure mode. A shock absorber buffer block that must return to shape thousands of times needs hardness combined with low compression set. A high-load caster wheel needs hardness combined with load-bearing and tear resistance. When only Shore is controlled, suppliers optimize for the gauge, not for the part.
How Shore A and Shore D Affect Metering and Mixing
Hardness does not live only in the formulation; it is created by the metering and mixing conditions on the line. Stoichiometry, component temperature, and mix quality all influence crosslink density and final Shore value. A small shift in the A/B ratio can move the reaction away from the target network and show up as a lower or higher durometer reading after cure.
In one Taizhou automotive buffer block line we upgraded, the previous semi-automatic process ran at 5.2% defect and ±1.2 mm tolerance. After moving to high-pressure foaming with closed-loop control, the same line held ±0.3 mm tolerance and brought defects down to 2%. The hardness stayed stable because the ratio stayed stable. For production managers, this is the reason to read hardness as a process output, not a raw material guarantee.
If your part combines a narrow Shore window with high output, confirm metering accuracy and mixing head speed before finalizing the BOM. Send your target hardness and shot weight to info@chinahaifeng.com and we can check whether the flow range matches.
Matching Hardness to Load, Impact, and Recovery
Shore value narrows the material class but does not choose the formulation. The table below shows how common polyurethane applications map across the two scales and what equipment considerations follow.
| Application | Typical working range | Scale that gives better resolution | Primary equipment consideration |
|---|---|---|---|
| Gaskets and cushion pads | 30–70 Shore A | Shore A | Smooth low-pressure casting, mold temperature control |
| Automotive suspension buffers | 35–65 Shore A | Shore A | Low-pressure 2A2B metering, ±0.3% dosing, external mold heat |
| Industrial rollers and wheels | 70 Shore A to 50 Shore D | Shore A or Shore D depending on formulation | High-shear mixing, vacuum defoaming, MOCA/BDO switching |
| Printing and conveying rollers | 80 Shore A to 60 Shore D | Shore D for harder grades | High-precision metering, color paste addition, automatic cleaning |
| High-load wear parts and screen plates | 50–75 Shore D | Shore D | Large-flow casting, wear-resistant additive tank |
These ranges are starting points, not a substitute for a molded sample. A 75 Shore A roller made with BDO and a 75 Shore A roller made with MOCA can differ in rebound and compression set even when the durometer agrees.
A Spec Confirmation Sequence Before You Lock the Line
Before a hardness value goes onto a production drawing, run it through this sequence. The goal is to make sure the number is testable, repeatable, and tied to the right equipment.
- Define the functional failure first: compression set, abrasion, impact, or recovery. Hardness is the confirmation, not the target.
- Pick the scale with resolution. If the expected reading sits above 90 Shore A or below 30 Shore D, switch scales.
- State the full material context: prepolymer type, chain extender, filler, post-cure time, and molded density where relevant.
- Confirm the metering and mixing equipment can hold the A/B ratio at your shot weight and cycle time. A hardness spec without ratio control is a wish, not a process.
- Run pilot samples at three points around the target hardness and measure after full cure, not just at demold.
Production teams usually find a hardness gap during pilot runs, when the part feels right on a hand gauge but fails after compression set or recovery testing. That is the wrong time to rework the chemistry. If you are still at the specification stage, work backward from the part’s end-use requirements and let the machine parameters follow the material choice.
Haifeng Polyurethane Machinery designs metering and pouring systems with ±0.3% dosing accuracy and closed-loop temperature control for low-pressure and high-pressure polyurethane processing. For parts with a narrow Shore window and high output, that control is what keeps hardness from drifting shift to shift.
Send your part drawing, target Shore value, and shot weight to info@chinahaifeng.com, or reach us on WhatsApp at 86 13566296633. We will confirm the metering range and mixing head configuration before you lock the BOM.
Common Questions About Shore A and Shore D in Polyurethane
Can Shore A and Shore D values be converted?
No single formula converts a Shore A reading to a Shore D reading. The scales use different indenter geometries and spring forces, so conversion charts are approximations at best. If a part reads near the top of the Shore A range or the bottom of the Shore D range, measure it on the other scale and specify that value. For production control, the useful step is to pick the scale that gives mid-range resolution for your target, then keep every incoming and molded check on that same scale.
Why do two parts with the same Shore reading perform differently?
A common assumption is that equal Shore hardness means equal performance. Hardness only measures the surface response to a small indentation. The polymer network behind that surface depends on prepolymer type, chain extender, crosslink density, filler, and post-cure. Two 80 Shore A rollers can differ in rebound, tear strength, and compression set. When a supplier says “same hardness,” ask for the full property set that matters for the part rather than treating the durometer number as the specification.
Should I specify hardness before or after formulation?
It depends on which side of the part carries more risk. If end-use performance is fixed, specify the functional requirement and let the formulator propose the hardness and the chemistry together. If the line and cycle time are already fixed, specify both the target Shore range and the metering window the machine can hold. The mistake is to lock a single Shore number before the part has been molded, then force the equipment to chase a reading the formulation cannot produce.
What hardness range do polyurethane rollers and wheels usually need?
A better question is what the roller or wheel needs to resist. Soft wheels for maneuverability often run 50 to 70 Shore A. Industrial rollers that must carry load and resist wear often fall between 80 Shore A and 60 Shore D. High-load wear parts can go to 50 Shore D and above. The range alone is not enough because hardness does not predict tear resistance or rebound. If your part needs a hardness in that span and you want to confirm whether metering can hold it at production speed, send your drawing and shot weight to info@chinahaifeng.com.