
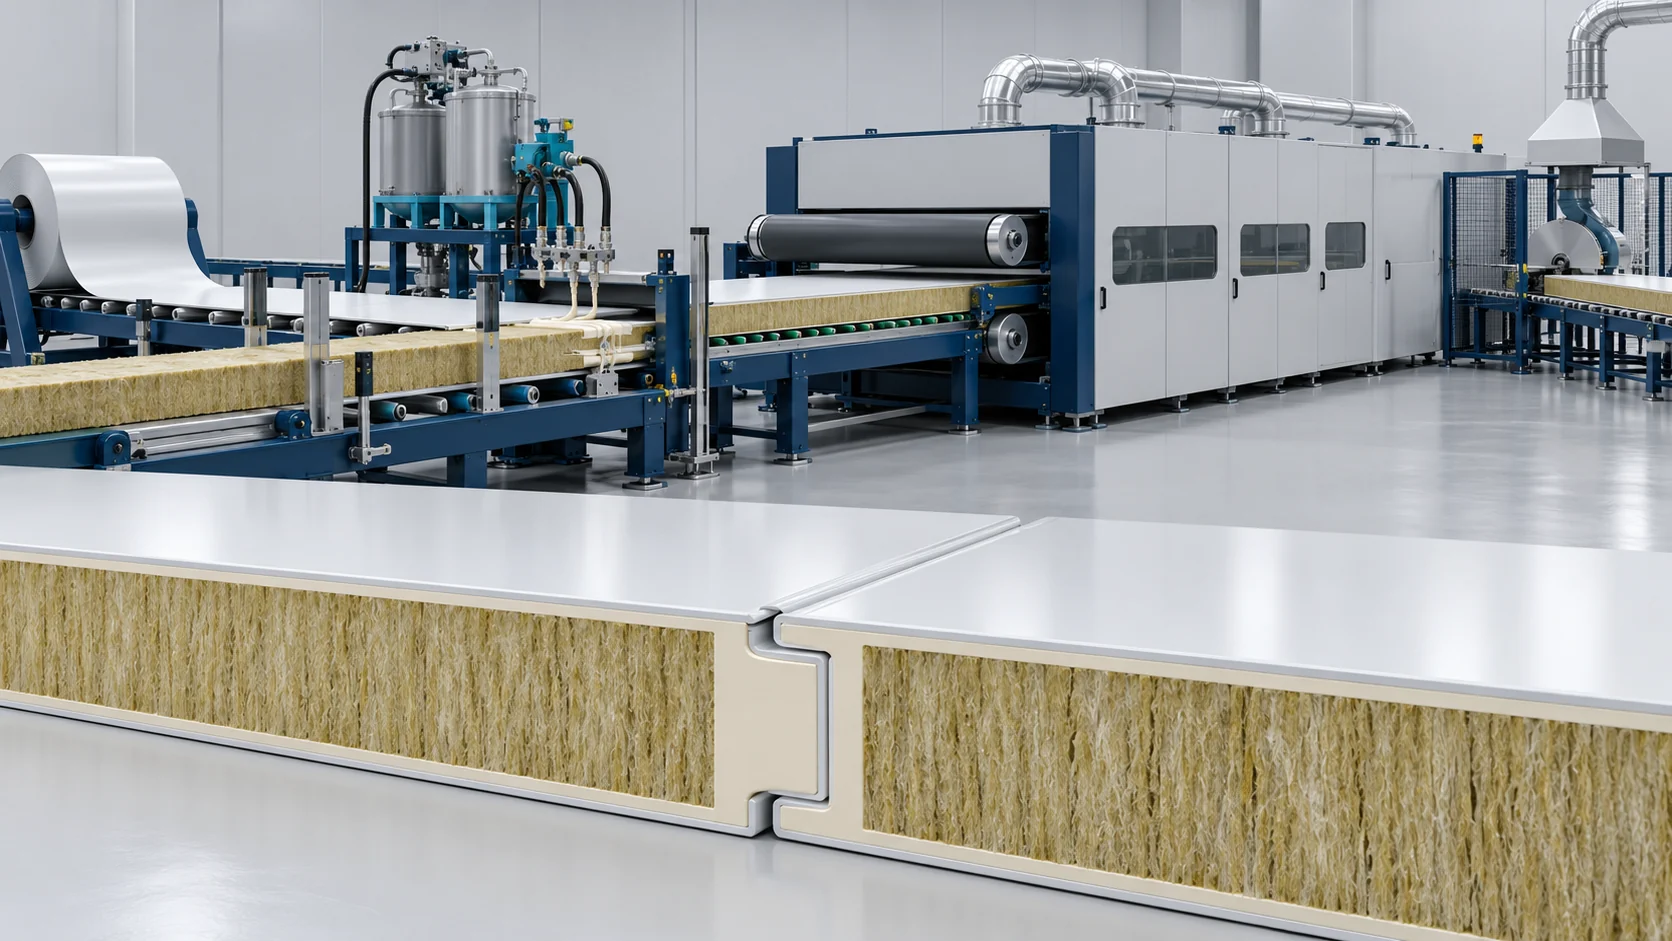
Cleanroom Sandwich Panel Production Solution
Configure PU/PIR foaming or rock wool lamination for cleanroom wall and ceiling panels, with controlled surfaces, joints, sealing and cutting. Concept illustration — not a photograph of delivered equipment or a customer installation.
Panel Manufacturing for Controlled Environments
Cleanroom panel manufacturing coordinates facing preparation, core processing, joint design and handling. The supplied surface-deviation reference is ≤0.3 mm over a 1 m measurement length, as confirmed by Haifeng. Room cleanliness classification, pressure retention and chemical-cleaning compatibility require assessment of the complete installed enclosure and ventilation system; the panel line does not certify a cleanroom class.
Surface Measurement
Specify the 1 m measurement length, instrument, panel support and sampling plan for the reported ≤0.3 mm deviation.
Joint and Seal Design
Agree gasket channels, joint tolerances and pressure-test conditions for the assembled envelope.
Haifeng configures facing, metering or adhesive application, lamination, cutting and handling for the selected panel route. Cleanroom qualification is a separate facility task.
Precision Cleanroom Panel Lamination Process
Facing preparation, route-specific core processing, controlled lamination and cutting with dust extraction.
High-Precision Flush Joint Roll Forming
Pre-painted medical-grade coils pass through micro-adjustable forming cassettes, shaping flush tongue-and-groove edges with integrated sealant channels.
Automated Core Positioning & Edge Foaming
For rock wool panels, slit and orient mineral strips, apply adhesive and configure PU edge foaming where specified. PU/PIR foam-core panels use a separate reactive laydown configuration; mineral wool is not itself foamed.
High-Rigidity Heated Double-Belt Lamination
The supplied 30 m reference laminator controls panel thickness and cure conditions. The reported surface deviation is ≤0.3 mm over a 1 m measurement length; thickness tolerance is a separate quantity.
Technical Specifications
Review the equipment and process parameters for Cleanroom Controlled Environment Panel Line. Final values depend on the material, tooling, production target and agreed configuration.
| Technical Parameter | Standard Specification / Value | Engineering Context & Verification |
|---|---|---|
| Target Application | Pharmaceutical GMP, Semiconductor, Bio-lab Cleanrooms | Application planning; installed-room classification is separate |
| Core Materials | Polyurethane (PUR) / Polyisocyanurate (PIR) / Structural Basalt Rock Wool | Route-specific core; finished-panel performance requires testing |
| Surface Flatness Tolerance | ≤0.3 mm over a 1 m measurement length | User-confirmed 1 m measurement basis; agree instrument and sampling |
| Joint Configuration | Flush Cleanroom Tongue-and-Groove with Gasket Slot | 50 Pa is a supplied pressure-test reference; define leakage criterion and assembly |
| Panel Thickness Range | 50 mm – 150 mm | Standard cleanroom wall and ceiling dimensions |
| Continuous Line Speed | 4 – 10 m/min | Balanced for rock wool insertion and curing |
Equipment for This Solution
Explore the coordinated production equipment and integrated systems.
Continuous PIR Sandwich Panel Line | Insulation Panels
30 m continuous PIR panel configuration with metering, laydown, heated lamination and synchronized cutting. Finished-panel fire classification depends on the tested construction.
Continuous Rock Wool Sandwich Panel Line | Insulation Panels
Continuous mineral-wool slitting, orientation, adhesive application and lamination, with separately configured PU edge foaming where required.
Key Cleanroom Engineering Advantages
For Cleanroom Controlled Environment Panel Line, assess material compatibility, process control, equipment interfaces and changeover needs against your production brief.
Measured Surface Control
Reference deviation ≤0.3 mm over 1 m; agree sampling and panel support.
Facing and Cleaning Compatibility
VHP compatibility depends on the selected coating, seal and cleaning conditions; qualify them separately.
Joint Inspection
Check profile and seals against the agreed leakage test.
Core Route Selection
Specify foam-core production or mineral-wool adhesive lamination. Finished-panel fire performance includes facings, adhesive and edge foam.
Related Project Case
Review the production configuration, delivery and results.
Frequently Asked Questions
Find answers about Cleanroom Controlled Environment Panel Line, including material selection, equipment configuration and the information needed to plan a production line.
How is the surface-deviation value measured?
Can one configuration process foam and rock wool?
Does the equipment certify ISO cleanroom class or VHP resistance?
How is cutting dust controlled?
How long does commissioning take?
Discuss Your Sandwich Panel Project
For Cleanroom Controlled Environment Panel Line, send finished-product drawings or samples, material data, target output, automation needs and factory conditions. Haifeng can use these inputs to discuss the line configuration and technical interfaces.


