
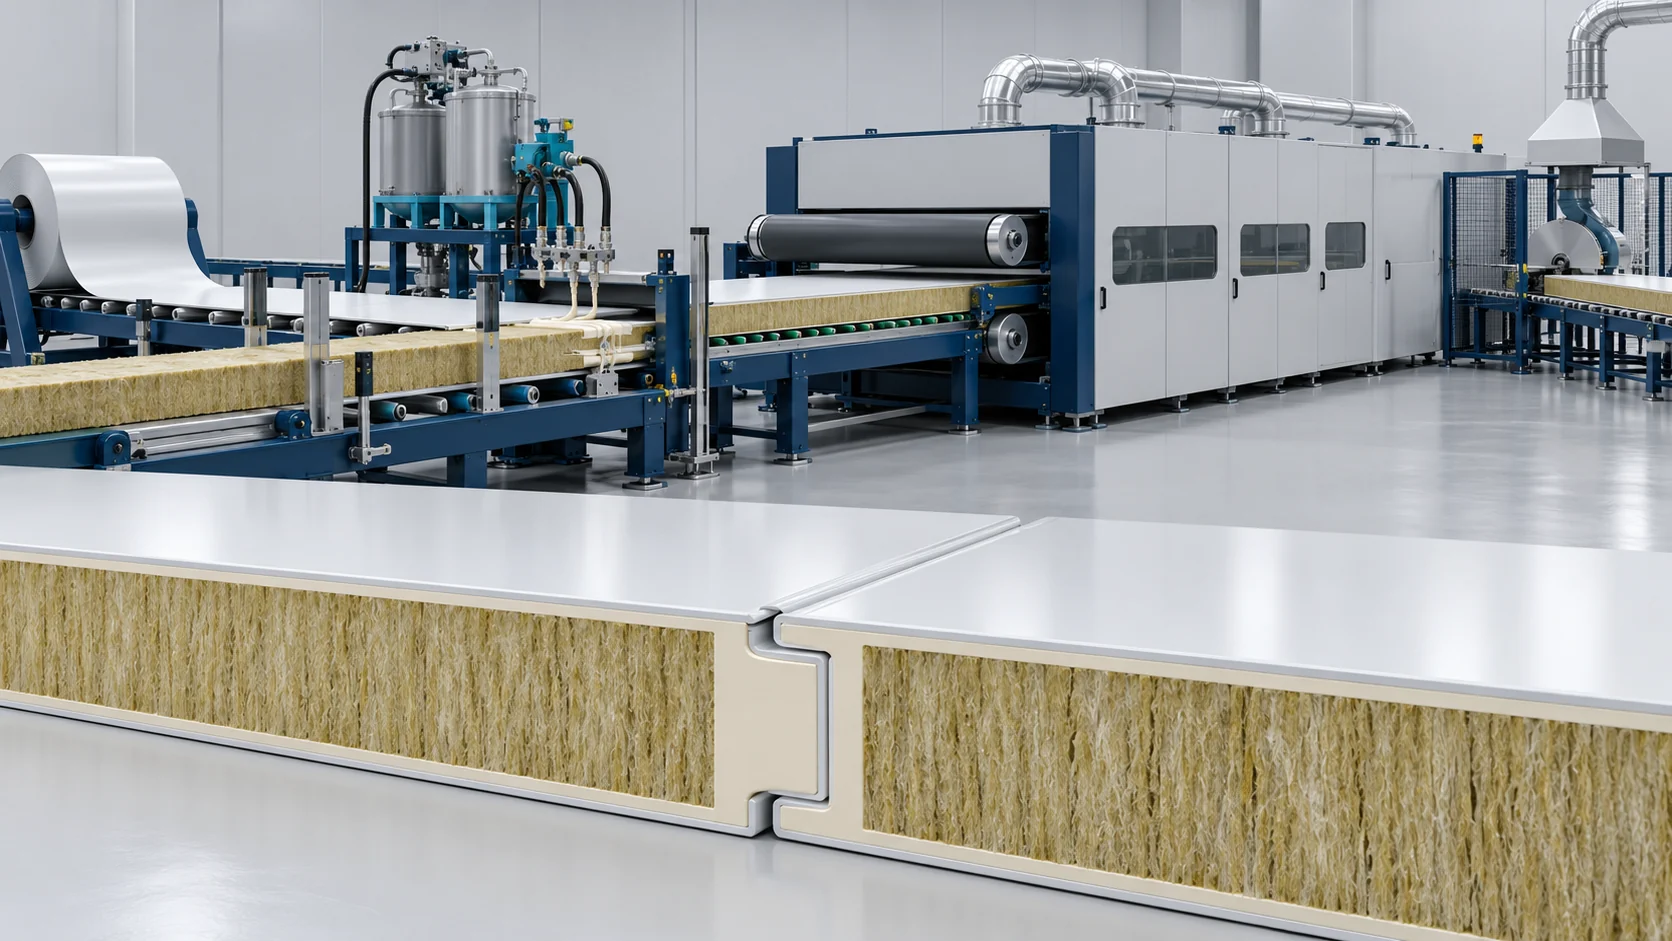
Решение для производства сэндвич-панелей для чистых помещений
Configure PU/PIR foaming or rock wool lamination for cleanroom wall and ceiling panels, with controlled surfaces, joints, sealing and cutting. Concept illustration — not a photograph of delivered equipment or a customer installation.
Panel Manufacturing for Controlled Environments
Cleanroom panel manufacturing coordinates facing preparation, core processing, joint design and handling. The supplied surface-deviation reference is ≤0.3 mm over a 1 m measurement length, as confirmed by Haifeng. Room cleanliness classification, pressure retention and chemical-cleaning compatibility require assessment of the complete installed enclosure and ventilation system; the panel line does not certify a cleanroom class.
Surface Measurement
Specify the 1 m measurement length, instrument, panel support and sampling plan for the reported ≤0.3 mm deviation.
Joint and Seal Design
Agree gasket channels, joint tolerances and pressure-test conditions for the assembled envelope.
Сравнение смежных производственных маршрутов
Select the core and joint before specifying cleanroom-panel equipment. Foam processing and rock-wool insertion need different preparation and bonding arrangements; facing, seals and cleaning compatibility require their own checks on the intended construction.
Precision Cleanroom Panel Lamination Process
Facing preparation, route-specific core processing, controlled lamination and cutting with dust extraction.
High-Precision Flush Joint Roll Forming
Specified coated-steel or SUS304 facings pass through the selected forming cassettes to produce flush joint profiles and sealing channels. Surface and cleaning compatibility are reviewed for the enclosure.
Automated Core Positioning & Edge Foaming
For rock wool panels, slit and orient mineral strips, apply adhesive and configure PU edge foaming where specified. PU/PIR foam-core panels use a separate reactive laydown configuration; mineral wool is not itself foamed.
High-Rigidity Heated Double-Belt Lamination
The supplied 30 m reference laminator controls panel thickness and cure conditions. The reported surface deviation is ≤0.3 mm over a 1 m measurement length; thickness tolerance is a separate quantity.
Технические характеристики
Review the equipment and process parameters for Cleanroom Controlled Environment Panel Line. Final values depend on the material, tooling, production target and agreed configuration.
| Технический параметр | Стандартная спецификация / Значение | Инженерный контекст и проверка |
|---|---|---|
| Целевое применение | Pharmaceutical GMP, Semiconductor, Bio-lab Cleanrooms | Application planning; installed-room classification is separate |
| Core Materials | Polyurethane (PUR) / Polyisocyanurate (PIR) / Structural Basalt Rock Wool | Route-specific core; finished-panel performance requires testing |
| Surface Flatness Tolerance | ≤0.3 mm over a 1 m measurement length | Agreed reference 1 m measurement basis; agree instrument and sampling |
| Joint Configuration | Flush Cleanroom Tongue-and-Groove with Gasket Slot | 50 Pa is a supplied pressure-test reference; define leakage criterion and assembly |
| Диапазон толщины панели | 50 мм – 150 мм | Standard cleanroom wall and ceiling dimensions |
| Скорость непрерывной линии | 4 – 10 м/мин | Balanced for rock wool insertion and curing |
Оборудование для этого решения
The foam-panel and rock-wool lines represent different core routes. Confirm feeding, adhesive and edge-dosing modules for the selected panel.
Непрерывная линия производства сэндвич-панелей PIR | Панели изоляции
Непрерывная линия производства сэндвич-панелей PIR для панелей изоляции. Ознакомьтесь с конфигурацией, требованиями к материалам и технологическими интерфейсами вместе с Haifeng.
Непрерывная линия производства сэндвич-панелей с каменной ватой | Панели изоляции
Непрерывная линия производства сэндвич-панелей с каменной ватой для изоляционных панелей. Ознакомьтесь с конфигурацией, требованиями к материалам и технологическими интерфейсами совместно с Haifeng.
Key Cleanroom Engineering Advantages
For Cleanroom Controlled Environment Panel Line, assess material compatibility, process control, equipment interfaces and changeover needs against your production brief.
Measured Surface Control
Reference deviation ≤0.3 mm over 1 m; agree sampling and panel support.
Facing and Cleaning Compatibility
VHP compatibility depends on the selected coating, seal and cleaning conditions; qualify them separately.
Joint Inspection
Check profile and seals against the agreed leakage test.
Core Route Selection
Specify foam-core production or mineral-wool adhesive lamination. Finished-panel fire performance includes facings, adhesive and edge foam.
Связанные проекты
The PU cleanroom-panel record is not automatically evidence for a rock-wool configuration or an installed cleanroom classification.
Часто задаваемые вопросы
Сравните производственные маршруты, требования к материалам, конфигурации оборудования и исходные данные проекта.
How is the surface-deviation value measured?
Can one configuration process foam and rock wool?
Does the equipment certify ISO cleanroom class or VHP resistance?
How is cutting dust controlled?
How long does commissioning take?
Какие исходные данные нужны для этой конфигурации?
What is needed to interpret a flatness or pressure-test reference?
Обсудите ваш проект сэндвич-панелей
Share the following for this application: Facing/coating, core material, panel and joint drawings, support conditions, flatness/leak test plan and cleaning regime. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


