
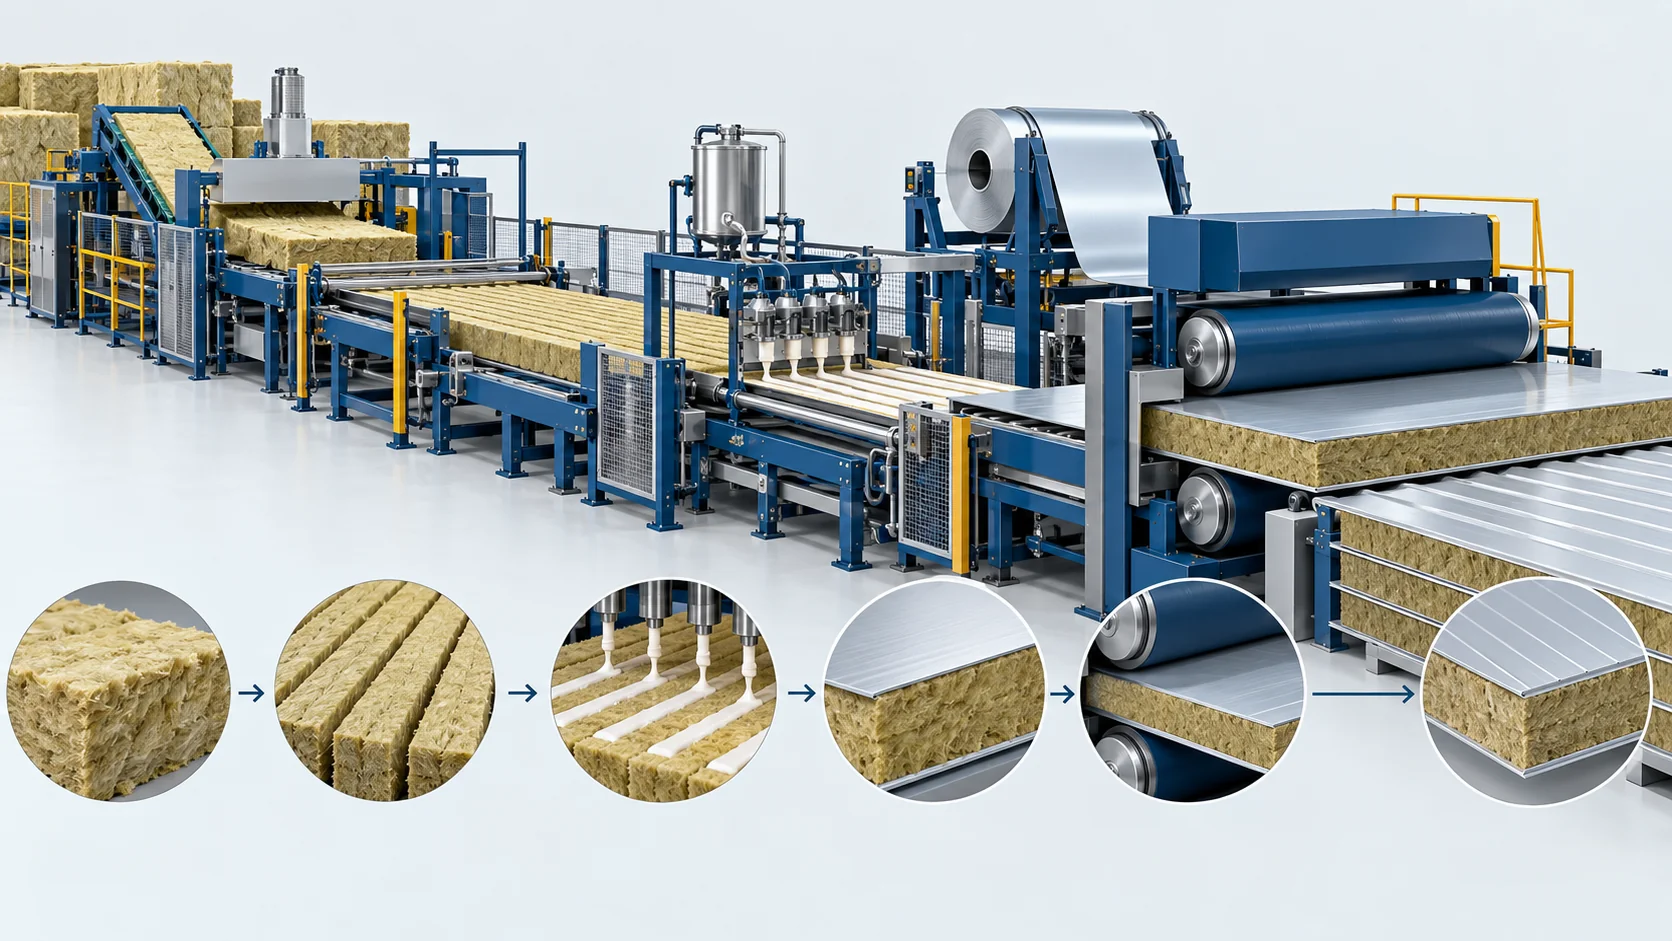
Continuous Rock Wool Sandwich Panel Line | Insulation Panels
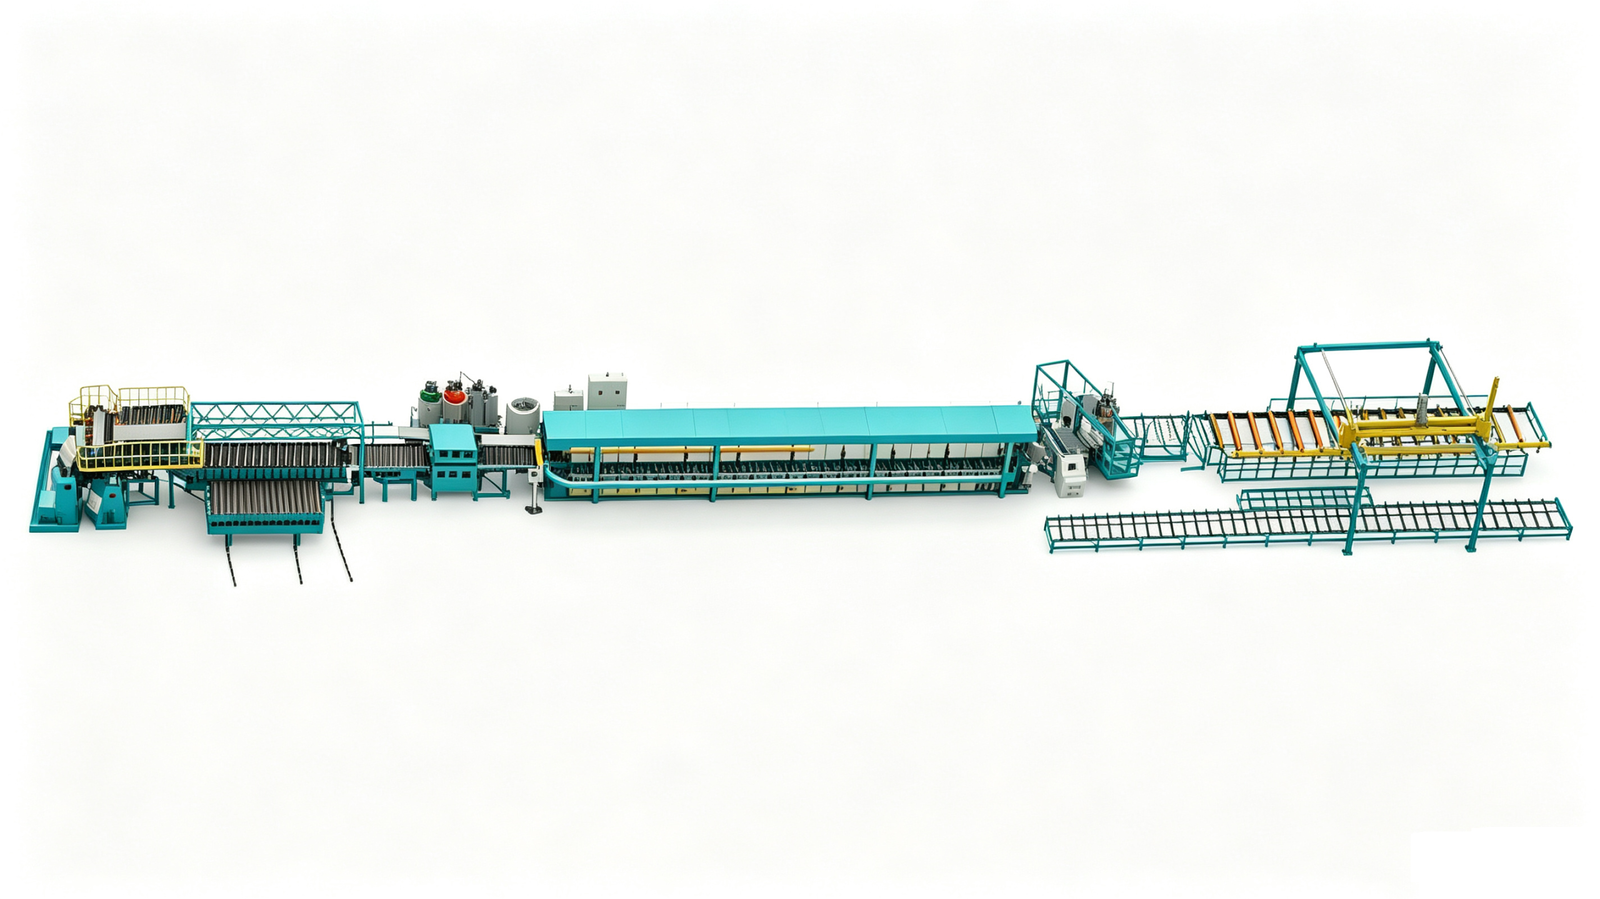
Continuous mineral-wool slitting, orientation, adhesive application and lamination, with separately configured PU edge foaming where required. Concept illustration — not a photograph of delivered equipment or a customer installation.
Max Line Speed
10 m/min — Continuous mineral wool output
Mineral-Wool Core
Finished-panel fire performance tested for its complete build-up
Edge Sealing
Optional configured edge treatment; joint sealing requires validation
Thickness Range
50–200 mm — Structural wall and roof
Product Overview
The HF-RW-30M reference processes mineral-wool slabs through slitting, 90° orientation, adhesive application and heated lamination. PU edge foaming is a separately configured option. Mineral-wool core performance does not by itself classify the finished panel with adhesive, facings, joints and edge foam.
Concept illustration — not a photograph of delivered equipment or a customer installation.
See the cleanroom panel manufacturing solution for a related mineral-wool configuration. The industrial PIR case is a different core route and is not evidence of rock-wool delivery.
Technical Specifications
| Technical Parameter | HF-RW-30M |
|---|---|
| Components | Mineral wool strips + 2-Component PU glue & side seal |
| Power Supply | 380V / 50Hz, 3-Phase |
| Working Pressure | 150 bar (Side PU injection unit) |
| Dimensions (L×W×H) | Total Line Length: Approx. 130m |
| Rock Wool Density Range | 80 – 140 kg/m³ |
| Panel Thickness Range | 50 mm – 200 mm |
| Maximum Continuous Speed | 8 – 10 m/min |
Key Features
Mineral-Wool Processing
Slitting and orientation prepare strips for the specified panel build-up.
Configured Edge Treatment
PU edge foaming and seals are selected for the joint and moisture requirements.
Adhesive Lamination
Bond performance is established by material and panel tests; no universal strength-improvement percentage is specified.
Related Production Systems
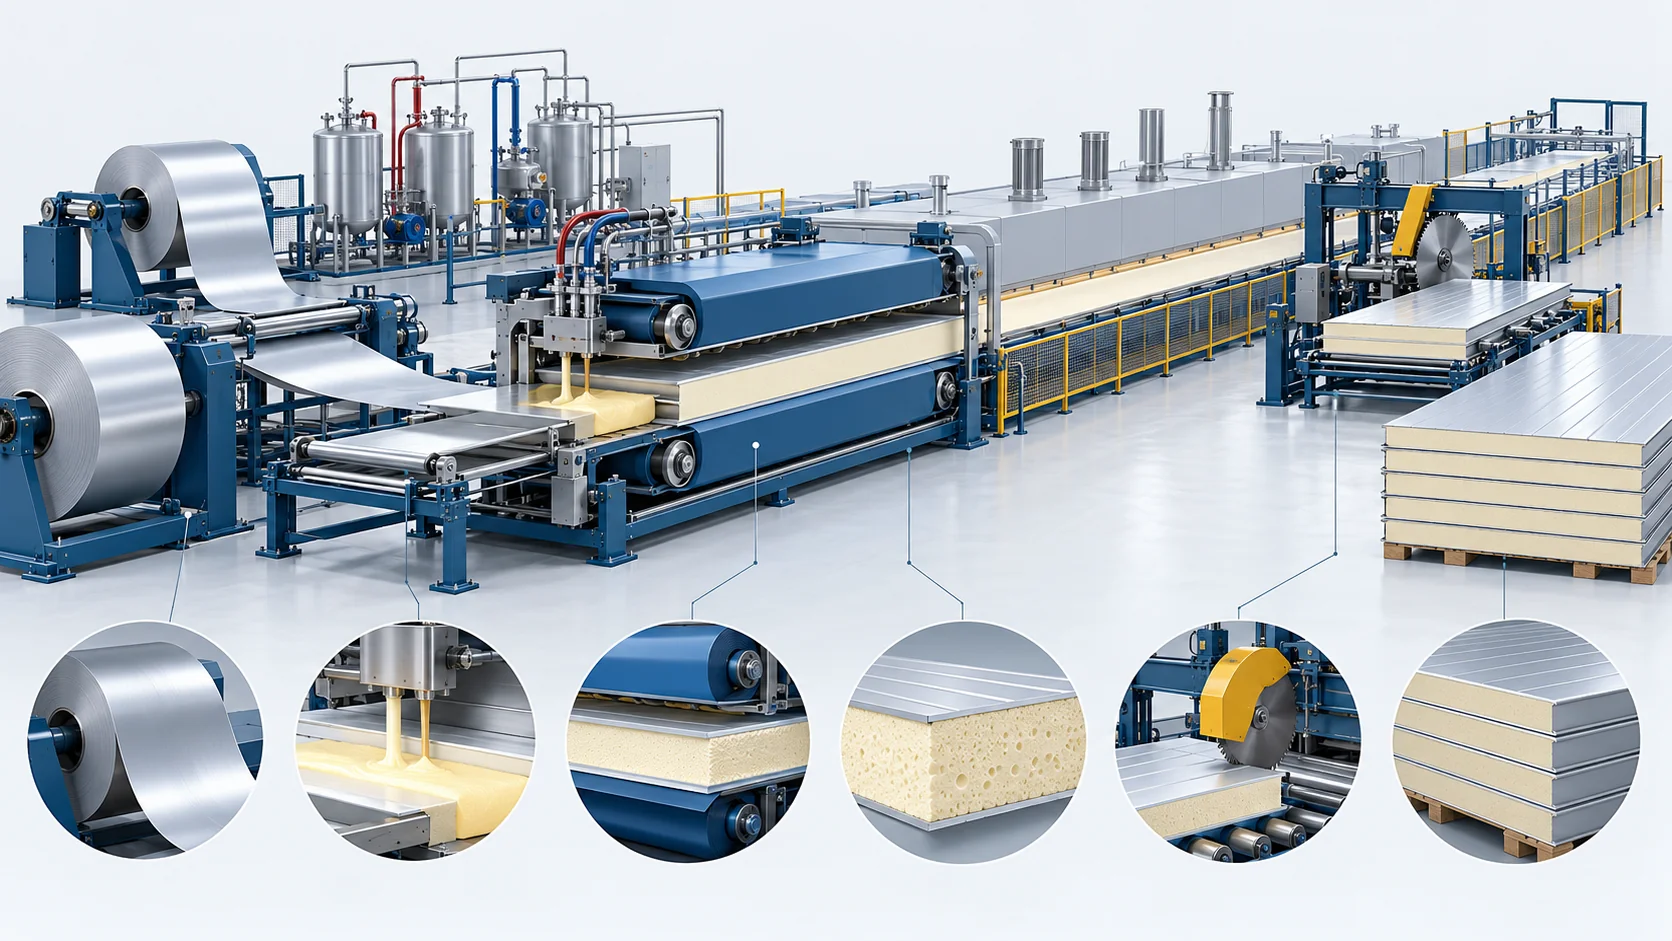
Continuous PIR Sandwich Panel Line | Insulation Panels
Sandwich Panel Production Lines
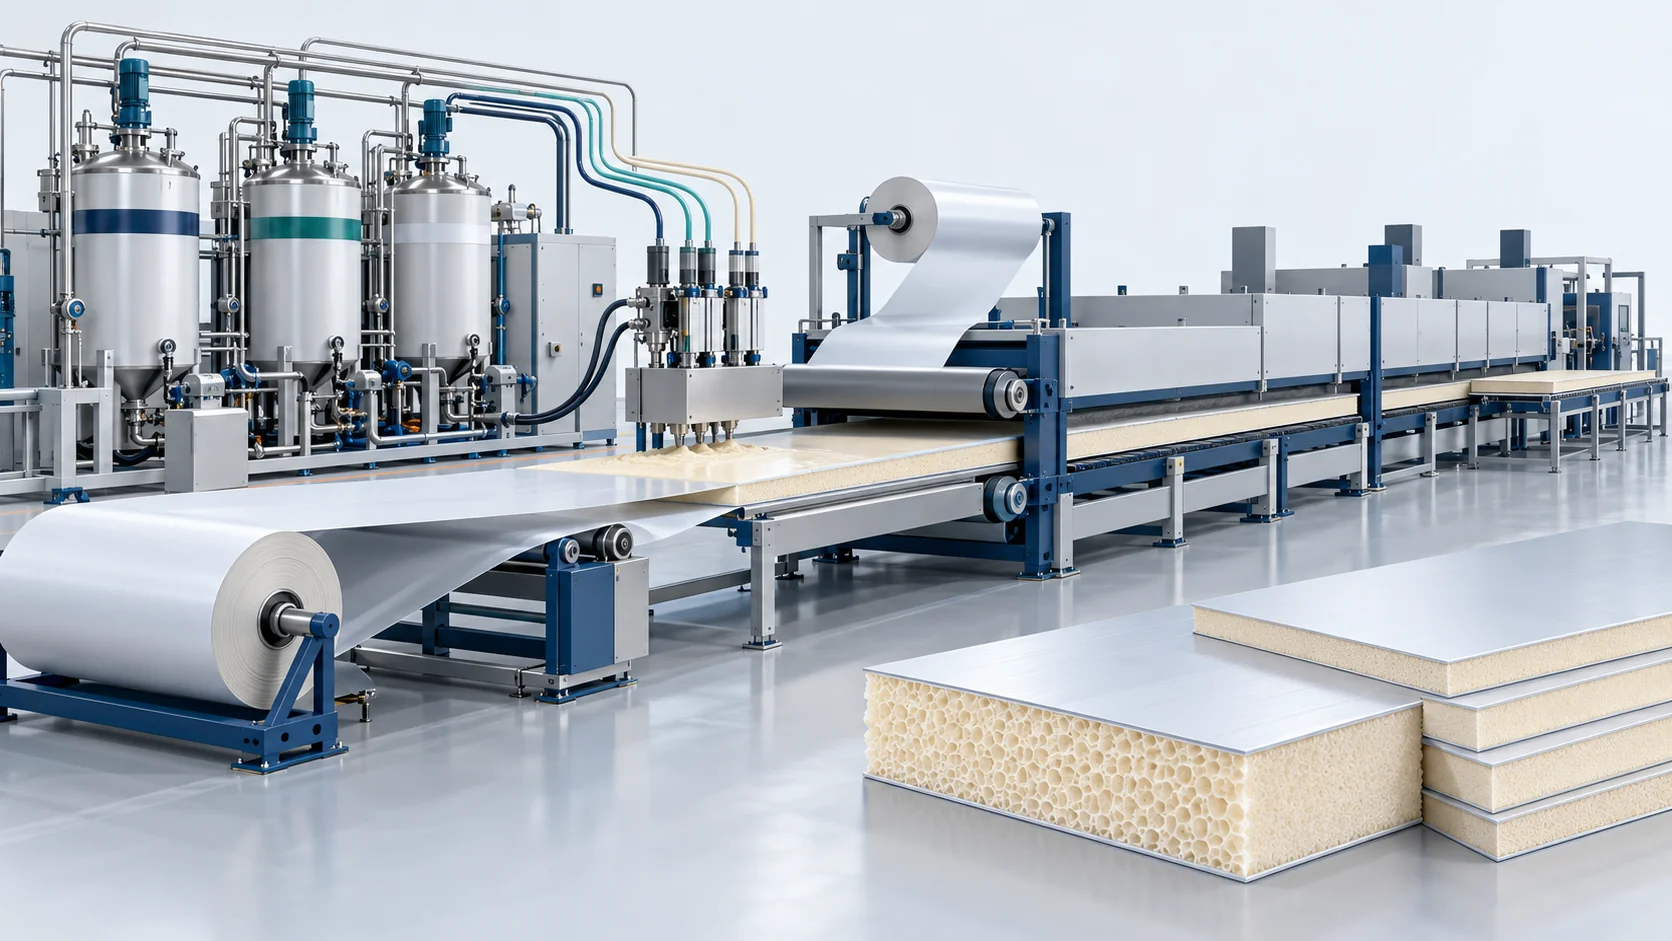
Continuous Phenolic Sandwich Panel Line | Insulation Panels
Sandwich Panel Production Lines
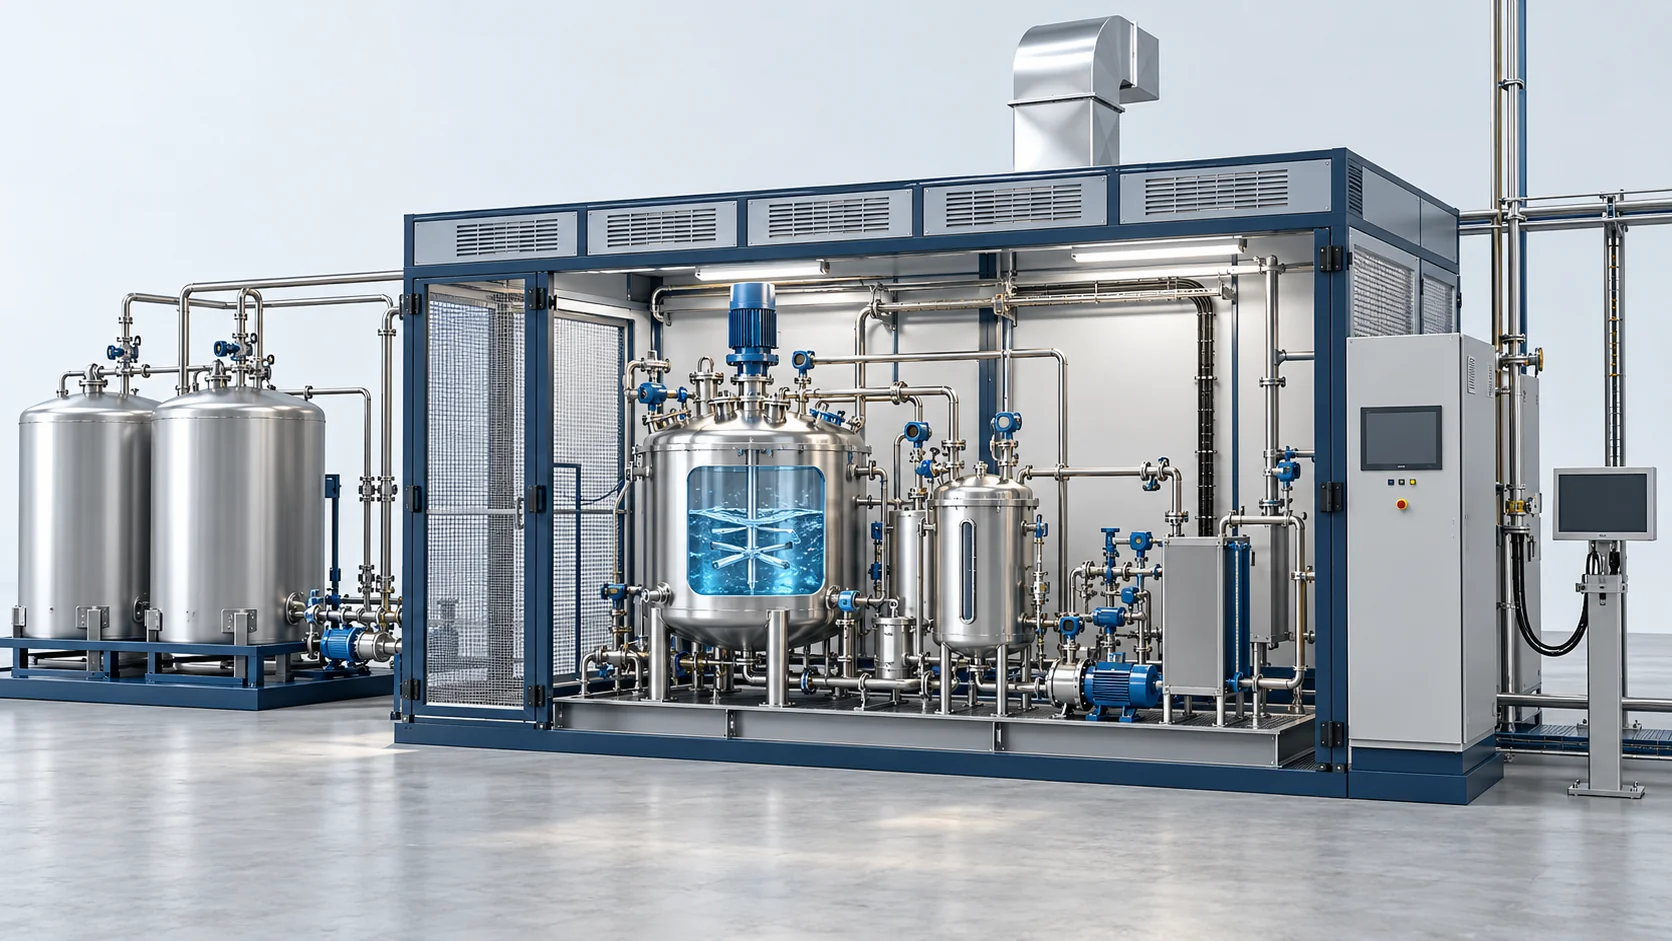
Continuous PU Sandwich Panel Line | Insulation Panels
High Pressure Polyurethane Machine


