
Continuous PIR Sandwich Panel Line | Insulation Panels
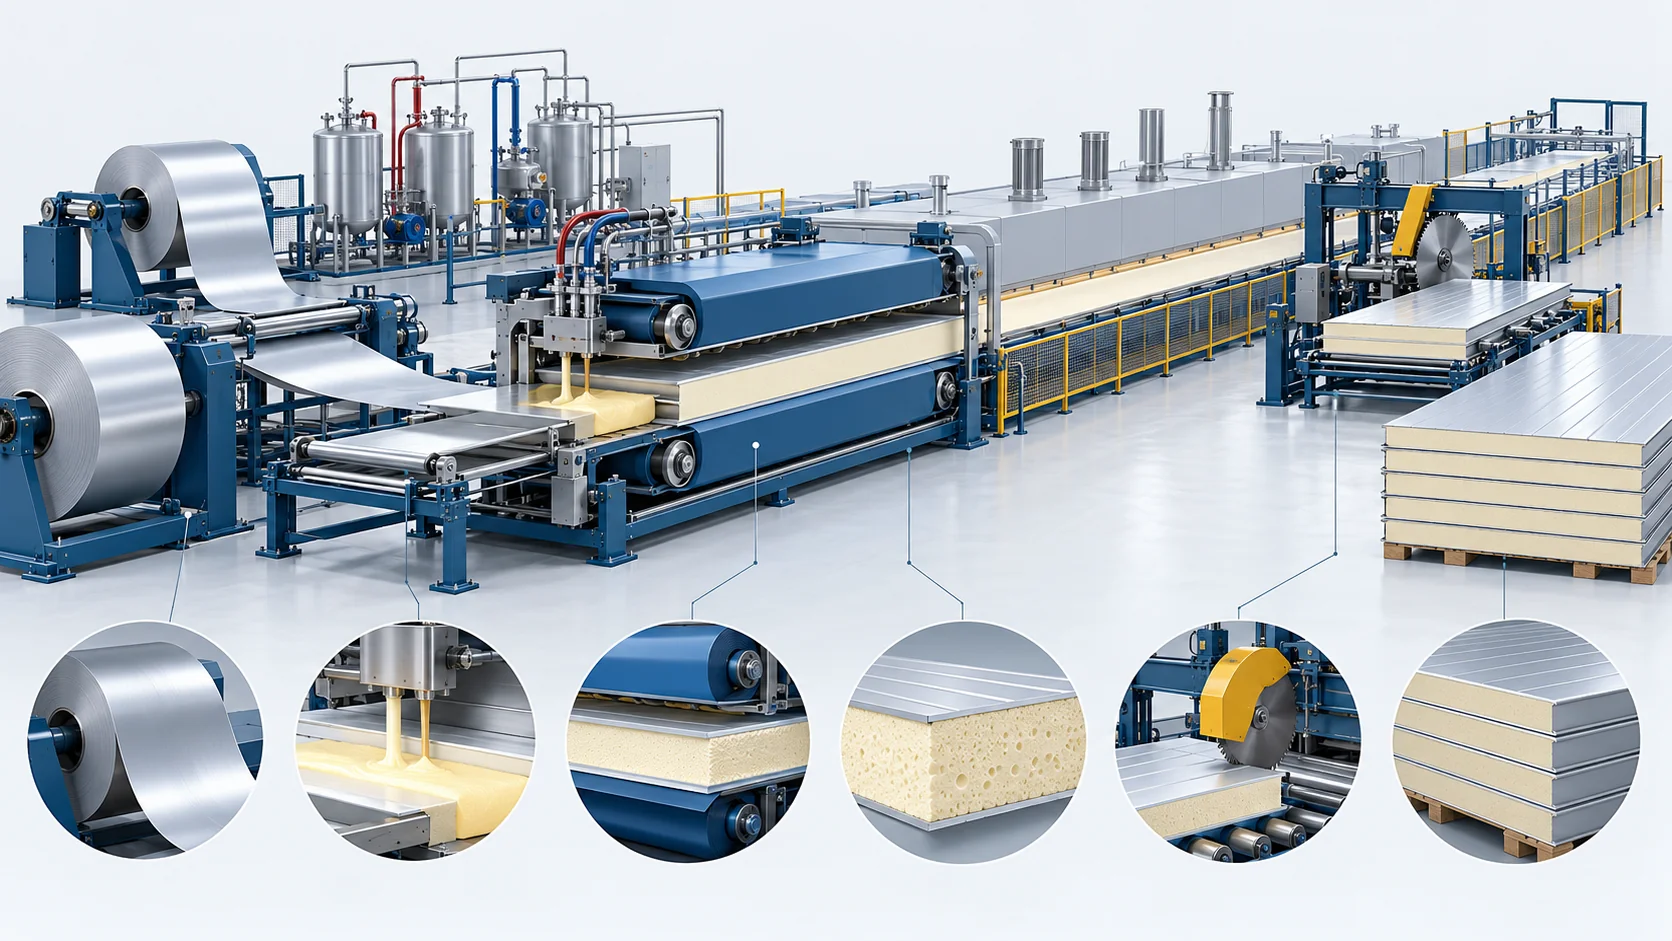
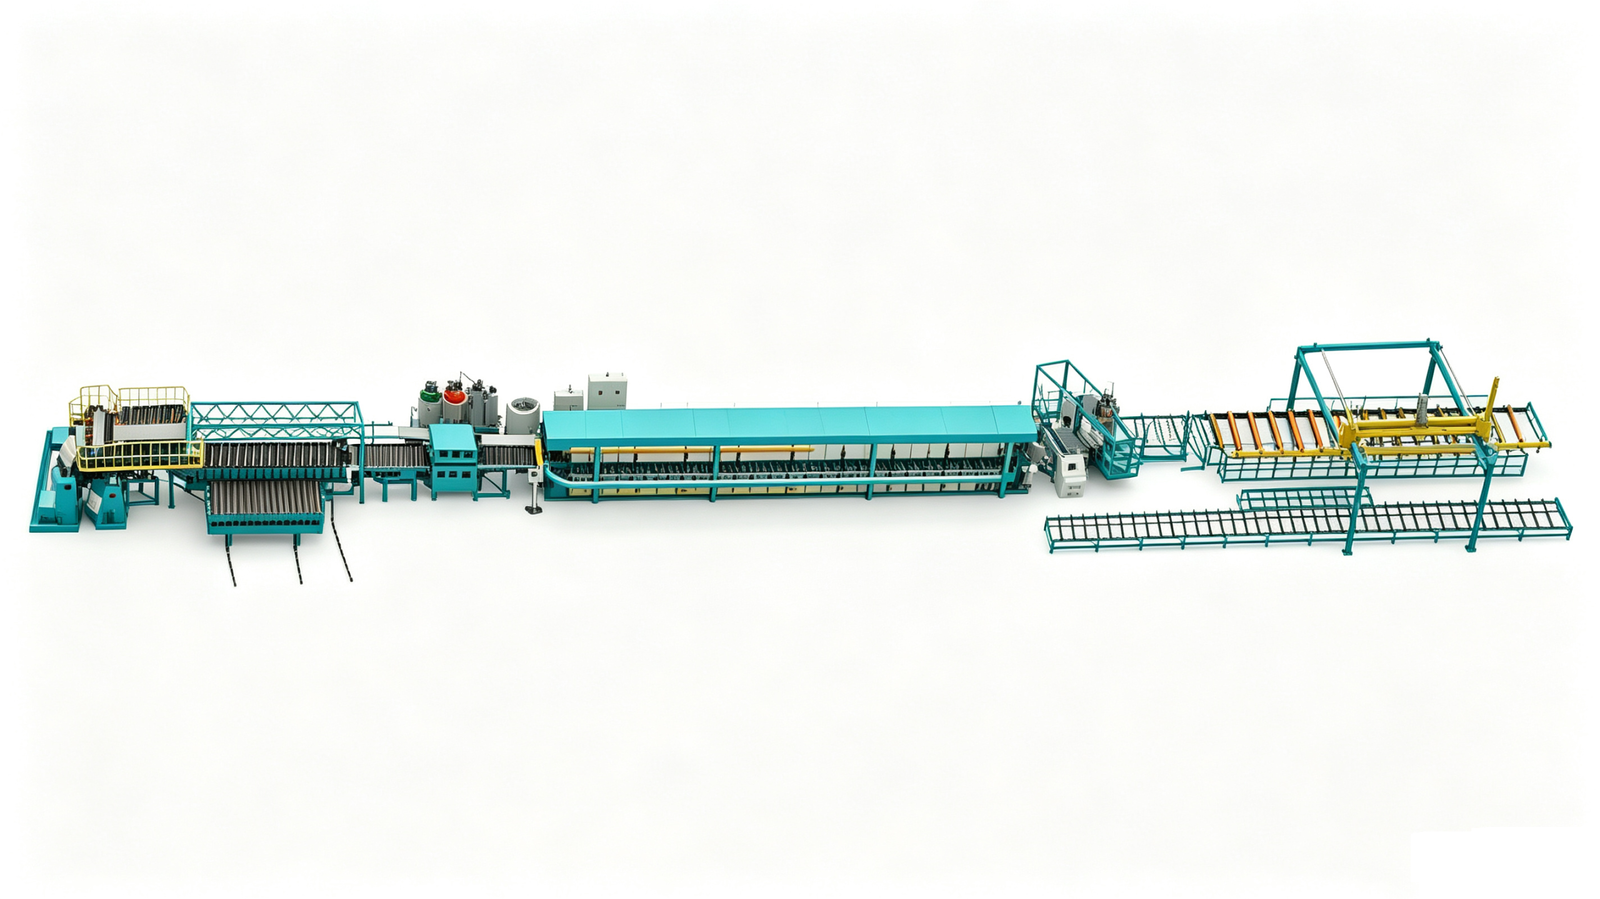
30 m continuous PIR panel configuration with metering, laydown, heated lamination and synchronized cutting. Finished-panel fire classification depends on the tested construction. Concept illustration — not a photograph of delivered equipment or a customer installation.
Max Line Speed
15 m/min listed limit; actual cure speed selected for the recipe
Double Belt Length
30 m — Continuous heated track
Panel Qualification
Fire classification requires finished-panel testing
Thickness Range
30–200 mm — Broad application scope
Product Overview
Concept illustration — not a photograph of delivered equipment or a customer installation.
Concept illustration — not a photograph of delivered equipment or a customer installation.
The Haifeng HF-PIR-30M is an automated continuous lamination line designed for high-performance polyisocyanurate (PIR) insulated panels. Combining high-pressure oscillating injection, heated 30-meter caterpillar double belts, and automated packaging systems, it satisfies global demands for cold storage envelopes and architectural facades.
Explore the application solution: Industrial Building Sandwich Panel Production Solution. This solution describes a separate 24 m reference line operating at 3–9 m/min.
Related project: Industrial Plant PIR Sandwich Panel Line. The project records sustained 12 m/min operation on 50 mm wall panels with a 30 m double belt; this is separate from the product's listed 15 m/min maximum line speed.
Production Workflow
Coil Uncoiling & Cold Roll Forming
Steel sheets are cold-rolled into architectural wall or roof profiles
Preheating
Sheet surfaces pass through hot-air tunnels to reach 45°C
High-Pressure PIR Dispensing
Servo oscillating head deposits pentane-blown PIR chemicals evenly
Double-Belt Continuous Curing
30-meter caterpillar maintains uniform hydraulic pressure at 65°C
Synchronous Flying Cut
Disc saw tracks panel movement and cuts to length without stopping
Inline Cooling & Stacking
Turnover rack vents core heat before automated shrink wrapping
Technical Specifications
Supplied HF-PIR-30M configuration references. Speed, thickness and dosing limits are not simultaneous guaranteed working points; actual production depends on cure and material duty.
| Technical Parameter | HF-PIR-30M |
|---|---|
| Components | Multi-Component (Polyol, Isocyanate, Pentane, Catalyst) |
| Output Range (g/s) | 60 – 200 kg/min (Customizable) |
| Mixing Ratio Range | 100:100 to 100:250 (High Isocyanate Index) |
| Ratio Accuracy | ±0.5% (Closed-loop flowmeter telemetry) |
| Power Supply | 380V / 50Hz, 3-Phase (Or 480V 60Hz Custom) |
| Working Pressure | 150 – 200 bar (High-pressure impingement) |
| Tank Capacity (L) | 500 L Stainless Steel Jacketed Tanks |
| Weight | Approx. 85 Tons |
| Dimensions (L×W×H) | 120m (L) × 4.5m (W) × 3.8m (H) |
| Double-Belt Caterpillar Length | 30 Meters |
| Panel Thickness Range | 30 mm – 200 mm |
| Maximum Line Speed | 15 m/min |
Key Features
PIR Recipe Control
Main components and additives are selected for the formulation; chemical index is not a certification.
30 m Continuous Belt
The listed 15 m/min upper limit is separate from thickness-specific stable production.
Pentane Handling
Configure detection, ventilation, isolation and interlocks. Certification requires documents for the actual ordered equipment.
Related Production Systems
Continuous Rock Wool Sandwich Panel Line | Insulation Panels
Sandwich Panel Production Lines
Continuous Phenolic Sandwich Panel Line | Insulation Panels
Sandwich Panel Production Lines
Continuous PU Sandwich Panel Line | Insulation Panels
High Pressure Polyurethane Machine


