Multi-shaft dispersion for PU resin and pigment batches is a mixing strategy built around a simple production fact: a high-viscosity resin does not wet or deagglomerate pigment uniformly in a single-shaft tank. A lab drawdown can pass while the production batch still carries soft agglomerates, streaking, or color drift. The multi-shaft disperser combines a slow anchor or wall-scraping shaft with one or more high-speed dispersing blades so the material is continuously turned, scraped, and sheared from the wall into the high-energy zone. The practical decision is not whether to agitate more, but how to specify shaft configuration, batch ratio, temperature control, and cleanout around the actual paste and production run.
Where Multi-Shaft Dispersion Fits in PU Production
Multi-shaft dispersion becomes necessary when the resin paste creates a significant viscosity gradient inside the mixing vessel. Polyester or filled polyol systems, high pigment loadings, flame retardants, conductive fillers, or thixotropic additives can all form a slow-moving layer near the vessel wall while the center remains fluid. A single high-speed shaft may leave that wall layer mostly untouched, so the final tint is dominated by whichever portion actually passed through the shear zone.
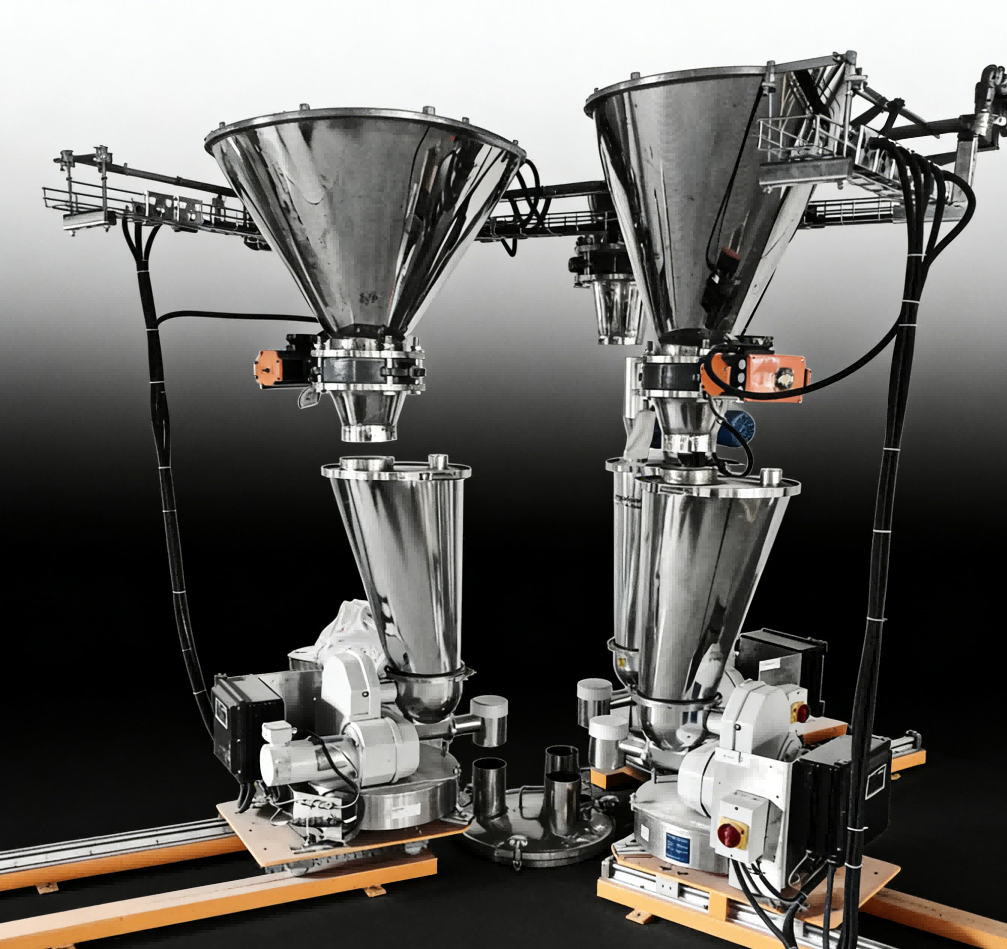
The typical configuration is a low-speed anchor or frame stirrer with wall scrapers, paired with one or more high-speed dispersing discs. The low-speed element moves bulk material, but the high-speed element breaks pigment agglomerates and wets solid surfaces. This combination matters more than adding motor power alone. The same drive power can appear to mix well while leaving dead zones, especially in shallow, wide vessels or when the batch is too large for the blade diameter.
For PU production, the output of the dispersion module is normally a tinted paste, filled resin masterbatch, or color-adjusted component that will later be metered into the main stream. Any variation in that paste becomes a ratio shift downstream. That is why the mixer should be treated as part of the metering loop, not as an isolated color kitchen.
Why Pigment Pastes Separate and What Multi-Shaft Mixing Changes
Pigment separation in a PU batch usually comes from four effects: wetting failure, density or particle-size differences, flocculation, and viscosity drift during temperature change. If the dispersing blade only works the center portion of the batch, unmixed material from the wall re-enters during discharge and creates color variation at the pour head.
A multi-shaft mixer changes the failure mode because the anchor or scraper continuously returns the wall layer to the shear zone. The high-speed blades still perform wetting and deagglomeration. However, shear alone does not guarantee dispersion. The paste needs enough residence time under the blades, a controlled temperature, and often vacuum to remove air introduced during powder incorporation. Under-dispersion frequently shows up as color shift after storage or as surface defects after casting, not as an immediate mixing failure.
| Production symptom | What to inspect first | Likely mixer contribution |
|---|---|---|
| Color shift after storage | Pigment wetting and fineness | Insufficient residence or recirculation |
| Streaks in cast PU | Wall layer returning | Poor wall scraping |
| Foam or voids | Vacuum and air entrainment | Missing deaeration step |
| Long dispersion time | Viscosity and blade size | Tip speed to vessel ratio is wrong |
| Batch-to-batch drift | Letdown and cleanout | Pigment residue or carryover |
| Temperature drift | Cooling jacket and sensor position | Shear heating too high |
Key Machine Design Inputs
Specify shaft configuration from the paste rheology, not from the mixer’s nominal capacity. The critical inputs are the gross vessel volume and working volume, the blade diameter relative to tank diameter, the speed range required at the process viscosity, and whether the wetted path tolerates the solvent and temperature used by the PU system. For most filled or pigmented resins, the high-speed blade should be sized so the material can fold from the wall into the blade zone without air entrainment. The low-speed element must be selected by torque at the highest operating viscosity, not only by motor power at water-like fluid values.
Temperature is the next constraint. Dispersing pigment into a reactive component or a heat-sensitive polyol can raise temperature quickly. A jacketed vessel or temperature probe becomes necessary when the paste contains a catalyst, blowing agent, or a pigment with a narrow heat-stability window. Cooling also prevents a viscosity drop from hiding incomplete dispersion. If the cooling jacket is undersized, the operator will reduce speed or shorten the cycle to stay under the temperature limit. That is how an otherwise correct mixer quietly loses dispersion ability.
Color paste dosing adds a separate question. Haifeng Polyurethane Machinery’s three-channel additive mixer is an example of a module that meters independent color pastes or liquid functional additives into the main PU material. Its three channels are independently controlled, handle a specified flow range from 0.1 to 100 g/s, and tolerate viscosity up to 10,000 mPa·s. A module like this links to the host PLC through Ethernet or RS485, but the dispersion step must still deliver a stable paste before the additive channel can dose it repeatably.
Batch Size and Cycle Time Calculation
Batch sizing starts with the paste consumption rate. Determine the required letdown mass per color from the shot weight per part, the number of shots per shift, and the pigment loading in the letdown. Over-sizing the dispersion vessel is a common error. A large vessel can still produce paste, but it may need longer incorporation time, a bigger heating or cooling load, and much larger cleanout effort. Under-sizing is more obvious: the paste cannot be produced in one pass, so operators split it and lose cycle time while adding contamination risk.
A practical design point is to keep the mixer working volume matched to the largest frequent batch, with an allowance for powder rise and blade circulation. Joint use by several colors means the cleanout time belongs in the cycle calculation. If a color change takes longer than the dispersion run, the multi-shaft mixer can become a bottleneck even though its blade speed is adequate.
Batch weight calculations feed mixer chamber sizing and pigment dosage correction. <How to Calculate Shot Weight in Polyurethane> covers shot-weight calculation for polyurethane dosing.
Specifying a Dispersion Module with Your PU Line
The mixer specification must reference the metering system. A stable dispersion loop usually includes a paste or pigment buffer tank, low-shear recirculation, closed-loop level or mass-flow control, and a purge path matched to the solvent used by the formulation. If the paste is fed into a multi-component metering machine, require a recipe that records agitator state, recirculation time, and the lot used for each tinted batch. This is important for traceability because color issues trend slower than ratio or pressure faults.
Color changeover should be specified as a sequence, not a single valve label. The sequence includes paste cut-off, solvent flush, air blow, and the reuse or disposal route for the flush mix. A well-designed module can bring this down to about two minutes, but only when the same cleaning solvent is compatible with all streams and the piping arrangement has no dead leg. If the line runs high-viscosity pastes, confirm the flush pressure and heated solvent path before accepting a stated changeover time.
For occasional colors, a smaller injection-style channel is usually more practical than forcing the main dispersion vessel to clean out after every low-volume tint. Reserve the multi-shaft vessel for high-use masterbatches or difficult pigments, and use the additive channels for small, frequently changed tints. That split protects both the dispersion quality and the production schedule.
Commissioning and QC Checks
Validate the disperser on the same raw material lots and temperature profile as production. A water trial proves shaft rotation, but it does not prove pigment wetting or wall cleanout in a filled PU paste. Use a base batch to check the low-speed element, then introduce pigment progressively while recording speed, amperage, vacuum, and temperature. The required fineness value should come from the pigment or PU system supplier, not from a generic plant rule.
A simple acceptance group can include: no visible agglomerates on a drawdown or cast sample at the agreed film thickness; viscosity within the supplier’s control window after 24 hours; color difference within the agreed limit after a storage cycle; cleanout time and residue weight within the planned cycle; and repeatable batch-to-batch color after three consecutive runs. If the paste is let down later, test the final part color in the actual letdown ratio rather than only approving the concentrated paste. This catches conditions that pass a concentrated drawdown but fail after final metering.
Specify the Mixer Around Your Paste, Not the Reverse
The most useful inquiry starts with the paste definition, because the mixer is downstream of the formulation and upstream of the metering accuracy. Send the resin system, pigment type and loading, paste viscosity at operating temperature, batch size, color changeover frequency, temperature limit, available cleaning solvent, and the fineness target you must hold. From those inputs, Haifeng Polyurethane Machinery can define the shaft configuration, cooling, vacuum, PLC recipe, and additive-channel interface for the production cell rather than starting from a catalog size.
Contact Haifeng Polyurethane Machinery at Info@chinahaifeng.com or WhatsApp: 86 13566296633 with the resin, pigment, batch, and letdown information above.
FAQ
How many shafts do we need for pigmented PU resin?
Start from the wall behavior, not an arbitrary shaft count. If the paste forms a thick wall layer or has filler settlement, a slow anchor or frame shaft with wall scrapers plus one or two high-speed dispersing blades is common. A single shaft can be enough for low-viscosity, easy-wetting pigments in small batches. Use the batch geometry and viscosity curve to justify the extra shaft. Adding a shaft without a clear wall-clearance or torque problem increases power, cleaning, and maintenance cost.
Does multi-shaft dispersion replace the metering machine’s dynamic mixer?
No. The dispersion vessel or paste module prepares a stable tint or masterbatch. The metering machine’s mixing head still performs final A/B mixing and shot distribution. They are linked because variation in the paste changes the ratio at the pour head, but one cannot replace the other. Specify the interface carefully: buffer tank capacity, recirculation, recipe selection, and purge sequence all need to be agreed between the dispersion module and metering line.
What viscosity range is appropriate for a multi-shaft disperser?
That depends on the shaft, blade, and tank design. Typical paste systems may run from a few thousand mPa·s to well above the range of ordinary stirring; the existing three-channel additive module mentioned above states compatibility up to 10,000 mPa·s for metering color pastes or liquid additives. Confirm the mixer’s torque and tip speed at your highest operating viscosity, not at water. Also confirm whether vacuum or heated walls are required. A single viscosity limit without shear rate and temperature is not a complete specification.
Can we use one mixer for multiple colors?
Yes, when the colors are ordered to reduce carryover and the cleanout time is accepted in the production plan. Light shades after dark pigments are the highest risk. A separate small additive channel or replaceable paste insert makes more sense for frequent low-volume colors. If the main vessel handles many colors, inspect the wall scraper clearance, shaft seals, and purge path closely, because pigment tends to settle in the same places every cycle. Do not assume a two-minute flush applies to every pigment sequence unless the supplier has verified the actual pair.
What is the main sign that a batch is under-dispersed?
The earliest sign is often not the liquid color. It appears after letdown or after a storage cycle as color drift, surface specking, or a cast part with soft pigment streaks. A fineness gauge drawdown catches many agglomerate problems before the batch leaves the vessel. If the paste passes a concentrated drawdown but the final part drifts, test the letdown ratio and the recirculation path. A stable dispersed paste may still fail if the pigment is not fully wetted or if settled material returns during discharge.
If you’re interested, check out these related articles:
SRIM Explained Structural Reaction Injection Molding Basics
Shore A Vs Shore D Hardness In Polyurethane
How To Calculate Shot Weight In Polyurethane
How Polyurethane Rollers Are Made From Casting To Cure
RRIM Vs RIM Which Process Suits Your Structural Part