Pot life is one of the most routinely misread values on a polyurethane data sheet. A processor sees a four-minute figure, adds a thirty-second pour buffer, and still discovers that viscosity is climbing inside the mixing head. The problem is rarely the value itself. It is the gap between the conditions used to measure that value and the conditions on the production floor.
What Pot Life Is — and What It Is Not
Pot life, also called working life, is the interval from the moment the components are mixed until the material reaches a point where it can no longer be poured, injected, spread, or cast without an unacceptable rise in defect risk [1]. For most polyurethane systems, that point is defined by viscosity increase, loss of flow, or the onset of gelation rather than by full cure.
Pot life is not cure time. A system can have a four-minute pot life and a thirty-minute demold time. Another can have a twenty-minute working window and a six-hour cure. The two values describe different stages of the reaction, and mixing them up is a common cause of under-sized equipment and rushed mold filling.
The Variables That Move Pot Life
A pot life value is only meaningful when the test conditions are stated. The same mixed system will show different working windows depending on four factors.
Material temperature. Reaction rate rises with temperature. As a general rule, a 10 °C increase can roughly halve pot life, while a 10 °C decrease can extend it [2]. A material tested at 25 °C in the laboratory will not behave the same way when it leaves a day tank at 45 °C.
Mixing ratio and catalyst package. A small deviation in the A:B ratio or a catalyst level change can shift pot life without changing the final hardness specification. This is why ratio drift on a worn metering pump often appears first as a process problem, not as an obvious property failure.
Moisture. Water reacts with isocyanate and accelerates thickening. On a humid day, a nominally identical batch can reach end of pot life sooner, especially if containers, hoses, or molds are not dry.
Mass and surface area. A large mass of mixed material retains exotherm and self-heats, shortening the working window. The same material spread in a thin layer can remain workable longer. Bench tests should therefore mimic the actual pour mass, not just the actual temperature.
How to Measure Pot Life in Practice
Three methods cover most production needs.
1. Viscosity curve. This is the most repeatable method. Condition the material to the intended processing temperature, mix a representative batch, and record viscosity at fixed intervals until viscosity doubles or reaches a defined upper limit [3]. The result is a curve, not a single point, and it shows whether the system fails gradually or abruptly.
2. Foam cup test for foaming systems. For polyurethane foam, the useful reference points are cream time, gel time, and rise time [4]. Pot life is not the same as rise time. Rise time describes foam growth after the material has already begun to expand, while pot life is the working limit for dispensing or mold filling before the reaction closes the window.
3. Production-floor validation. After the bench test, run the same formulation through the actual machine path: tank, heat exchanger, hoses, mixing head, and mold. This catches variables the bench cannot see, including residence time in recirculation lines and heat pickup from the pump.
On foam lines, operators often confuse rise time with pot life because both are reported in seconds. <The Role Of Rise Time In Polyurethane Foaming> covers rise-time measurement and where it sits in the reaction timeline.
From Bench Number to a Real Dispense Window
A bench pot life of 240 seconds does not give you 240 seconds of usable dispensing. The practical dispense window is the bench result minus the time consumed by mixing, transfer, mold approach, and a process margin.
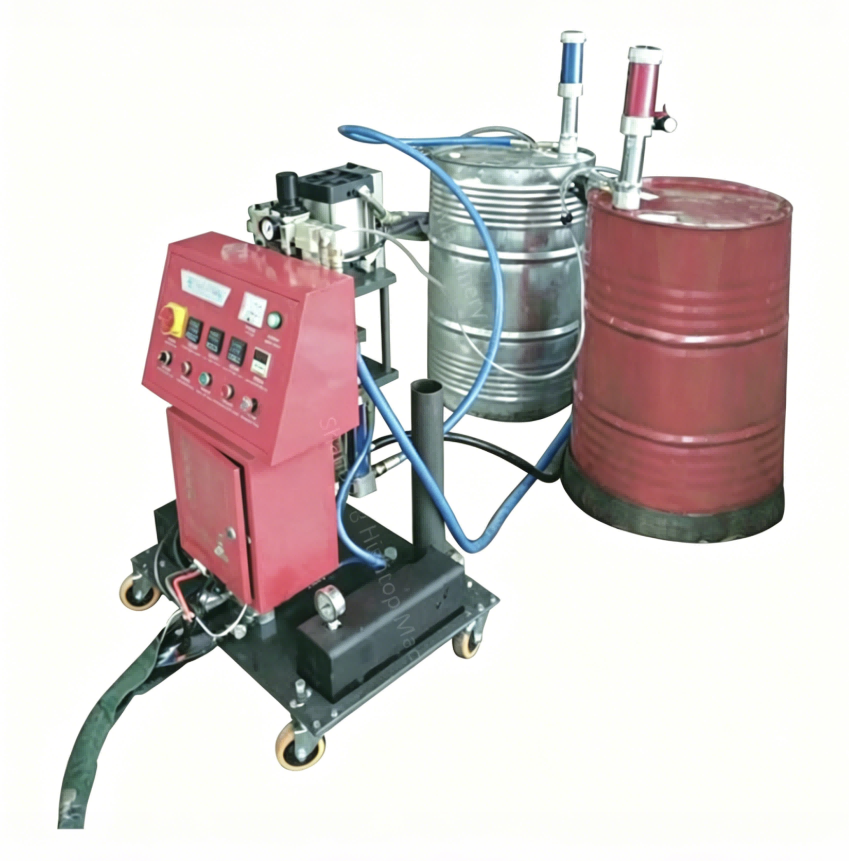
On a low-pressure casting line, that margin can be consumed quickly. Material sitting in a long hose or a poorly flushed mixing head accumulates residence time before it even reaches the mold. If the machine recirculates mixed material, the clock starts earlier than the operator thinks. Equipment with short mix-head paths, precise metering, and controlled tank temperature keeps the measured bench window from being wasted before the pour begins.
Pot life is useful only when it is matched to a repeatable pour-to-cure sequence. <How Polyurethane Rollers Are Made From Casting To Cure> covers the casting sequence and why the dispense window drives roller quality.
Once the working window is known, the next constraint is how much material can be moved inside it. This is where shot weight enters the calculation. If one mold cavity requires more material than the machine can accurately deliver inside the pot life window, the operator compensates by pouring faster, which usually introduces turbulence, air entrapment, or ratio deviation.
A measured pot life is only half the planning equation; the other half is how much each shot must weigh. <How To Calculate Shot Weight In Polyurethane> covers shot size calculation and its effect on dispense timing.
Need to match a measured pot life to equipment timing? Send your material names, bench result, test temperature, and target cycle time to Info@chinahaifeng.com or WhatsApp +86 135 6629 6633. Include the shot weight and the current mix-head type; that is enough to work out whether the dispense window is the constraint or the machine cadence is.
Pot Life Measurement Checklist
- Record the test temperature, relative humidity, and batch size with every pot life result.
- Use the same A:B ratio and mixing speed as the production line, not a hand-mix convenience sample.
- Measure viscosity at fixed intervals rather than relying on a single gel point.
- For foam systems, record cream time, gel time, and rise time separately.
- Test at the actual pour mass to capture exotherm effects.
- Validate the bench result through the machine path before locking the dispense window.
- Re-test when the catalyst lot, polyol lot, or isocyanate index changes.
Choose Equipment Around the Window, Not Around the Machine
If the current machine cannot dispense inside the measured pot life, the answer is not always a faster pour. It may be lower material temperature, shorter hose length, better metering stability, or a mix head that flushes cleanly between shots. Start from the material window and specify the equipment backward from there.
For help with metering accuracy, temperature control, or mix-head selection matched to your pot life data, contact Haifeng Polyurethane Machinery at Info@chinahaifeng.com or WhatsApp +86 135 6629 6633.
Frequently Asked Questions
What is the difference between pot life and cure time?
Pot life describes how long a mixed material remains workable for pouring or injection. Cure time describes when the part reaches handling or demold strength. A short pot life does not automatically mean a fast cure, and a long pot life does not guarantee a slow cure.
Does higher temperature always shorten pot life?
In most polyurethane systems, higher temperature shortens pot life because the reaction accelerates. The relationship is not linear, and moisture or mass effects can override a small temperature change. This is why the temperature must be stated with every measurement.
Can I determine pot life from a technical data sheet without running a test?
A data sheet value is a starting point, not a production guarantee. Use it to plan a bench test, then validate the result under your actual temperature, ratio, and pour mass. The same formulation can behave differently on a humid day or with a new raw material lot.
Is rise time the same as pot life for foam systems?
No. Rise time measures foam expansion after the reaction has progressed. Pot life is the earlier working limit for dispensing or mold filling. Confusing the two is a common cause of late pours and partially filled molds.
How can I extend pot life without changing the formulation?
Lower the material temperature, reduce the batch size to limit exotherm, dry the containers and molds, and shorten the time between mixing and dispensing. These changes must be verified against final part properties.
References
[1] ISO 10364:2007, Structural adhesives — Determination of the pot life (working life) of multi-component adhesives. International Organization for Standardization, Geneva, 2007.
[2] G. Oertel, Polyurethane Handbook, 2nd ed. Munich: Hanser Publishers, 1994.
[3] ISO 9514:2019, Paints and varnishes — Determination of the pot life of liquid systems — Preparation and conditioning of samples and guidelines for testing. International Organization for Standardization, Geneva, 2019.
[4] ASTM D7487-18, Standard Practice for Polyurethane Raw Materials: Polyurethane Foam Cup Test. ASTM International, West Conshohocken, PA, 2018.
If you’re interested, check out these related articles:
SRIM Explained Structural Reaction Injection Molding Basics
Shore A Vs Shore D Hardness In Polyurethane
How Polyurethane Rollers Are Made From Casting To Cure
RRIM Vs RIM Which Process Suits Your Structural Part