
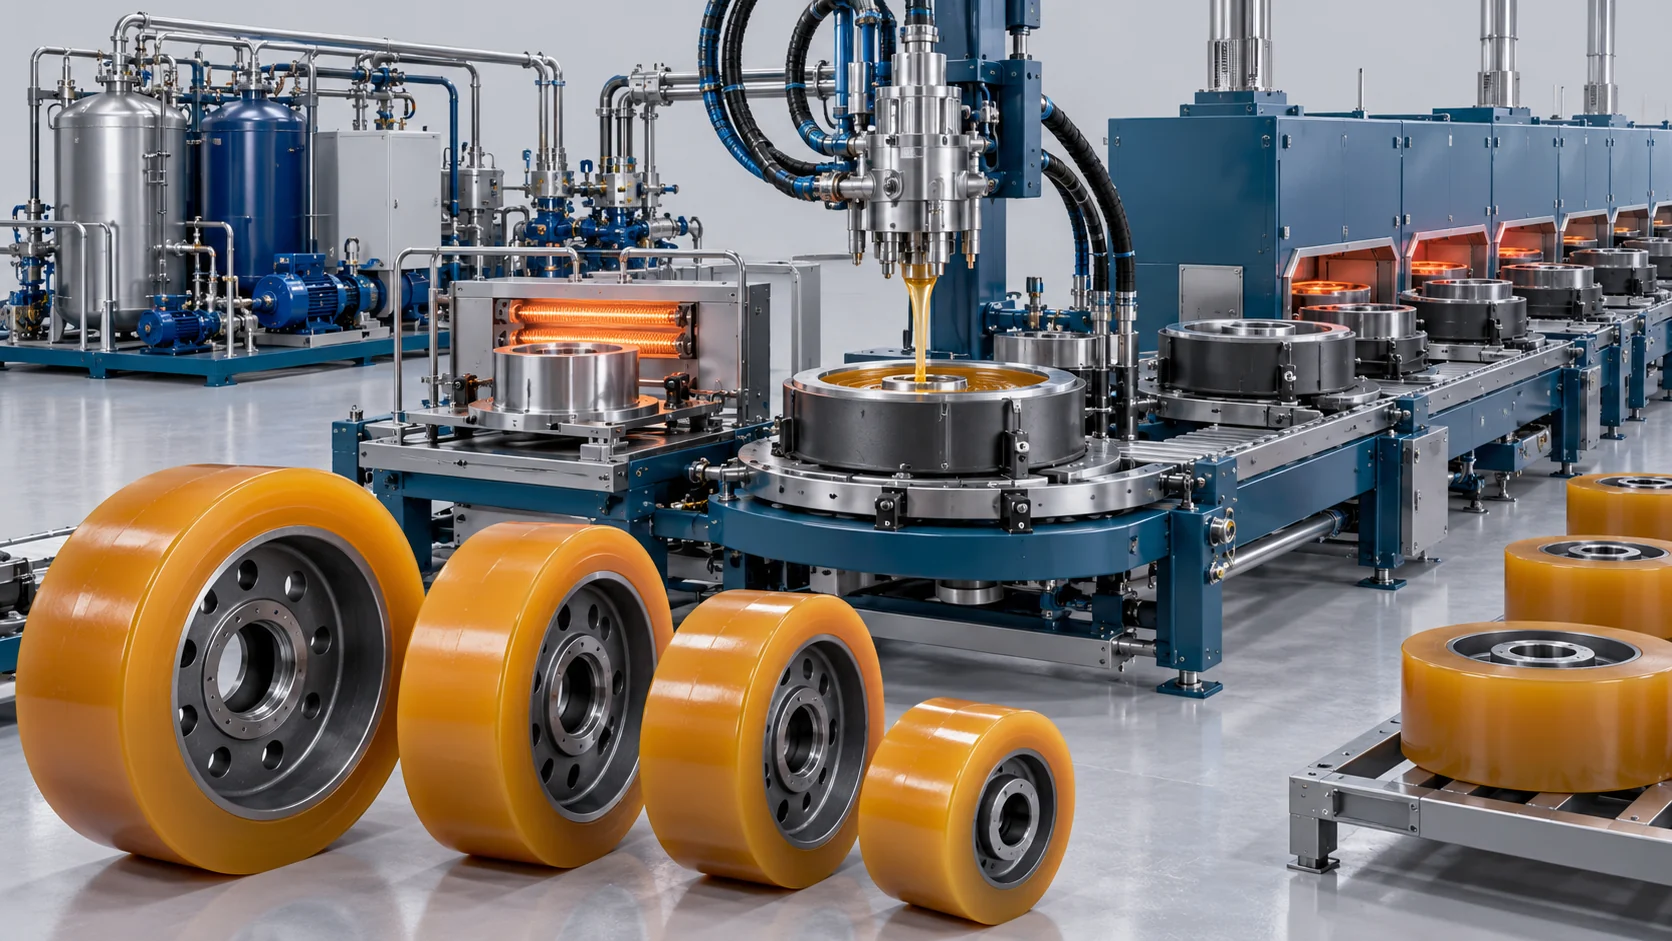
Heavy-Duty Solid Wheel Casting Solution
Configured polyurethane solid-wheel production with core preparation interfaces, induction preheating, dual-flow dispensing and indexed mold curing.
Extreme Interfacial Bonding for Heavy-Load Material Handling Wheels
Configured polyurethane solid-wheel production with core preparation interfaces, induction preheating, dual-flow dispensing and indexed mold curing. The package covers material preparation, dual-flow dynamic mixing, induction hub preheating, the specified heated mold line and controls. Automatic blasting/cleaning and hydraulic demolding are optional. Prepolymer and bonding agents are supplied separately; site power and compressed air are customer interfaces. Capacity depends on parallel mold positions, cycle stages and product size.
Hub Induction Preheating
The specified induction stage conditions the metal hub; adhesive selection and actual bonding performance require validation.
Dual-Flow Dispensing
Programmed leading and main-fill rates are selected for hub clearance and tread cavity geometry.
The equipment package is selected against finished-part geometry, material, output target and factory interfaces. Material properties, life comparisons and inspection results require project-specific test records.
Turnkey Automated Wheel Casting Workflow
A synchronized, automated manufacturing sequence from raw metal hub preparation to finished solid polyurethane wheels.
Hub Surface Blasting & Bonding Primer Coating
Forged steel or cast iron wheel cores are automatically grit-blasted to Sa 2.5 cleanliness and spray-coated with Chemlok adhesive in an automated booth.
Medium-Frequency Rapid Induction Heating
The primed cores pass through an automated induction coil, heating the metal to 90°C ± 2°C in 45 seconds to activate adhesive bonding groups.
High-Accuracy Closed-Loop Servo Metering
Servo gear pumps meter MDI prepolymer and 1,4-BDO crosslinker through heated lines under Coriolis feedback, holding mix ratio accuracy within ±0.2%.
Reference Solution Engineering Envelope
Supplied configuration references. Values depend on the stated formulation, tool and operating conditions; component qualification and reported project outcomes require separate records.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Continuous Casting Output | 2.0 to 18.0 kg/min | Dual-flow matrix servo gear pump skid |
| Induction Preheating Rate | 45 seconds per hub | Medium-frequency automated induction heating unit |
| Target Metal Hub Temperature | 90°C ± 2°C | Infrared pyrometer closed-loop temperature control |
| Interfacial Bonding Strength | Greater than 30 kN/m | ASTM D429 Method B 90° peel adhesion test; original specimen and method records require verification |
| Dispensing / Indexing Reference | Less than 90 seconds | Distinct from 15-minute mold cure; actual sequence to be verified |
| Daily Shift Wheel Capacity | Up to 800 finished wheels | Supplied brief reference; requires confirmed parallel positions/cavities, line balance and shift records |
Core Equipment for This Solution
The package covers material preparation, dual-flow dynamic mixing, induction hub preheating, the specified heated mold line and controls. Automatic blasting/cleaning and hydraulic demolding are optional. Prepolymer and bonding agents are supplied separately; site power and compressed air are customer interfaces. Capacity depends on parallel mold positions, cycle stages and product size.
Core Advantages of Haifeng Wheel Systems
Configured process controls and engineering interfaces for the selected equipment package.
Hub Induction Preheating
The specified induction stage conditions the metal hub; adhesive selection and actual bonding performance require validation.
Dual-Flow Dispensing
Programmed leading and main-fill rates are selected for hub clearance and tread cavity geometry.
Material and Endurance Testing
Rolling heat and bond durability are verified for wheel size, compound, load and speed rather than inferred from the dispenser.
Indexed Production Interfaces
Mold indexing and curing can operate in parallel. Total output requires a complete line balance and operating record.
Related Project Draft
Review the project configuration described in the supplied brief. Project records and reported results require verification before public use.
Frequently Asked Questions
Find answers about Heavy-Duty Solid Wheel Casting Solution, including material selection, equipment configuration and the information needed to plan a production line.
How are hub preheating and bonding targets validated?
How does dispensing time differ from in-mold curing time?
How are wheel rolling temperature and durability verified?
How is the complete wheel-line shift output established?
Request a Solid Wheel Casting Equipment Proposal
Share the finished part or drawing, material system, target capacity, automation requirements and factory utilities so the equipment and tooling interfaces can be discussed.


