
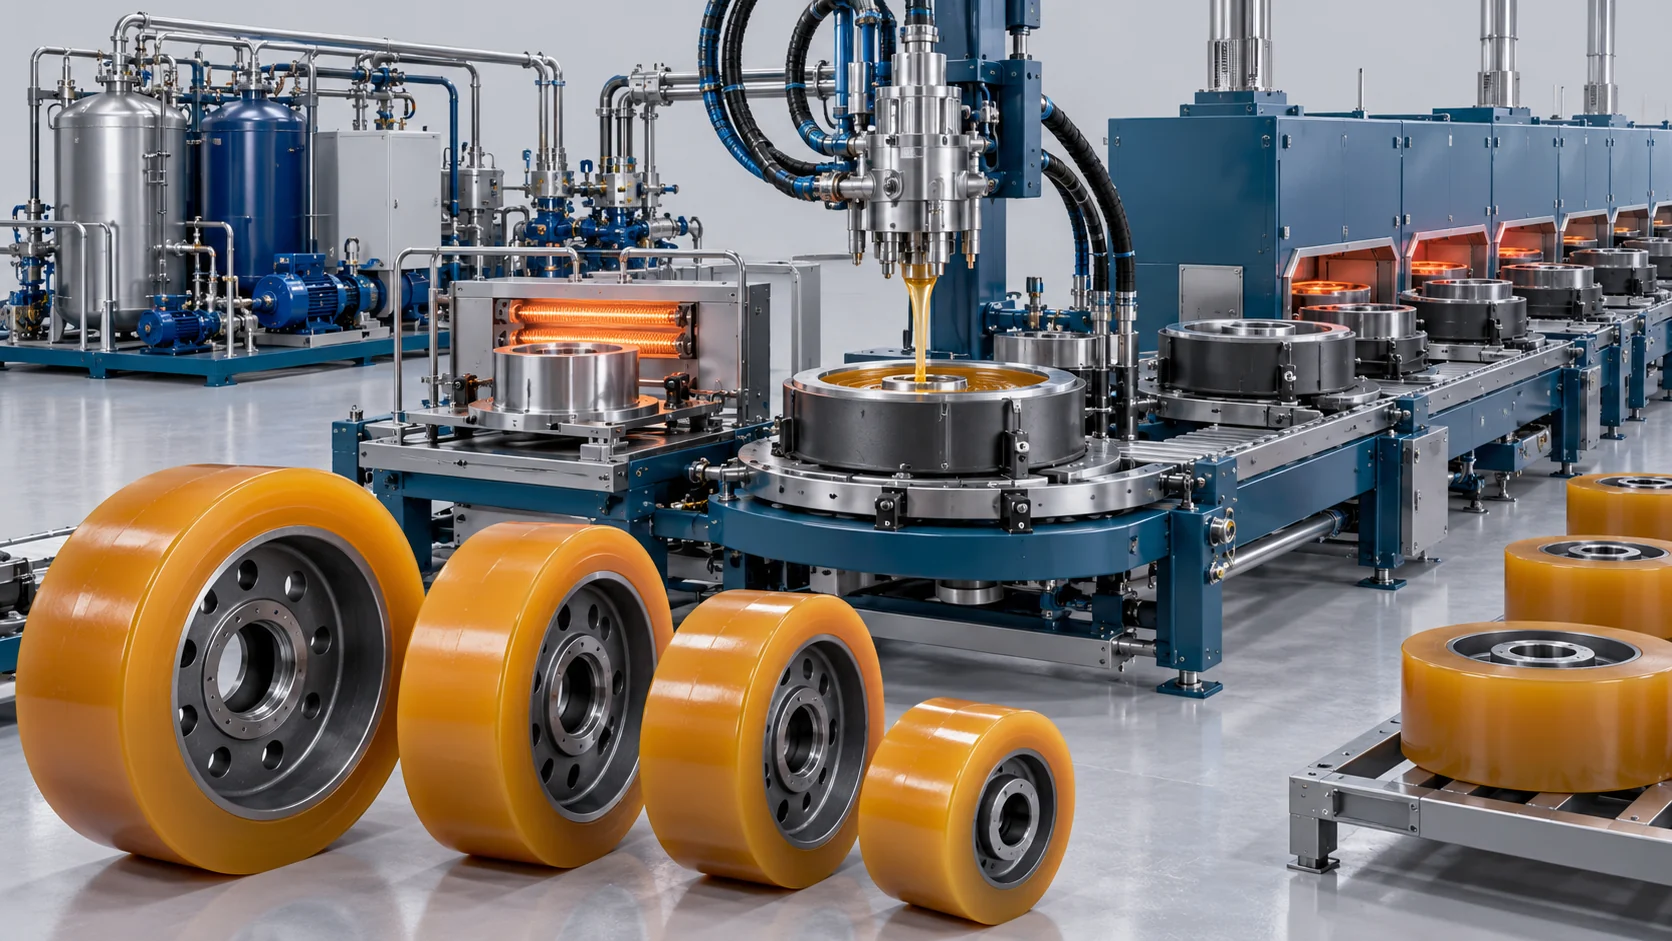
حل صب العجلات الصلبة للخدمة الشاقة
إنتاج مُهيَّأ لعجلات البولي يوريثان الصلبة، يشمل واجهات تجهيز القلب والتسخين المسبق بالحث والتوزيع ثنائي التدفق والمعالجة في قوالب مُفهرسة.
Extreme Interfacial Bonding for Heavy-Load Material Handling Wheels
Configured polyurethane solid-wheel production with core preparation interfaces, induction preheating, dual-flow dispensing and indexed mold curing. The package covers material preparation, dual-flow dynamic mixing, induction hub preheating, the specified heated mold line and controls. Automatic blasting/cleaning and hydraulic demolding are optional. Prepolymer and bonding agents are supplied separately; site power and compressed air are customer interfaces. Capacity depends on parallel mold positions, cycle stages and product size.
Hub Induction Preheating
The specified induction stage conditions the metal hub; adhesive selection and actual bonding performance require validation.
Dual-Flow Dispensing
Programmed leading and main-fill rates are selected for hub clearance and tread cavity geometry.
Balance hub preparation, induction preheat, dosing, indexing and mold cure as separate stages. Parallel tooling can change the output interval, but it does not shorten the material cure automatically. Verify bonding and wheel endurance on the intended assembly.
Turnkey Automated Wheel Casting Workflow
A synchronized, automated manufacturing sequence from raw metal hub preparation to finished solid polyurethane wheels.
Hub Surface Blasting & Bonding Primer Coating
Forged steel or cast iron wheel cores are automatically grit-blasted to Sa 2.5 cleanliness and spray-coated with Chemlok adhesive in an automated booth.
Medium-Frequency Rapid Induction Heating
The primed cores pass through an automated induction coil, heating the metal to 90°C ± 2°C in 45 seconds to activate adhesive bonding groups.
High-Accuracy Closed-Loop Servo Metering
Servo gear pumps meter MDI prepolymer and 1,4-BDO crosslinker through heated lines under Coriolis feedback, holding mix ratio accuracy within ±0.2%.
النطاق الهندسي للحل المرجعي
مراجع التكوين المورَّدة. تعتمد القيم على التركيبة والتجهيزات القالبية وظروف التشغيل المذكورة؛ وتتطلب مؤهلات المكوّنات ونتائج المشروع المُبلَّغ عنها سجلات منفصلة.
| المعامل | القيمة / الوحدة | التكوين / الظروف المطبَّقة |
|---|---|---|
| Continuous Casting Output | 2.0 to 18.0 kg/min | Dual-flow matrix servo gear pump skid |
| Induction Preheating Rate | 45 seconds per hub | Medium-frequency automated induction heating unit |
| Target Metal Hub Temperature | 90°C ± 2°C | Infrared pyrometer closed-loop temperature control |
| Interfacial Bonding Strength | Greater than 30 kN/m | ASTM D429 Method B 90° peel adhesion test; applies to the selected specimen and method |
| Dispensing / Indexing Reference | Less than 90 seconds | Distinct from 15-minute mold cure; actual sequence to be verified |
| Daily Shift Wheel Capacity | Up to 800 finished wheels | Planning reference for the agreed parallel positions, cavity count, line balance and shift schedule |
المعدات الأساسية لهذا الحل
The linked automatic wheel line has selected hub-heating, dispensing and heated-mold interfaces; preparation and removal automation must be itemized.
Core Advantages of Haifeng Wheel Systems
ضوابط عملية وواجهات هندسية مُهيّأة لحزمة المعدات المختارة.
Hub Induction Preheating
The specified induction stage conditions the metal hub; adhesive selection and actual bonding performance require validation.
Dual-Flow Dispensing
Programmed leading and main-fill rates are selected for hub clearance and tread cavity geometry.
Material and Endurance Testing
Rolling heat and bond durability are verified for wheel size, compound, load and speed rather than inferred from the dispenser.
Indexed Production Interfaces
Mold indexing and curing can operate in parallel. Total output requires a complete line balance and operating record.
مشاريع ذات صلة
The AGV wheel case does not by itself establish all forklift loads, rolling heat or endurance; match wheel design and service conditions.
الأسئلة الشائعة
Find answers about Heavy-Duty Solid Wheel Casting Solution, including material selection, equipment configuration and the information needed to plan a production line.
How are hub preheating and bonding targets validated?
How does dispensing time differ from in-mold curing time?
How are wheel rolling temperature and durability verified?
How is the complete wheel-line shift output established?
ما المدخلات اللازمة لهذا التكوين؟
How should a complete wheel-line shift output be calculated?
Request a Solid Wheel Casting Equipment Proposal
Share the following for this application: Wheel/hub CAD, covering thickness, material/primer, preheat, shot, molds, load/speed and shift requirements. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


