
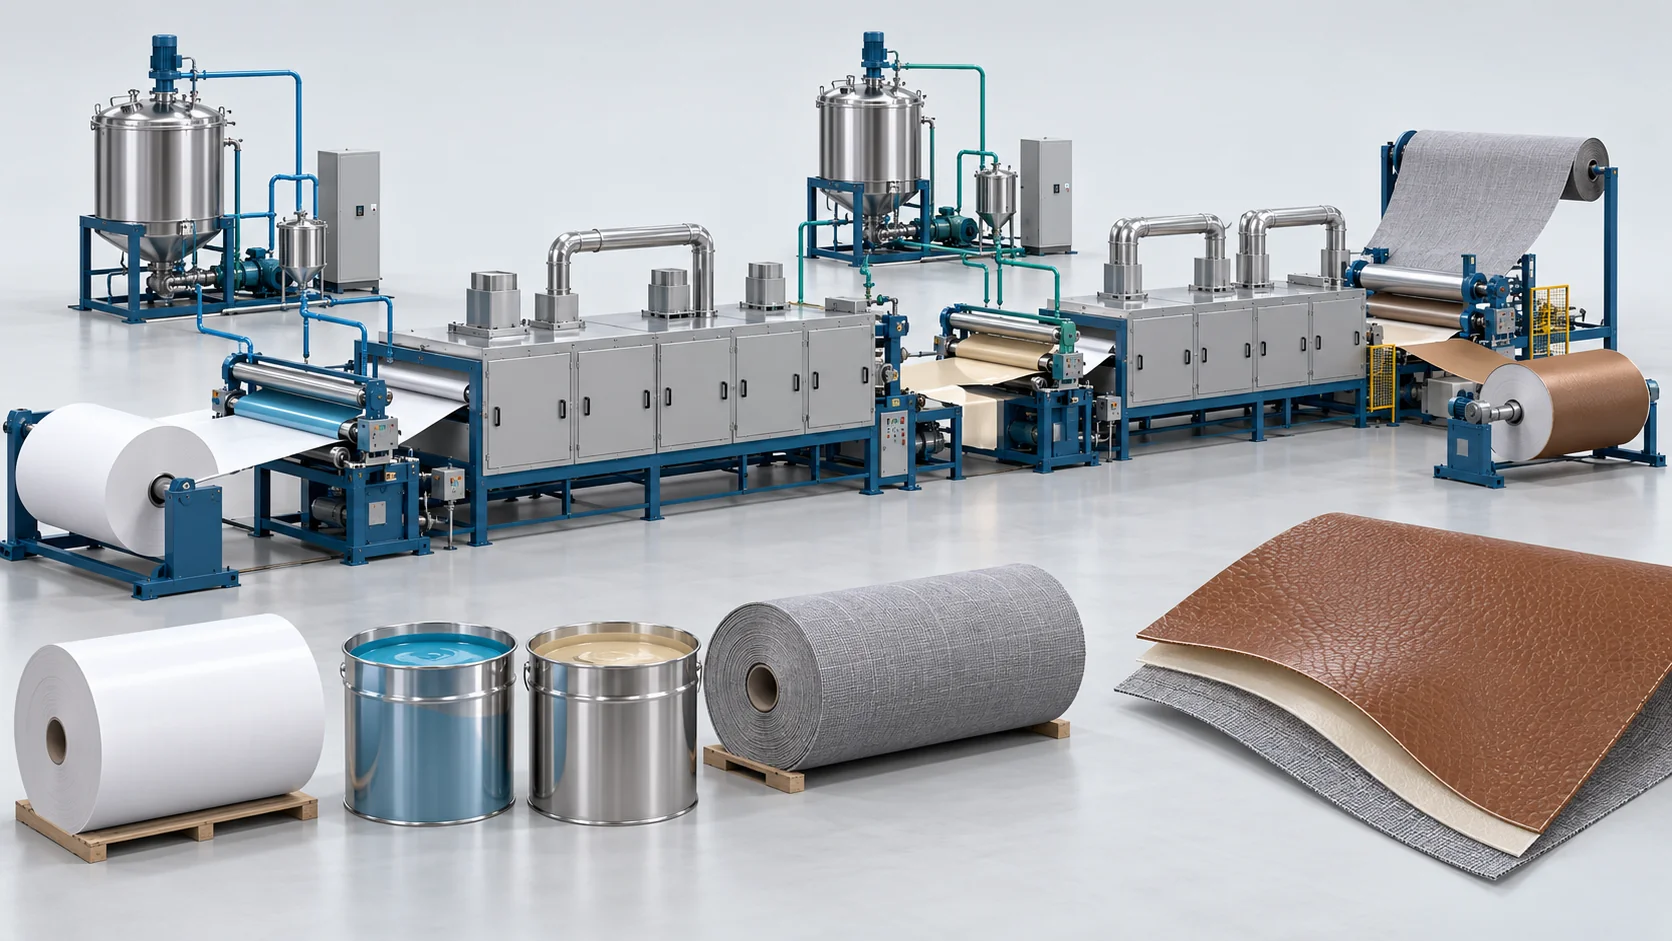
Dry-Process Transfer Coating Solution
Release-paper topcoat and adhesive delivery, coordinated drying and lamination for dry-process PU synthetic leather.
High-Peel, Cold-Flex Mechanical Superiority for Athletic Footwear
Release-paper topcoat and adhesive delivery, coordinated drying and lamination for dry-process PU synthetic leather.
Equipment and process scope
Topcoat supply, proportioned adhesive stream, coating dies, ovens, laminator and winding interfaces; release paper, fabric, resin chemistry and solvent recovery are specified separately.
Validation and production planning
Topcoat and adhesive circuits have different chemistry and rates. Dry-process is not synonymous with solvent-free. Flex testing, coating peel strength and VOC performance require substrate, temperature, thickness, conditioning and original reports; finished leather results are not equipment certifications. ISO 5423 is a polyurethane industrial-boot specification; citing it alone does not establish a general synthetic-leather cold-flex method. Identify the applicable annex, material scope and report.
Topcoat supply, proportioned adhesive stream, coating dies, ovens, laminator and winding interfaces; release paper, fabric, resin chemistry and solvent recovery are specified separately. Topcoat and adhesive circuits have different chemistry and rates. Dry-process is not synonymous with solvent-free. Flex testing, coating peel strength and VOC performance require substrate, temperature, thickness, conditioning and original reports; finished leather results are not equipment certifications. ISO 5423 is a polyurethane industrial-boot specification; citing it alone does not establish a general synthetic-leather cold-flex method. Identify the applicable annex, material scope and report.Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Turnkey Release Paper Transfer Coating Workflow
Configuration sequence from the supplied brief. Material, tool, pressure/temperature basis and complete line balance require verification. Topcoat and adhesive circuits have different chemistry and rates. Dry-process is not synonymous with solvent-free. Flex testing, coating peel strength and VOC performance require substrate, temperature, thickness, conditioning and original reports; finished leather results are not equipment certifications. ISO 5423 is a polyurethane industrial-boot specification; citing it alone does not establish a general synthetic-leather cold-flex method. Identify the applicable annex, material scope and report.
Continuous Flying-Splice Paper Unwinding
Supplied process reference: Textured silicone release paper is unwound through dual flying-splice turrets, with servo dancer rolls holding tension within ±2 N.
Enclosed Slot Die Topcoat Application
Supplied process reference: High-viscosity polyether resin is extruded through an enclosed slot die across 1,420 mm paper, holding thickness variance within ±1.5 µm.
Primary Multi-Zone Progressive Drying
Supplied process reference: The web passes through a 30m convection tunnel (75–125°C), evaporating carrier solvents and crosslinking the polyurethane skin.
Reference Solution Engineering Envelope
Supplied configuration and validation references; material/component results are separate from equipment ratings.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Working Web Coating Width | Up to 1,600 mm | Precision enclosed slot die and reverse roll stations; supplied configuration or material target, pending the applicable original records |
| Release Paper Tension Precision | Within ±2.0 N | Closed-loop servo floating dancer arm feedback; supplied configuration or material target, pending the applicable original records |
| Liquid Coating Thickness Profile | 0.05 to 0.25 mm | Tolerance held strictly within ±1.5 µm across web; supplied configuration or material target, pending the applicable original records |
| Cold-Flex Fatigue Resistance | Greater than 200,000 Cycles | Bally flexometer tested at -20°C under ISO 5423; supplied configuration or material target, pending the applicable original records |
| Interfacial Peel Bond Strength | Greater than or equal to 60 N/3cm | ISO 2411 testing on high-density microfiber substrates; supplied configuration or material target, pending the applicable original records |
| Synchronized Production Line Speed | 10.0 to 30.0 m/min | Multi-zone hot air convection drying tunnels; supplied configuration or material target, pending the applicable original records |
Core Equipment for This Solution
Topcoat supply, proportioned adhesive stream, coating dies, ovens, laminator and winding interfaces; release paper, fabric, resin chemistry and solvent recovery are specified separately.
Core Advantages of Haifeng Transfer Systems
Configured equipment functions and interfaces for the selected material and tooling.
-20°C 200,000 Flex Durability
Supplied configuration function: Low-glass-transition polyether matrices prevent brittle micro-cracking under freezing footwear action. Project-dependent performance requires validation.
≥ 60 N/3cm High Peel Strength
Supplied configuration function: High-pressure heated lamination nips force reactive adhesive deep into base fabric pores. Project-dependent performance requires validation.
±2 N Zero-Wrinkle Tension
Supplied configuration function: Real-time servo dancer regulation isolates paper tension transients, slashing paper tear shutdowns by 85%. Project-dependent performance requires validation.
±1.5 µm Streak-Free Finish
Supplied configuration function: Enclosed slot die heads eliminate manual knife streaks, reproducing sharp release paper grain textures. Project-dependent performance requires validation.
Related Project Draft
An anonymous project brief from the supplied document. Original attribution, dates, acceptance and outcome records require verification before public use.
Frequently Asked Questions
How does the slot die coater prevent blade streaks on high-gloss patent leather?
Can this transfer line process high-depth 3D textured silicone release paper?
What maintains stable ±2 N tension during automatic flying splices at 25 m/min?
How does the progressive oven prevent solvent bubble blisters in thick coats?
Discuss Your Production Goals
Share your product or drawing, material system, target output, automation needs and factory utilities so the equipment and interfaces can be configured.


