
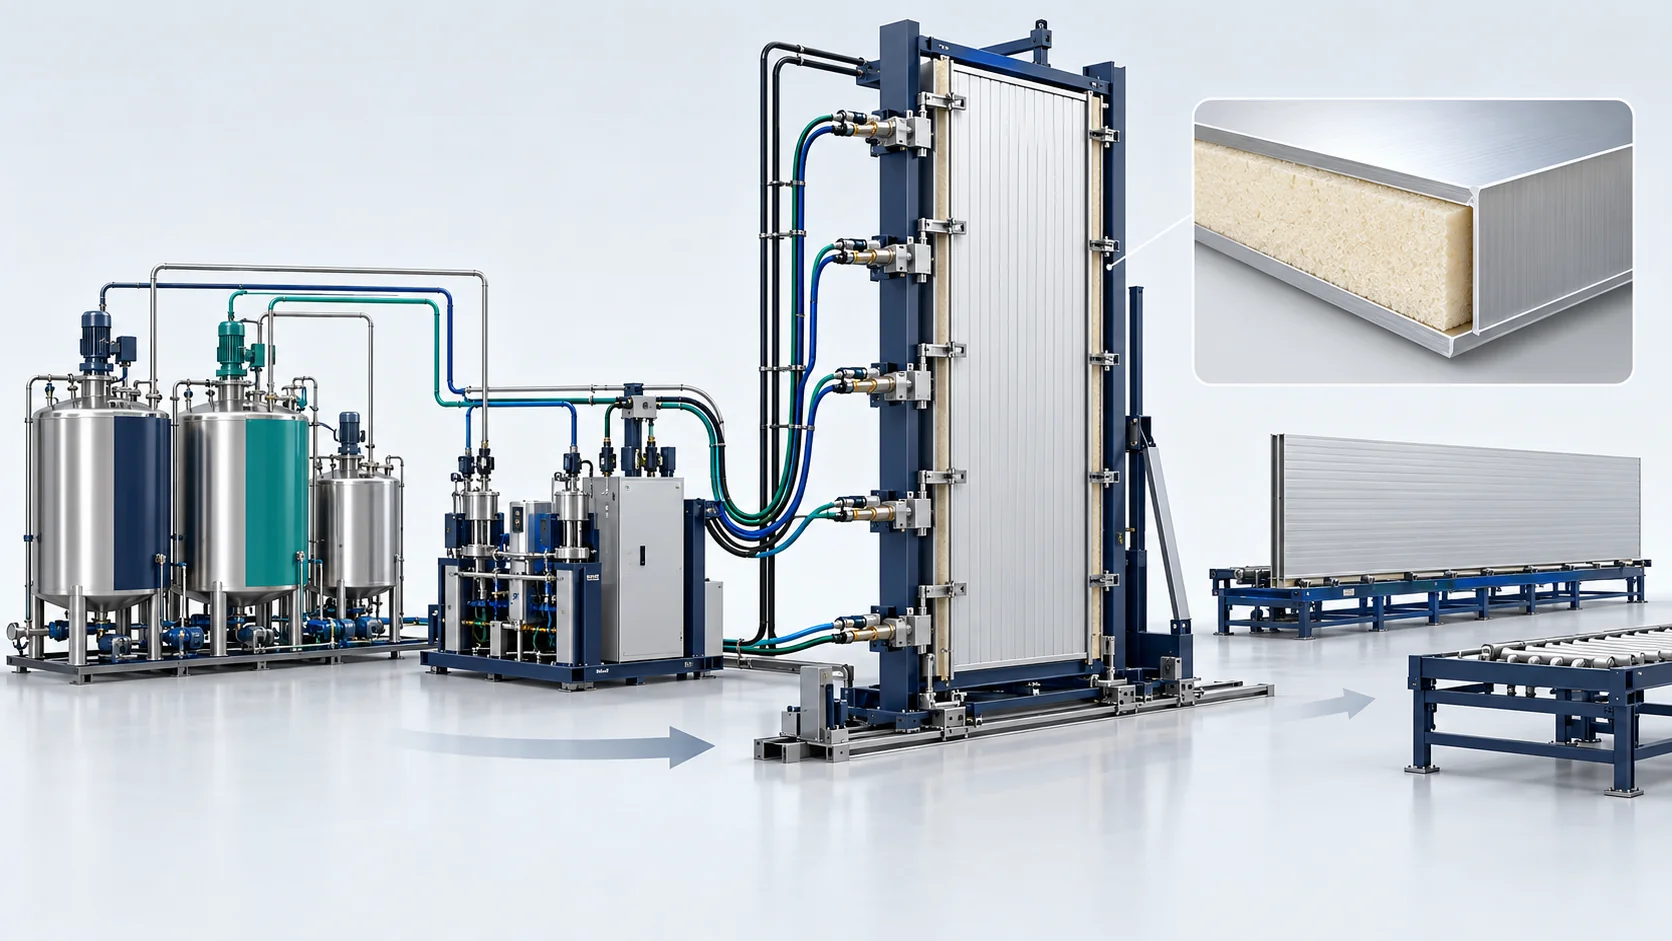
40ft Reefer Container Foaming Solution
Six-head PU delivery and vertical fixture control for long reefer-container sidewalls, with part-specific fill and curing sequences.
Monolithic Thermal Integrity for 40ft Global Intermodal Reefer Containers
Six-head PU delivery and vertical fixture control for long reefer-container sidewalls, with part-specific fill and curing sequences.
Equipment and process scope
Material conditioning, multi-head metering, vertical clamping fixture and synchronized controls. Shell geometry, molds, blowing-agent system, exhaust and site interfaces are agreed separately.
Validation and production planning
A 110 kg shot in 23.5 s implies 280.9 kg/min, exceeding the stated combined 240 kg/min maximum. Reconcile output, shot mass and actual injection duration. Whole-container heat transmission is a finished-assembly test, not the material conductivity or machine rating; ATP-related claims need original assembly reports.
Material conditioning, multi-head metering, vertical clamping fixture and synchronized controls. Shell geometry, molds, blowing-agent system, exhaust and site interfaces are agreed separately. A 110 kg shot in 23.5 s implies 280.9 kg/min, exceeding the stated combined 240 kg/min maximum. Reconcile output, shot mass and actual injection duration. Whole-container heat transmission is a finished-assembly test, not the material conductivity or machine rating; ATP-related claims need original assembly reports.Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Turnkey Vertical Reefer Panel Foaming Workflow
Configuration sequence from the supplied brief. Material, tool, pressure/temperature basis and complete line balance require verification. A 110 kg shot in 23.5 s implies 280.9 kg/min, exceeding the stated combined 240 kg/min maximum. Reconcile output, shot mass and actual injection duration. Whole-container heat transmission is a finished-assembly test, not the material conductivity or machine rating; ATP-related claims need original assembly reports.
Sheet Loading & 13.5m Vertical Clamping
Supplied process reference: Corrugated stainless exterior skins and interior liners are loaded into the vertical press; hydraulic toggles clamp the bed under 1.2 bar counter-pressure.
Sealed Nitrogen Conditioning & Metering
Supplied process reference: Cyclopentane-polyol and polymeric isocyanates are conditioned in dual 500 L tanks at 24°C under dry nitrogen blankets, metered by servo axial piston pumps.
Six-Head Synchronous Base Injection
Supplied process reference: Six high-pressure impingement heads discharge simultaneously along the tool base, injecting 110 kg of formulation within 25 seconds at 220 kg/min.
Reference Solution Engineering Envelope
Supplied configuration and validation references; material/component results are separate from equipment ratings.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Clamping Platen Length | Up to 13,500 mm (12.2m finished panel) | Accommodates standard 40ft High-Cube reefer side walls; supplied configuration or material target, pending the applicable original records |
| Clamping Pressure Resistance | 1.2 bar continuous side-wall counter-pressure | Heavy-duty welded steel frame with hydraulic toggles; supplied configuration or material target, pending the applicable original records |
| Combined Chemical Output | 80.0 to 240.0 kg/min | Six-head synchronized high-pressure proportioning skid; supplied configuration or material target, pending the applicable original records |
| Container Heat Leakage Rate | U ≤ 0.32 W/(m²·K) | reported under ATP international perishable transport rules; supplied configuration or material target, pending the applicable original records |
| Panel Thickness Uniformity | Within ±0.5 mm across 12.2m length | Precision-machined heated vertical clamping platens; supplied configuration or material target, pending the applicable original records |
| In-Mold Foam Curing Cycle | Less than or equal to 20 minutes | Water-heated platens maintained at 48°C ± 1°C; supplied configuration or material target, pending the applicable original records |
Core Equipment for This Solution
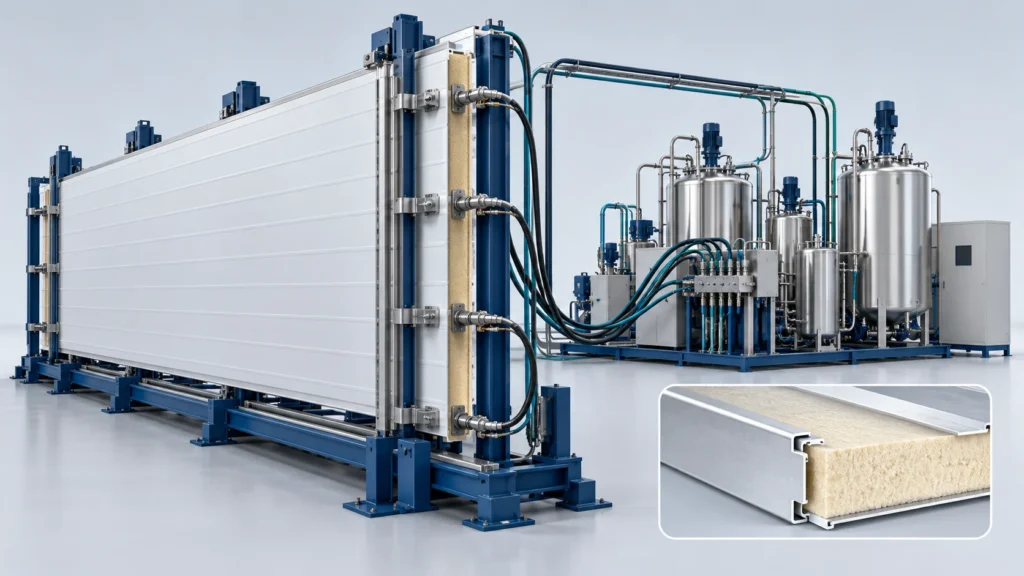
Material conditioning, multi-head metering, vertical clamping fixture and synchronized controls. Shell geometry, molds, blowing-agent system, exhaust and site interfaces are agreed separately.
Core Advantages of Haifeng Reefer Systems
Configured equipment functions and interfaces for the selected material and tooling.
ATP reported U ≤ 0.32 W/(m²·K)
Supplied configuration function: Monolithic 12.2-meter seamless construction eliminates splicing cold bridges, meeting global perishable transport rules. Project-dependent performance requires validation.
1.2 Bar Anti-Bulging Clamping
Supplied configuration function: Heavy vertical hydraulic structure withstands 1.2 bar expansion force, keeping wall thicknesses within ±0.5 mm. Project-dependent performance requires validation.
25-Second Rapid 110 kg Shot
Supplied configuration function: Six synchronized base heads flood cavities in 25 seconds, eliminating vertical density gradients. Project-dependent performance requires validation.
Natural Vertical Air Venting
Supplied configuration function: Vertical rising expansion purges air upward naturally, aims to reduce horizontal core air pockets. Project-dependent performance requires validation.
Related Project Draft
An anonymous project brief from the supplied document. Original attribution, dates, acceptance and outcome records require verification before public use.
Frequently Asked Questions
How does vertical foaming prevent air entrapment along 12-meter panels?
Can the vertical press handle both 40ft High-Cube and 20ft standard panels?
What maintains equal chemical delivery across all six injection heads?
How does the machine handle explosive cyclopentane formulations safely?
Discuss Your Production Goals
Share your product or drawing, material system, target output, automation needs and factory utilities so the equipment and interfaces can be configured.


