
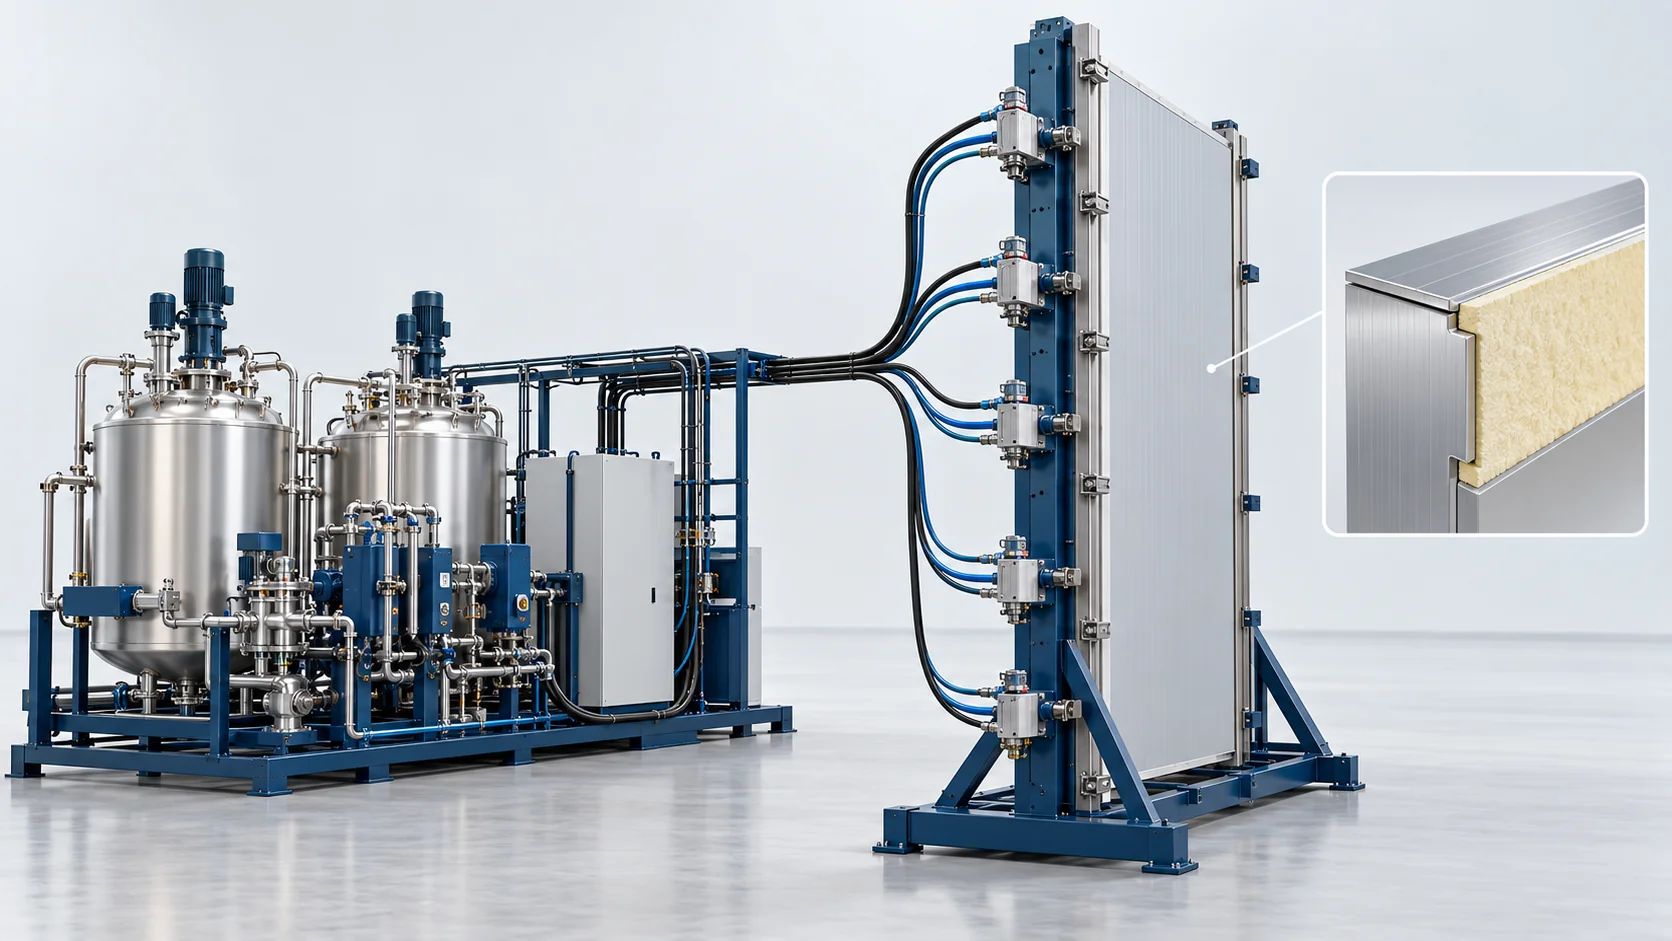
High-Pressure PU Foaming Line | Reefer Sidewalls
Six-head PU delivery and vertical fixture control for long reefer-container sidewalls, with part-specific fill and curing sequences.
Discharge Flow Rate
80–240 kg/min, combined chemical output across the configured six-head system
Mix Ratio
100:110 to 100:150 (By weight)
Accuracy Reference
±0.3% (Under continuous Coriolis mass flow tracking)
Material Conditioning Reference
24°C ±0.5°C in the listed day-tank conditioning
High-Capacity Vertical Foaming for 40ft Intermodal Reefer Panels
Six-head PU delivery and vertical fixture control for long reefer-container sidewalls, with part-specific fill and curing sequences.
The HF-RFC40-VPR coordinates six-head PU delivery with a vertical clamping fixture for long reefer sidewall panels. The listed combined chemical-output range is 80–240 kg/min.
For a 110 kg reference shot, 240 kg/min constant combined output gives a calculated injection time of 27.5 seconds. This is a sizing calculation, not a measured production result. Actual shot timing also depends on the flow profile, head sequencing and material reaction window.
Panel geometry, fixture loading and curing conditions are agreed for the project. Whole-container heat transmission and thermal-bridge performance are tested on the complete assembly.
Concept illustration: Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Material Flow and Working Principle
Sheet Positioning & Vertical Mold Clamping
Exterior corrugated stainless steel sheets and interior food-grade lining skins are loaded into the vertical press bed; hydraulic toggle locks clamp the 13.5m platens under 1.2 bar counter-pressure.
High-Pressure Chemical Conditioning
Specialized low-k polyol blends and polymeric isocyanates are conditioned in dual 500 L jacketed day tanks at 24°C ± 0.5°C under dry nitrogen blankets to maintain reaction kinetics.
Synchronous Six-Head Impingement Injection
The configured six-head system meters the selected formulation within an 80–240 kg/min combined-output range. For a 110 kg reference shot, 27.5 s is calculated at constant 240 kg/min; actual timing follows the qualified flow profile.
Vertical Rising Core Expansion & Curing
The liquid matrix creams rapidly, rising vertically through the 70 mm core gap; precision water-heated platens maintain 48°C to cure the panel within 20 minutes without density gradients.
Vertical Mold Opening & Overhead Extraction
Hydraulic cylinders retract the vertical clamping platens; automated overhead cranes grip the finished 12-meter monolithic panel and transfer it to container box assembly.
Need a quote for this equipment?
Request a QuoteModel and Technical Parameters
Reference combined output: 80–240 kg/min across six configured heads. A 110 kg reference shot requires 27.5 s at constant 240 kg/min; this is a calculation rather than a measured shot time. Fixture loading, material reaction window, flow profile and finished-container thermal tests are defined separately.
| Technical Parameter | HF-RFC40-VPR |
|---|---|
| Components | 2 Components (A: Polyol blend + Cyclopentane, B: Polymeric MDI) |
| Output Range | 80–240 kg/min, combined chemical output across the configured six-head system |
| Mixing Ratio Range | 100:110 to 100:150 (By weight) |
| Accuracy Reference | ±0.3% (Under continuous Coriolis mass flow tracking) |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 440V/480V 60Hz optional) |
| Working Pressure | 15.0 to 17.5 MPa (High-pressure metering and delivery lines) |
| Tank / Hopper Capacity | Day tanks: 2 x 500 L (Stainless steel with N2 blanket) |
| Weight | 24,500 kg (Combined vertical press frame and metering skid) |
| Dimensions (L×W×H) | 14,200 mm x 3,600 mm x 4,200 mm |
| Shot Mass and Calculated Injection-Time Reference | 110 kg reference shot. At 240 kg/min constant combined output, calculated injection time is 27.5 s; actual timing follows the qualified flow profile and material window. |
Key Equipment Features
Material conditioning, multi-head metering, vertical clamping fixture and synchronized controls. Shell geometry, molds, blowing-agent system, exhaust and site interfaces are agreed separately.
Configured Vertical Clamping
Long vertical platens and hydraulic locking are selected for the panel dimensions and foaming load. Frame height and panel length are separate quantities.
Six-Head Combined Delivery: 80–240 kg/min
Coordinate head sequencing and the liquid distribution profile for the selected shot and available reaction time.
Finished-Container Thermal Assessment
Panel joints, insulation material and complete enclosure construction determine heat transmission; assess them through assembly testing.
Long-Panel Tooling Interfaces
Panel lengths up to the supplied 12,200 mm reference are reviewed with skins, molds, handling and installation clearances.
Discuss Your Equipment Configuration
Share your product, materials, tooling and production requirements so we can review the equipment and interfaces for your project.
Frequently Asked Questions
How are shot mass, flow and injection time related?
Does vertical foaming guarantee uniform density?
Does panel production establish whole-container thermal performance?
What does the fixture length describe?
Ready to discuss your project?
Contact Our Team


