
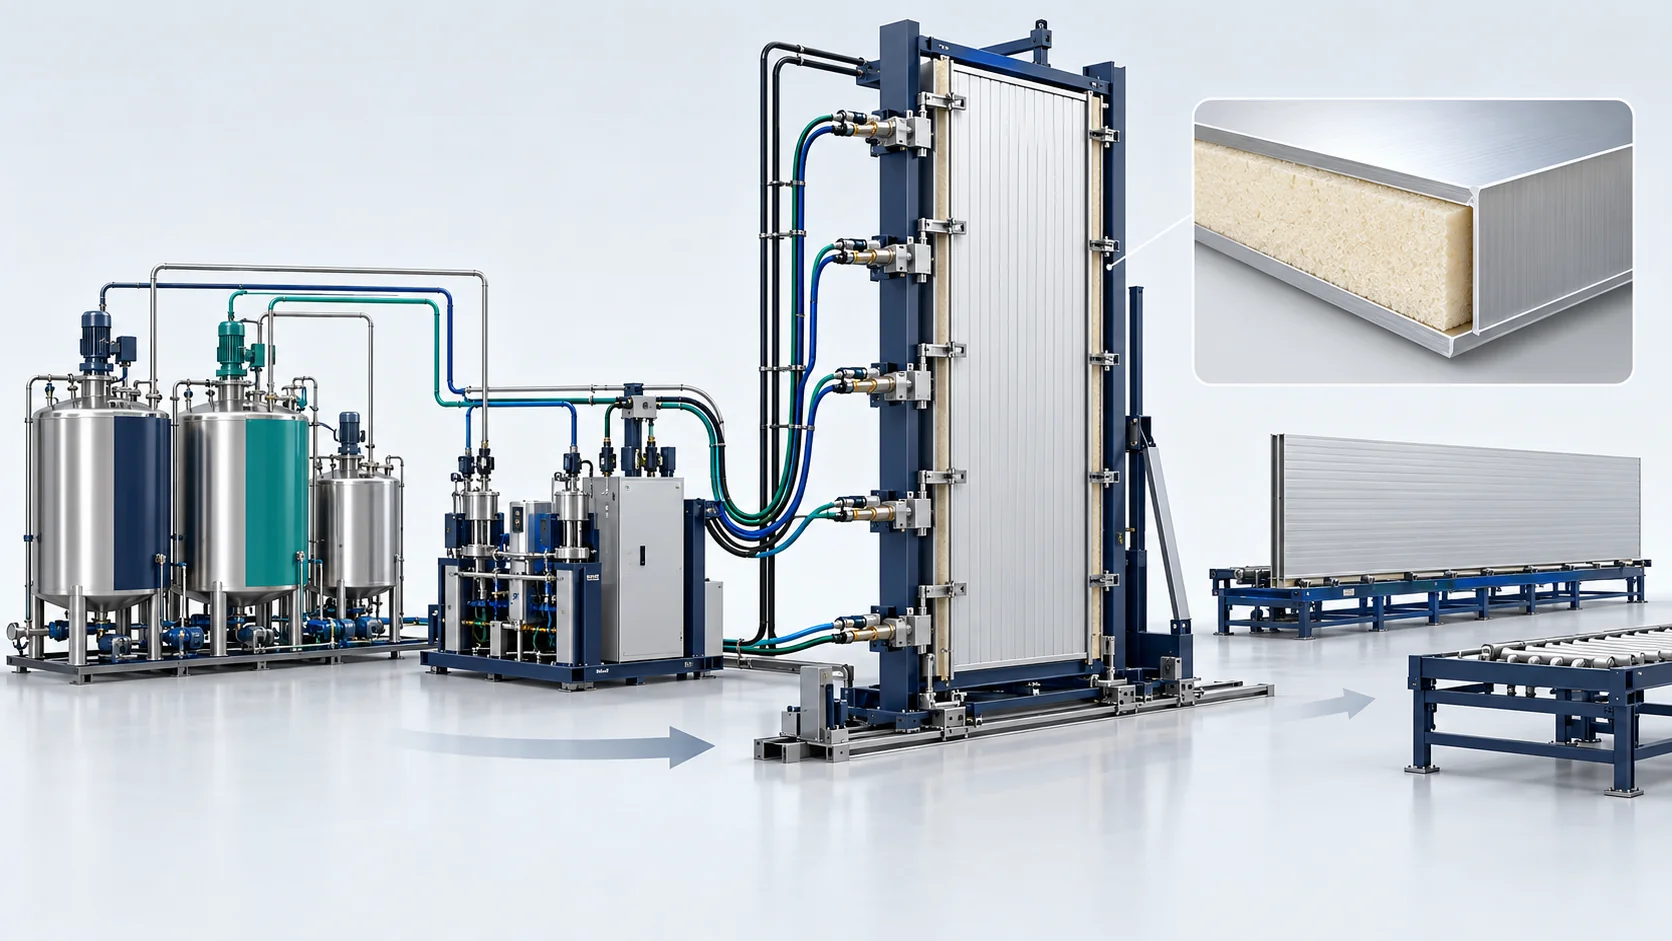
Решение для вспенивания 40-футовых рефрижераторных контейнеров
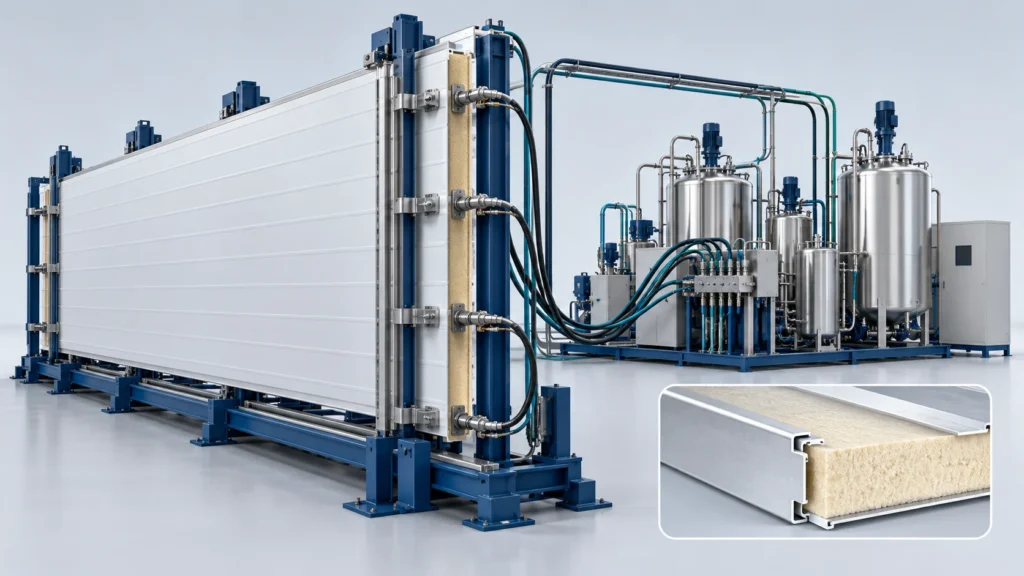
Configure six-head PU delivery and vertical fixture interfaces for long reefer-container sidewall panels.
Monolithic Thermal Integrity for 40ft Global Intermodal Reefer Containers
Long reefer sidewalls need a defined skin construction, injection layout, head sequence, fixture restraint and cure. Combined chemical output is the complete system rate, not a per-head value. Container heat leakage and transport qualification require tests of the actual assembly and cannot be inferred from the foaming equipment alone.
Определенный объем поставки
Define the metering circuits, heads, vertical fixture, temperature control and safety interfaces. Different container lengths and skins require their own tool and changeover assessment.
Исходные данные для выбора процесса
Container sidewall build, lengths/thicknesses, skins, total shot, head layout, fixture, blowing-agent system and thermal-test requirements.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Define the metering circuits, heads, vertical fixture, temperature control and safety interfaces. Different container lengths and skins require their own tool and changeover assessment.
40ft Reefer Container Foaming Workflow
Prepare and clamp the panel → Condition and balance feeds → Inject and cure → Demold and inspect. Define preparation, filling, cure and output timing separately for the selected configuration.
Prepare and clamp the panel
Confirm skins, dimensions, spacers, vents and fixture closure.
Condition and balance feeds
Review material conditions, head delivery and the total shot.
Inject and cure
Validate sequencing and fill along the long panel.
Технические характеристики эталонного решения
Существующая конфигурация и справочные данные испытаний. Настройки оборудования, результаты по материалам и результаты по готовой сборке приведены отдельно; применяйте каждое значение только к его задокументированной конфигурации и условиям.
Для более широкого планирования производства и ознакомления со смежными технологическими маршрутами изучите Cold Chain PU Insulation Turnkey Plant.
| Параметр | Значение / единица измерения | Применимая конфигурация / условия |
|---|---|---|
| Clamping Platen Length | Up to 13,500 mm (12.2m finished panel) | Accommodates standard 40ft High-Cube reefer side walls |
| Clamping Pressure Resistance | 1.2 bar continuous side-wall counter-pressure | Heavy-duty welded steel frame with hydraulic toggles |
| Combined Chemical Output | 80.0 to 240.0 kg/min — configuration reference | Complete six-head system total; confirm the selected flow with shot mass, duration, material and injection records |
| Container Heat Leakage Rate | U ≤ 0.32 W/(m²·K) | reported under ATP international perishable transport rules |
| Panel Thickness Uniformity | Within ±0.5 mm across 12.2m length | Precision-machined heated vertical clamping platens |
| In-Mold Foam Curing Cycle | Less than or equal to 20 minutes | Water-heated platens maintained at 48°C ± 1°C |
Основное оборудование для этого решения
Справочные данные по оборудованию выбираются по документированному для них процессу. Основное дозирование, вспомогательная подача и альтернативные схемы не являются единым стандартным комплексом.
Управление процессом и прикладные проверки
Оцените эти функции с учетом выбранного материала, оснастки и производственного задания. Для результатов готовых деталей требуется отдельное приемочное подтверждение.
Combined-flow clarity
Use total shot mass and duration to interpret the system output.
Long-tool coordination
Match platen envelope, restraints and injection points to the finished panel.
Assembly-level thermal evidence
Report heat leakage with the tested container construction and method.
Связанные проекты
Это справочные данные по родственным применениям. Сравнивайте фактические материалы, процесс и поставленные модули; приведенные показатели проекта не являются приемочными результатами для другой линии.
Часто задаваемые вопросы
Can the system flow be multiplied by the number of heads?
Does the listed heat-leakage value establish transport approval?
Какая информация необходима для предварительной конфигурации?
Обсудите ваши производственные задачи
Share the following with your production brief: Container sidewall build, lengths/thicknesses, skins, total shot, head layout, fixture, blowing-agent system and thermal-test requirements. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


