
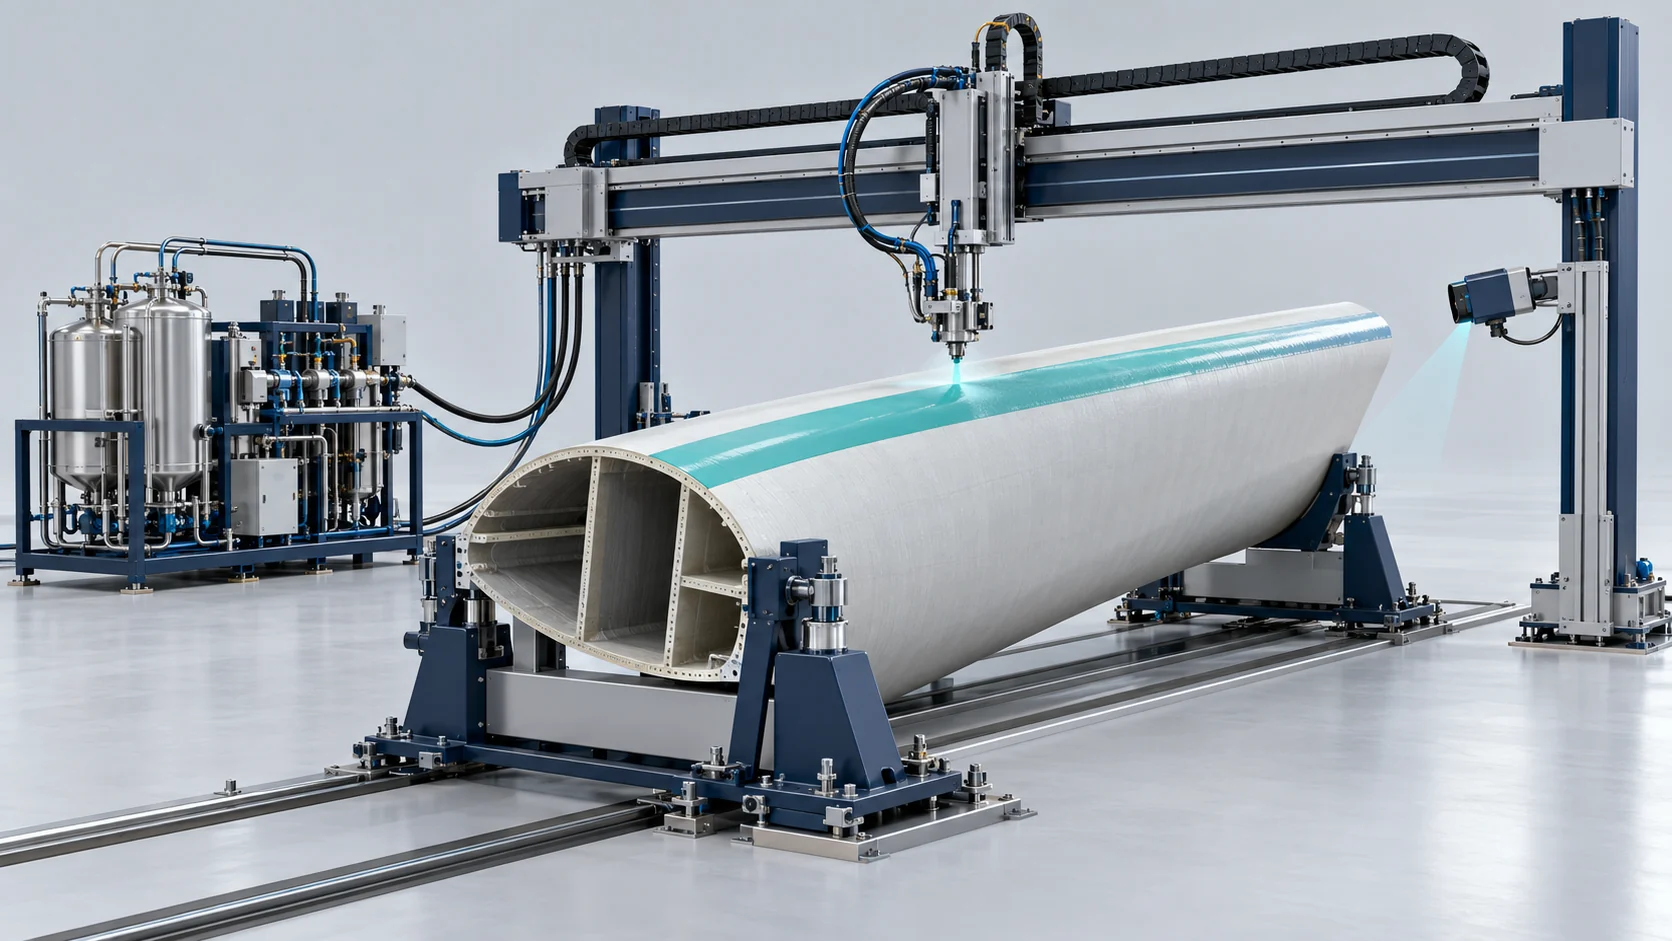
Wind Blade Leading-Edge Coating Solution
Servo-metered spraying for the polyaspartic resin/aliphatic-isocyanate leading-edge coating described in the supplied brief. Robotic tracking and film inspection are separately specified options.
Polyaspartic Leading-Edge Coating Configuration
Servo-metered spraying for the polyaspartic resin/aliphatic-isocyanate leading-edge coating described in the supplied brief. Robotic tracking and film inspection are separately specified options.
Servo Metering
The specified feed-control system manages the selected coating ratio and calibrated delivery window.
Film-Build Control
Traverse, atomization and inspection are configured against a dry-film target; wet-film settings are established separately.
Select the equipment, coating build-up and inspection plan against the substrate, part geometry, production target and site conditions. Material qualification and reported outcomes require project-specific records.
Turnkey Precision Leading-Edge Protection Workflow
A configured sequence of substrate preparation, material conditioning, application, cure and inspection for the selected coating system.
Prepare the Surface
Confirm preparation and coating compatibility for the blade substrate.
Define the Application Path
Specify robotic tracking and its interface separately for the actual blade geometry.
Meter the Coating
Condition and meter the selected polyaspartic resin and aliphatic-isocyanate components.
Reference Solution Engineering Envelope
Supplied configuration and coating-system references. Values depend on the stated material, substrate, test and operating conditions; original records are not attached.
| Item | Reference / Selection Input | Conditions |
|---|---|---|
| Metering output reference | 0.5–4.5 kg/min | Supplied equipment-configuration range; calibrate with the selected material. |
| Fluid-pressure reference | 10–14 MPa | Confirm circuit and operating conditions in the equipment schedule. |
| Pressure-ripple reference | <±0.1 MPa | Brief process-control value requiring measurement records; no pulse-free assertion. |
| Dry-film target | 300 ±20 µm | Target for the selected application; wet-film settings and final inspection are separate. |
| Submitted rain-erosion reference | 120 m/s; 15 h; no reported pitting | Supplied material/ specimen result; original coating, cure and report pending. |
| Submitted airfoil comparison | <0.2% | Original definition, geometry and comparison records pending; not turbine energy performance. |
Core Equipment for This Solution
The package covers servo metering, temperature-conditioned passages, the specified atomizing head and controls. Gantry tracking and non-contact film measurement are optional. Polyaspartic coating is supplied by the selected material supplier; clean surface-preparation facilities and conditioned compressed air are customer interfaces. Coating qualification and aerodynamic results require component-specific records.
Core Advantages of Haifeng Blade Solutions
Configured process mechanisms and project interfaces for the selected equipment package.
Servo Metering
The specified feed-control system manages the selected coating ratio and calibrated delivery window.
Film-Build Control
Traverse, atomization and inspection are configured against a dry-film target; wet-film settings are established separately.
Rain-Erosion Test Evidence
Laboratory erosion testing is specific to the coating, substrate, cure and test conditions and requires original reports.
Airfoil Evaluation Evidence
Surface profile and wind-tunnel results are component-specific; a spray configuration alone does not establish turbine energy yield.
Related Project Draft
Review the project configuration described in the supplied brief. Project records and reported results require verification before public use.
Frequently Asked Questions
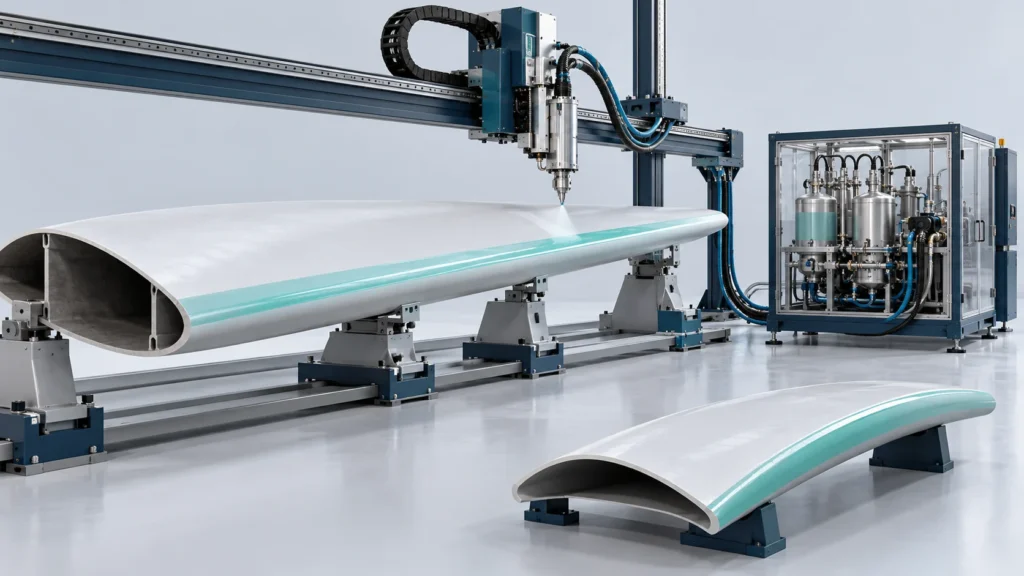
Find answers about Wind Blade Leading-Edge Polyurea Solution, including material selection, equipment configuration and the information needed to plan a production line.
How are dry and wet coating thickness controlled?
Do spray stability and wind-tunnel results establish turbine energy gains?
How is laboratory rain-erosion performance evaluated?
Can a factory package be used for field blade repairs?
Request a Wind Blade LEP Coating Proposal
Share the substrate or finished part, selected materials, coating and quality requirements, target output, automation needs and factory or worksite conditions.


