
Metal-Core MC Nylon Gear Casting Solution
Metal-core conditioning and vacuum-assisted MC Nylon casting for hybrid gear tooling and part-development trials.
Heavy Torque Capacity Meets Acoustic Silence in Industrial Drives
Metal-core conditioning and vacuum-assisted MC Nylon casting for hybrid gear tooling and part-development trials.
Equipment and process scope
Monomer circuits, metering/mixing, induction preheat, vacuum interface and controls. Splined hub, gear mold, post-treatment and final load/noise qualification are separate.
Validation and production planning
Sound-pressure reduction in dB(A) and sound-power results under GB/T 3768 require consistent definitions and test geometry. 4,550 N·m torque and 8,000-hour life are different qualification claims. The stated March 2026 8,000-hour follow-up needs reconciled implementation/test dates. A metal core is an insert, not a third liquid chemical stream.
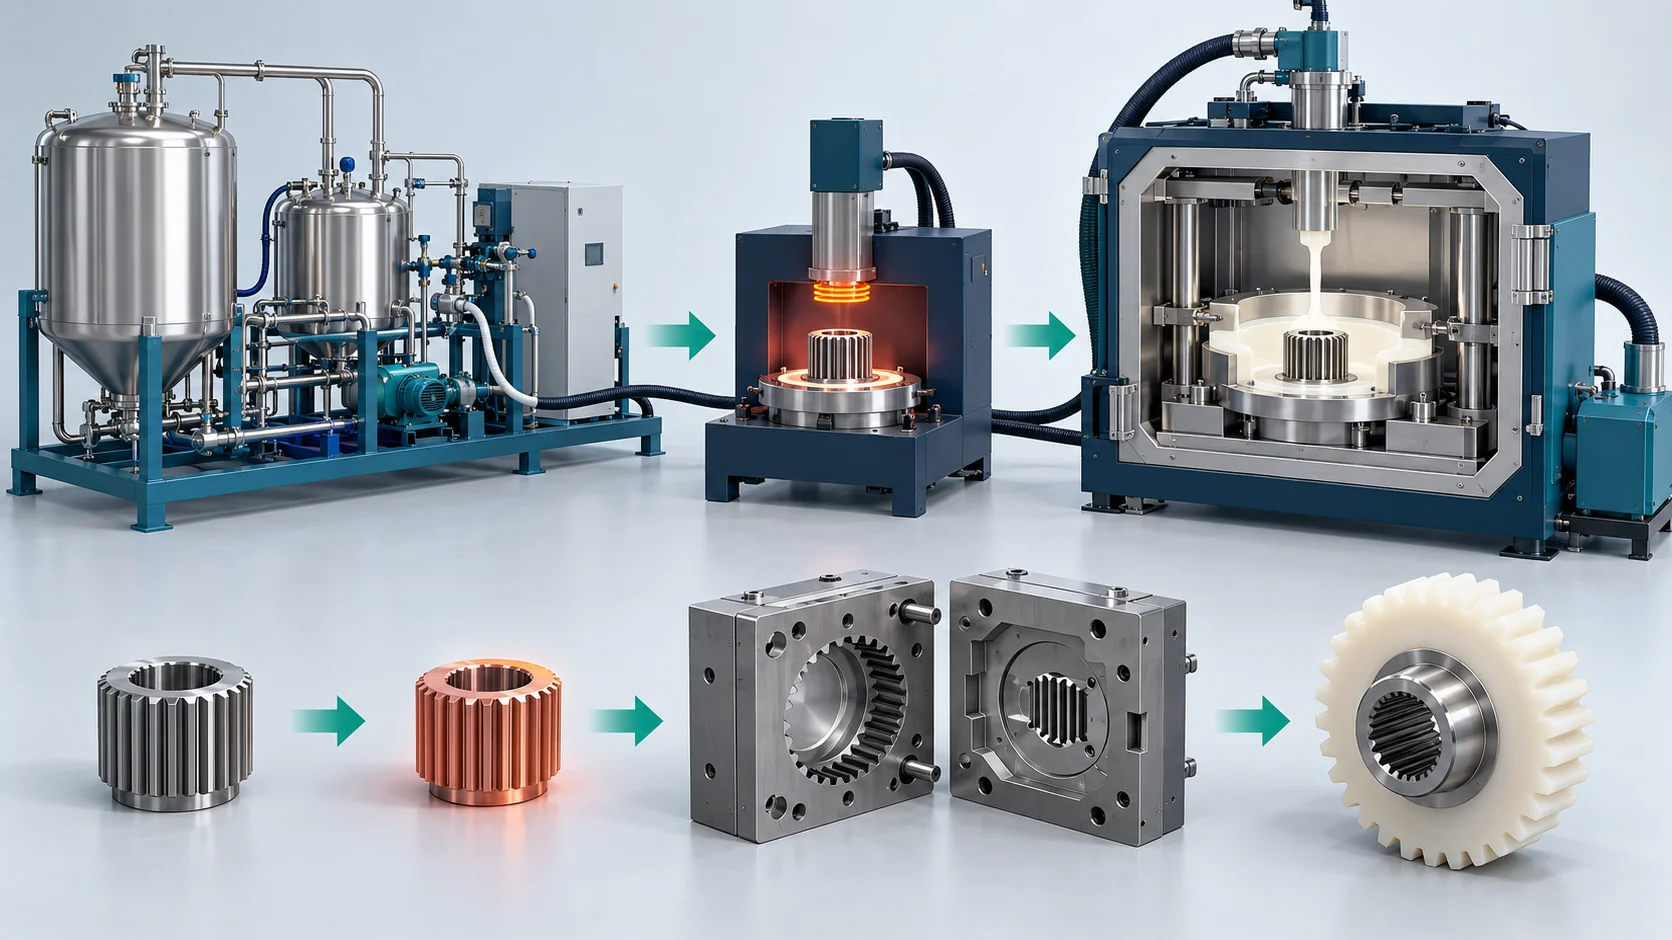
Monomer circuits, metering/mixing, induction preheat, vacuum interface and controls. Splined hub, gear mold, post-treatment and final load/noise qualification are separate. Sound-pressure reduction in dB(A) and sound-power results under GB/T 3768 require consistent definitions and test geometry. 4,550 N·m torque and 8,000-hour life are different qualification claims. The stated March 2026 8,000-hour follow-up needs reconciled implementation/test dates. A metal core is an insert, not a third liquid chemical stream.Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Turnkey In-Situ Hybrid Gear Casting Workflow
Configuration sequence from the supplied brief. Material, tool, pressure/temperature basis and complete line balance require verification. Sound-pressure reduction in dB(A) and sound-power results under GB/T 3768 require consistent definitions and test geometry. 4,550 N·m torque and 8,000-hour life are different qualification claims. The stated March 2026 8,000-hour follow-up needs reconciled implementation/test dates. A metal core is an insert, not a third liquid chemical stream.
Hub Surface Preparation & Induction Preheating
Supplied process reference: Forged 40Cr steel hubs machined with knurled dovetails are blasted to Sa 2.5 and heated to 160°C in an induction coil under nitrogen in 60s.
Robotic Loading & 1 kPa Tool Evacuation
Supplied process reference: A robotic gripper transfers the hot hub into a 165°C gear mold; hydraulic clamps seal platens while vacuum skids draw cavity pressure to 1 kPa.
Toughened Monomer Thermal Conditioning
Supplied process reference: Low-viscosity caprolactam and elastomeric tougheners are conditioned at 135°C under 0.01 kPa vacuum, metered at 1:1 ratios within ±0.2%.
Reference Solution Engineering Envelope
Supplied configuration and validation references; material/component results are separate from equipment ratings.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Continuous Monomer Pour Output | 3.0 to 20.0 kg/min | Continuous variable servo-driven high-temperature pump skid; supplied configuration or material target, pending the applicable original records |
| Induction Metal Core Heating Rate | 160°C ± 2°C in ≤ 60 seconds | Medium-frequency induction heating coil under nitrogen; supplied configuration or material target, pending the applicable original records |
| Maximum Transmitted Gear Torque | Up to 4,500 N·m | Splined 40Cr steel hub with dovetail mechanical interlock; supplied configuration or material target, pending the applicable original records |
| Gear Meshing Noise Attenuation | Greater than or equal to 15 dB(A) | Measured vs conventional forged steel gears in closed gearbox; supplied configuration or material target, pending the applicable original records |
| Mold Cavity Pre-Vacuum Level | Down to 1.0 kPa (Absolute) | Multi-stage vacuum evacuation skid with tool sealing; supplied configuration or material target, pending the applicable original records |
| Finished Gear Diameter Envelope | Ø 400 mm to Ø 1,200 mm | Involute gear tooth tooling (Module m = 6– 16); supplied configuration or material target, pending the applicable original records |
Core Equipment for This Solution
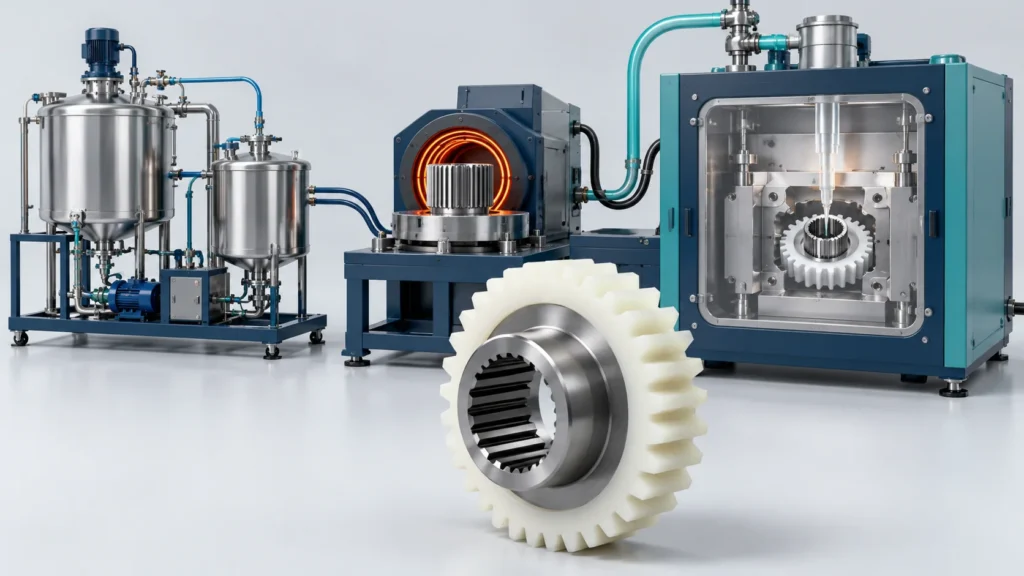
Monomer circuits, metering/mixing, induction preheat, vacuum interface and controls. Splined hub, gear mold, post-treatment and final load/noise qualification are separate.
Core Advantages of Haifeng Gear Systems
Configured equipment functions and interfaces for the selected material and tooling.
15 dB(A) Severe Drive Silencing
Supplied configuration function: Damping nylon tooth envelopes absorb tooth-mesh impacts, cutting gearbox roar by 15 dB(A). Project-dependent performance requires validation.
Zero Thermal Shrink Tension
Supplied configuration function: 160°C induction preheating allows nylon and steel to crystallize concurrently, eliminating tooth root cracks. Project-dependent performance requires validation.
4,500 N·m High-Torque Transmission
Supplied configuration function: Internal forged 40Cr splined hubs absorb driving loads, preventing plastic keyway wall deformation. Project-dependent performance requires validation.
1 kPa Pinhole-Free Tooth Roots
Supplied configuration function: Deep vacuum evacuation pulls low-viscosity monomer deep into tooth roots without cavitation voids. Project-dependent performance requires validation.
Related Project Draft
An anonymous project brief from the supplied document. Original attribution, dates, acceptance and outcome records require verification before public use.
Frequently Asked Questions
Why is preheating metal hubs to 160°C critical before nylon casting?
How does 1 kPa vacuum infiltration improve gear tooth mechanical strength?
How does the hybrid gear achieve a 15 dB(A) transmission noise reduction?
What prevents the nylon rim from slipping on the steel hub under 4,500 N·m torque?
Discuss Your Production Goals
Share your product or drawing, material system, target output, automation needs and factory utilities so the equipment and interfaces can be configured.


