
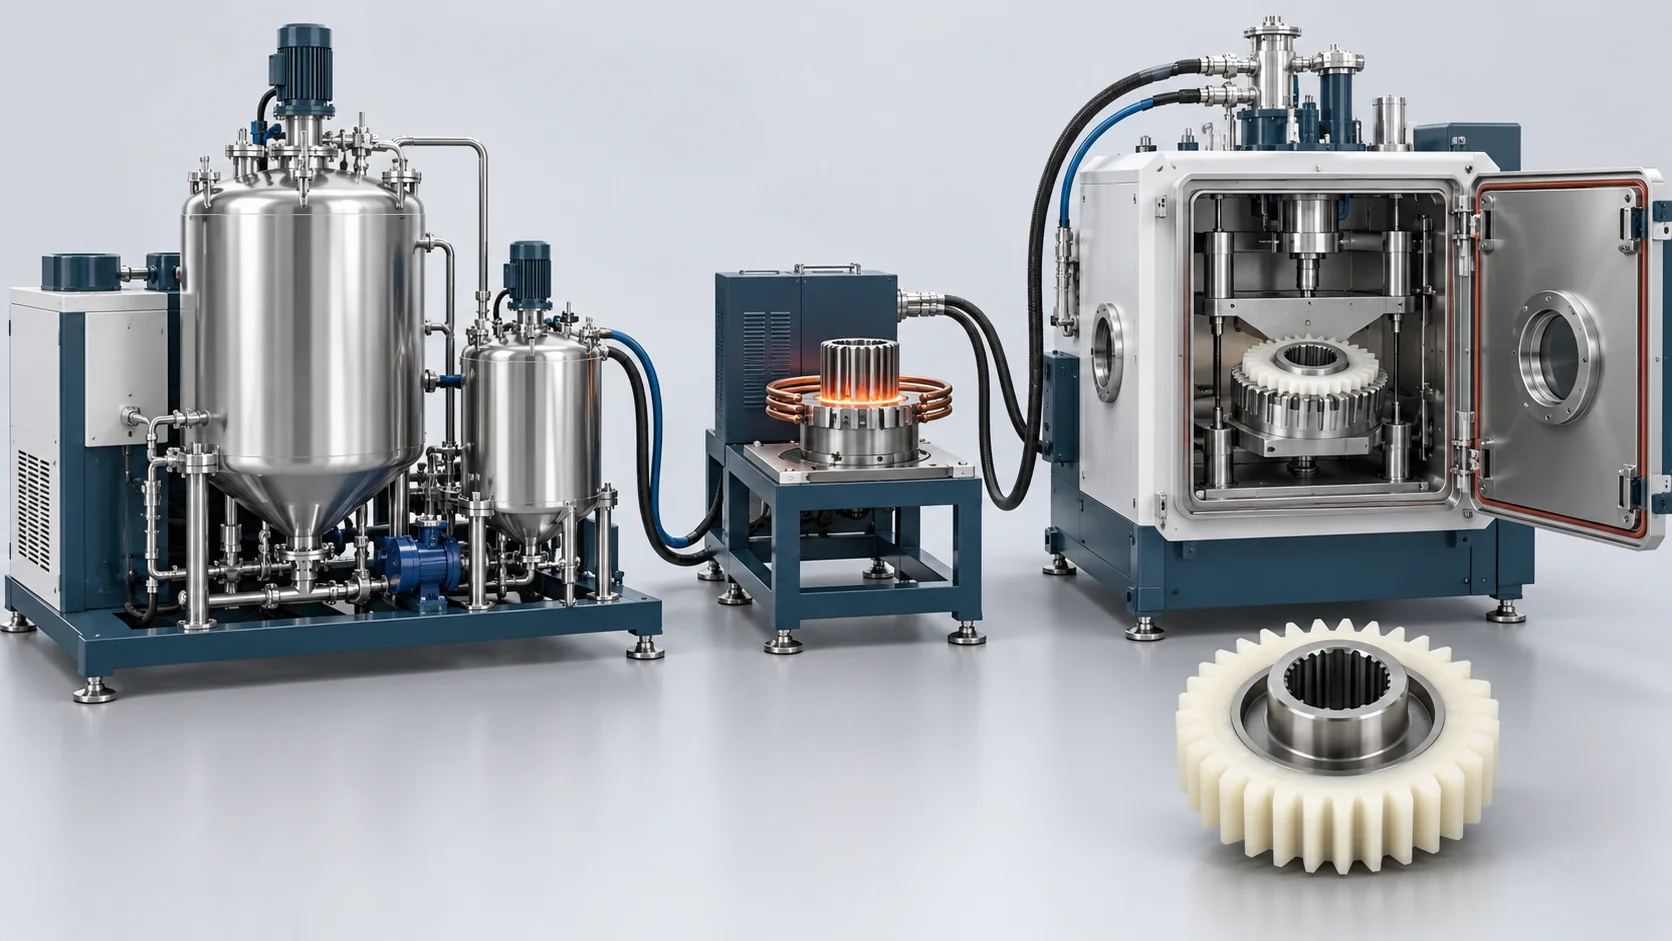
MC Nylon Casting Machine | Metal-Core Gears
Metal-core conditioning and vacuum-assisted MC Nylon casting for hybrid gear tooling and part-development trials.
In-Situ Induction Preheated Casting for Heavy Metal-Core MC Nylon Gears
Metal-core conditioning and vacuum-assisted MC Nylon casting for hybrid gear tooling and part-development trials.
Metal-core conditioning and vacuum-assisted MC Nylon casting for hybrid gear tooling and part-development trials.
Monomer circuits, metering/mixing, induction preheat, vacuum interface and controls. Splined hub, gear mold, post-treatment and final load/noise qualification are separate.
Sound-pressure reduction in dB(A) and sound-power results under GB/T 3768 require consistent definitions and test geometry. 4,550 N·m torque and 8,000-hour life are different qualification claims. The stated March 2026 8,000-hour follow-up needs reconciled implementation/test dates. A metal core is an insert, not a third liquid chemical stream.
Concept illustration: Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Material Flow and Working Principle
Metal Hub Grit Blasting & Nitrogen Induction Preheating
Forged 40Cr steel splined hubs are grit-blasted to Sa 2.5 cleanliness, loaded into an induction coil, and heated to 160°C ± 2°C under nitrogen in 60 seconds to match nylon crystal kinetics.
Automated Hub Transfer & 1 kPa Vacuum Tool Clamping
A robotic gripper transfers the hot hub into a preheated gear tooth mold (165°C); hydraulic clamps seal the tool while high-speed vacuum pumps draw cavity pressure down to 1 kPa.
High-Accuracy Toughened Monomer Metering
Dual positive displacement pumps meter dry caprolactam monomer and elastomeric tougheners at 135°C under Coriolis feedback, holding stoichiometric ratios within ±0.2%.
Deep-Cavity Vacuum Tooth Infiltration
The dynamic mixing head dispenses reactive monomer into the evacuated gear teeth; negative pressure draws liquid resin smoothly into delicate tooth roots without cavitation.
In-Situ Isothermal Crystallization & Annealing
The nylon polymerizes and crystallizes around the metal core at 165°C, bonding tightly without shrink tension; demolded gears transfer to thermal oil baths for final stress-relief.
Model and Technical Parameters
Supplied HF-MCG120-INS configuration references, pending original calibration and acceptance documents. Material, finished-part and project outcomes are separate from equipment ratings. Sound-pressure reduction in dB(A) and sound-power results under GB/T 3768 require consistent definitions and test geometry. 4,550 N·m torque and 8,000-hour life are different qualification claims. The stated March 2026 8,000-hour follow-up needs reconciled implementation/test dates. A metal core is an insert, not a third liquid chemical stream.
| Technical Parameter | HF-MCG120-INS |
|---|---|
| Components | Monomer Streams A & B + Solid Forged Steel Splined Hub |
| Output Range (g/s) | 3.0 to 20.0 kg/min (Continuous adjustable) |
| Mixing Ratio Range | 1:1 Fixed (Volumetric/weight balanced) |
| Ratio Accuracy | ±0.2% (Under continuous Coriolis mass flow tracking) |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 440V/480V 60Hz optional) |
| Working Pressure | 0.3 to 0.5 MPa (Liquid metering and head line) |
| Tank Capacity (L) | Day tanks: 2 x 150 L (Stainless steel with thermal jackets) |
| Weight | 5,600 kg (Casting machine, induction heater, and mold bed) |
| Dimensions (L×W×H) | 3800 mm x 2400 mm x 2600 mm |
| Metal Core Induction Preheating | 160°C ± 2°C (Heating duration ≤ 60 seconds); Medium-frequency induction coil; supplied reference pending original configuration or test records |
| Maximum Transmitted Torque | Up to 4,500 N·m (Splined hybrid gear hub); Heavy gear test rig; supplied reference pending original configuration or test records |
| Gear Meshing Noise Reduction | ≥ 15 dB(A) (Compared to forged steel gear); Sound level meter at 1m distance; supplied reference pending original configuration or test records |
| Mold Cavity Vacuum Level | Down to 1.0 kPa (Absolute pressure); Pre-injection vacuum manifold; supplied reference pending original configuration or test records |
Key Equipment Features
Monomer circuits, metering/mixing, induction preheat, vacuum interface and controls. Splined hub, gear mold, post-treatment and final load/noise qualification are separate.
160°C Induction Metal Preheating
Supplied configuration reference: In-line induction heating brings steel hubs to 160°C in 60s, completely eliminating thermal contraction shrink gaps. Actual capability requires material and tooling validation.
4,500 N·m High-Torque Transmission
Supplied configuration reference: Interlocked steel splined hubs carry extreme driving torques up to 4,500 N·m without tooth rim shear. Actual capability requires material and tooling validation.
15 dB(A) Acoustic Meshing Cut
Supplied configuration reference: Elastic MC nylon tooth flanks absorb gear-mesh impact dynamics, lowering drive noise by 15 dB(A). Actual capability requires material and tooling validation.
1 kPa Vacuum Tooth Infiltration
Supplied configuration reference: Pre-evacuating tool teeth to 1 kPa pulls liquid monomer deep into root fillets, eliminating porosity. Actual capability requires material and tooling validation.


