
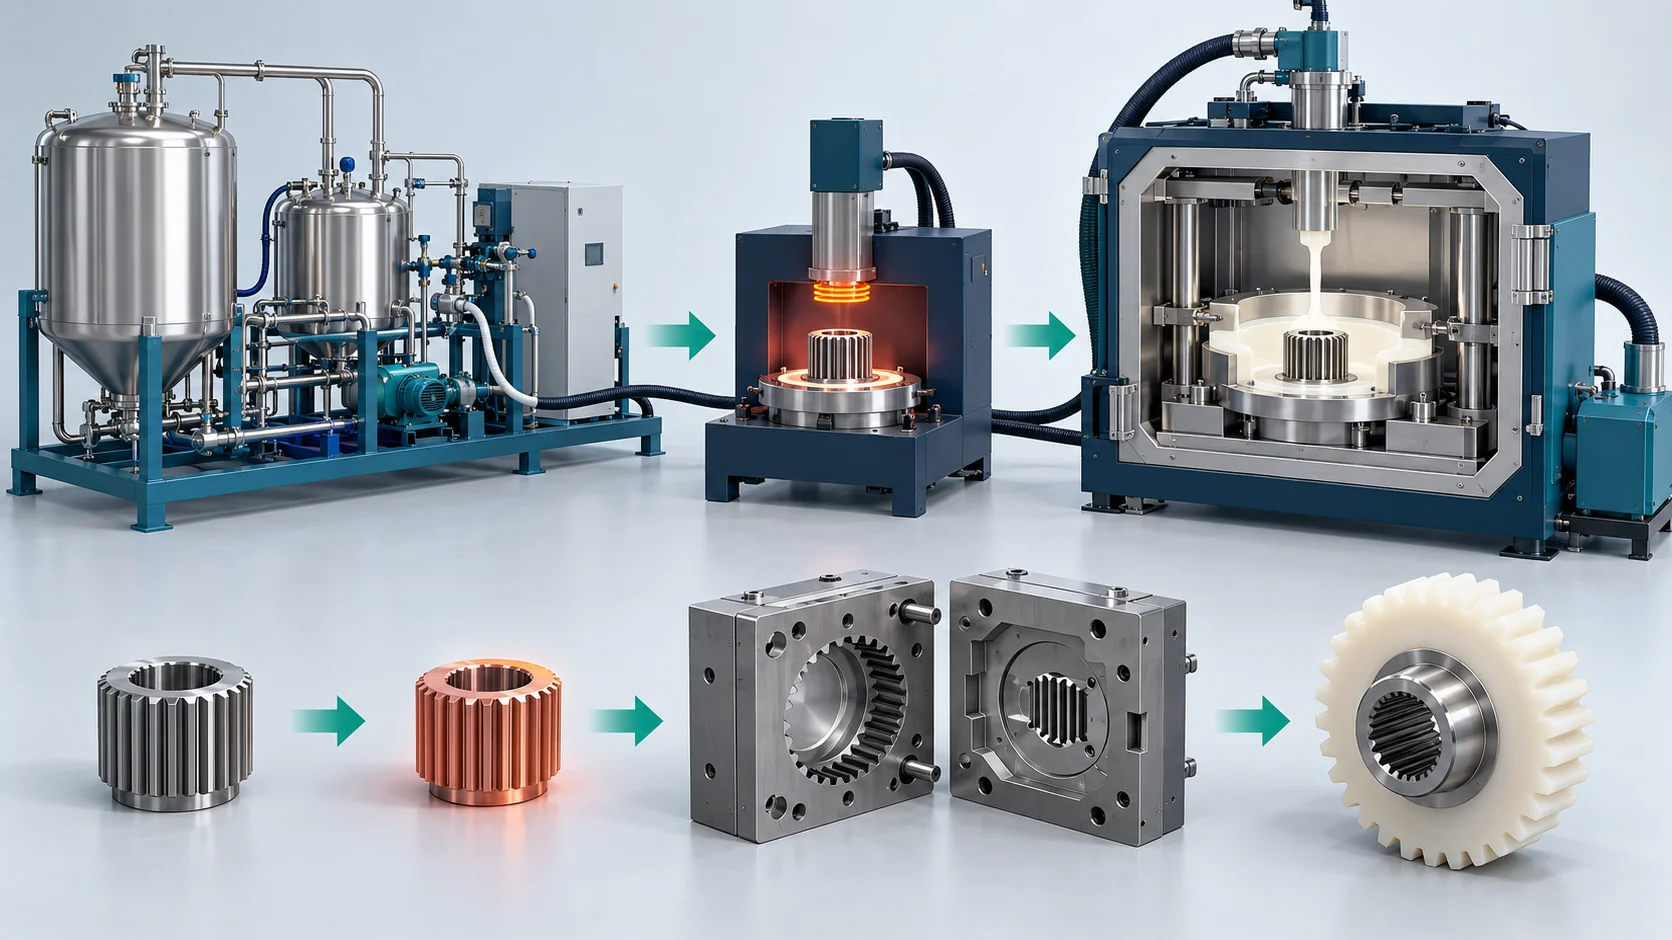
Решение для литья шестерен из MC-нейлона с металлическим сердечником
Coordinate metal-hub preparation and vacuum-assisted MC Nylon casting for a defined hybrid gear design.
Heavy Torque Capacity Meets Acoustic Silence in Industrial Drives
Hybrid gear casting combines a prepared metal hub, mechanical interlock, heated tooling and the selected nylon reaction system. Hub preheating and vacuum assistance support processing but do not prove zero residual stress, no voids or a universal torque capacity. Gear noise is an assembled-drive measurement.
Определенный объем поставки
Specify hub preparation, induction heating, casting, thermal treatment and machining. Gear tooth design and drivetrain qualification remain separate from the material-delivery package.
Исходные данные для выбора процесса
Hub/tooth drawings, interlock, load and speed, thermal cycles, machining allowances and noise-test conditions.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Specify hub preparation, induction heating, casting, thermal treatment and machining. Gear tooth design and drivetrain qualification remain separate from the material-delivery package.
Metal-Core MC Nylon Gear Casting Workflow
Prepare and locate the hub → Condition hub, mold and monomer → Cast and polymerize → Finish and qualify. Define preparation, filling, cure and output timing separately for the selected configuration.
Prepare and locate the hub
Confirm material, interlock, surface preparation and positioning.
Condition hub, mold and monomer
Review heating and vacuum conditions for the selected construction.
Cast and polymerize
Validate filling and thermal behavior at the metal/nylon interface.
Технические характеристики эталонного решения
Существующая конфигурация и справочные данные испытаний. Настройки оборудования, результаты по материалам и результаты по готовой сборке приведены отдельно; применяйте каждое значение только к его задокументированной конфигурации и условиям.
| Параметр | Значение / единица измерения | Применимая конфигурация / условия |
|---|---|---|
| Continuous Monomer Pour Output | 3.0 to 20.0 kg/min | Непрерывно регулируемая насосная установка на шестерённых насосах высокого давления с сервоприводом |
| Induction Metal Core Heating Rate | 160°C ± 2°C in ≤ 60 seconds | Medium-frequency induction heating coil under nitrogen |
| Maximum Transmitted Gear Torque | Up to 4,500 N·m | Splined 40Cr steel hub with dovetail mechanical interlock |
| Gear Meshing Noise Attenuation | Greater than or equal to 15 dB(A) | Measured vs conventional forged steel gears in closed gearbox |
| Mold Cavity Pre-Vacuum Level | Down to 1.0 kPa (Absolute) | Multi-stage vacuum evacuation skid with tool sealing |
| Finished Gear Diameter Envelope | Ø 400 mm to Ø 1,200 mm | Involute gear tooth tooling (Module m = 6– 16) |
Основное оборудование для этого решения
Справочные данные по оборудованию выбираются по документированному для них процессу. Основное дозирование, вспомогательная подача и альтернативные схемы не являются единым стандартным комплексом.
Управление процессом и прикладные проверки
Оцените эти функции с учетом выбранного материала, оснастки и производственного задания. Для результатов готовых деталей требуется отдельное приемочное подтверждение.
Defined metal/nylon interface
Coordinate mechanical retention and thermal preparation without assuming stress-free bonding.
Inspected casting quality
Agree internal/interface inspection instead of using vacuum as proof of no defects.
Comparable drive tests
Evaluate torque and noise on the same gear geometry, speed, load and enclosure baseline.
Связанные проекты
Это справочные данные по родственным применениям. Сравнивайте фактические материалы, процесс и поставленные модули; приведенные показатели проекта не являются приемочными результатами для другой линии.
Вопросы и ответы по планированию производства
Подбор, объём поставки и валидация для этого производственного направления.
Does a vacuum-assisted process guarantee torque capacity?
How should noise reduction be compared?
Какая информация необходима для предварительной конфигурации?
Обсудите ваши производственные задачи
Share the following with your production brief: Hub/tooth drawings, interlock, load and speed, thermal cycles, machining allowances and noise-test conditions. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


