
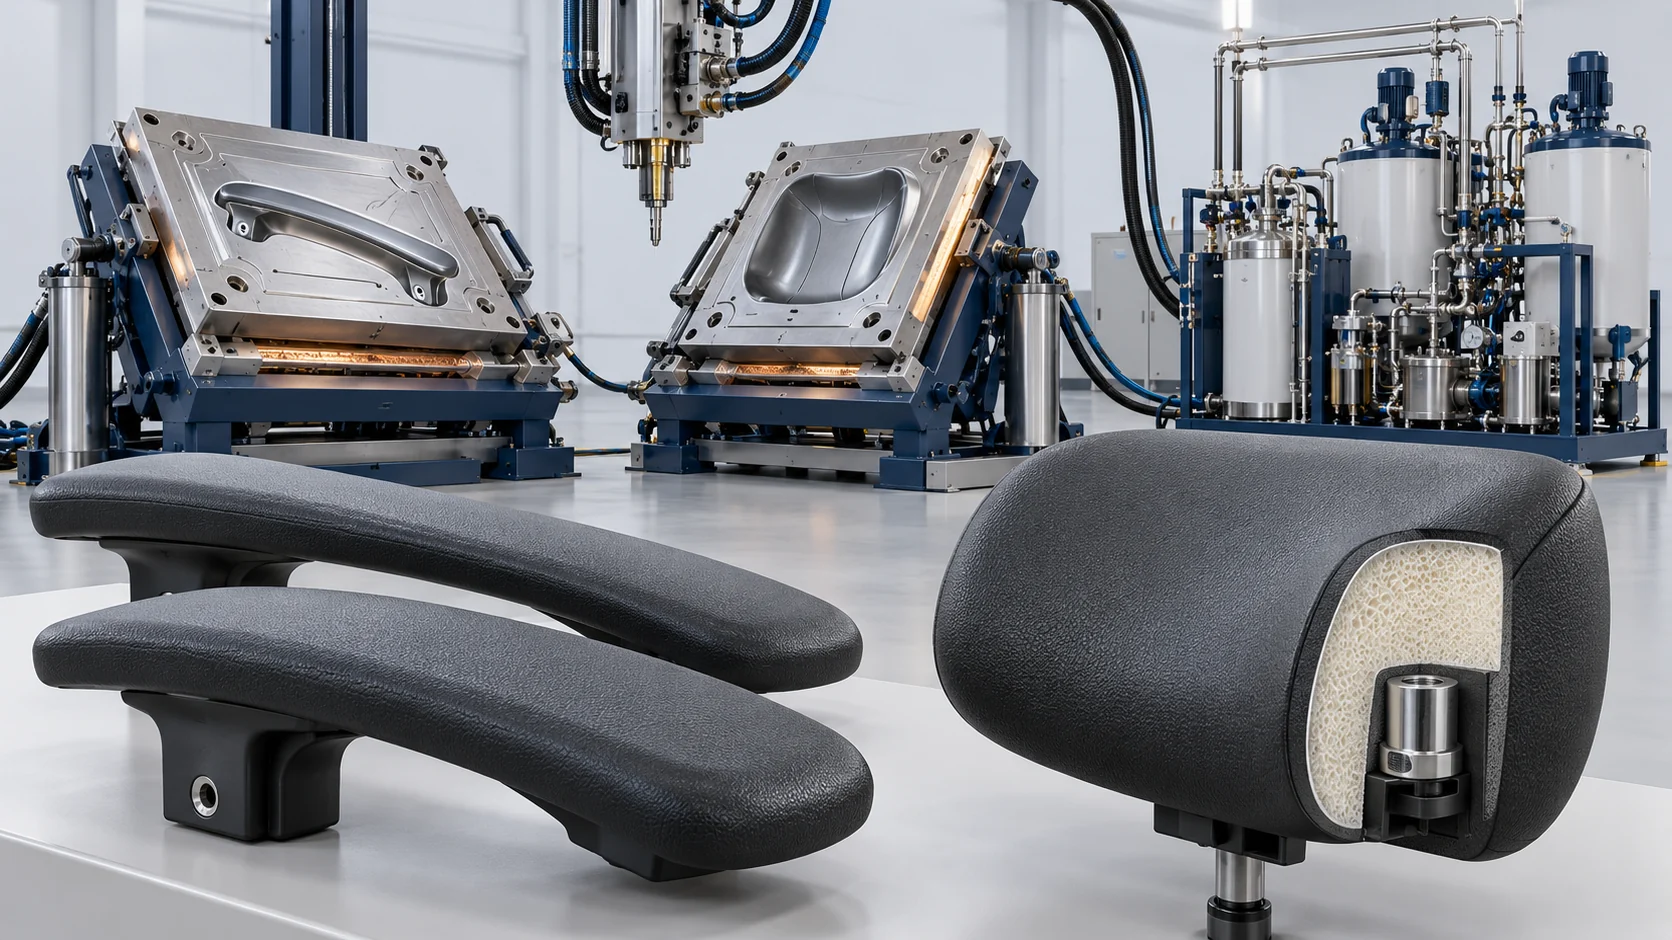
Integral Skin PU Foam Molding Solution
Precision reaction injection molding systems for integral skin armrests, headrests, and medical furniture, delivering wear-resistant solid skins and soft cores.
Precision Polyurethane Integral Skin Solutions for Ergonomic & Medical Furniture
Office chair armrests, dental patient chairs, and medical bed headrests require tactile soft-touch comfort combined with heavy scratch resistance and barrier impermeability against harsh hospital disinfectants. Traditional hand-upholstered fabric or PVC vinyl covers feature exposed stitched seams that harbor biological contaminants, trap dirt, and split under repeated mechanical abrasion. Haifeng’s automated high-pressure polyurethane integral skin foaming solution forms a seamless, dense outer skin that chemically transitions into an elastic, shock-absorbing microcellular core in a single mold shot. Operating with eco-friendly water-blown chemistry, it delivers flawless grain replication and durable chemical resistance.
Application-Specific Process Configuration
Office chair armrests, dental patient chairs, and medical bed headrests require tactile soft-touch comfort combined with heavy scratch resistance and barrier impermeability against harsh hospital disinfectants. Traditional hand-upholstered fabric or PVC vinyl covers feature exposed stitched seams that harbor biological contaminants, trap dirt, and split under repeated mechanical abrasion. Haifeng’s automated high-pressure polyurethane integral skin foaming solution forms a seamless, dense outer skin that chemically transitions into an elastic, shock-absorbing microcellular core in a single mold shot. Operating with eco-friendly water-blown chemistry, it delivers flawless grain replication and durable chemical resistance.
Integrated Delivery and Training
Haifeng delivers complete integral skin manufacturing cells—from low-emission high-pressure metering units and tilting mold clamps to automated In-Mold Coating (IMC) booths—allowing furniture producers to upgrade to premium seamless tactile components. Haifeng provides a 1-year comprehensive machine warranty, on-site installation, tooling commissioning and operator training, with long-term spare parts and remote PLC diagnostic support.
Haifeng delivers complete integral skin manufacturing cells—from low-emission high-pressure metering units and tilting mold clamps to automated In-Mold Coating (IMC) booths—allowing furniture producers to upgrade to premium seamless tactile components. Haifeng provides a 1-year comprehensive machine warranty, on-site installation, tooling commissioning and operator training, with long-term spare parts and remote PLC diagnostic support.
From Material Preparation to Finished Components
Coordinate formulation, metering, forming, curing and finishing around the selected product and production schedule.
Armature Positioning & In-Mold Coating
Metal mounting cores or nylon skeletons are secured onto mold positioning pins; automated or manual guns apply eco-friendly In-Mold Coating (IMC) or water-based release agents onto heated aluminum cavities.
Precision High-Pressure Tilting Injection
Servo displacement pumps inject water-blown self-skinning polyol and isocyanate at up to 190 bar through an anti-drip mixing head, while the mold carrier tilts 15°–45° dynamically to force displaced air upward toward perimeter vents.
Temperature-Driven Skin-to-Core Formation
Liquid contacting the cooler mold surface condenses and crosslinks rapidly into a solid, abrasion-resistant elastomeric outer skin, while the warmer core matrix expands into a resilient microcellular shock absorber.
Technical Specifications
Application and configuration data from the supplied engineering brief; final selection follows the product, formulation and factory layout.
| Technical Parameter | Standard Specification / Value | Engineering Context & Verification |
|---|---|---|
| Target Application | Medical Furniture Armrests, Office Chair 3D/4D Pads | Tactile high-wear furniture interfaces |
| Material Matrix | Polyurethane Integral Skin Elastomer (Water-Blown) | Eco-friendly zero-ODP formulation |
| Surface Hardness Range | Shore A 45 to Shore A 80 (Customizable) | Tailored from plush softness to rigid grips |
| Core Density Range | 250 – 450 kg/m³ | High shock-absorbing microcellular core |
| Metering Output Capacity | 10 – 35 kg/min (Customizable) | Micro-shot precision servo axial pumps |
| Demolding Cycle Time | 90 – 140 seconds (Standard 120 s) | High-cadence multi-carrier production |
| Surface Abrasion Endurance | >100,000 Rub Cycles (Taber / Wyzenbeek) | Verified zero peel or surface blistering |
Equipment for This Solution
The listed application machines show their own configurations. Furniture tooling, recipe, output and automation are configured for this solution.
Key Engineering Advantages
Process-specific equipment and controls selected for the furniture application.
Seamless Hygienic Impermeability
100% non-porous outer skin completely repels hospital sanitizers, fluids, and dirt without seam stitch traps.
Flawless Pinhole-Free Cosmetics
Synchronized mold tilting kinematics eliminate air pockets, delivering Class-A textured grain replication.
Variable Tactile Softness
Digital stoichiometric adjustment allows precise calibration between firm commercial armrests and plush medical headrests.
Rapid 120s Production Turnover
Accelerated reaction kinetics maximize manufacturing efficiency across compact multi-station mold lines.
Related Project Case
Review the production configuration, delivery and results.
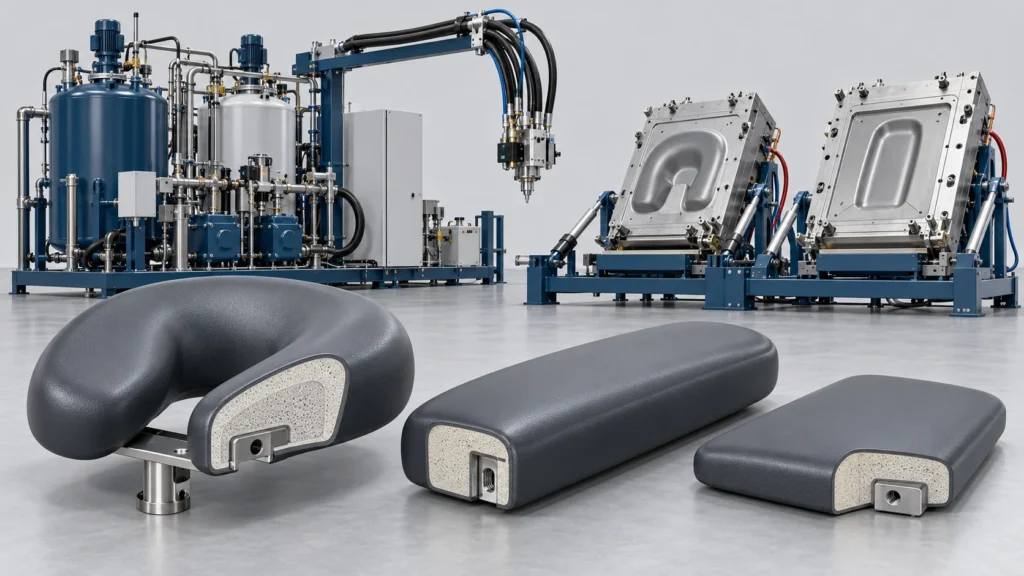
Medical Furniture Integral Skin PU Line Project in Russia
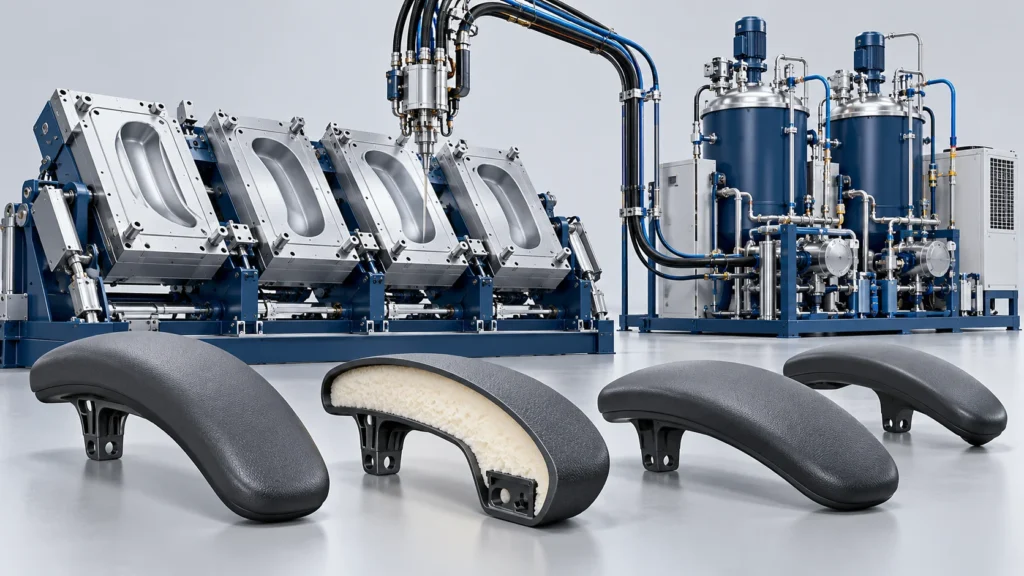
Office Chair Armrest Integral Skin PU Line Project in China
Frequently Asked Questions
Answers on process selection, equipment integration and delivery support.
How does an integral skin foam form both a solid skin and a soft core in one shot?
Can Haifeng equipment run 100% water-blown eco-friendly self-skinning PU?
How do tilting mold fixtures eliminate surface pinholes?
What is the typical installation and commissioning timeline on-site?
Discuss Your Furniture Production Project
For Polyurethane Integral Skin Foam Plant Solution, send finished-product drawings or samples, material data, target output, automation needs and factory conditions. Haifeng can use these inputs to discuss the line configuration and technical interfaces.


