
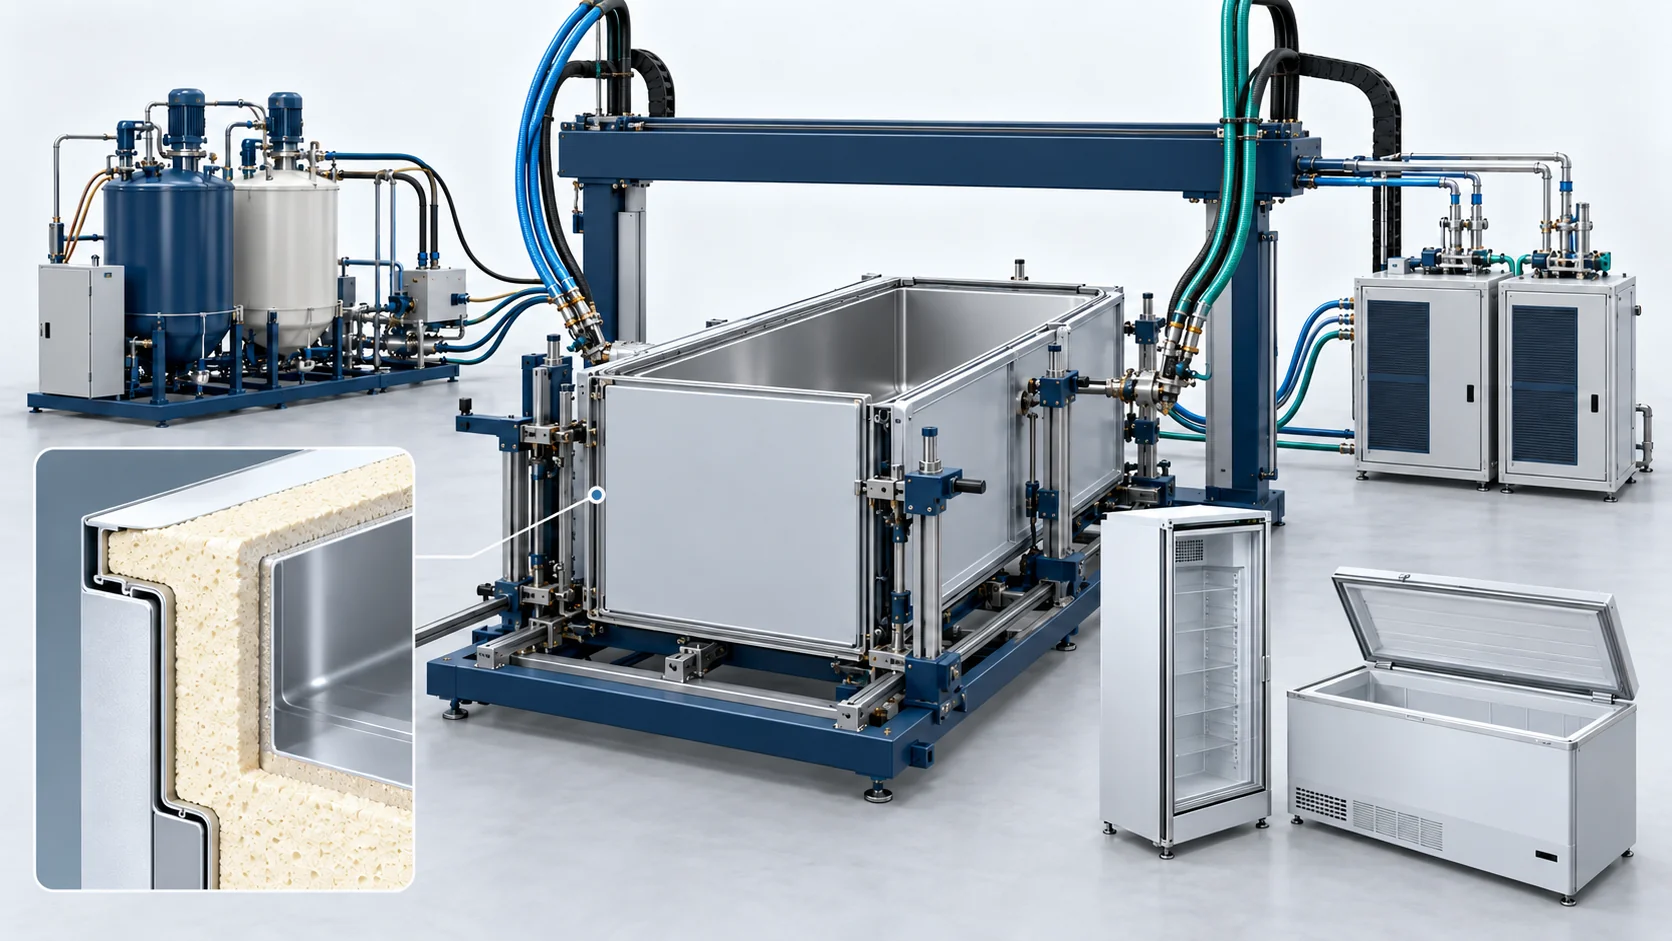
Commercial Freezer Foaming Solution
Plan high-mix freezer cabinet foaming with adjustable fixtures, two-head injection, coordinated temperature control and model-specific changeover procedures.
Agile Manufacturing for Diverse Commercial Display Refrigeration
Plan high-mix freezer cabinet foaming with adjustable fixtures, two-head injection, coordinated temperature control and model-specific changeover procedures. Core scope includes high-pressure metering and mixing, adjustable cabinet fixtures, head-positioning interfaces and temperature controls. Cyclopentane feed, detection, ventilation and interlocks require a project-specific hazardous-area assessment. Shells, chemistry, utilities and downstream handling are agreed interfaces.
Product, material and tooling
Core scope includes high-pressure metering and mixing, adjustable cabinet fixtures, head-positioning interfaces and temperature controls. Cyclopentane feed, detection, ventilation and interlocks require a project-specific hazardous-area assessment. Shells, chemistry, utilities and downstream handling are agreed interfaces.
Capacity and acceptance
Review all preparation, dispensing, curing, handling and inspection stages. Material and component results require separate original test records.
Configuration references are reviewed for the selected material, product geometry and acceptance conditions. ATEX suitability and Zone 1/2 boundaries are project-specific and require documentation; gas sensors and nitrogen alone do not establish certification. A 210-second mold dwell is not total line takt.
Flexible Commercial Freezer Foaming Workflow
The supplied process sequence is a configuration reference. Temperature, pressure, output and cure settings are confirmed for the selected material and tooling. ATEX suitability and Zone 1/2 boundaries are project-specific and require documentation; gas sensors and nitrogen alone do not establish certification. A 210-second mold dwell is not total line takt.
Recipe Model Selection & Motorized Sizing
Configured reference: Operators select cabinet model recipes on the HMI; motorized screw-jacks reset platen lengths (1.0–3.0 m) in under 8 minutes.
Cabinet Loading & 200 kN Hydraulic Lock
Configured reference: Pre-assembled outer and inner shells transfer into the bed; hydraulic cylinders clamp platens under 200 kN force to resist foam expansion.
Servo Rail Head Alignment & Docking
Configured reference: Dual high-pressure impingement heads traverse along linear guide rails to pre-calculated ports matching cabinet length.
Reference Solution Engineering Envelope
Values transcribed from the supplied configuration brief. Material properties and finished-product benchmarks are separate validation targets, not general equipment guarantees.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Cabinet Length Accommodation | 1,000 to 3,000 mm | Motorized adjustable fixture bed with recipe presets; supplied reference requiring configuration or test verification |
| Fixture Tool Changeover Time | Less than or equal to 8 minutes | Automated screw-jack drives and hydraulic locking pins; supplied reference requiring configuration or test verification |
| Combined Injection Output | 80.0 to 220.0 kg/min | Dual high-pressure impingement heads on servo rails; supplied reference requiring configuration or test verification |
| Total In-Mold Curing Cycle | Less than or equal to 210 seconds | At 45°C ± 1°C multi-zone tempered water circulation; supplied reference requiring configuration or test verification |
| Hydraulic Clamping Lock Force | 200 kN total clamping force | Heavy-duty steel frame resisting foam expansion; supplied reference requiring configuration or test verification |
| Hydrocarbon Safety Compliance | Project-specific assessment and documented scope | Hazardous-area classification, components, detection, ventilation and installed interfaces require engineering and original certification records |
Core Equipment for This Solution
The linked pages describe shared preparation or feed-system families, not proof of delivery of the dedicated models listed in the case. Core scope includes high-pressure metering and mixing, adjustable cabinet fixtures, head-positioning interfaces and temperature controls. Cyclopentane feed, detection, ventilation and interlocks require a project-specific hazardous-area assessment. Shells, chemistry, utilities and downstream handling are agreed interfaces.
Cyclopentane PU Foaming Machine | Refrigerators and Freezers
The HF-CP200-HP is an explosion-proof high-pressure polyurethane foaming machine engineered for precision cyclopentane premixing and uniform insulation filling in domestic and commercial refrigeration lines.
Cyclopentane Safety and Premixing System | PU Foaming
Cyclopentane storage/feed, premixing or inline blending and monitoring interfaces configured for a PU/PIR panel line. The project schedule defines supply boundaries and equipment documentation.
Core Advantages of Haifeng Commercial Systems
Engineering functions and interfaces developed for the specified product and material system.
Recipe-Driven Fixture Setup
Configure and validate recipe-driven fixture setup for the selected product, formulation, tooling and production conditions.
Two-Head Injection Planning
Configure and validate two-head injection planning for the selected product, formulation, tooling and production conditions.
Tool Temperature Control
Configure and validate tool temperature control for the selected product, formulation, tooling and production conditions.
Hydrocarbon Safety Interfaces
Configure and validate hydrocarbon safety interfaces for the selected product, formulation, tooling and production conditions.
Related Project Draft
Review the project configuration described in the supplied brief. Project records and reported results require verification before public use.
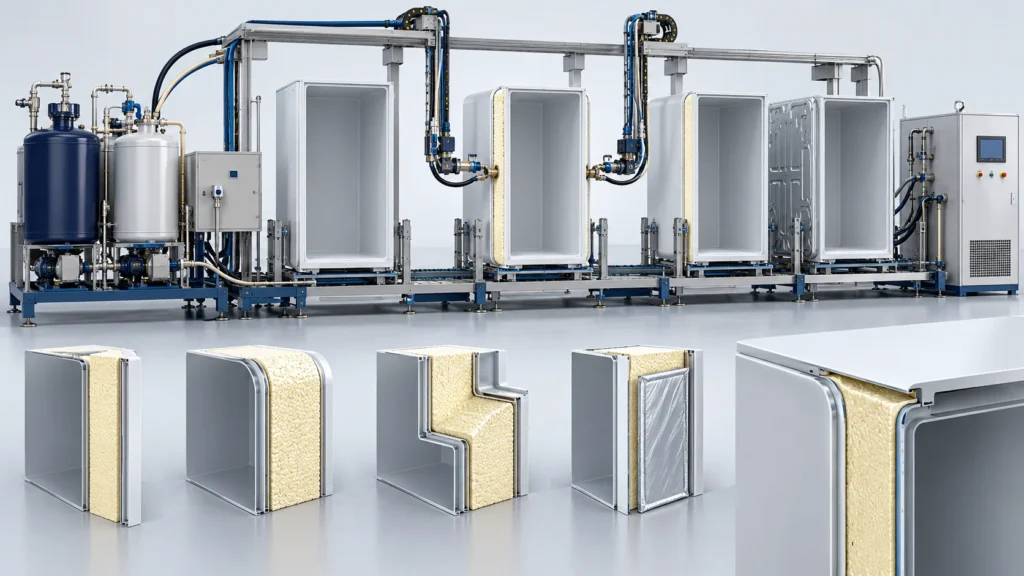
Frequently Asked Questions
Technical questions to establish the equipment scope, material window and validation plan.
How is two-head injection evaluated for long cabinets?
Can the fixture support different cabinet geometries?
How are clamping and sealing requirements established?
How are model recipes and changeovers configured?
Request a Commercial Freezer Foaming Proposal
Share your finished product or drawing, material system, target capacity, automation requirements and factory conditions to discuss the line configuration.


