
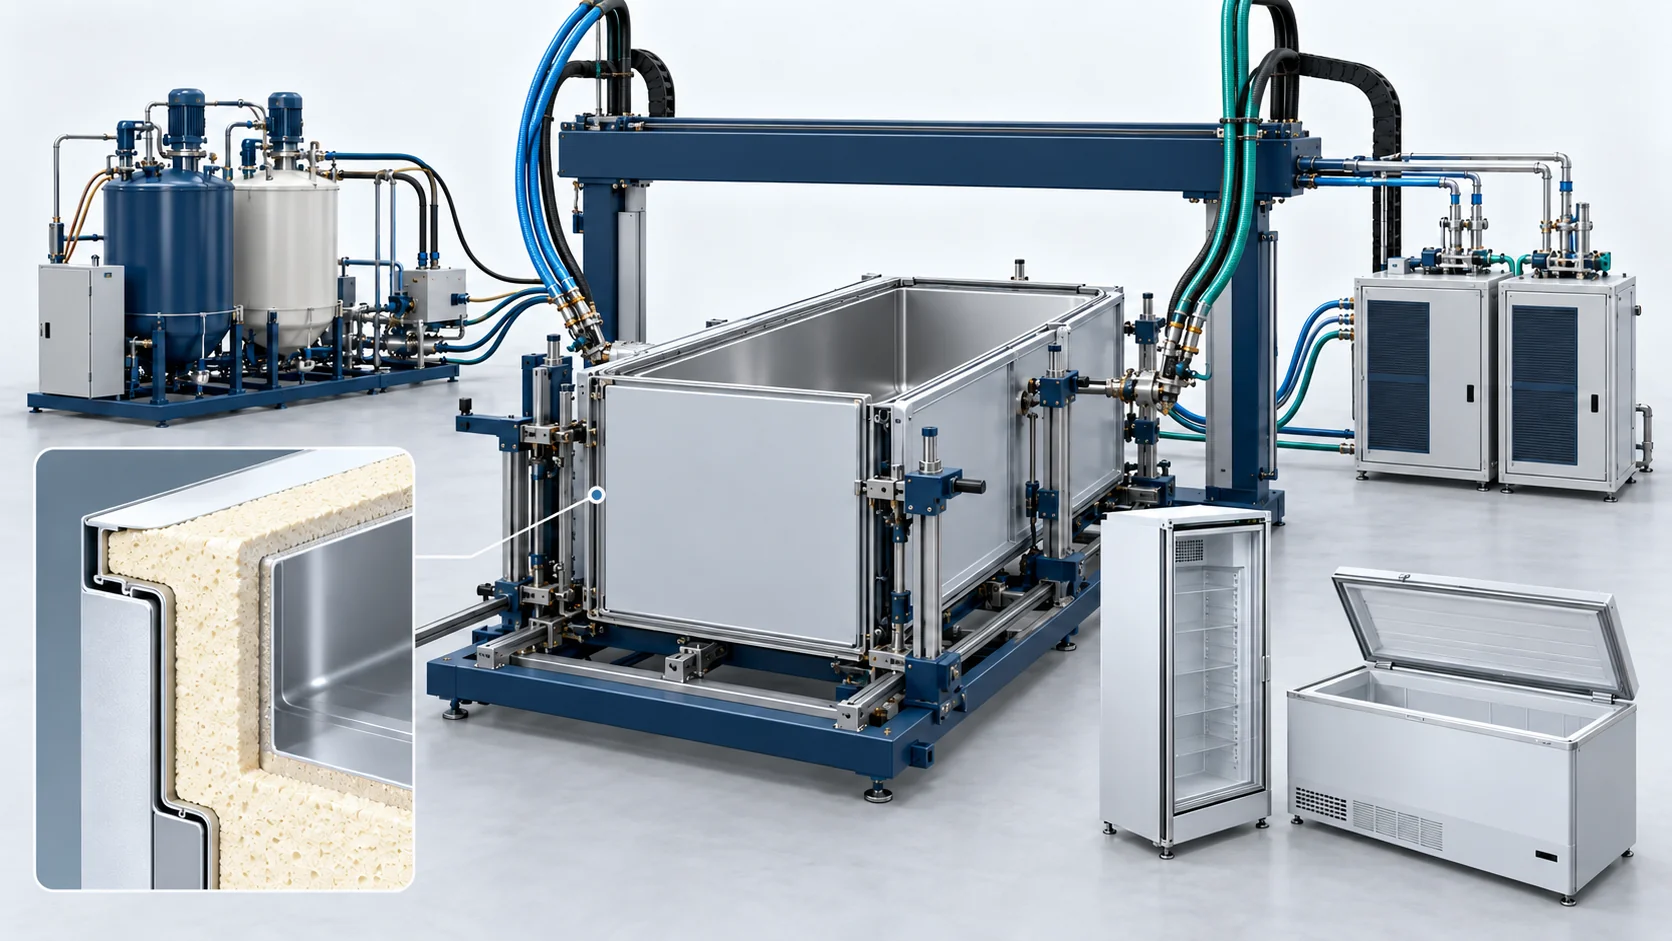
Solución de espumado para congeladores comerciales
Planifique el espumado de armarios de congelador de alta variedad con utillajes ajustables, inyección de dos cabezales, control de temperatura coordinado y procedimientos de cambio de modelo específicos.
Agile Manufacturing for Diverse Commercial Display Refrigeration
Plan high-mix freezer cabinet foaming with adjustable fixtures, two-head injection, coordinated temperature control and model-specific changeover procedures. Core scope includes high-pressure metering and mixing, adjustable cabinet fixtures, head-positioning interfaces and temperature controls. Cyclopentane feed, detection, ventilation and interlocks require a project-specific hazardous-area assessment. Shells, chemistry, utilities and downstream handling are agreed interfaces.
Producto, material y utillaje
Core scope includes high-pressure metering and mixing, adjustable cabinet fixtures, head-positioning interfaces and temperature controls. Cyclopentane feed, detection, ventilation and interlocks require a project-specific hazardous-area assessment. Shells, chemistry, utilities and downstream handling are agreed interfaces.
Capacidad y aceptación
Revise todas las etapas de preparación, dispensación, curado, manipulación e inspección. Los resultados de materiales y componentes requieren condiciones de ensayo acordadas por separado.
Plan adjustable cabinet fixtures, two-head delivery and temperature circuits for the actual model mix. Define changeover from the last accepted part to the next accepted model, including operator tasks and any material change or trial shots.
Flexible Commercial Freezer Foaming Workflow
La secuencia de proceso suministrada es una referencia de configuración. La temperatura, la presión, la producción y los ajustes de curado se confirman para el material y el utillaje seleccionados.
Recipe Model Selection & Motorized Sizing
Configured reference: Operators select cabinet model recipes on the HMI; motorized screw-jacks reset platen lengths (1.0–3.0 m) in under 8 minutes.
Cabinet Loading & 200 kN Hydraulic Lock
Configured reference: Pre-assembled outer and inner shells transfer into the bed; hydraulic cylinders clamp platens under 200 kN force to resist foam expansion.
Servo Rail Head Alignment & Docking
Configured reference: Dual high-pressure impingement heads traverse along linear guide rails to pre-calculated ports matching cabinet length.
Envolvente de ingeniería de la solución de referencia
Valores transcritos del informe de configuración suministrado. Las propiedades de los materiales y los parámetros de referencia del producto terminado son objetivos de validación independientes, no garantías generales del equipo.
| Parámetro | Valor / Unidad | Configuración / Condiciones aplicables |
|---|---|---|
| Cabinet Length Accommodation | 1,000 to 3,000 mm | Motorized adjustable fixture bed with recipe presets; supplied reference requiring configuration or test verification |
| Fixture Tool Changeover Time | Less than or equal to 8 minutes | Automated screw-jack drives and hydraulic locking pins; supplied reference requiring configuration or test verification |
| Combined Injection Output | 80.0 to 220.0 kg/min | Dual high-pressure impingement heads on servo rails; supplied reference requiring configuration or test verification |
| Total In-Mold Curing Cycle | Less than or equal to 210 seconds | At 45°C ± 1°C multi-zone tempered water circulation; supplied reference requiring configuration or test verification |
| Hydraulic Clamping Lock Force | 200 kN total clamping force | Heavy-duty steel frame resisting foam expansion; supplied reference requiring configuration or test verification |
| Hydrocarbon Safety Compliance | Project-specific assessment and documented scope | Hazardous-area classification, components, detection, ventilation and installed interfaces require engineering and original certification records |
Equipos principales de esta solución
The refrigerator metering platform and hydrocarbon premixing/safety references serve separate duties. Verify actual head/fixture and site interfaces.
Máquina de espumado PU con ciclopentano | Refrigeradores y congeladores
Máquina de espumado de PU con ciclopentano para frigoríficos y congeladores. Revise con Haifeng la configuración, los requisitos de materiales y las interfaces del proceso.
Sistema de seguridad y premzclado para ciclopentano | Espumado de PU
Sistema de seguridad y premzclado para ciclopentano para el espumado de PU. Revise la configuración, los requisitos de materiales y las interfaces de proceso con Haifeng.
Core Advantages of Haifeng Commercial Systems
Funciones de ingeniería e interfaces desarrolladas para el producto y el sistema de materiales especificados.
Fixture setup
Define recipes, locking and verification for each cabinet family.
Head delivery
Review total and individual-head shots and the actual filling sequence.
Tool temperature
Balance conditioning and cure across the model mix.
Site integration
Specify blowing-agent feed, detection, ventilation and interlocks for the installed cell.
Proyectos relacionados
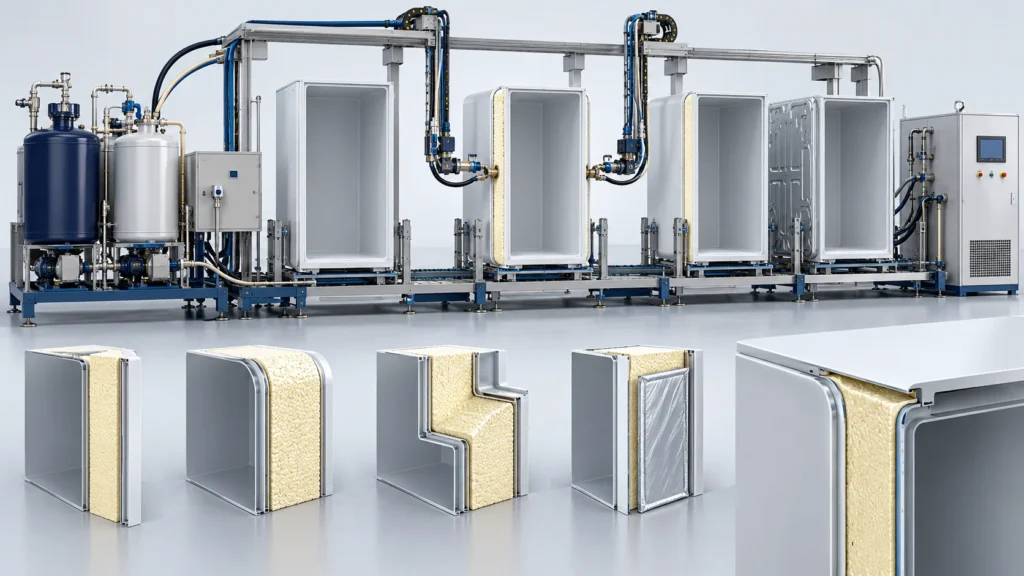
The freezer upgrade supports its selected cabinet family and retained/new modules, not every length or changeover combination.
Preguntas frecuentes
Preguntas técnicas para definir el alcance del equipo, la ventana de materiales y el plan de validación.
How is two-head injection evaluated for long cabinets?
Can the fixture support different cabinet geometries?
How are clamping and sealing requirements established?
How are model recipes and changeovers configured?
¿Qué datos se necesitan para esta configuración?
What should a cabinet changeover time include?
Request a Commercial Freezer Foaming Proposal
Share the following for this application: Cabinet models, shot and material, fixture range, changeover mix, head access, shifts and retained equipment. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


