

Automotive Sedan Spoiler RIM Dosing System Project in China
Haifeng delivered a high-pressure RIM dosing system for sedan spoilers, cutting tooling Capex by 55% with zero sink marks and 180s cycle times.
Project Overview
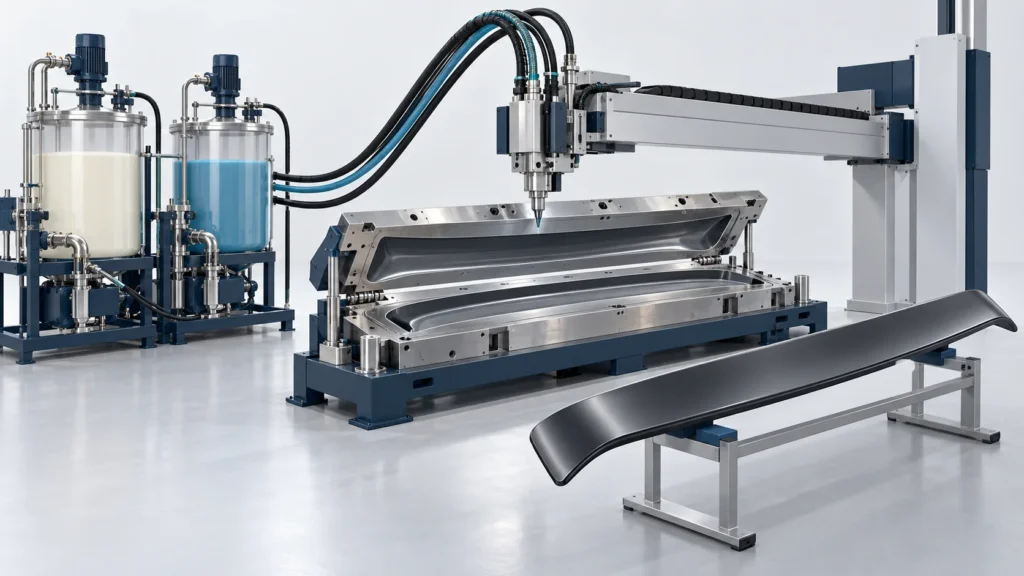
Illustration notice. Process illustrations are not verified photographs of this installation.
Project reference basis. Figures and configuration details are reported in the supplied project brief. They are reference values for the stated application, rather than verified acceptance results or a guarantee for another installation. Confirm the source records, material, tooling, operating schedule and test method when assessing a comparable project.
Haifeng successfully delivered and commissioned a high-precision Reaction Injection Molding (RIM) dosing system for a Sino-Foreign automotive exterior styling joint venture in China, cutting tooling and equipment Capex by 55% while eliminating sink marks on aerodynamic sedan rear spoilers. The project delivered a customized dual-component high-pressure polyurethane metering unit with an onboard industrial PLC control cabinet, dynamic temperature conditioning skids, and precision digital interface synchronization for the client's existing hydraulic clamping press.
Prior to commissioning, the manufacturer struggled with quality inconsistencies during the production of aerodynamic sedan spoilers. High-pressure injection molding of standard thermoplastics frequently induced sink marks and turbulent flow lines at structural rib junctions where wall thicknesses transition between 3mm and 6mm, resulting in surface imperfections that compromised the final Class-A paint finish. The customer required a low-cavity-pressure processing solution compatible with their existing steel tooling and clamping infrastructure, ensuring stable 0.4%–0.6% linear shrinkage compensation and smooth 1°–2° draft demolding without surface scuffing.
Operational since January 2025 on a continuous two-shift daily schedule across a 220 m² footprint, the installation provides reliable production stability. By leveraging Haifeng's closed-loop Ratio Lock metering and laminar low-pressure mold filling, the client produces high-durability exterior spoilers with superior stone-impact resilience and uniform substrate density ready for high-gloss Class-A painting.
Planning a related production line
Use this record as an application-specific reference. Reinforcement introduction, resin chemistry, tooling, consolidation and qualification differ between RIM, LFI, SMC and HP-RTM. A result from one process does not establish performance of another.
Production brief for technical discussion
Provide a finished-product drawing or sample, material data, target output, automation needs and factory conditions. Haifeng will review the process, equipment interfaces and acceptance plan for your own production goals.
Concept illustration: The process image is a concept illustration used to explain the equipment arrangement; it does not document the delivered site.
Solutions Delivery
Haifeng deployed a high-pressure impingement RIM platform optimized for low-pressure cavity flow, eliminating flow lines and reducing molding cycle times down to 180 seconds across the complete production sequence:
1. Closed-Loop Stoichiometric Ratio Lock: Polyol and isocyanate streams are metered via servo-driven displacement pumps under real-time closed-loop control, ensuring exact stoichiometric proportions and laminar cavity filling that prevents air entrapment.
2. Onboard Integrated Automation Architecture: The master PLC system and touch HMI are integrated directly onto the dosing chassis, synchronizing injection trigger curves, hydraulic interlocks, and safety protocols with the client’s existing clamping press.
3. Dual-Circuit Dynamic Thermal Stability: An external dynamic temperature conditioning skid maintains raw precursor and steel mold thermal equilibrium within ±1.0°C, ensuring uniform exotherm across variable 3mm–6mm wall geometries.
4. Self-Cleaning High-Pressure Injection Head: Haifeng’s hydraulic impingement mixing head executes rapid 0.3-second sharp shut-offs without chemical solvent flushing, maintaining continuous uptime across multi-shift operations.
Implementation & Training:
– Installation & Commissioning Timeline: 10 days from mechanical positioning and fluid piping to hydraulic press interlocking and trial shots.
– Operator Training: 3 days covering stoichiometric calibration, recipe management, self-cleaning head maintenance, and preventive seal checks.
– Key Commissioning Milestones: Dry-cycle pressure calibration, closed-loop ratio verification, steel mold thermal mapping, and first-article aerodynamic profile inspection.
| Equipment | Model | Qty | Function |
|---|---|---|---|
| High-Pressure Polyurethane RIM Dosing Machine | HF-RIM-HP40 | 1 Unit | Stoichiometric ratio metering, high-pressure impingement mixing & stream control |
| Integrated Industrial PLC Control Cabinet | HF-PLC-COMPACT | 1 Set | Built-in master process logic, servo pressure regulation & press digital interlocking |
| Dual-Circuit Dynamic Mold Temperature Controller | HF-TCU-36 | 2 Units | Precision dynamic fluid and mold thermal balancing for steel tooling |
| High-Pressure Impingement Mixing Head | HF-MIX-L16 | 1 Unit | High-velocity dual-component impingement mixing with hydraulic clean-off |
Project Results
Submit Your Production Goals
Share your product, material, target capacity, automation requirements and factory conditions to discuss a production line matched to your requirements.


