
Composite Compression Press | PCM and SMC
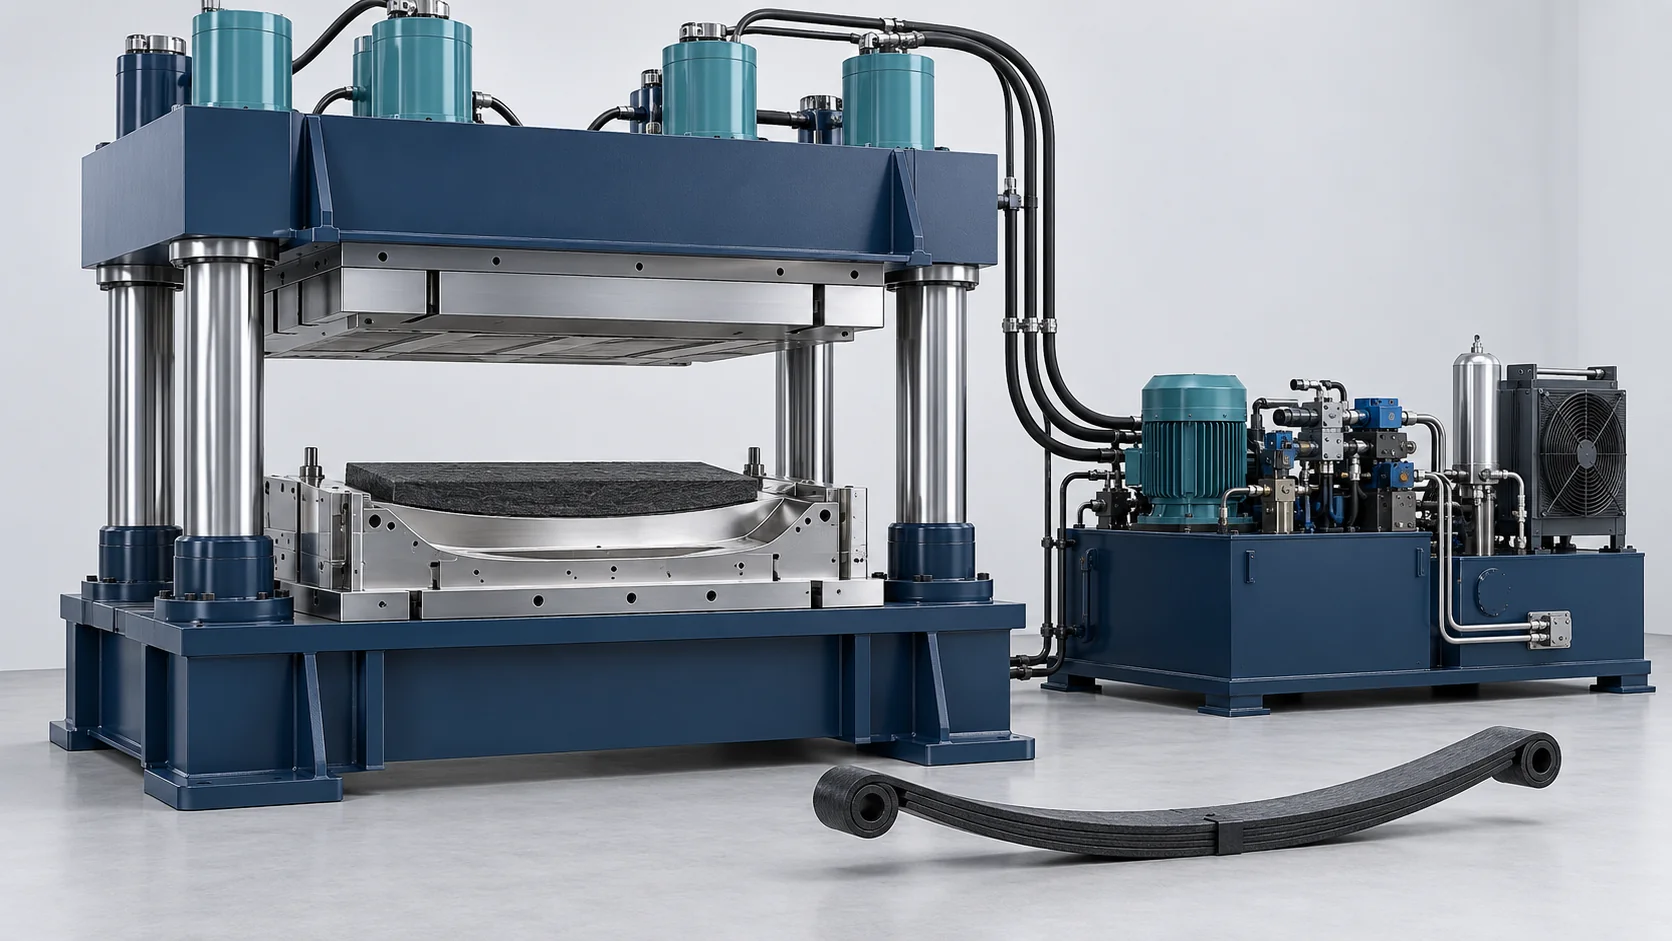
A multi-cylinder hydraulic compression press with active platen leveling for specified composite tooling and solid preforms.
Precision Active-Leveling Compression for Structural Leaf Springs
A multi-cylinder hydraulic compression press with active platen leveling for specified composite tooling and solid preforms.
A multi-cylinder hydraulic compression press with active platen leveling for specified composite tooling and solid preforms.
Press frame, hydraulic power/accumulator, platen-leveling feedback, heating and controls. Prepreg/SMC charge, molds, handling and part qualification are separately agreed.
Nominal pressing force is 30,000 kN, approximately 3,059 metric tonnes-force. Hydraulic-system pressure, tool cavity pressure and platen leveling are separate quantities. Spring weight and fatigue figures describe the specified finished-part comparison and test.
Concept illustration: Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Material Flow and Working Principle
Automated Charge Stacking & Preheating
High-strength continuous glass fiber epoxy prepreg sheets (PCM) or high-fiber vinyl SMC blanks are cut by ultrasonic knives and robotically stacked into a parabolic charge pack.
Fast Robot Placement in Heated Tooling
A specialized pneumatic needle gripper transfers the thick charge pack into the lower tool cavity heated to 150°C ± 1°C inside the 3,000-ton press.
High-Speed Closing & Active Micro-Leveling
The press descends at 400 mm/s; upon contact, four corner leveling cylinders engage, ramping to full 3,000-ton force in 1.8 seconds while holding parallelism within ±0.02 mm.
Isothermal High-Pressure Consolidation
The tool maintains continuous 12.0 MPa cavity pressure for 180 seconds, ensuring dense resin flow into parabolic tapers and crosslinking the matrix without internal voids.
Automated Extraction & Deflashing
Platen cylinders de-pressurize and open smoothly; hydraulic bottom ejector pins elevate the hot leaf spring for robotic extraction and robotic edge-milling.
Model and Technical Parameters
Supplied HF-PCM3000-AL configuration references for the selected material, tooling and operating conditions. Nominal pressing force is 30,000 kN, approximately 3,059 metric tonnes-force. Hydraulic-system pressure, tool cavity pressure and platen leveling are separate quantities. Spring weight and fatigue figures describe the specified finished-part comparison and test.
| Technical Parameter | HF-PCM3000-AL |
|---|---|
| Components | Solid preform or prepreg tooling; no liquid proportioning |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 440V/480V 60Hz optional) |
| Working Pressure | 25.0 to 31.5 MPa (Main hydraulic cylinder system) |
| Weight | 145,000 kg (Complete press frame, cylinders, and hydraulics) |
| Dimensions (L×W×H) | 6200 mm x 4500 mm x 7800 mm (Machine bed footprint & height) |
| Active Leveling Precision | ≤ 0.02 mm (Under 30,000 kN off-center load); Optical linear encoders on 4 corners; configuration-specific reference |
| Full Pressurization Time | ≤ 1.8 seconds (Ramp to 3,000-ton clamp); High-speed accumulator assist; configuration-specific reference |
| Platen Fast Downward Speed | Up to 400 mm/s (Servo gravity fast approach); Platen descent stroke; configuration-specific reference |
| Leaf Spring Fatigue Durability | ≥ 1,000,000 Cycles (Full load bench test); Automotive leaf spring test rig; configuration-specific reference |
| Nominal pressing force | Nominal Pressing Force: 30,000 kN (approximately 3,059 metric tonnes-force); configuration-specific reference |
| Supplied preform fiber fraction | 60% to 70% Fiber Content by weight (Prepreg formulation); configuration-specific reference |
| Active platen leveling precision | ±0.02 mm (4-Corner active dynamic leveling precision); configuration-specific reference |
| Hydraulic oil reservoir | Hydraulic oil reservoir: 4,500 L (Mineral hydraulic fluid); configuration-specific reference |
Key Equipment Features
Press frame, hydraulic power/accumulator, platen-leveling feedback, heating and controls. Prepreg/SMC charge, molds, handling and part qualification are separately agreed.
±0.02 mm 4-Corner Active Leveling
Supplied configuration reference: Four independent digital servo cylinders correct platen tilt dynamically under severe off-center parabolic spring charges. Actual capability requires material and tooling validation.
1.8-Second Fast Pressurization
Supplied configuration reference: Servo variable pumps and accumulators ramp to 3,000 tons in 1.8 seconds, preventing fast-curing epoxy pre-gel defects. Actual capability requires material and tooling validation.
120 kg Chassis Weight Reduction
Supplied configuration reference: Replaces multi-leaf steel spring packs with lightweight composite springs, shedding 120 kg per truck. Actual capability requires material and tooling validation.
1 Million Fatigue Cycle Lifespan
The supplied 1,000,000-cycle reference is a finished-spring bench result for the specified material, geometry and loading; it is not a press rating or general fatigue-life guarantee.


