
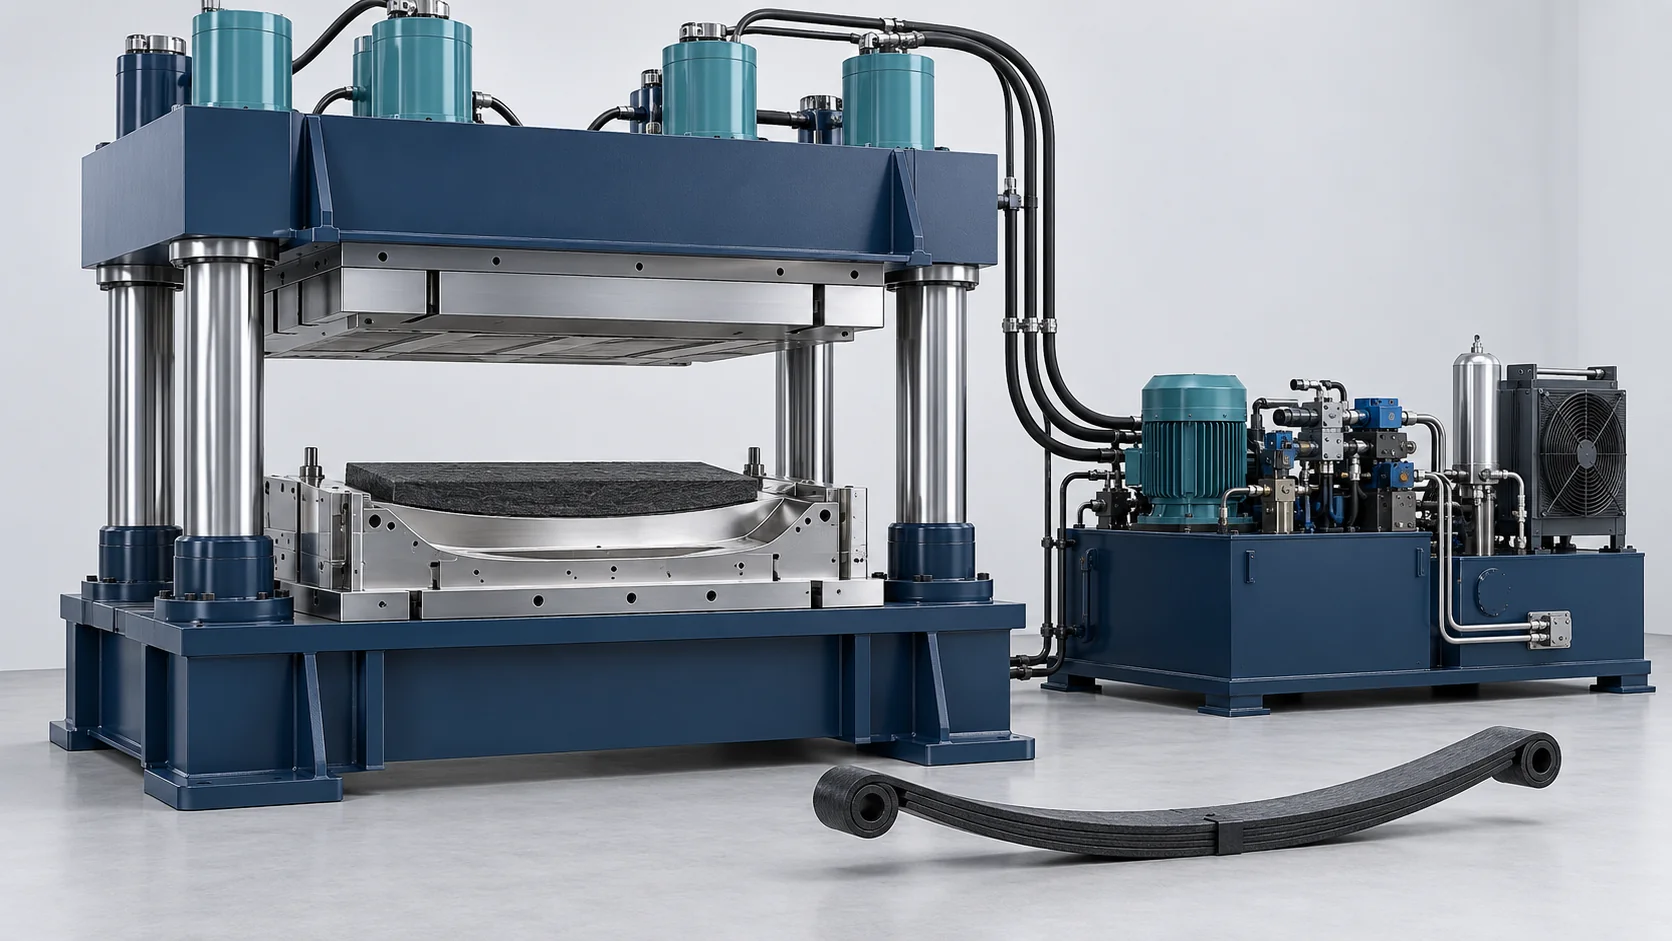
Пресс для композитов | PCM и SMC
Многоцилиндровый гидравлический пресс с активной системой выравнивания плит для заданной оснастки для композитов и цельных преформ.
Nominal Pressing Force
Nominal Pressing Force: 30,000 kN (approximately 3,059 metric tonnes-force); configuration-specific reference
Hydraulic Working Pressure
25.0 to 31.5 MPa (Main hydraulic cylinder system)
Platen Leveling Reference
±0.02 mm (4-Corner active dynamic leveling precision); configuration-specific reference
Fast Platen Descent
Up to 400 mm/s (Servo gravity fast approach); Platen descent stroke; configuration-specific reference
Precision Active-Leveling Compression for Structural Leaf Springs
Многоцилиндровый гидравлический пресс с активной системой выравнивания плит для заданной оснастки для композитов и цельных преформ.
Многоцилиндровый гидравлический пресс с активной системой выравнивания плит для заданной оснастки для композитов и цельных преформ.
Press frame, hydraulic power/accumulator, platen-leveling feedback, heating and controls. Prepreg/SMC charge, molds, handling and part qualification are separately agreed.
Nominal pressing force is 30,000 kN, approximately 3,059 metric tonnes-force. Hydraulic-system pressure, tool cavity pressure and platen leveling are separate quantities. Spring weight and fatigue figures describe the specified finished-part comparison and test.
Концептуальная иллюстрация: Сгенерированная концептуальная иллюстрация для обсуждения процесса; это не фотография указанной машины, предприятия заказчика или реализованного проекта.
Поток материалов и принцип работы
Automated Charge Stacking & Preheating
High-strength continuous glass fiber epoxy prepreg sheets (PCM) or high-fiber vinyl SMC blanks are cut by ultrasonic knives and robotically stacked into a parabolic charge pack.
Fast Robot Placement in Heated Tooling
A specialized pneumatic needle gripper transfers the thick charge pack into the lower tool cavity heated to 150°C ± 1°C inside the 3,000-ton press.
High-Speed Closing & Active Micro-Leveling
The press descends at 400 mm/s; upon contact, four corner leveling cylinders engage, ramping to full 3,000-ton force in 1.8 seconds while holding parallelism within ±0.02 mm.
Isothermal High-Pressure Consolidation
The tool maintains continuous 12.0 MPa cavity pressure for 180 seconds, ensuring dense resin flow into parabolic tapers and crosslinking the matrix without internal voids.
Automated Extraction & Deflashing
Platen cylinders de-pressurize and open smoothly; hydraulic bottom ejector pins elevate the hot leaf spring for robotic extraction and robotic edge-milling.
Нужно коммерческое предложение на это оборудование?
Запросить предложениеМодель и технические параметры
Supplied HF-PCM3000-AL configuration references for the selected material, tooling and operating conditions. Nominal pressing force is 30,000 kN, approximately 3,059 metric tonnes-force. Hydraulic-system pressure, tool cavity pressure and platen leveling are separate quantities. Spring weight and fatigue figures describe the specified finished-part comparison and test.
| Технический параметр | HF-PCM3000-AL |
|---|---|
| Компоненты | Solid preform or prepreg tooling; no liquid proportioning |
| Электропитание | 380 В, 3 фазы, 50 Гц (по заказу 440 В/480 В 60 Гц) |
| Рабочее давление | 25.0 to 31.5 MPa (Main hydraulic cylinder system) |
| Масса | 145,000 kg (Complete press frame, cylinders, and hydraulics) |
| Габариты (Д×Ш×В) | 6200 mm x 4500 mm x 7800 mm (Machine bed footprint & height) |
| Active Leveling Precision | ≤ 0.02 mm (Under 30,000 kN off-center load); Optical linear encoders on 4 corners; configuration-specific reference |
| Full Pressurization Time | ≤ 1.8 seconds (Ramp to 3,000-ton clamp); High-speed accumulator assist; configuration-specific reference |
| Platen Fast Downward Speed | Up to 400 mm/s (Servo gravity fast approach); Platen descent stroke; configuration-specific reference |
| Leaf Spring Fatigue Durability | ≥ 1,000,000 Cycles (Full load bench test); Automotive leaf spring test rig; configuration-specific reference |
| Nominal pressing force | Nominal Pressing Force: 30,000 kN (approximately 3,059 metric tonnes-force); configuration-specific reference |
| Supplied preform fiber fraction | 60% to 70% Fiber Content by weight (Prepreg formulation); configuration-specific reference |
| Active platen leveling precision | ±0.02 mm (4-Corner active dynamic leveling precision); configuration-specific reference |
| Hydraulic oil reservoir | Hydraulic oil reservoir: 4,500 L (Mineral hydraulic fluid); configuration-specific reference |
Ключевые особенности оборудования
Press frame, hydraulic power/accumulator, platen-leveling feedback, heating and controls. Prepreg/SMC charge, molds, handling and part qualification are separately agreed.
±0.02 mm 4-Corner Active Leveling
Supplied configuration reference: Four independent digital servo cylinders correct platen tilt dynamically under severe off-center parabolic spring charges. Actual capability requires material and tooling validation.
Configured Pressurization Sequence
Coordinate the hydraulic pressure ramp, tool closure and consolidation with the selected prepreg or SMC reaction window. The nominal force is 30,000 kN; complete cycle time includes handling and cure.
Composite Part and Tooling Interfaces
Select charge, molds, thermal cycle and handling for the intended spring or panel. Component weight and fatigue requirements are evaluated on the finished design.
1 Million Fatigue Cycle Lifespan
The supplied 1,000,000-cycle reference is a finished-spring bench result for the specified material, geometry and loading; it is not a press rating or general fatigue-life guarantee.
Обсудите конфигурацию вашего оборудования
Сообщите о вашей продукции, материалах, оснастке и требованиях к производству, чтобы мы могли рассмотреть оборудование и интерфейсы для вашего проекта.
Часто задаваемые вопросы
Why is ±0.02 mm active leveling critical when molding parabolic leaf springs?
How does 1.8-second fast pressurization benefit fast-curing epoxy prepregs?
What enables composite leaf springs to survive 1 million fatigue cycles?
Can this press also mold carbon fiber battery covers and chassis panels?
Готовы обсудить ваш проект?
Свяжитесь с нашей командой


