
HFFR Flame Retardant TPU Solution
Gravimetric TPU and mineral-additive feeding with configured compounding, venting and pelletizing for cable-grade development.
High-Filler Compounding Without Sacrificing Cable Flexibility
Gravimetric TPU and mineral-additive feeding with configured compounding, venting and pelletizing for cable-grade development.
Equipment and process scope
Pellet feed, staged powder side feeds, liquid additives, compounding extruder and pelletizing stages; cable extrusion, final formulation and finished-cable qualification are separate.
Validation and production planning
This is pellet/additive compounding rather than a primary liquid reactive-polymerization route. UL 94 V-0 at 0.8 mm and oxygen index concern the tested compound/specimen; they do not establish cable qualification or machine certification. Feeder accuracy and final dispersion are different measures.
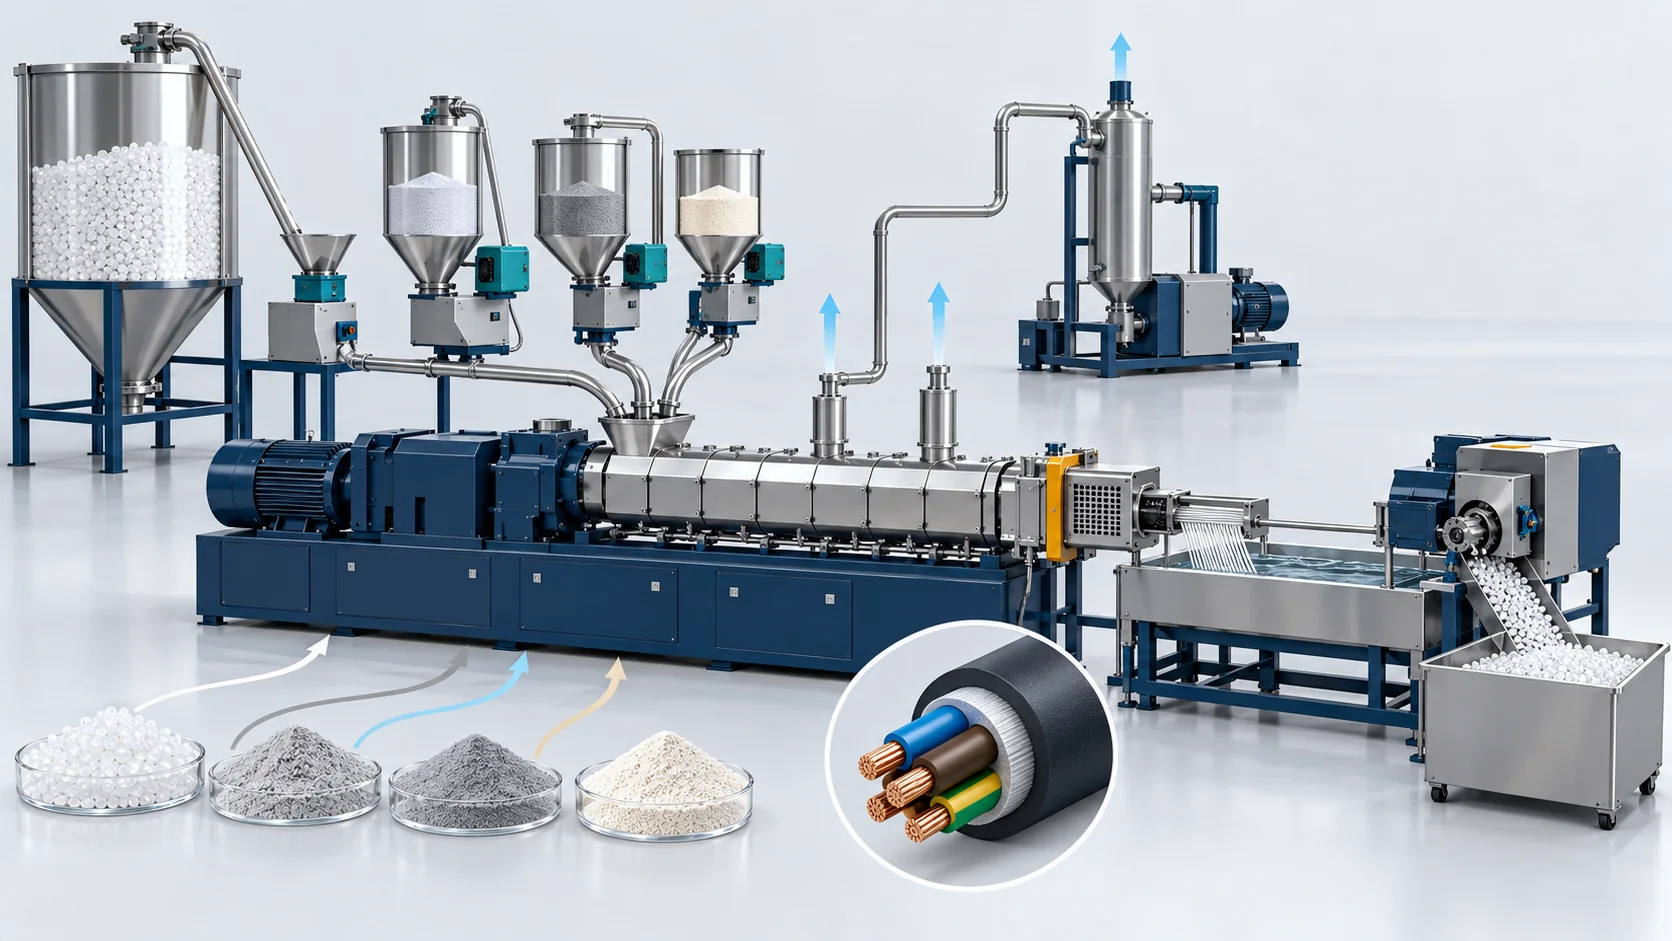
Pellet feed, staged powder side feeds, liquid additives, compounding extruder and pelletizing stages; cable extrusion, final formulation and finished-cable qualification are separate. This is pellet/additive compounding rather than a primary liquid reactive-polymerization route. UL 94 V-0 at 0.8 mm and oxygen index concern the tested compound/specimen; they do not establish cable qualification or machine certification. Feeder accuracy and final dispersion are different measures.Generated concept illustration for process discussion; not a photograph of the specified machine, a customer facility or a delivered project.
Turnkey HFFR TPU Compounding Process
Configuration sequence from the supplied brief. Material, tool, pressure/temperature basis and complete line balance require verification. This is pellet/additive compounding rather than a primary liquid reactive-polymerization route. UL 94 V-0 at 0.8 mm and oxygen index concern the tested compound/specimen; they do not establish cable qualification or machine certification. Feeder accuracy and final dispersion are different measures.
Gravimetric Loss-in-Weight Feeding
Supplied process reference: TPU base pellets and liquid processing aids are metered into the main feed throat with digital gravimetric accuracy within ±0.3%.
Low-Temperature Screw Plasticization
Supplied process reference: The virgin TPU resin is melted across Zones 1–5 through forward-conveying blocks, forming a stable melt seal at 175°C.
Twin-Stage Forced Powder Injection
Supplied process reference: Dual-stage side stuffers compact and inject de-aerated mineral flame retardants (ATH/MCA) into the melt pool at Zones 6 and 8.
Reference Solution Engineering Envelope
Supplied configuration and validation references; material/component results are separate from equipment ratings.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Continuous Production Output | 300.0 to 800.0 kg/hour | High-torque co-rotating twin-screw compounding line; supplied configuration or material target, pending the applicable original records |
| Mineral Filler Loading Capacity | 40% to 60% by weight | Dual-stage forced side stuffers with powder de-aeration; supplied configuration or material target, pending the applicable original records |
| Finished Material Flame Rating | UL94 V-0 (At 0.8 mm thickness) | Vertical burn test compliant with zero burning drips; supplied configuration or material target, pending the applicable original records |
| Retained Tensile Elongation | Greater than or equal to 400% | ASTM D412 testing on compounded cable jacket matrix; supplied configuration or material target, pending the applicable original records |
| Limiting Oxygen Index (LOI) | Greater than or equal to 35% | ASTM D2863 oxygen index measurement on compound; supplied configuration or material target, pending the applicable original records |
| Pelletizing Mechanism Type | Die-face water-ring cutting | Tungsten-titanium carbide die plate with water ring; supplied configuration or material target, pending the applicable original records |
Core Equipment for This Solution
Pellet feed, staged powder side feeds, liquid additives, compounding extruder and pelletizing stages; cable extrusion, final formulation and finished-cable qualification are separate.
Core Advantages of Haifeng HFFR Systems
Configured equipment functions and interfaces for the selected material and tooling.
reported UL94 V-0 Fire Safety
Supplied configuration function: Dense micro-dispersion of non-halogenated minerals yields self-extinguishing flame resistance without dripping. Project-dependent performance requires validation.
60% Filler Capacity
Supplied configuration function: Dual-stage side feeders eliminate hopper bridging, allowing massive powder loading up to 60 wt%. Project-dependent performance requires validation.
Preserved Flexibility (> 400% Elongation)
Supplied configuration function: Low-shear gear blocks prevent polymer chain breakdown, ensuring extreme cable flexibility at -30°C. Project-dependent performance requires validation.
Flawless Cable Jacket Surface
Supplied configuration function: Complete powder de-aeration and 0.05 kPa vacuum drying eliminate pinholes and surface craters (Ra ≤ 1.2 µm). Project-dependent performance requires validation.
Related Project Draft
An anonymous project brief from the supplied document. Original attribution, dates, acceptance and outcome records require verification before public use.
Frequently Asked Questions
How does the machine achieve UL94 V-0 at thin 0.8 mm cable walls?
Why is water-ring cutting preferred over strand cutting for HFFR compounds?
How does the system prevent ATH decomposition during processing?
Can this line produce flame-retardant compounds for robotic drag-chain cables?
Discuss Your Production Goals
Share your product or drawing, material system, target output, automation needs and factory utilities so the equipment and interfaces can be configured.


