
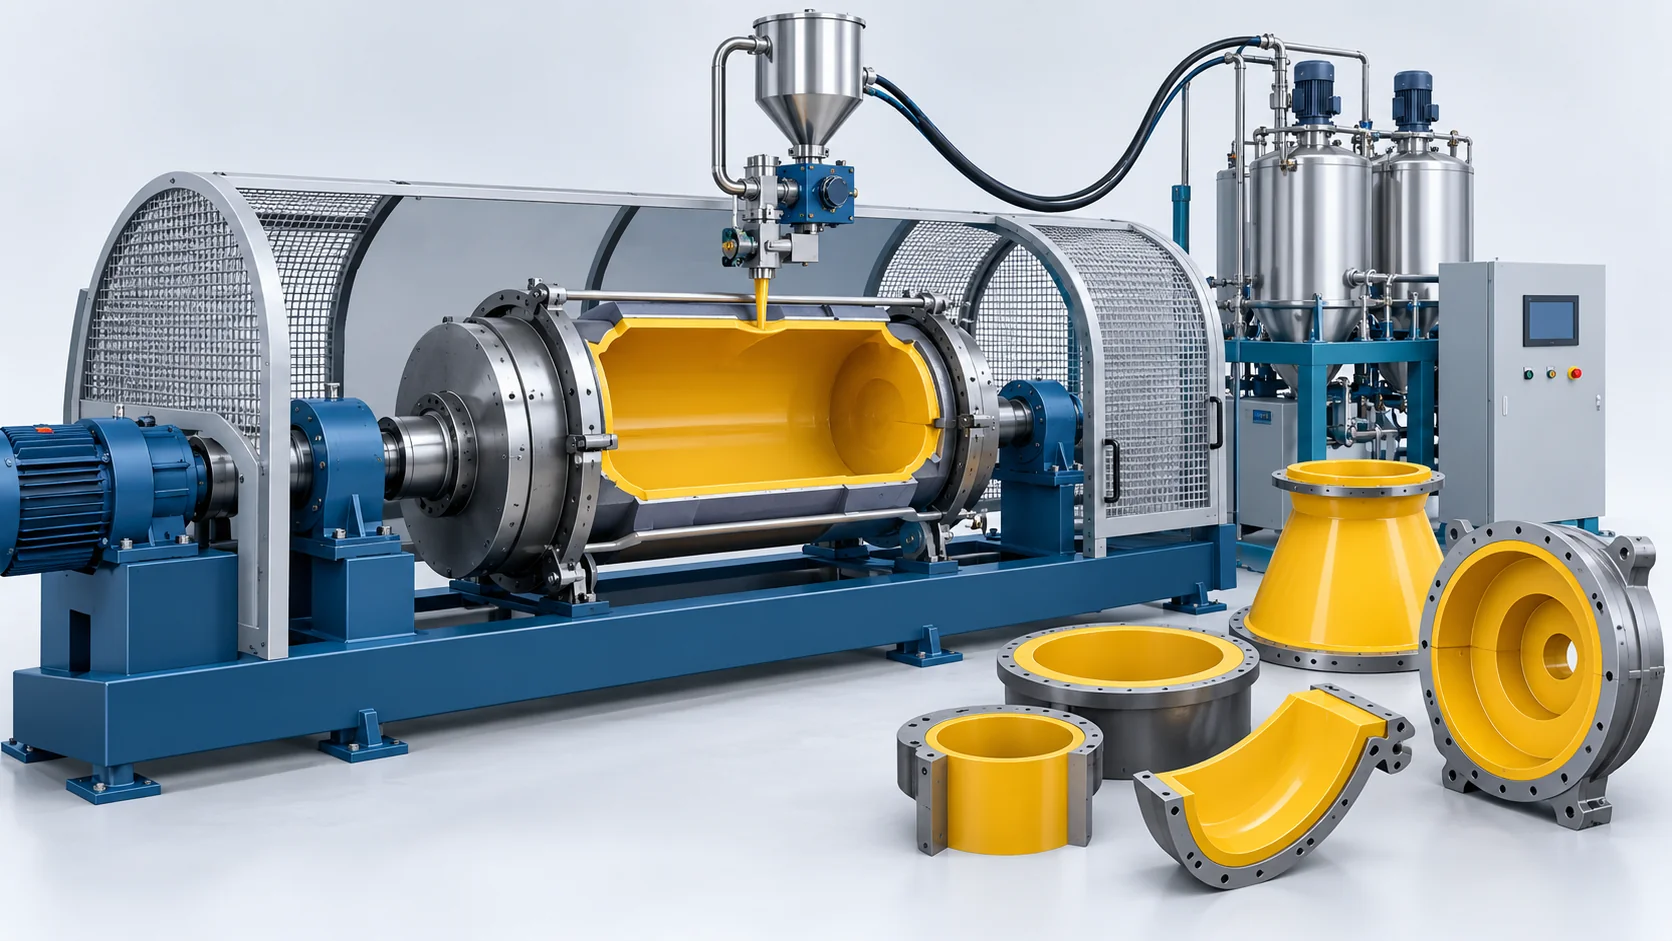
Centrifugal PU Casting Machine | Pump and Cyclone Liners
High-volume CPU metering, an extended dispensing boom and configured centrifugal tooling for mineral-processing pump and cyclone liners.
Heavy Centrifugal Elastomer Casting for Mining Slurry Handling
High-volume CPU metering, an extended dispensing boom and configured centrifugal tooling for mineral-processing pump and cyclone liners.
High-volume CPU metering, an extended dispensing boom and configured centrifugal tooling for mineral-processing pump and cyclone liners.
The package covers material preparation, high-volume metering, an extended servo dispensing arm, the specified centrifugal station and controls. Hydraulic mold handling and heated curing equipment are optional. Chemicals are supplied separately; lifting equipment and compressed air are customer interfaces. Tooling mass, imbalance and permitted speed are confirmed together.
Material Flow and Working Principle
High-Temperature Degassing & Chemical Conditioning
High-performance NDI or PPDI prepolymers are heated via thermal oil jackets to 125°C in 250 L stainless steel tanks and continuously degassed below 0.05 kPa to extract micro-bubbles.
High-Volume Servo-Gear Proportioning
High-displacement servo-driven rotary gear pumps deliver chemicals through electrically heated lines, with Coriolis flow meters continuously adjusting pump displacement within ±0.2%.
High-Shear Dynamic Micro-Room Mixing
Component streams enter a water-jacketed dynamic mixing chamber equipped with a hardened helical rotor operating at 4,000 RPM, achieving thorough homogenization without premature reaction scorch.
Centrifugal Injection via Extended Servo Boom
The casting sequence is developed for the actual mold and liner mass. Permitted speed, balancing, filling time and the material gel window require project validation; the supplied maximum flow is 25 kg/min.
Centrifugal In-Mold Curing & Annealing
Centrifugal spinning continues during gelation (15–20 minutes) to prevent shrinkage voids, followed by mold opening and transfer to hot air ovens for secondary crosslinking.
Model and Technical Parameters
Configuration values from the supplied HF-CPU250-CF brief. Final performance is confirmed for the chemical formulation, tool, operating conditions and original calibration records. Casting-circuit pressure is distinct from finished-component service or qualification pressure.
| Technical Parameter | HF-CPU250-CF |
|---|---|
| Components | 2 Primary Streams (A: Prepolymer, B: Curative) + 1 Additive Stream |
| Output Range (g/s) | 4.0 to 25.0 kg/min (Continuous adjustable) |
| Mixing Ratio Range | 100:10 to 100:40 (By weight) |
| Ratio Accuracy | ±0.2% (Continuous closed-loop Coriolis feedback) |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 440V/480V 60Hz optional) |
| Working Pressure | 0.4 to 0.8 MPa (Metering lines and dynamic head) |
| Tank Capacity (L) | Tank A: 250 L (Oil-jacketed), Tank B: 100 L (Stainless steel) |
| Weight | 5,200 kg (Including centrifugal turntable station) |
| Dimensions (L×W×H) | 4200 mm x 2600 mm x 2800 mm |
| Centrifugal Table Velocity | Up to 1,500 RPM (Variable frequency AC motor); Dynamic balanced load condition |
| Maximum Mold Load Capacity | Up to 800 kg (Tooling plus part weight); Centrifugal turntable bed |
| Servo Pouring Boom Stroke | 2,200 mm (Horizontal reach); 3-Axis cantilever arm |
| Process Heating Limit | Up to 135°C (Circulating thermal oil jacket); Tanks, pumps, and delivery lines |
Key Equipment Features
The package covers material preparation, high-volume metering, an extended servo dispensing arm, the specified centrifugal station and controls. Hydraulic mold handling and heated curing equipment are optional. Chemicals are supplied separately; lifting equipment and compressed air are customer interfaces. Tooling mass, imbalance and permitted speed are confirmed together.
Configured Centrifugal Tooling
Station load, tooling balance and permitted rotational speed are agreed for the actual liner geometry.
Extended Dispensing Boom
The supplied 2.2 m reach is a positioning envelope; filling trajectories are developed for the tool.
High-Volume Metering
The supplied output range is 4–25 kg/min. The filling window must also match part mass and formulation gel time.
Material-Specific Heating
Feed and mold heating are selected for the chosen prepolymer and curative system.


