
Carbon Fiber Body-in-White HP-RTM Solution
HP-RTM systems for selected carbon-fiber automotive structures, with resin delivery, vacuum tooling and thermal control matched to the part design. Structural performance is established through component and vehicle qualification.
Precision HP-RTM Solutions for Automotive Carbon Fiber Structures
HP-RTM equipment meters, mixes and delivers fast-reacting polyurethane or epoxy resin into closed tooling containing a carbon-fiber preform. Filling and cure depend on the resin processing window, fiber architecture, gate layout, vacuum and thermal recipe. The related B-pillar project reports 60% lower component weight than its conventional ultra-high-strength steel baseline and a 3-minute complete molding/demolding cycle. These results do not establish a 60% reduction in total body-in-white weight, universal aerospace-grade strength or vehicle crashworthiness. Void content, laminate quality, dimensions and cure are inspected separately; structural and crash performance follow the component and vehicle validation program.
Reference B-Pillar: 60% Lower Weight
The related project compares its carbon-fiber B-pillar component with conventional ultra-high-strength steel assemblies. This is a component/design result; stiffness, crash behavior and total vehicle mass require separate assessment.
Controlled Preform Filling
Coordinate vacuum, injection profile and thermal recipes for the supplied 50%–60% fiber-volume reference. The stated injection-system limit up to 150 bar is distinct from cavity loading; internal defects and void content require inspection.
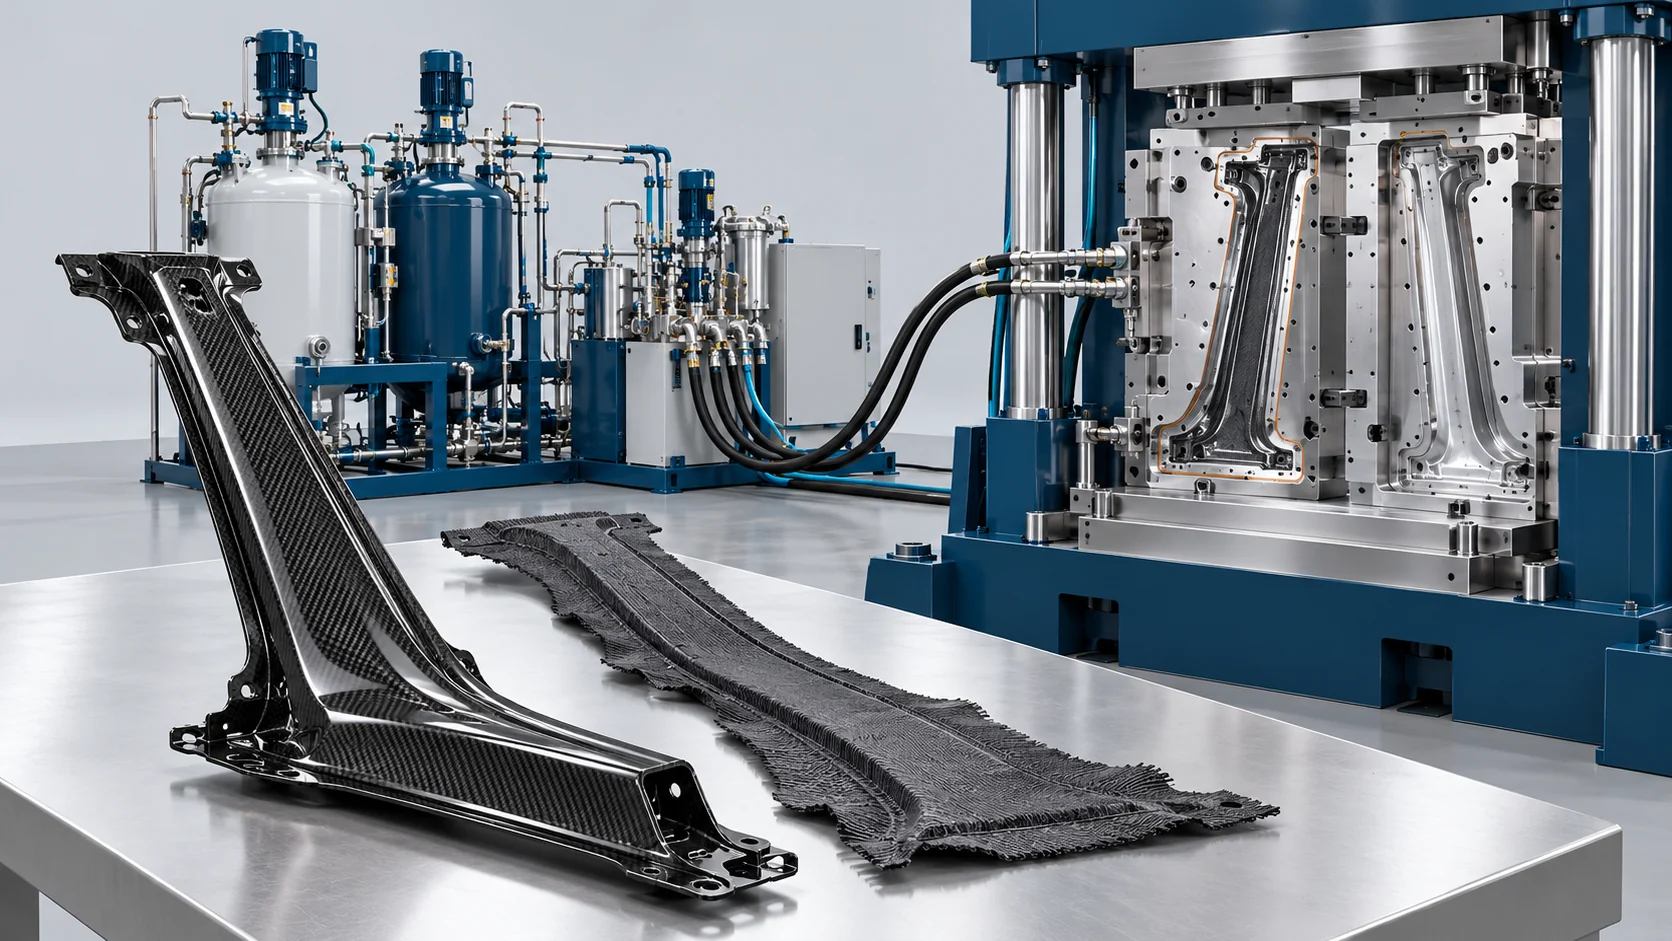
Haifeng delivers complete HP-RTM processing architectures—from high-pressure dual-component metering units and dynamic vacuum controllers to optional hydraulic presses—empowering Tier-1 composite suppliers to achieve automotive-grade mass production.Concept illustration — not a photograph of delivered equipment or a customer installation.
Turnkey Carbon Fiber HP-RTM Manufacturing Workflow
A reference workflow from preform loading through injection, cure and demolding. The 180–300-second complete molding window is not injection time or a universal cure-only duration.
Preform Loading & Vacuum
Dry carbon fiber preforms are seated into the heated steel tool; the mold clamps and deep vacuum is drawn to purge trapped air
High-Pressure Resin Injection
The HP-RTM metering unit injects mixed resin at up to 150 bar, driving fast, uniform penetration into the dense carbon preform
Rapid Polymerization
Tool-temperature control supports resin-specific cure and demold readiness. The stated 3-minute project reference is the complete molding/demolding cycle; cure-only duration is established for the selected resin, thickness and tooling.
Engineering Specifications & Production Capacity
Technical parameters for this Haifeng HP-RTM production system.
| Technical Parameter | Standard Specification / Value | Engineering Context & Verification |
|---|---|---|
| Target Application | Carbon Fiber B-Pillars, Roof Crossmembers, Floor Beams | Body-in-white structural crash management |
| Material Matrix | Fast-Curing Polyurethane or Epoxy Resin + Carbon Fiber | Material/laminate reference; structural properties and crash behavior require component and vehicle qualification |
| Injection Pressure | 30 – 150 bar (Customizable) | Extreme pressure penetration for dense preforms |
| Fiber Volume Fraction (FVF) | 50% – 60% | High-density continuous fiber reinforcement |
| Stoichiometric Accuracy | ±0.5% | Servo closed-loop dynamic Ratio Lock |
| Demolding Cycle Time | 180 – 300 seconds (Standard 3 min) | Complete molding reference including press movements, filling, cure and demolding; not injection or cure-only time |
| Mold Temperature Window | 90°C – 130°C | Multi-circuit dynamic oil/water TCU regulation |
| Scope of Supply | Turnkey (HP-RTM Skid, TCU, Vacuum Unit + Optional Press) | Complete workcell delivery or press retrofit |
HP-RTM Equipment for This Application
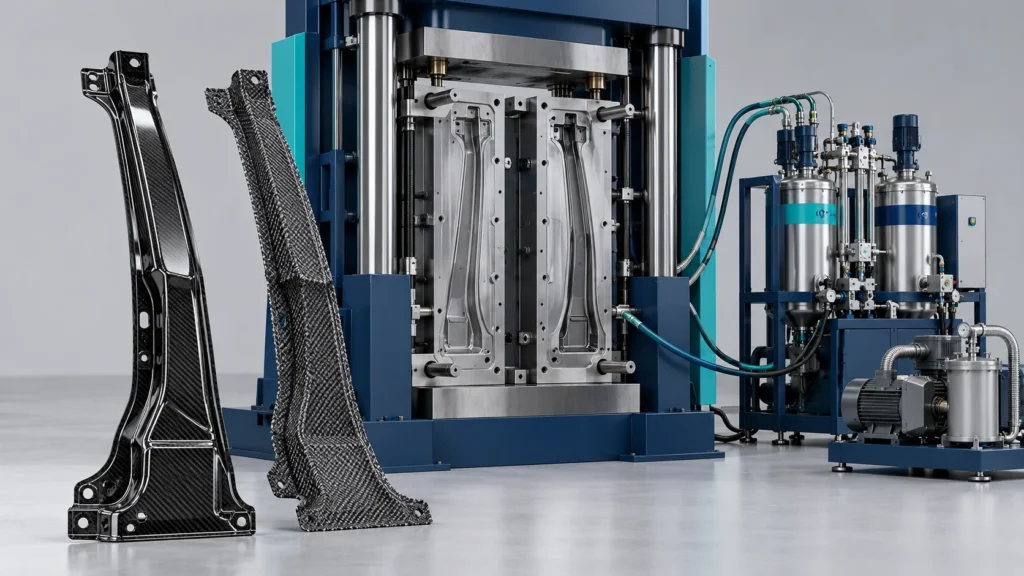
An application configuration for repeatable filling of structural carbon-fiber preforms.
Key Engineering Advantages
Why leading automotive composite builders select Haifeng HP-RTM equipment.
Reference B-Pillar Weight Comparison
The related project reports 60% lower B-pillar component weight than its conventional steel baseline. This is not a reduction of total body-in-white or vehicle weight.
Controlled Impregnation and Inspection
Vacuum and resin delivery support filling for the specified preform. Gate layout, viscosity and reaction time are coordinated; dry spots and void content require inspection.
Reference Complete Molding Window
The application lists 180–300 seconds, with 3 minutes reported in the related project. This includes the complete molding/demolding sequence rather than injection time alone.
Structural Qualification Planning
Crash response depends on geometry, laminate, cure quality and joining. Component and vehicle tests establish structural behavior; the injection unit does not guarantee it.
Proven Manufacturing Project
See how an EV structural composite manufacturer deployed Haifeng's HP-RTM system to produce lightweight carbon fiber B-pillars.
Frequently Asked Questions
Engineering and purchasing questions about this HP-RTM production route.
How does HP-RTM differ from traditional low-pressure RTM?
Can Haifeng's HP-RTM system process both polyurethane and epoxy resins?
Can this HP-RTM equipment integrate with our existing high-tonnage press?
Does Haifeng provide complete turnkey lines including presses and tooling?
What is the typical installation and commissioning timeline on-site?
Discuss Your HP-RTM Production Project
Share your component, material and production targets for a tailored solution.


