
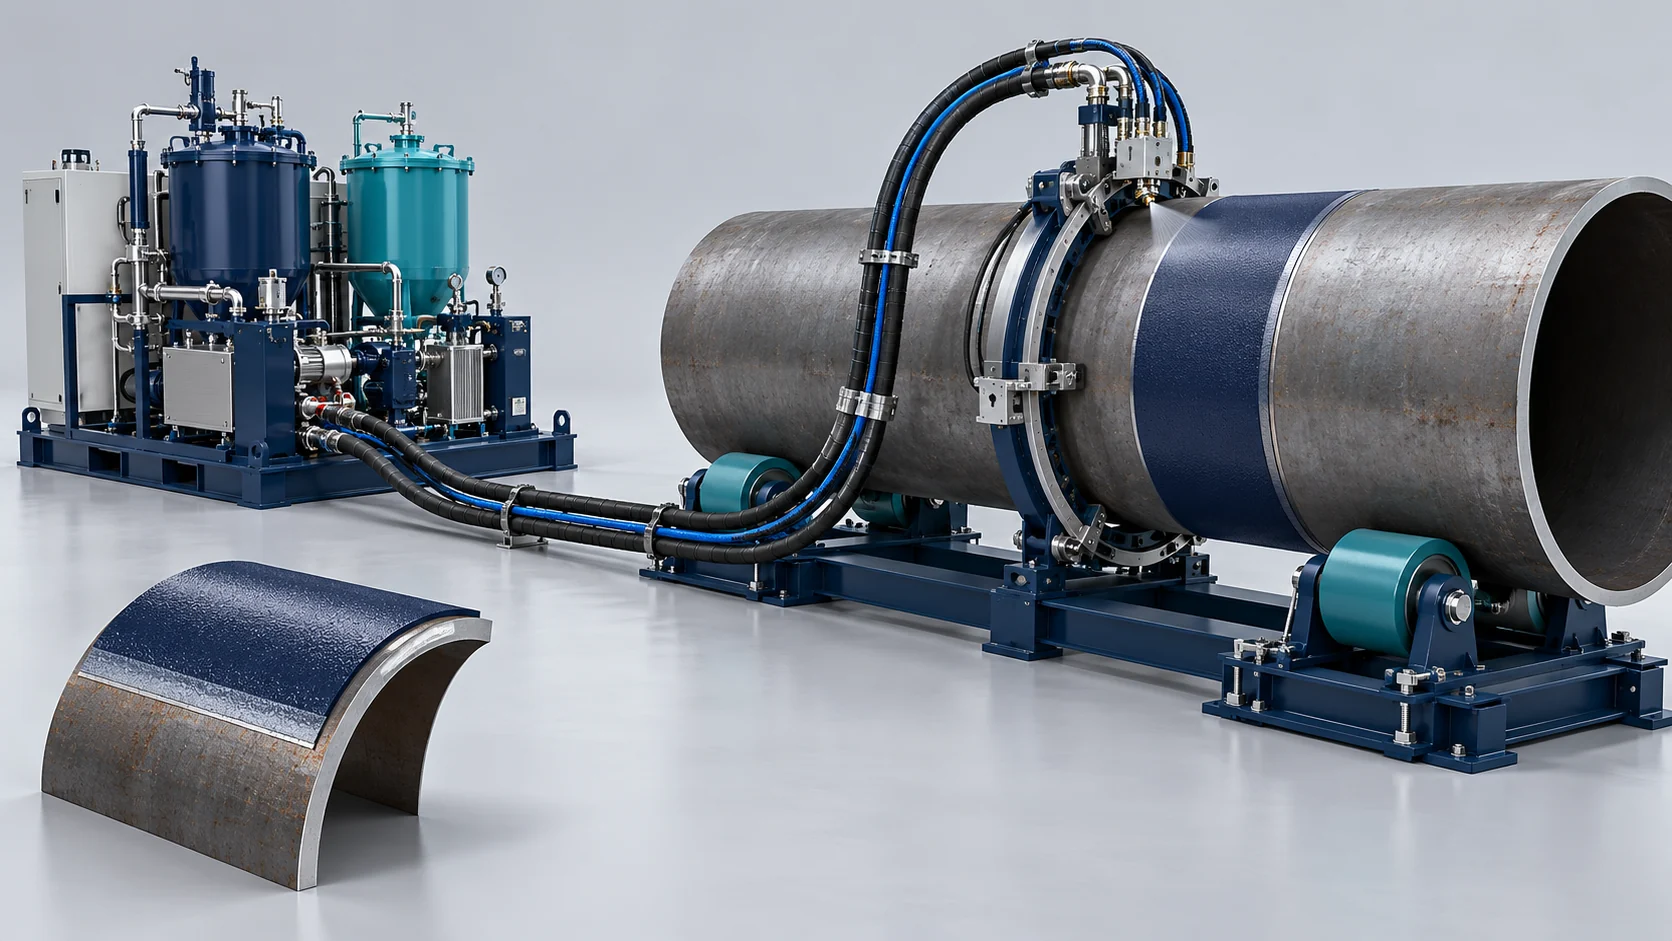
Buried Pipeline Polyurea Coating Solution
Hydraulic-driven two-component spraying with heated delivery hoses and configured rotary/orbital interfaces for pipeline external and field-joint coating.
Impermeable Dielectric Barriers for High-Pressure Energy Pipelines
Hydraulic-driven two-component spraying with heated delivery hoses and configured rotary/orbital interfaces for pipeline external and field-joint coating. The package covers hydraulic-driven proportioning, specified heated hoses, mechanical-cleanout guns, the agreed pipe rotation or orbital carriage and controls. Induction heating and mobile generation are optional. Coating and primer come from the selected material supplier; blasting and lifting are customer interfaces. This spray route does not constitute a complete three-layer polyethylene extrusion coating line.
Hydraulic-Driven Proportioning
The specified proportioning arrangement is calibrated for the stated volumetric recipe and operating window.
Heated Delivery Interfaces
Hose length, pressure loss and material temperature are verified together under the selected ambient conditions.
Select the equipment, coating build-up and inspection plan against the substrate, part geometry, production target and site conditions. Material qualification and reported outcomes require project-specific records.
End-to-End Pipeline Outer-Wall Coating Workflow
A configured sequence of substrate preparation, material conditioning, application, cure and inspection for the selected coating system.
Abrasive Blasting & Medium-Frequency Preheating
The steel pipe surface is blasted to Sa 2.5 cleanliness (profile 60–80 µm) and heated to 50–65°C via induction coils to activate chemical bonding.
Moisture-Barrier Epoxy Primer Application
Apply the selected primer to the prepared substrate within its specified film-build and recoat window. Adhesion and outgassing performance require confirmation for the actual substrate and coating system.
High-Pressure Hydraulic Heating & Metering
Polyurea components A and B are pressurized to 18–21 MPa via coaxial hydraulic cylinders and heated to 65°C through 120-meter copper-mesh umbilical hoses.
Reference Solution Engineering Envelope
Supplied configuration and coating-system references. Values depend on the stated material, substrate, test and operating conditions; original records are not attached.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Pipeline Outer Diameter Range | Ø 400 mm to Ø 1,420 mm | Motorized pipe roller carriage or orbital ring |
| Fluid Working Pressure | 16.0 to 21.0 MPa | Continuous double-acting hydraulic proportioner |
| Continuous Spray Output | 3.0 to 14.0 kg/min | Dual-gun high-velocity impingement setup |
| Maximum Heated Hose Length | Up to 120 meters | Copper-mesh jacketed all-weather umbilical cable |
| Cathodic Disbondment Radius | Less than 4.2 mm | Tested at 65°C for 48 hours under ASTM G8; supplied material/test result requires original specimen, method and report |
| Holiday Inspection | Method and voltage confirmed for coating thickness | Holiday-test voltage does not establish dielectric breakdown strength per millimeter; original material test required |
Core Equipment for This Solution
The package covers hydraulic-driven proportioning, specified heated hoses, mechanical-cleanout guns, the agreed pipe rotation or orbital carriage and controls. Induction heating and mobile generation are optional. Coating and primer come from the selected material supplier; blasting and lifting are customer interfaces. This spray route does not constitute a complete three-layer polyethylene extrusion coating line.
Core Advantages of Haifeng Pipeline Solutions
Configured process mechanisms and project interfaces for the selected equipment package.
Hydraulic-Driven Proportioning
The specified proportioning arrangement is calibrated for the stated volumetric recipe and operating window.
Heated Delivery Interfaces
Hose length, pressure loss and material temperature are verified together under the selected ambient conditions.
Configured Pipe Traversal
Rotary or orbital movement is selected for the pipe and joint geometry; coating build is verified by inspection.
Coating Inspection Interfaces
Holiday inspection settings and adhesion tests are established for the actual coating build-up and agreed method.
Related Project Draft
Review the project configuration described in the supplied brief. Project records and reported results require verification before public use.
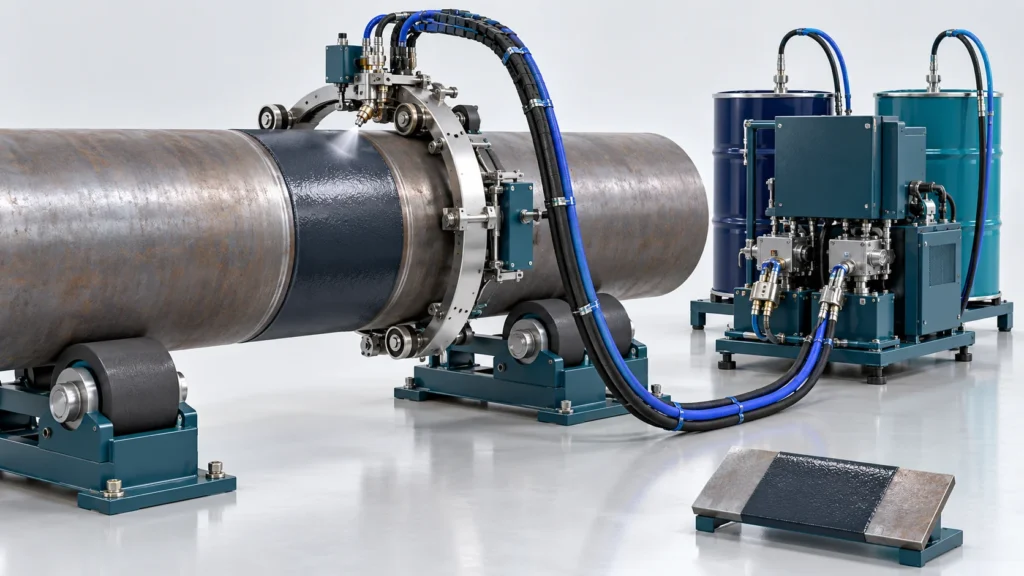
Frequently Asked Questions
Find answers about Buried Pipeline Polyurea Coating Solution, including material selection, equipment configuration and the information needed to plan a production line.
How does this spraying route relate to existing 3PE pipe coatings?
How are long heated hoses configured?
How are surface preparation and inspection settings selected?
Does an external coating package also cover internal spraying?
Request a Pipeline Coating Equipment Proposal
Share the substrate or finished part, selected materials, coating and quality requirements, target output, automation needs and factory or worksite conditions.


