
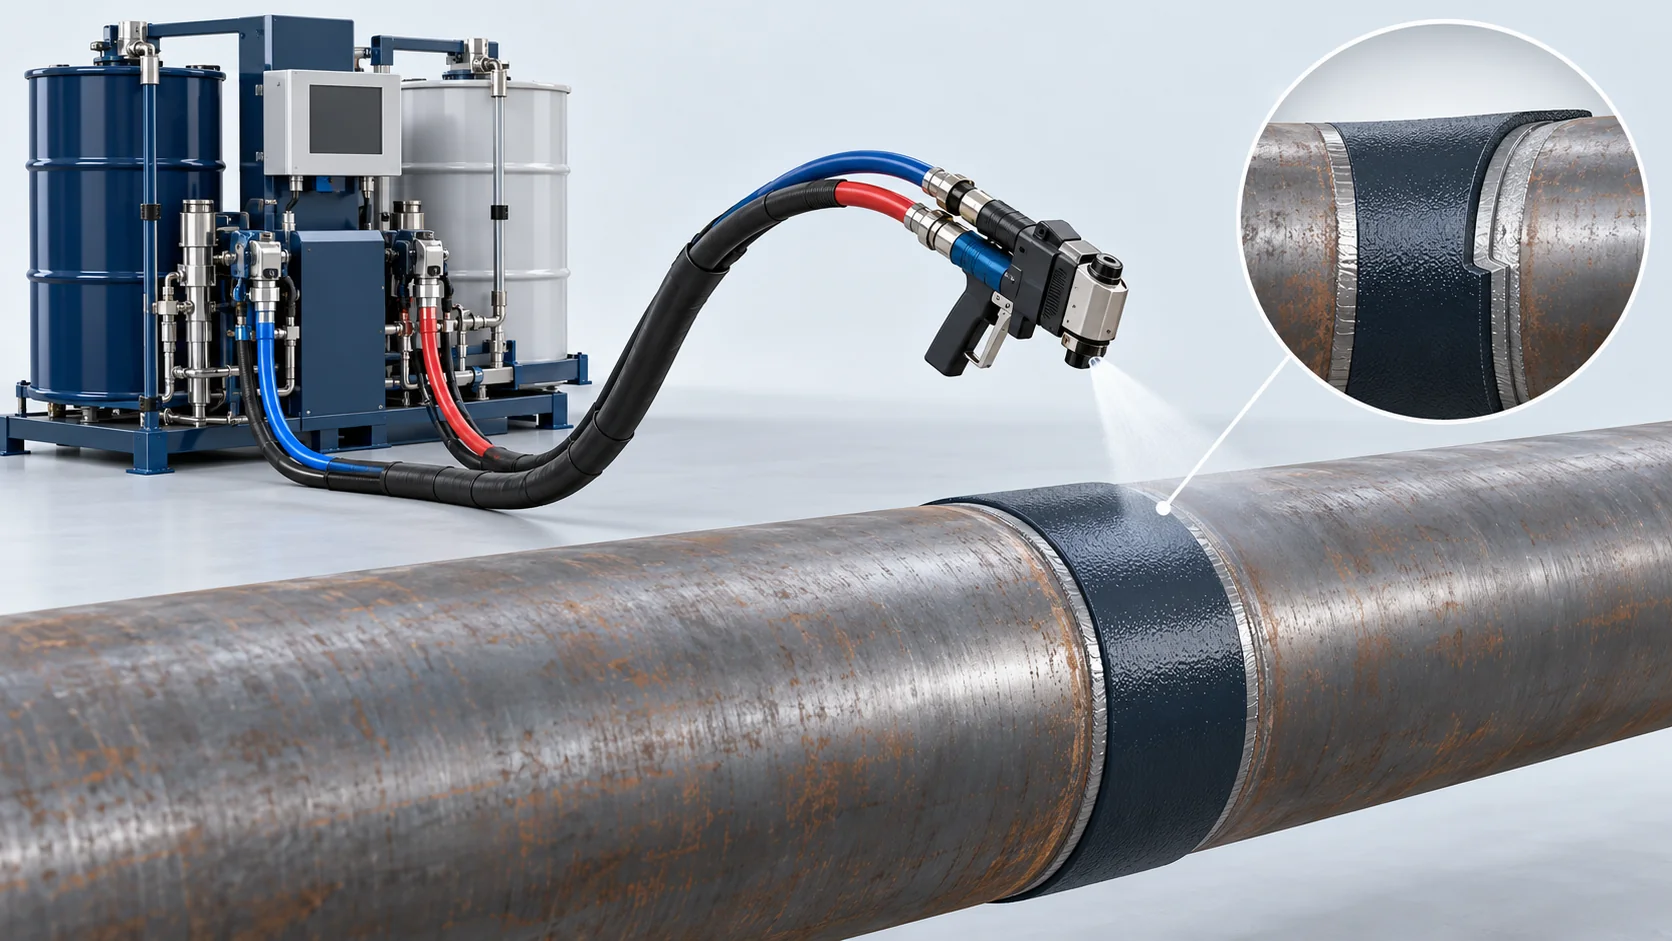
Polyurea Spray Machine | Pipeline and Field-Joint Coating
Hydraulic-driven two-component spraying with heated delivery hoses and configured rotary/orbital interfaces for pipeline external and field-joint coating.
Precision Helical Polyurea Application for Heavy-Duty Pipelines
Hydraulic-driven two-component spraying with heated delivery hoses and configured rotary/orbital interfaces for pipeline external and field-joint coating.
Hydraulic-driven two-component spraying with heated delivery hoses and configured rotary/orbital interfaces for pipeline external and field-joint coating.
The package covers hydraulic-driven proportioning, specified heated hoses, mechanical-cleanout guns, the agreed pipe rotation or orbital carriage and controls. Induction heating and mobile generation are optional. Coating and primer come from the selected material supplier; blasting and lifting are customer interfaces. This spray route does not constitute a complete three-layer polyethylene extrusion coating line.
Material Flow and Working Principle
Induction Heating & Substrate Pre-Conditioning
The bare steel pipe (grit-blasted to Sa 2.5) rotates through a medium-frequency induction heater, elevating steel temperatures to 50–65°C to accelerate chemical bonding and drive off microscopic surface moisture.
Hydraulic Pulse-Free Metering
A mechanically linked dual-acting hydraulic proportioner draws isocyanate and polyamine streams from 200 L drums, displacing both fluids at a 1:1 volumetric ratio up to 21 MPa without pressure drops during stroke transitions.
Long-Distance Thermal Delivery
Fluid passes through inline cast-aluminum primary heaters and a 120-meter copper-mesh wrapped heated umbilical cable, maintaining material temperatures at 65°C ± 1°C directly to the gun manifold.
Automated Helical Impingement Spraying
High-pressure fluid streams impinge inside multiple mechanical-purge guns mounted on a servo tracking ring, depositing a seamless, fan-shaped liquid polyurea layer as the pipe advances helically.
Online NDT Spark Testing & Cooling
The specified online ndt spark testing & cooling stage is configured for the selected material, substrate and operating window. Settings and resulting coating quality require the agreed process and original inspection records.
Model and Technical Parameters
Configuration references from the supplied HF-PIPE1400-HYD brief. Pressure circuit designation, output, heating and hose capability require confirmation under the stated operating conditions. Coating properties and laboratory qualification belong to the selected material/substrate system and require original reports.
| Technical Parameter | HF-PIPE1400-HYD |
|---|---|
| Components | 2 Components (1:1 Fixed Volumetric Ratio) |
| Output Range (g/s) | 3.0 to 14.0 kg/min (Continuous spray output) |
| Mixing Ratio Range | 1:1 Fixed (Volumetric ratio) |
| Ratio Accuracy | ±0.5% (Under steady working pressure differential < 1.0 MPa) |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 440V/480V 60Hz optional) |
| Working Pressure | 16.0 to 21.0 MPa (Hydraulic fluid lines); circuit designation to be confirmed |
| Tank Capacity (L) | Direct 200 L drum feed (Optional 60 L day tanks) |
| Weight | 1,850 kg (Proportioner skid and carriage frame) |
| Dimensions (L×W×H) | 3200 mm x 1600 mm x 1850 mm |
| Pipe Diameter Range | Ø 400 mm to Ø 1,420 mm (OD); Automated pipe roller carriage |
| Heated Hose Length | Up to 120 meters (Copper-mesh wrapped); Ambient -15°C testing condition |
| Heating Core Power | 18 kW (9 kW per individual component); Inline fluid heating blocks |
| Coating Thickness Profile | 1.5 to 2.0 mm (Adjustable traverse speed); Single-pass helical winding |
Key Equipment Features
The package covers hydraulic-driven proportioning, specified heated hoses, mechanical-cleanout guns, the agreed pipe rotation or orbital carriage and controls. Induction heating and mobile generation are optional. Coating and primer come from the selected material supplier; blasting and lifting are customer interfaces. This spray route does not constitute a complete three-layer polyethylene extrusion coating line.
Hydraulic-Driven Proportioning
The specified proportioning arrangement is calibrated for the stated volumetric recipe and operating window.
Heated Delivery Interfaces
Hose length, pressure loss and material temperature are verified together under the selected ambient conditions.
Configured Pipe Traversal
Rotary or orbital movement is selected for the pipe and joint geometry; coating build is verified by inspection.
Coating Inspection Interfaces
Holiday inspection settings and adhesion tests are established for the actual coating build-up and agreed method.


