
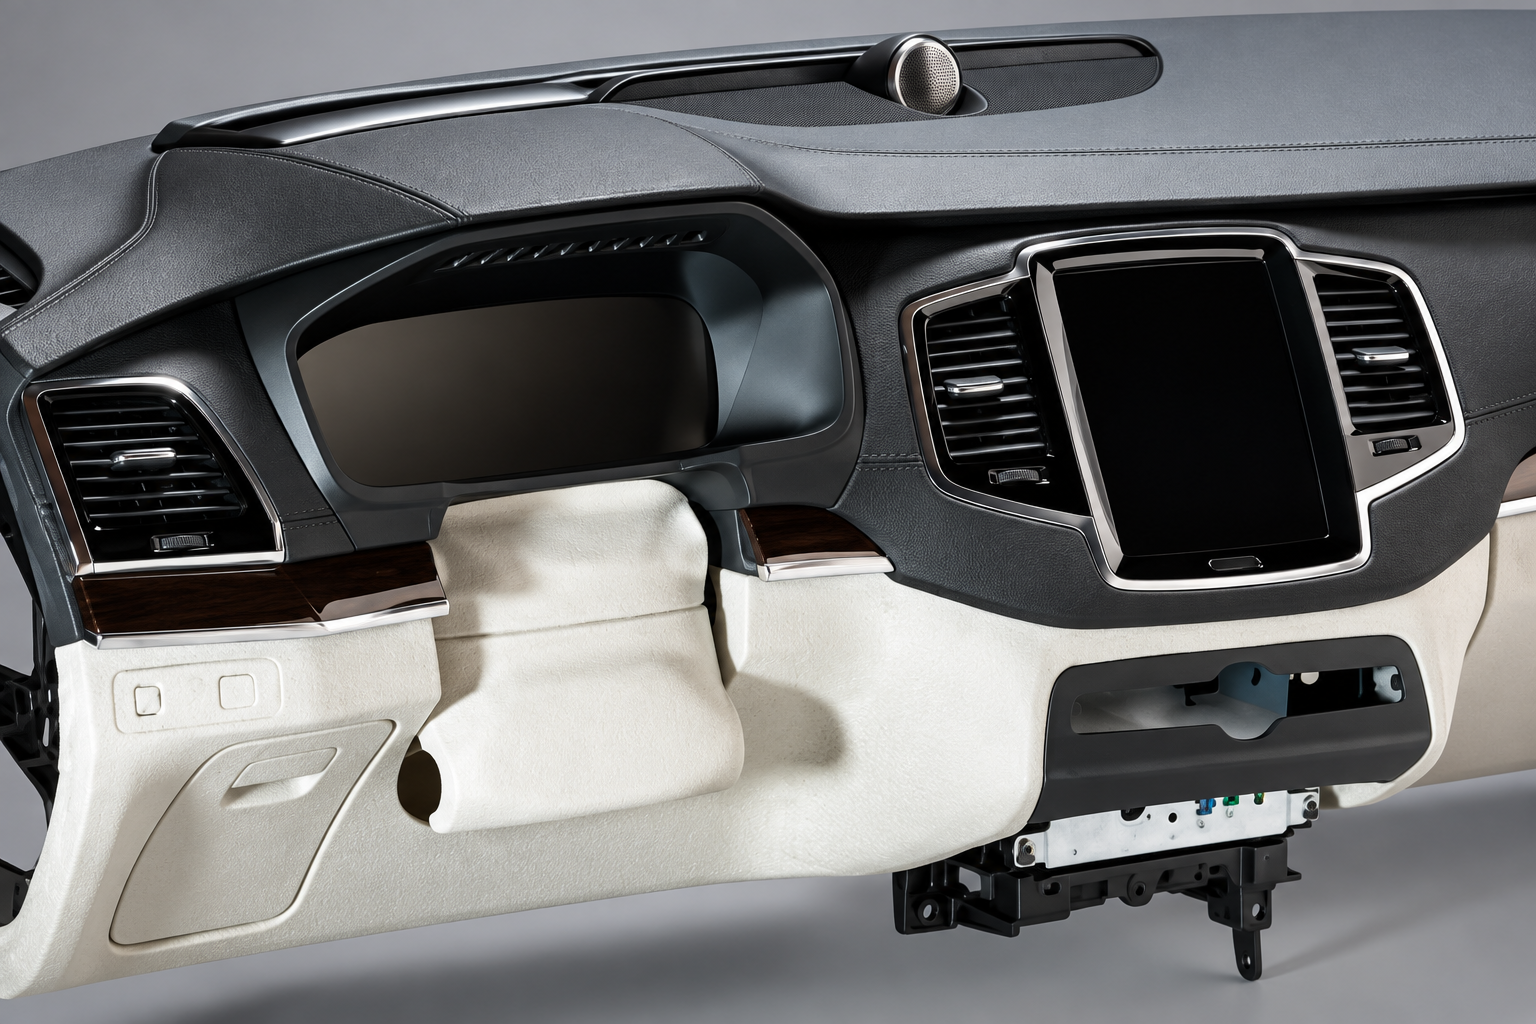
Automotive Dashboard PU Backfoaming Solution
Precision high-pressure polyurethane backfoaming systems for automotive cockpits, delivering flawless narrow-gap filling and certified passenger airbag tear safety.
Precision Polyurethane Backfoaming Solutions for Automotive Dashboards
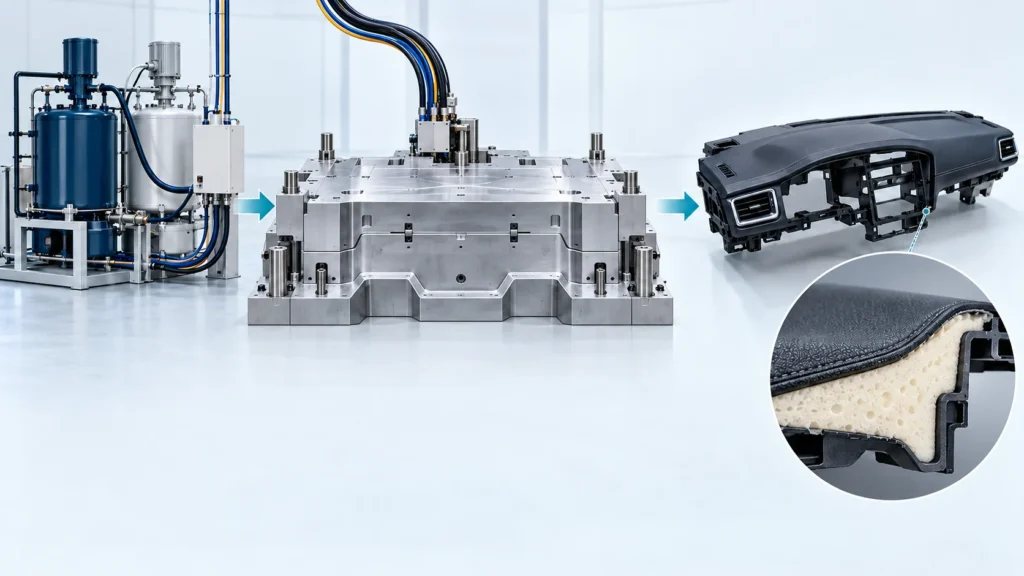
Premium automotive instrument panels feature a three-layer architecture: a rigid structural skeleton, a soft intermediate polyurethane foam cushion, and a luxurious outer skin (PVC, TPO, or PU film). Filling the extremely narrow interspace (frequently under 5mm) across broad 1.5-meter dashboard spans presents extreme rheological challenges. Trapped air pockets cause skin blistering, while inconsistent foam density across the invisible Passenger Airbag (PAB) tear seam risks delayed deployment or lethal fragmentation during collisions. Haifeng’s high-pressure polyurethane backfoaming solution combines laminar impingement dispensing with dynamic mold tilting, delivering bubble-free narrow-gap penetration and certified passenger airbag deployment safety across extreme temperatures (-40°C to +85°C).
Void-Free <5mm Narrow-Gap Filling
Closed-loop stoichiometric metering and low-viscosity impingement mixing deliver smooth laminar cavity filling across broad 1.5m spans, eliminating skin sink marks and voids.
Certified Passenger Airbag Tear Safety
Strict density and thermal exotherm control ensure the polyurethane foam tears cleanly along the laser-weakened scoreline without brittle fragments across -40°C to +85°C.
Haifeng delivers complete dashboard processing equipment—from precision closed-loop metering skids to multi-axis tilting clamping presses—guaranteeing high-yield cockpit manufacturing for automotive Tier-1 suppliers.
Automotive Dashboard Backfoaming Workflow
A synchronized four-stage workflow delivering high-yield, air-free cockpit dashboard assemblies.
Precursor Thermal Preparation
Dual-circuit TCU units stabilize polyol and isocyanate within ±0.5°C to lock in flow front kinetics
Component Loading & Tilting Clamping
The skin and skeleton are seated in the heated mold; the fixture closes and tilts to optimal venting angles
Low-Pressure High-Velocity Dispensing
The high-pressure mixing head injects liquid foam into the narrow cavity; low cavity pressure flows the resin evenly without washing out skin grains
Engineering Specifications & Technical Parameters
Technical parameters for this Haifeng automotive production system.
| Technical Parameter | Standard Specification / Value | Engineering Context & Verification |
|---|---|---|
| Target Application | Instrument Panels, Cockpit Consoles, Glove Boxes | Premium soft-touch interior assemblies |
| Material Matrix | Semi-Rigid Microcellular Polyurethane Foam | Fast-curing cockpit safety foam |
| Narrow-Gap Filling Capability | Down to <5.0 mm | Verified on full-span dashboard boundaries |
| Core Density Range | 120 – 180 kg/m³ | Optimized for soft touch and structural support |
| Metering Output Capacity | 20 – 60 kg/min (Customizable) | Servo axial piston pumps with Ratio Lock |
| Demolding Cycle Time | 60 – 90 seconds (Standard 70 s) | High-throughput cockpit production |
| Airbag Deployment Rating | 100% Pass (-40°C to +85°C) | Validated on high-speed dynamic deployment rigs |
| Scope of Supply | Turnkey (Backfoaming Skid, TCU, Master PLC + Tilting Clamp) | Complete workcell or press retrofit |
Electric Mold Carrier and Metering Configuration
The following reference package supplements this dashboard backfoaming solution. It combines high-pressure metering with an optional electric mold carrier, mold identification, stored movement recipes and material-supply interfaces. These values describe one configuration and are separate from broader machine-family or part-performance values above.
| Parameter | Reference configuration | Selection notes |
|---|---|---|
| Reference metering output | 80–320 g/s at POL:ISO = 2:1 | Configuration-specific reference; does not replace every machine-family output range |
| Reference injection pressure | 10–20 MPa adjustable | Distinct from tank pressure and hydraulic protection settings |
| Example head duties | 250–320 g/s closed-mold; 80–150 g/s open-pour | Head count and final head arrangement require the approved configuration |
| Material temperature control | ±2°C stated deviation | Confirm setpoint with the selected formulation |
| Mold platen size | 2,000 × 1,000 mm | Tooling interfaces from the instrument-panel mold drawing |
| Maximum mold envelope | 2,000 × 1,000 × 750 mm | Width × depth × height reference |
| Platen loading | 1,500 kg upper and 1,500 kg lower | Verify individual tool weights and mounting |
| Upper-platen lift | 800 mm | Check tooling clearance and material-loading access |
| Tilting movement | Upper: 80°; lower: 45°, toward the operator | Angles refer to this electric carrier configuration |
| Clamping capacity | Specified ≥60 t | Confirm tooling load and project acceptance basis |
| Carrier motion timing | Parallel closing ≤5 s; complete carrier open/close sequence ≤8 s | Motion timing is not the foam-curing or demolding cycle |
| Carrier control | Siemens S7-1500 PLC; mold recognition and stored motion recipes | PROFIBUS communication is described for the carrier interface |
| Per-station mold temperature unit | 9 kW; water circulation at least 90 L/min; stated upper control temperature 95°C | Final mold-temperature setpoint agreed for material and tooling |
| Utility reference | 380 V, 50 Hz; 50 kVA cabinet supply; dry oil-free air 0.6–0.8 MPa, 1,000 NL/min | Review final electrical and pneumatic load schedule |
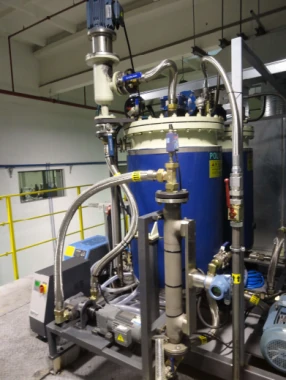
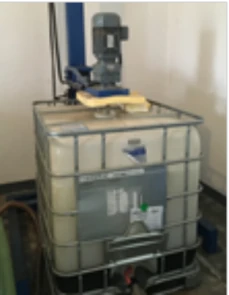
Material supply can include IBC polyol stirring, automatic diaphragm-pump refill and separately specified polyol nucleation. Tank capacities and the final color/head arrangement are defined in the approved equipment schedule.
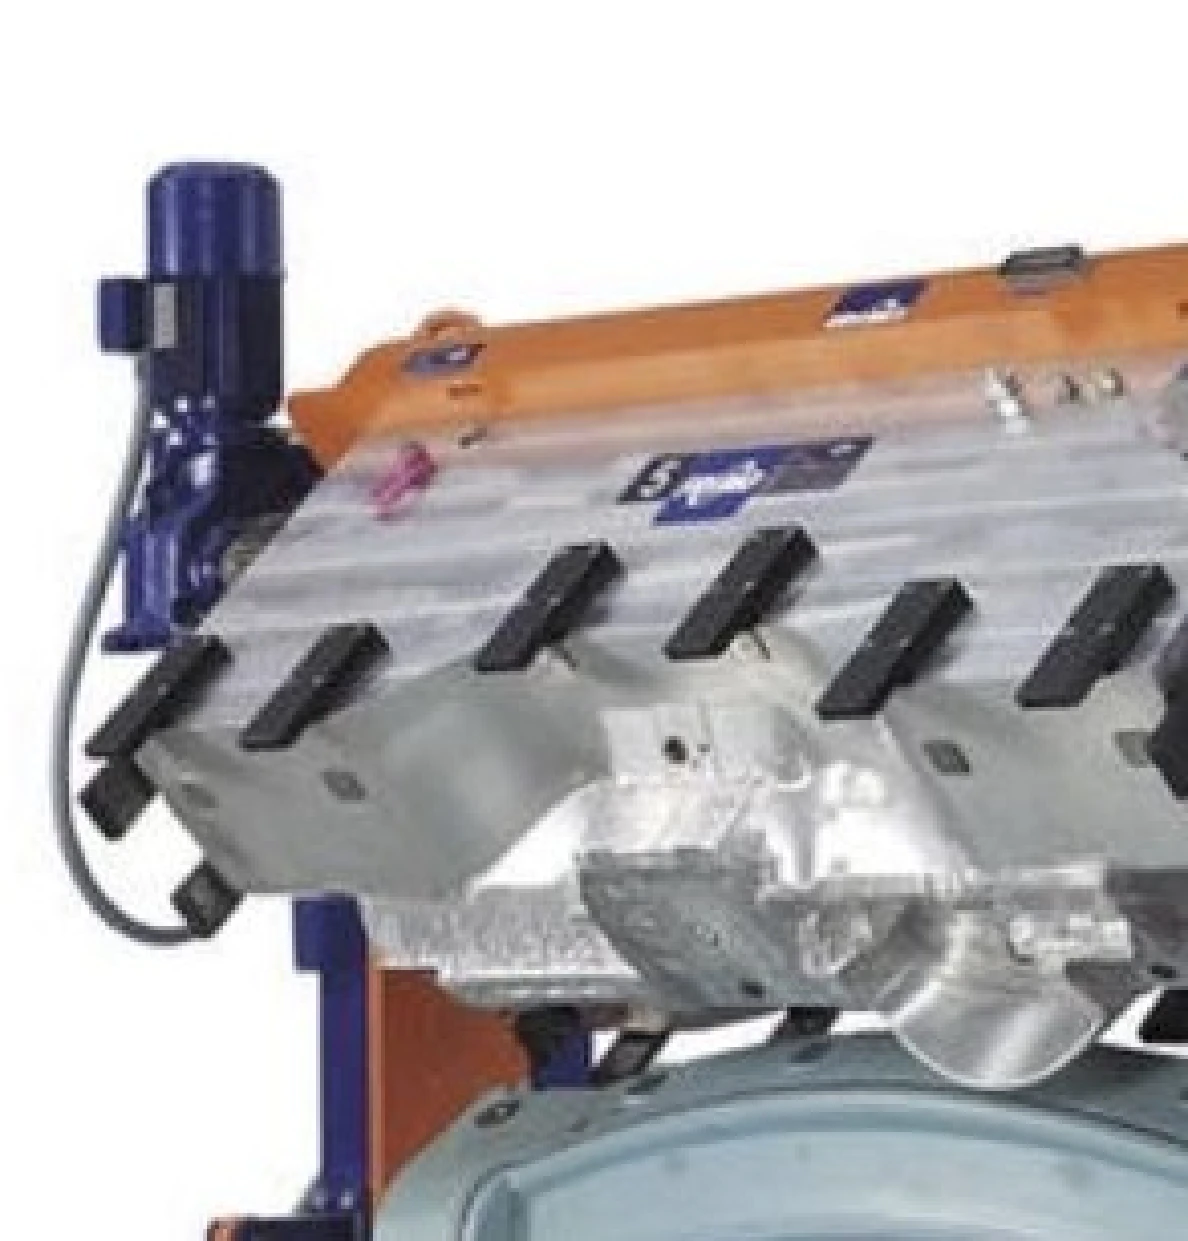
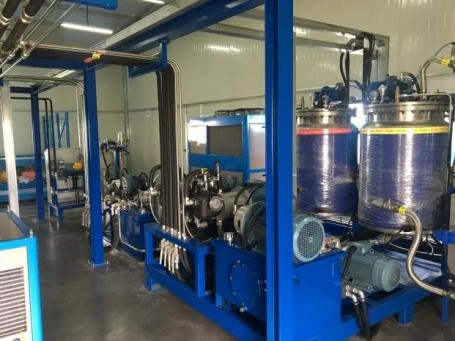
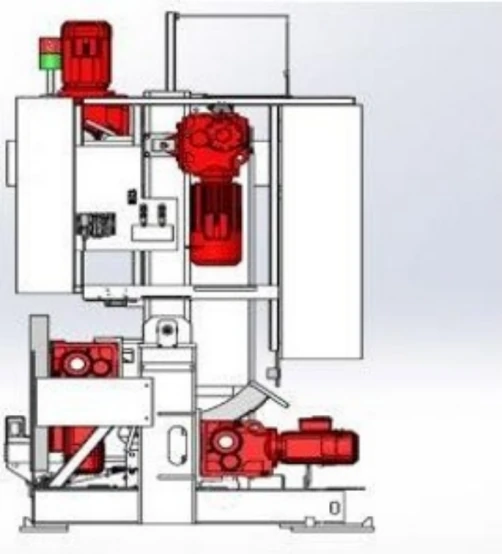
Dashboard Workcell — Technical Reference Illustrations
Equipment illustrations show the relevant process sections and configuration references.
Key Engineering Advantages
For Automotive Dashboard PU Backfoaming Line, assess material compatibility, process control, equipment interfaces and changeover needs against your production brief.
Bubble-Free <5mm Narrow-Gap Penetration
Smooth laminar fluid flow fills tight edges without entrapping air or distorting skin textures.
100% PAB Airbag Deployment Safety
Clean tear propagation along laser weakness lines without loose fragment dispersion.
Rapid 70s Demolding Cadence
Rapid curing kinetics maximize manufacturing output per mold carrier.
Strict Low-VOC Compliance
Fulfills VDA 278 mandates, eliminating passenger cabin odor and windshield fogging.
Related Automotive Project
See the production line delivery and measured project outcomes.
Frequently Asked Questions
Engineering and purchasing questions about this polyurethane production route.
How does Haifeng prevent voids in <5mm dashboard cavities?
How is airbag safety verified?
What is the typical installation timeline?
Is the electric mold carrier mandatory?
Does the 8-second carrier sequence equal the finished-part demolding cycle?
How are different mold programs managed?
Discuss Your Automotive Production Project
Share the part, material and target capacity for a tailored solution.
Relevant Haifeng Equipment
Equipment is shortlisted by the part, material system and process trials. An optional electric mold carrier and reference high-pressure metering package are detailed in the technical supplement.


