
PU Injection Pultrusion Machine | Composite Solar Frames
Continuous closed-die injection pultrusion with line-synchronized metering and separate injection-box pressure control.
Closed-Die High-Pressure Resin Injection for Solar Frames
Continuous closed-die injection pultrusion with line-synchronized metering and separate injection-box pressure control.
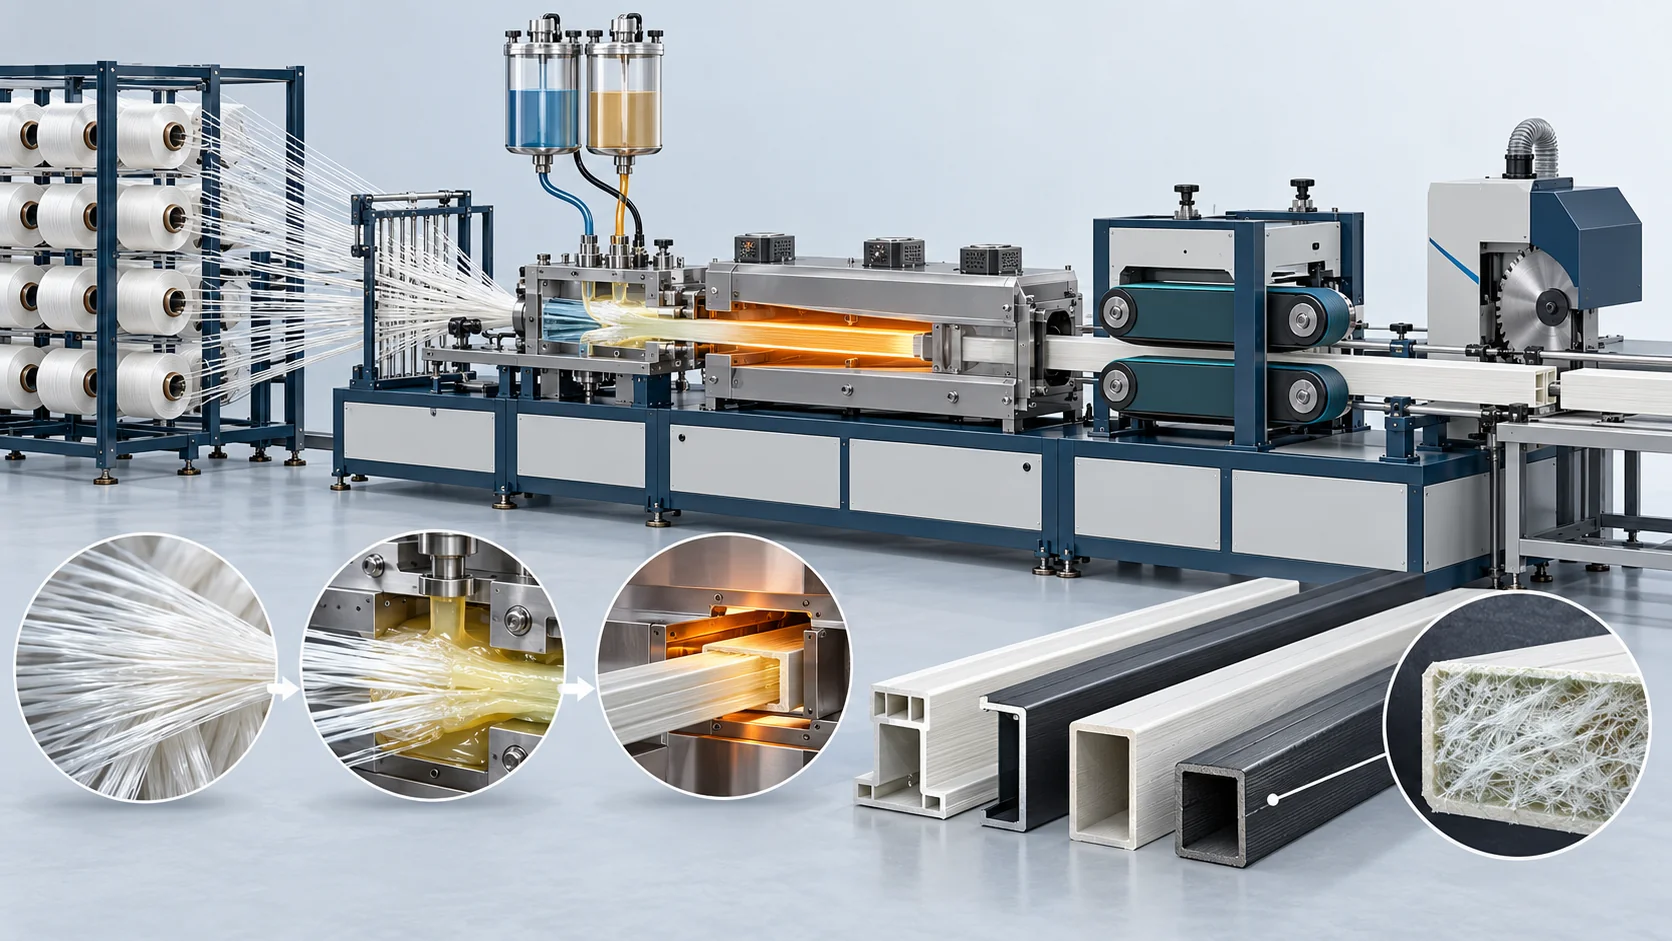
The HF-PVI-40H is an industrial high-pressure resin proportioning and direct injection system developed specifically for continuous polyurethane composite photovoltaic (PV) frame manufacturing. Replacing outdated open-bath resin impregnation methods, this system injects fast-reacting polyurethane resin directly into a sealed injection die under high hydraulic pressure, supporting controlled impregnation for the supplied high-fiber-volume reference; fiber fraction and wet-out are measured for the selected profile.
Equipped with high-precision axial piston metering pumps and dynamic mass flow tracking, the HF-PVI-40H controls the specified stoichiometric ratio even when line pulling speeds fluctuate. Its high-pressure impingement mixing head mounts directly to the pultrusion die face, ensuring rapid, homogeneous chemical homogenization without mechanical shear blades or solvent flushing, supporting closed-die profile production; internal voids, insulation and mechanical properties require defined material and profile tests.
Material Flow and Working Principle
Sealed Conditioning & Degassing
Polyol and isocyanate resins are conditioned in sealed, nitrogen-blanketed stainless steel tanks with continuous recirculating temperature control to prevent moisture absorption and viscosity variation.
Synchronized Ratio-Lock Metering
Independent servo-driven high-pressure axial piston pumps feed components through steel-reinforced lines, while high-frequency flow sensors monitor throughput and automatically correct displacements within ±0.3%.
High-Pressure Impingement Direct Injection
The component streams impinge within the compact mixing head at 10 to 15 MPa, achieving instantaneous molecular mixing, and discharge straight into the sealed injection box of the pultrusion die.
Dense Fiber Wet-Out & Rapid Curing
The reactive polyurethane saturates dense fiberglass bundles under die cavity pressure, then cures within the multi-zone heated pultrusion die before emerging as a fully polymerized structural profile.
Model and Technical Parameters
Supplied HF-PVI-40H configuration for continuous closed-die injection pultrusion. The stated 10–15 MPa refers to the metering/mixing circuit; injection-box pressure is separately controlled. Final process settings depend on resin, fiber architecture and tooling.
| Technical Parameter | HF-PVI-40H |
|---|---|
| Components | 2 Components (A: Polyol resin, B: Polymeric MDI) |
| Output Range (g/s) | 0.8 to 8.0 kg/min (Continuous adjustable) |
| Mixing Ratio Range | 100:90 to 100:130 (By weight) |
| Ratio Accuracy | ±0.3% (Dynamic speed-slaved calibration) |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 480V 60Hz optional) |
| Working Pressure | 10.0 to 15.0 MPa (High-pressure delivery and impingement) |
| Tank Capacity (L) | Tank A: 150 L, Tank B: 150 L (Stainless steel 304) |
| Weight | 1,450 kg (Base machine skid) |
| Dimensions (L×W×H) | 2200 mm x 1500 mm x 1950 mm |
| Pultrusion Line Speed Tracking | 0.2 to 2.0 m/min (Line-speed slaved); Continuous automatic sync |
| Die Cavity Injection Pressure | 0.5 to 2.5 MPa (Inside injection box); Sealed die running condition |
| Fluid Heating Temperature | 25°C to 60°C (Circulating thermal loop); Tanks and high-pressure hoses |
| Total Installed Power | 22 kW (Including drive and heating); Maximum operating load |
Key Equipment Features
The package covers high-pressure metering and mixing, a closed injection box, line-synchronized feed control and controls for continuous pultrusion. Pulling, cutting and heating equipment are optional interfaces. Resin, fibers, nitrogen and site utilities are agreed external interfaces. This continuous route is distinct from the existing matched-mold injection solution.
Line-Synchronized Metering
The feed-control interface follows the continuous pultrusion line speed and agreed ratio setpoints.
Closed Injection Box
A closed-die feed arrangement replaces the open resin bath; emissions and exposure controls remain material- and site-dependent.
Fiber Impregnation Control
Metering/mixing circuit pressure and injection-box pressure are controlled separately. Fiber fraction and void content require defined measurements.
Head Shutoff and Cleaning
The specified head shutoff reduces retained mixed resin; the cleaning sequence is established for the selected formulation.


