High-Pressure PU Foaming Machine | Automobile Acoustic Pads
High-pressure PU foaming equipment for automotive acoustic pads, with 50-1000 g/s pouring, ≤±0.3% metering accuracy, two-stage mixing and hydraulic mold carrier integration.
Pouring Rate
50-1000 g/s
Metering Accuracy
≤±0.3%
Dynamic Stirring Speed
7000-12000 r/min after impingement mixing
Impingement Mixing Pressure
10-18 MPa
Engineered for Soundproof, Precision-Foamed Automobile Acoustic Pads
High-pressure impingement mixing followed by dynamic stirring supports metered production of large-format automotive acoustic pads.
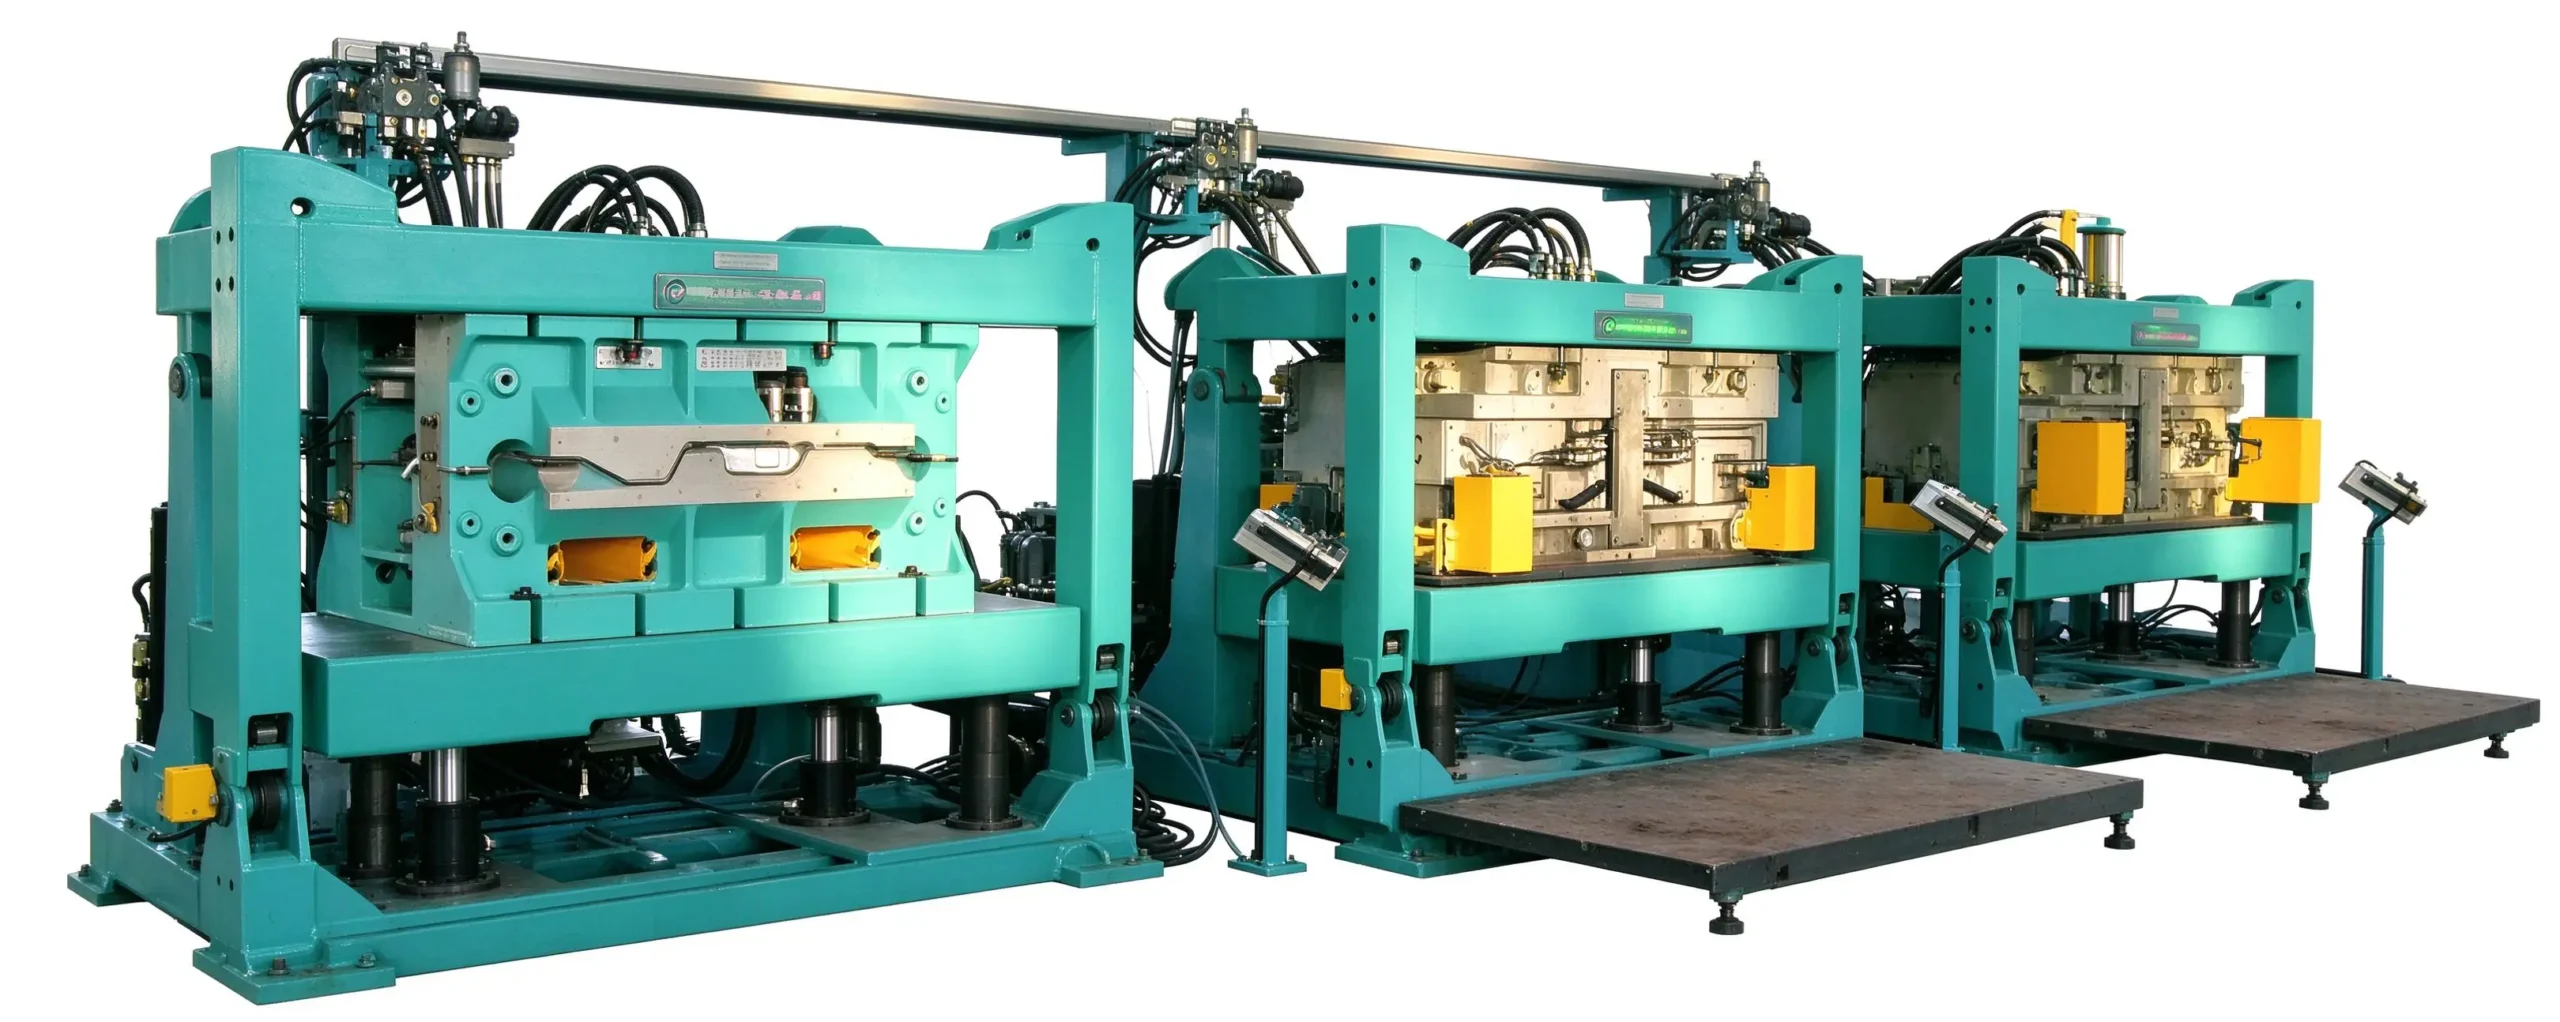
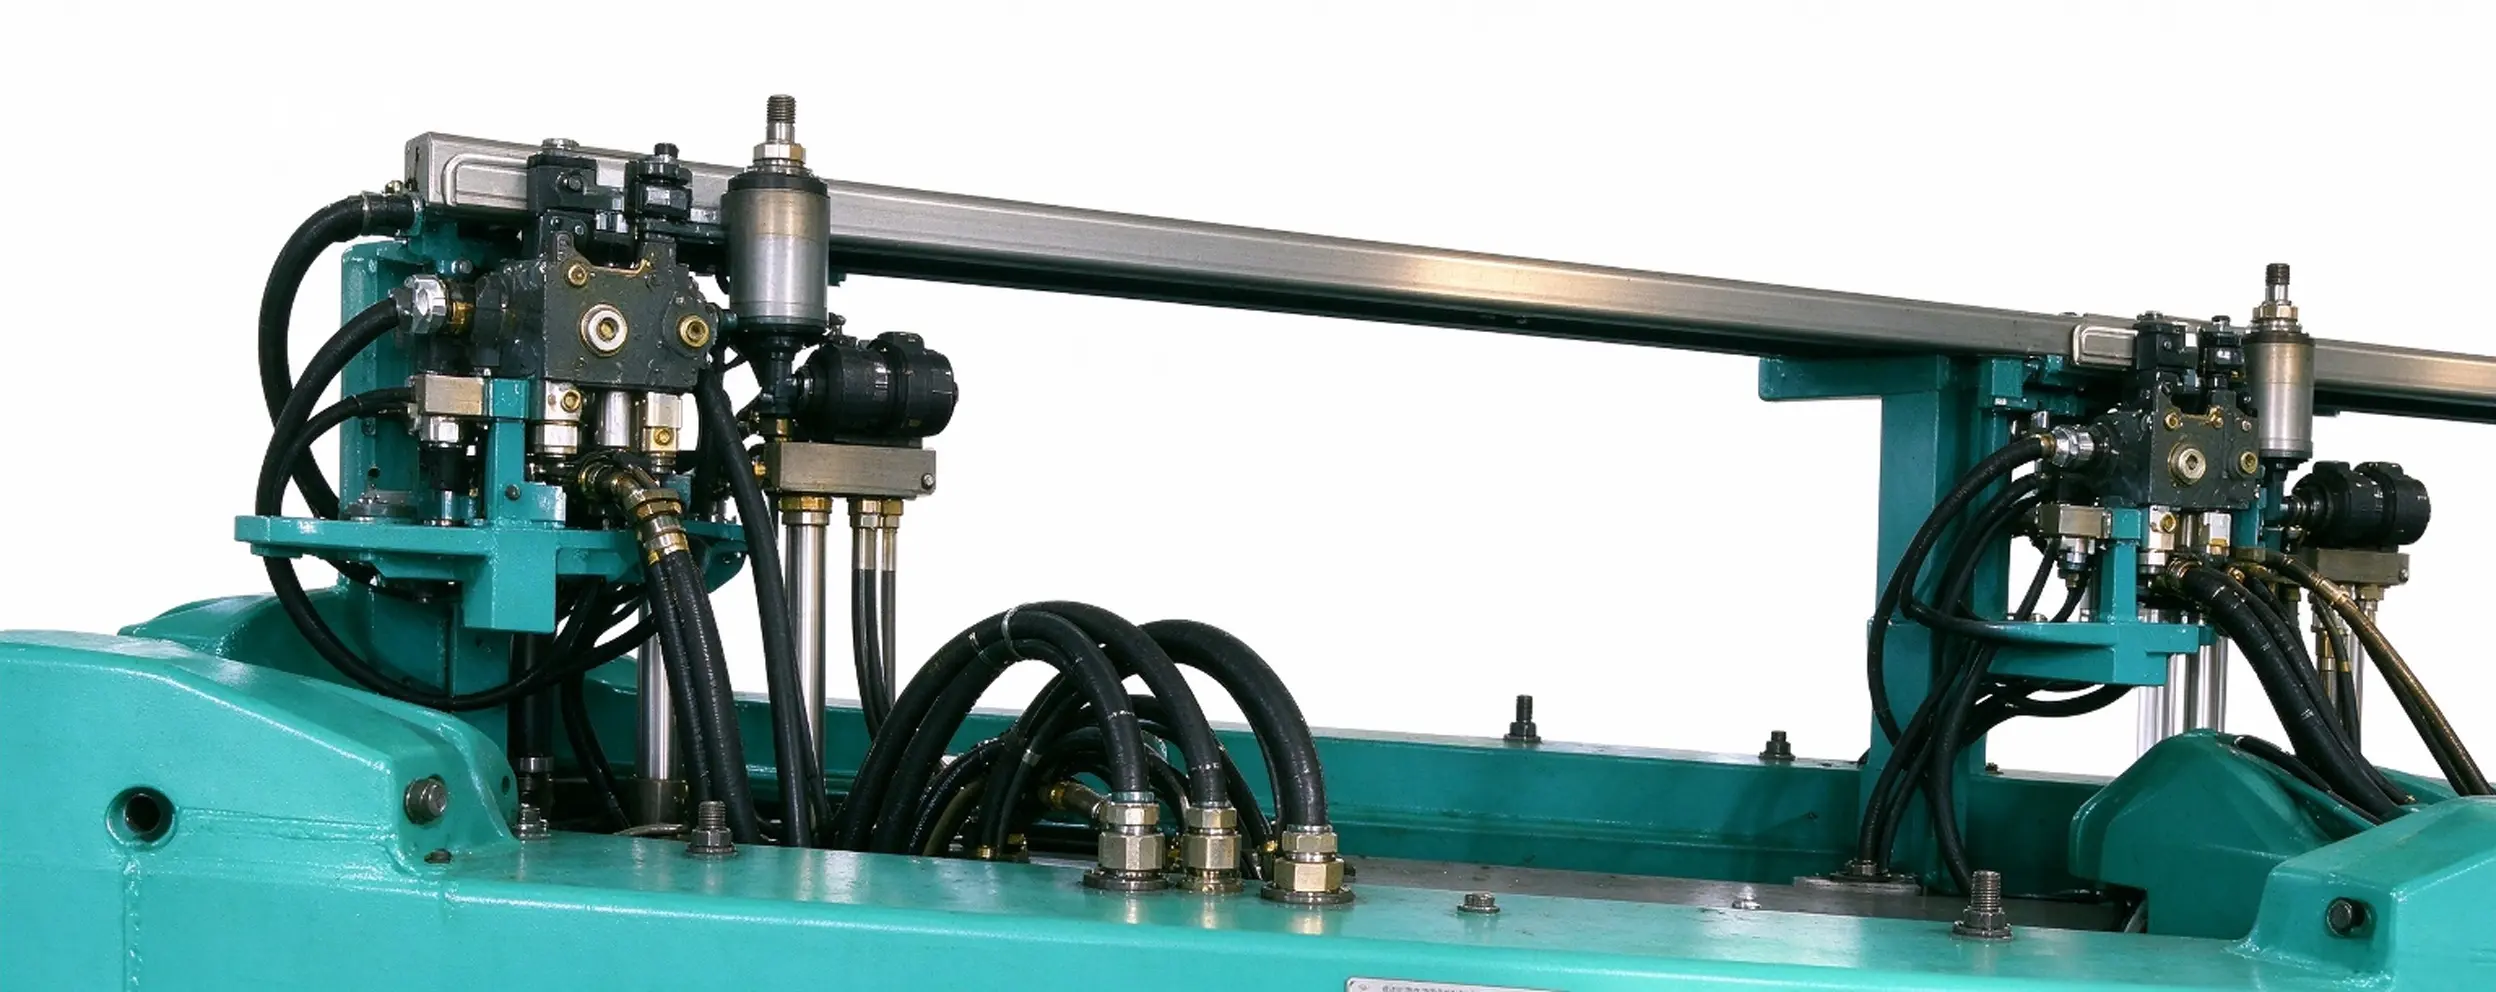
The HF-HPM-1A1B-AcousticPad is a high-pressure polyurethane foaming machine for automotive acoustic pads. It meters two components and combines high-pressure impingement mixing with a following dynamic stirring stage before controlled pouring.
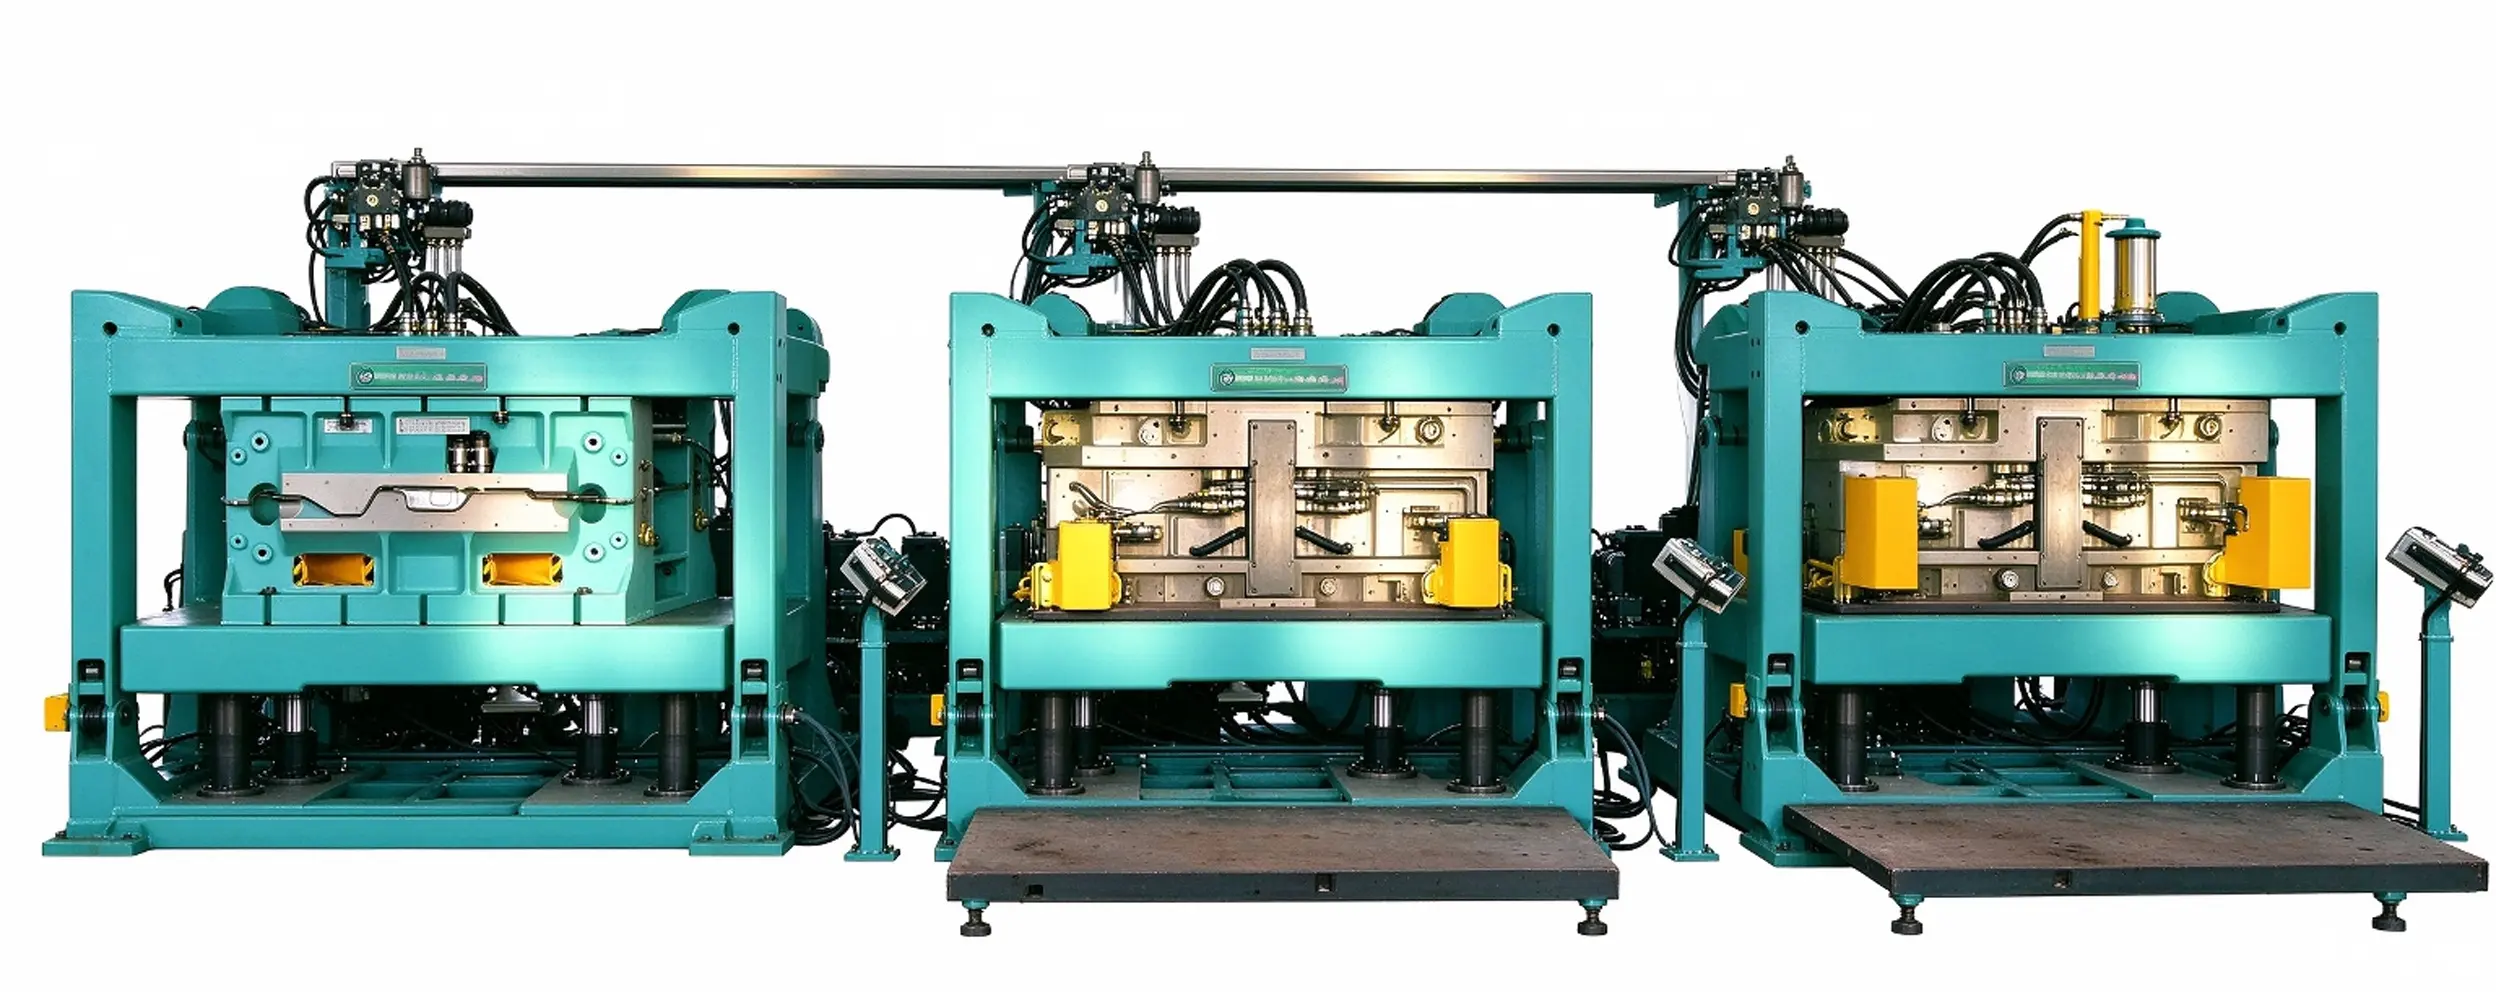
With one or more hydraulic mold carriers, the line can coordinate mold opening, closing, locking, clamping and part removal. The configuration supports engine-compartment acoustic pads, under-carpet pads and wheel-arch liners, with mold boards up to 2,000 × 1,500 mm.
The production route covers material conditioning, metering and mixing, pouring, foaming, curing, demolding and edge trimming. Final acoustic, thermal and dimensional performance depends on the selected PU system, mold design and validated process settings.
Operation Workflow
Raw Material Preparation
Prepare polyether polyol and isocyanate at the target mix ratio (100:45-60) for the acoustic foam recipe, with proper conditioning for uniform cell formation.
Mold Carrier Loading & Temperature Setting
Load polyol into Tank A and isocyanate into Tank B; the 1A1B temperature control maintains 20-45°C, while the hydraulic mold carrier positions and locks the mold.
Metering, Two-Stage Mixing and Pouring
The PLC meters the two components within the specified ±0.3% accuracy range. The configured assembly first uses high-pressure impingement at 10-18 MPa, then a dynamic stirring stage at 7000-12000 r/min before metered pouring into the acoustic pad mold.
Foaming, Curing, Demolding & Trimming
The material foams and cures in the mold; the mold carrier opens and ejects the part, and automatic edge trimming completes the acoustic pad with consistent dimensions.
Technical Specifications
Reference specifications for the two-stage mixing configuration. Tank size, recipe, mold carriers and the acceptance window are defined for each acoustic pad program.
| Technical Parameter | HF-HPM-1A1B-AcousticPad |
|---|---|
| Components | 1A1B two-component PU system |
| Output Range (g/s) | 50-1000 g/s pouring rate |
| Mixing Ratio Range | Polyether:Isocyanate = 100:45-60 (reference recipe) |
| Ratio Accuracy | ±0.3% (reported full dynamic range) |
| Working Pressure | 10-18 MPa impingement mixing pressure |
| Tank Capacity (L) | 100 L or 150 L per tank (optional) |
| Dynamic Stirring Speed | 7000-12000 r/min after high-pressure impingement mixing |
| Tank Configuration | 1A1B Two-Component Independent Temp Control + Circulation Stirring |
| Temperature Control | 20-45℃ |
| Cleaning System | Automatic Air Purge Cleaning (Solvent-Free & Eco-Friendly) |
| Power | 5.5-7.5 kW |
| Control System | PLC + Touch Screen + Multi-Formula Storage |
| Application System | PU flexible / semi-rigid acoustic foam system (customized per acoustic pad recipe) |
| Warranty | 1 Year |
| Certification | Confirm applicable documents for the quoted configuration |
Key Advantages
Six equipment and process features to consider when configuring a high-pressure PU foaming machine for automobile acoustic pads.
Two-Stage Mixing and Precise Metering
Two-component high-pressure impingement mixing is followed by dynamic stirring. The stated ≤±0.3% metering accuracy supports repeatable dosing; finished acoustic performance depends on the recipe and mold process.
Uniform Pouring over Large Areas
Supports acoustic pad molds up to 2,000 × 1,500 mm. Hydraulic mold carriers can be configured for large parts and alternating production.
Automatic Mold Carrier & Edge Trimming
The hydraulic mold carrier completes opening, closing, locking, mold-plate up/down, clamping and edge trimming, replacing manual trimming with consistent dimensions and less labor.
Eco-Friendly Solvent-Free Cleaning
Automatic air-purge cleaning reduces the need for solvent cleaning of the mixing assembly. Finished-part emissions still depend on the material system and must be evaluated against the application requirements.
PLC Intelligent Control with Multi-Formula Switchover
One-click multi-formula switchover and fault self-check reduce manual errors and enable rapid changeovers between different acoustic pad specifications.
Complete Automated Production Line Integration
Pairs with hydraulic mold carriers for fully automated metering-to-edge-trimming production of engine-compartment pads, under-carpet pads and wheel-arch liners.


