
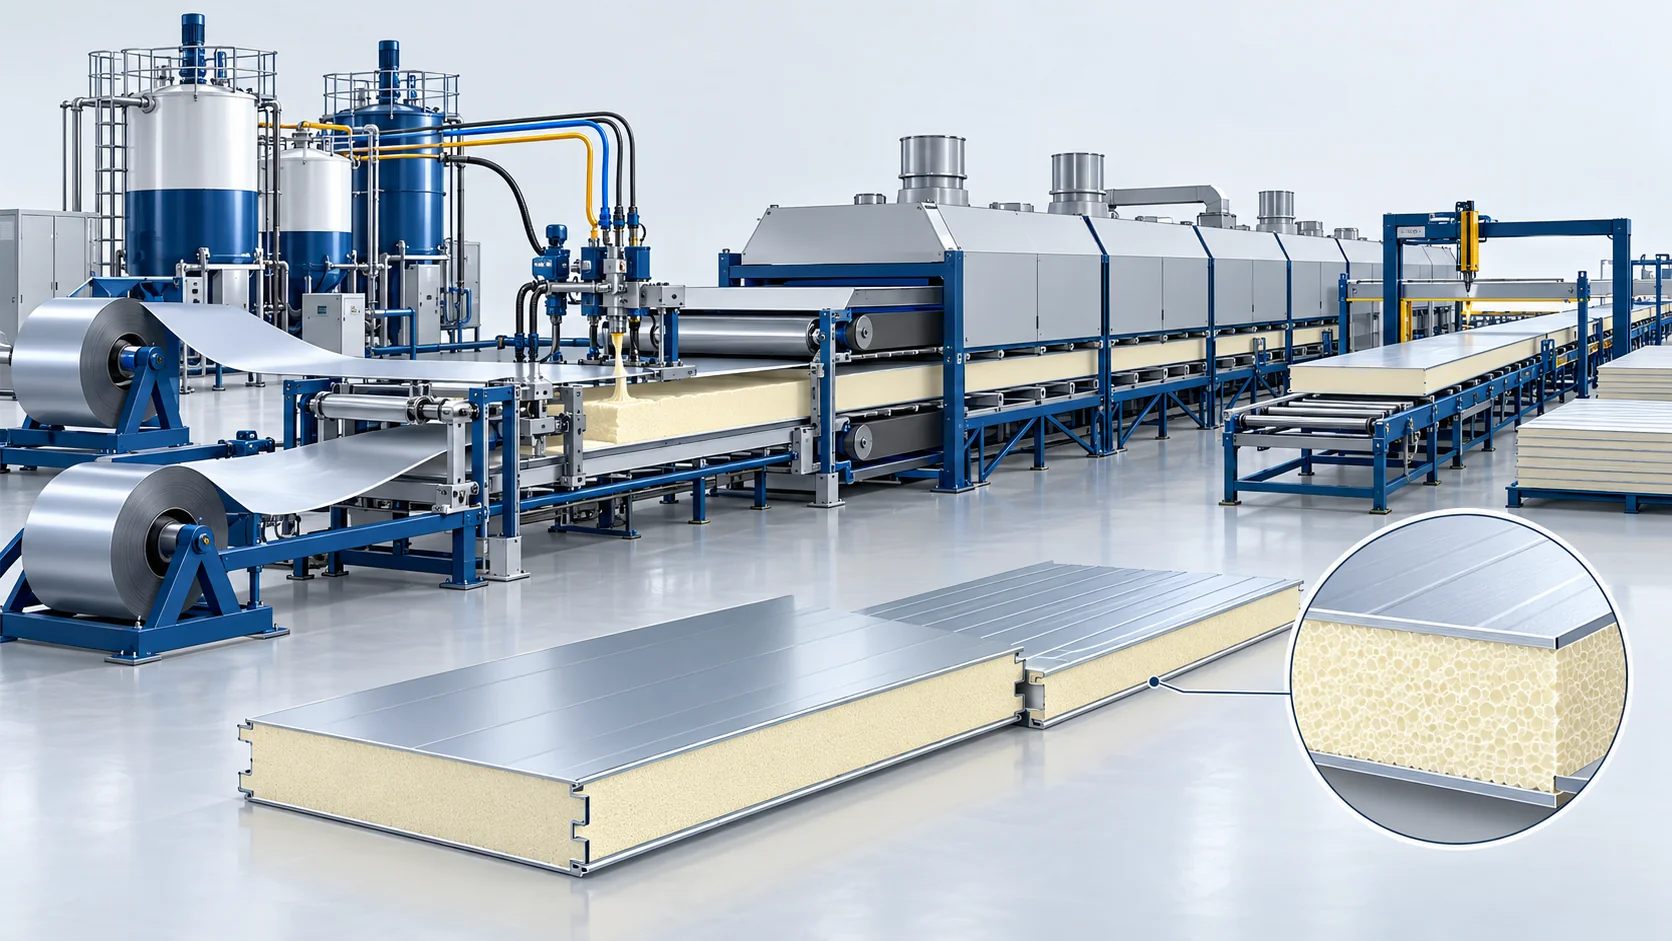
Continuous PIR Panel Line | Cold Storage Insulation
Built for industrial cold storage panels, the HF-PIR42-CB delivers continuous 6-component high-pressure dosing, high-frequency oscillating spray, and a 42-meter double-belt laminator for fire-retardant PIR insulation up to 200 mm thickness. Concept illustration — not a photograph of delivered equipment or a customer installation.
High-Capacity Continuous PIR Insulated Panel Lamination
The HF-PIR42-CB is a 42-meter continuous double-belt sandwich panel production line engineered for manufacturing high-density, fire-retardant PIR cold storage panels with exceptional thermal insulation and structural flatness.
The HF-PIR42-CB supplied reference coordinates facing preparation, six-stream metering, traversing laydown, a 42 m double belt, cutting and stacking. The stated stream list is polyol, isocyanate, catalyst 1, catalyst 2, flame retardant and blowing agent. Water, where part of the recipe, requires a defined feed arrangement and is not automatically a seventh independent stream.
Reference limits include 40–200 mm panel thickness and 4–15 m/min belt operation. These limits are not simultaneous cure guarantees. A separate supplied 80–350 kg/min metering envelope must be matched to actual core demand, including low-flow turndown. Core compression, bond strength, thermal performance and fire reaction require panel tests.
Concept illustration — not a photograph of delivered equipment or a customer installation.
Material Flow and Working Principle
Continuous Uncoiling & Roll Forming
Prepare and profile facings; surface activation is selected for the facing and validated with bond tests.
Multi-Component High-Pressure Metering
Six independent chemical streams are metered by high-precision axial piston pumps equipped with Coriolis mass flow meters, maintaining exact stoichiometry for high-index PIR formulations.
High-Frequency Oscillating Laydown
The mixed chemicals enter a multi-orifice high-pressure impingement mixing head mounted to a servo-driven crosshead swinging at up to 120 cycles/minute, spraying a uniform liquid fan across the lower steel facing.
Continuous 42-Meter Double-Belt Curing
The expanding foam and steel facings enter the 42-meter double-belt conveyor, where precision ground steel slats apply controlled heat (45–65°C) and side-block containment to cure the PIR matrix to exact thickness.
Synchronized Flying Cross-Cutting & Stacking
The continuous cured panel is cut to custom lengths (up to 18 meters) by a high-speed tracking flying saw without stopping the line, then automatically cooled and vacuum-stacked for packaging.
Model and Technical Parameters
Configuration values from the supplied equipment brief. Final settings and capability are confirmed for the selected material and project conditions. Thickness, speed and dosing limits are independent; confirm minimum delivery against panel demand. Polyol:isocyanate ratio and isocyanate index are different quantities.
| Technical Parameter | HF-PIR42-CB |
|---|---|
| Components | 6 Components (Polyol, Iso, Catalyst 1, Catalyst 2, Flame Retardant, Blowing Agent) |
| Output Range (g/s) | 80.0 to 350.0 kg/min (Continuous output) |
| Mixing Ratio Range | 100:130 to 100:250 supplied polyol:isocyanate ratio reference; confirm mass/volume basis. This ratio is not the isocyanate index. |
| Ratio Accuracy | ±0.3% (Independent Coriolis mass flow loops) |
| Power Supply | 380V, 3-Phase, 50Hz (Custom 440V/480V 60Hz optional) |
| Working Pressure | 14.0 to 18.0 MPa (Six-component high-pressure lines) |
| Tank Capacity (L) | Day tanks: 2 x 1000 L (Main), 4 x 200 L (Additives) |
| Weight | Approximately 85,000 kg (Complete line mechanical weight) |
| Dimensions (L×W×H) | 95,000 mm x 5,500 mm x 4,500 mm (Total line footprint) |
| Double-Belt Effective Length | 42 meters (High-precision ground steel slats); Laminator Press Section |
| Panel Thickness Range | 40 to 200 mm (Continuously adjustable); Finished Sandwich Panel |
| Continuous Line Speed | 4.0–15.0 m/min listed drive envelope; viable production speed depends on thickness, recipe and cure |
| Total Installed Power | 185 kW (Drive motors, heaters, roll forming); Peak production load |
Key Equipment Features
The package covers coil handling and forming, six-stream metering and foaming, traversing distribution, a 42 m double-belt section, flying cutting and stacking. Cam-lock insertion and rock-wool processing are optional. Steel coils, chemistry, building services and power are agreed external interfaces.
42 m Double-Belt Section
The specified laminator provides a controlled curing and pressure section for the chosen panel build-up.
PIR Formulation Control
Independent dosing supports the selected PIR formulation. Fire classification belongs to tested finished panels.
Traversing Distribution
A servo distribution boom spreads the mixture across the specified web width.
Six-Stream Metering
Separate streams control main components and additives against the agreed material recipe.


