

Producing consistent polyurethane foam is not just a matter of keeping the machine running. A fresh drum of catalyst, a two-degree shift in material temperature, or a formulation tweak that looks minor on paper can change cream time, rise profile, and cell structure within a single shift. When parts come out softer than expected, the foam collapses mid-rise, or the mold opens with a sticky surface, the investigation almost always leads to the same place: the balance between the gelling and blowing reactions — and the amine catalyst package that controls it.
What Amine Catalysts Actually Do
In a polyurethane foaming system, two reactions compete for the same isocyanate group. The first is the gelling reaction: isocyanate reacts with polyol to build the urethane polymer network that gives foam its strength and load-bearing ability. The second is the blowing reaction: isocyanate reacts with water to release carbon dioxide, which expands the mixture into cells [1].
Without a catalyst, both reactions are too slow at normal processing temperatures — the foam would not rise to full height before viscosity stops it, or the cycle would stretch far beyond what production budgets allow. Tertiary amine catalysts lower the activation energy of the isocyanate reactions, accelerating the chemistry without being permanently consumed. That is why “amine catalyst” in polyurethane formulation almost always means a tertiary amine: primary and secondary amines react with isocyanate themselves and become part of the polymer chain, which changes stoichiometry rather than simply speeding up kinetics [2].
The critical subtlety is selectivity. Tertiary amines do not accelerate gelling and blowing at the same rate. Some push the urethane reaction more aggressively, while others favor the isocyanate–water reaction. Formulation work is largely about choosing amines, and amine ratios, so both reactions keep pace with the mold geometry, target density, and line speed of the process.
Gelling vs. Blowing Catalysts: Two Competing Reactions
The distinction is easiest to read as a table:
| Factor | Gelling reaction | Blowing reaction |
|---|---|---|
| Reactants | Isocyanate + polyol | Isocyanate + water |
| Primary product | Urethane linkage → polymer network | Urea + CO₂ gas |
| What it builds | Strength, hardness, load bearing | Cell structure, density, rise |
| If it runs too fast | Dense foam, high exotherm, shrinkage risk | Collapsed or coarse cells, splits, weak walls |
Calling a catalyst “gelling” or “blowing” is a simplification. Every amine accelerates both reactions to some degree; the label describes which one it favors. In flexible slabstock and molded foam, a small dose of a blowing-selective amine such as bis(2-dimethylaminoethyl)ether (BDMAEE) is often paired with a gelling-leaning workhorse such as triethylenediamine (TEDA) — chemically, 1,4-diazabicyclo[2.2.2]octane. That pairing is what gives formulators independent control over cell opening and skin quality.
The practical consequence of this competition is timing. If the blowing reaction runs ahead, carbon dioxide is released before the polymer matrix builds enough viscosity to hold the gas; bubbles coalesce or break, producing a collapsed or coarse structure. If gelling runs too far ahead, the network stiffens before full expansion, trapping a dense, heavy foam with poor breathability and, in molded parts, a real risk of dimensional instability.
Reading Reaction Timing: Cream, Gel, Rise, and Tack-Free
Production teams tend to discuss four time markers rather than reaction kinetics, and each responds differently to catalyst choice.
- Cream time — from mixing start to the first visible change, usually a slight clouding or the beginning of expansion.
- Gel time — the point at which the polymer has reacted enough to form a soft solid; a probe drawn out will string.
- Rise time — the moment the foam reaches full height and stops expanding.
- Tack-free time — when the surface no longer feels sticky, whether in slabstock or molded work [3].
A blowing-heavy amine shortens cream and rise time significantly but does less to build early gel strength. A gelling-heavy amine hardens the matrix sooner; that can narrow the gel-to-rise window, which helps quick demold but becomes risky if cells have not finished opening.
Rise time is one of the first numbers to drift when the catalyst package changes. The Role Of Rise Time In Polyurethane Foaming covers how to measure it consistently and what a healthy rise curve looks like line to line.
The four markers only make sense when read together. A formulation that shows the same rise time but a longer gel time than a month ago is no longer the same process — even if the foam looks acceptable at demold. That is why reaction profile data, not just final density, belongs in batch records.
Key Amine Catalyst Types and How They Behave
The table below is a general guide, not a rigid grade list. Suppliers sell proprietary packages — including heat-activated or acid-blocked versions — that release active amine only as the mold temperature climbs.
| Amine class | Common example | Selectivity profile | Typical role |
|---|---|---|---|
| Gelling-leaning tertiary amine | TEDA (1,4-diazabicyclo[2.2.2]octane) | Strong gelling, moderate blowing | Workhorse in flexible and rigid foam |
| Blowing-selective tertiary amine | BDMAEE (bis(2-dimethylaminoethyl)ether) | Strong blowing | Small doses paired with TEDA |
| Moderate, reduced-odor amine | Dimethylcyclohexylamine (DMCHA) | Moderate gelling/blowing | Used where odor control matters |
| Reactive amine | Dimethylethanolamine (DMEA) | Moderate, OH-functional | Reduces VOC and fogging |
The same amine can behave differently as dosage and temperature change. Activity climbs with material temperature, so a package tuned for a 25 °C tank feed may run noticeably faster at 35 °C. Catalyst selection and temperature control are therefore two halves of one decision, not independent settings. Final flexible foam properties are ordinarily confirmed against standardized test methods such as ASTM D3574 [4].
The same formulation choices that shift gel and rise times also show up in standardized property tests. Measuring Polyurethane Foam Resilience A Practical Test Guide covers how resilience is measured and what the rebound value reveals about cell structure and formulation.
Dosage, Index Interactions, and Common Troubleshooting
In water-blown flexible foam, total amine loading typically falls around 0.1 to 1.0 parts per hundred parts polyol (pphp), with most production formulas in the lower-to-middle portion of that window [3]. Exact levels depend on target density, mold temperature, gel-time requirements, and any tin co-catalyst present. They are formulation-specific, not universal constants.
Amine choice also interacts with the isocyanate index. The index — the ratio of isocyanate groups to available hydroxyl and water groups — sets the ceiling for crosslink density and water-blown intensity; a catalyst package cannot create a reaction that the stoichiometry will not support. Raising the index changes hardness and compression set far more than a small amine ratio adjustment, so I always ask teams to confirm metered component ratios before re-formulating. That instinct matches the classical literature, which treats the gelling–blowing balance as the central lever in foam formulation [5].
| Observation | Common catalyst-related cause | First checks |
|---|---|---|
| Slow cream or weak rise | Lost catalyst activity, low temperature, metering underfeed | Verify catalyst flow and drum age; check tank temperature |
| Coarse or collapsed cells | Blowing too fast, gelling too slow | Raise gelling amine share; recheck water and temperature |
| Shrinkage after demold | Gelling too fast, delayed cell opening | Reduce gelling amine share; verify mold temperature |
| Sticky surface, slow tack-free | Under-catalyzed surface cure | Check package and mold surface temperature |
| Dense, heavy foam, poor breathability | Network built before full expansion | Rebalance blowing/gelling amine ratio |
Shrinkage is one of the clearest signals that the gelling reaction is running ahead of the blowing reaction. Causes Of Shrinkage In Polyurethane Foam How To Control It walks through the mechanism and the process adjustments that bring the two back into balance.
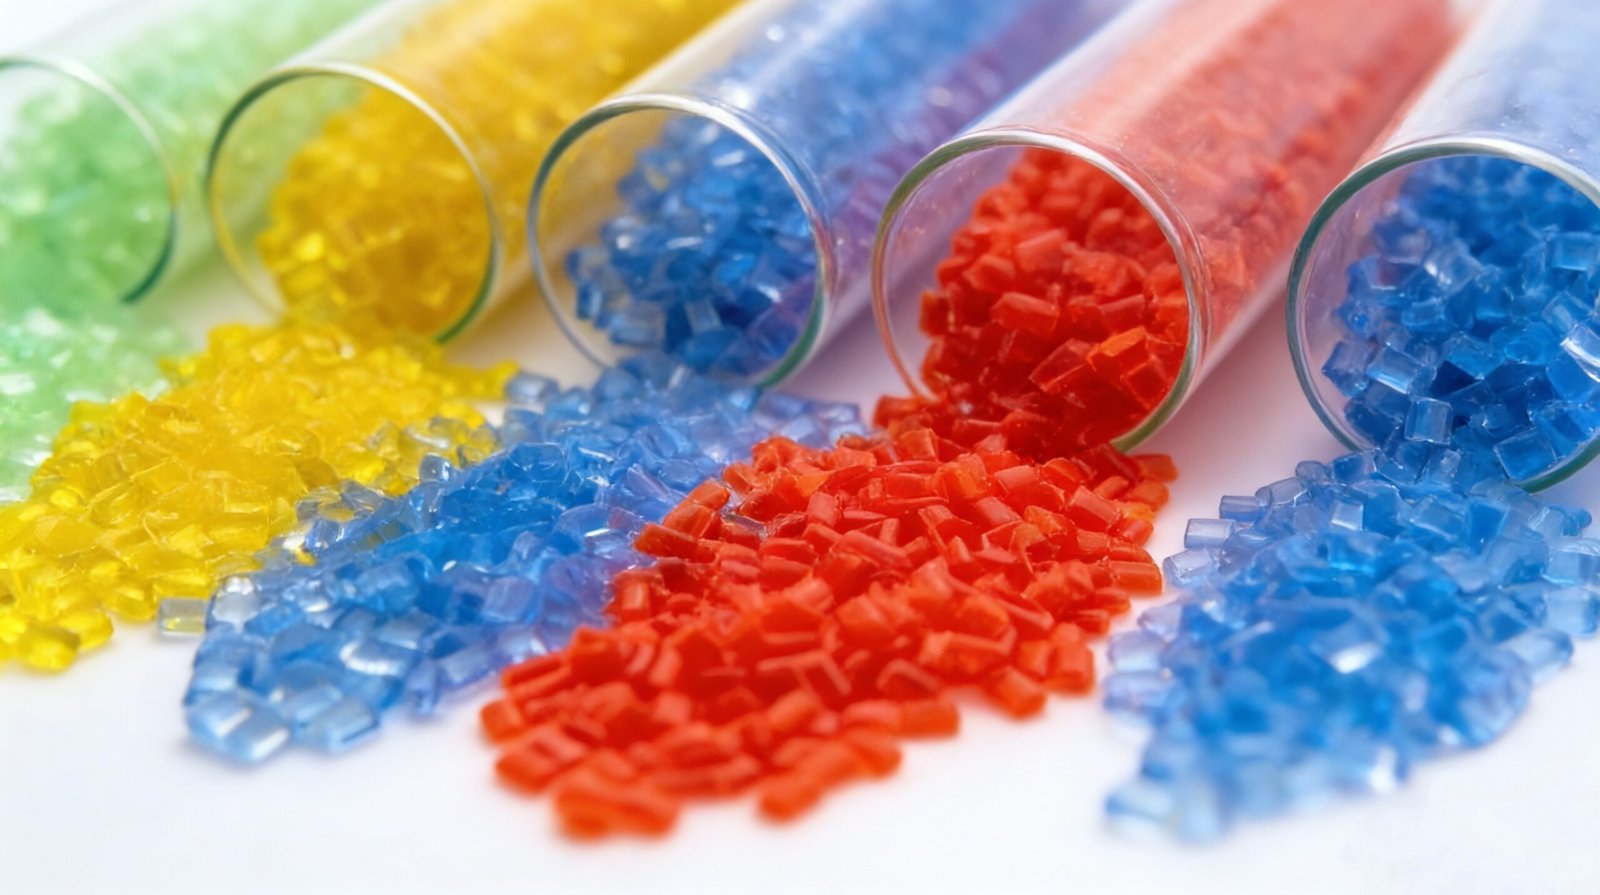
Why Metering and Mixing Equipment Matters for Catalyzed Systems
Catalyst adjustments only work if the line delivers the intended amounts. Amine catalysts are typically dosed at low flow rates — often a small fraction of the polyol stream — so a metering drift of even ±0.5% can shift effective catalyst loading by several percent. That is enough to move cream and gel time measurably even when the recipe on the PLC has not changed.
On high-pressure foaming and pouring machines, component temperatures are controlled independently. If the amine or polyol line runs a few degrees above setpoint, catalyst activity shifts at constant dosage. Mixing head condition matters in the same way: a worn or poorly maintained mixer seeds gas irregularly, and the reaction profile changes even if the chemistry is untouched.
From an equipment standpoint, this is why metering stability usually matters more for catalyzed systems than peak output. Servo-driven metering with full-range accuracy around ±0.3%, stable tank temperature control, and consistent mixing head maintenance keep the catalyst contribution repeatable, so the formulation logic stays valid across shifts.
If batch records show cream or rise time drifting while the recipe stays fixed, start with the metering loop before changing the catalyst package. Send Info@chinahaifeng.com these six values: cream, gel, rise, and tack-free times; both component tank temperatures; and your target cycle time. That data is enough to separate a mechanical drift from a chemical one — and to keep you from re-formulating a process that was never the problem.
A Practical Selection Checklist
Catalyst choice is a process decision, not a raw-material purchase order. Run through these points before committing to a package:
- Confirm target density and whether the system is water-blown or physically blown; blowing load sets the required blowing catalyst share.
- Record current cream, gel, rise, and tack-free times. Do not work from memory.
- Check the isocyanate index before touching the catalyst package. An index error defeats any catalyst change.
- Match catalyst activity to actual material and mold temperature setpoints.
- If odor, fogging, or VOC limits apply, prefer reactive amines or delayed-action packages.
- Verify the metering accuracy of the catalyst stream. If it is the least stable line, correct equipment first.
- Pilot a new combination on a small run with a fixed-temperature cure check before scaling to full production.
Need a Foaming Process Review?
When cream, gel, and rise times shift on a fixed recipe, the answer is rarely a single catalyst package swap. Haifeng Polyurethane Machinery builds metering and mixing lines for repeatable catalyzed foaming and can read your current reaction profile before you change formulation. Describe your line layout, raw materials, and target cycle to:
Email: Info@chinahaifeng.com
WhatsApp: 86 13566296633
FAQ
What is the difference between gelling and blowing amine catalysts?
Both are tertiary amines, but gelling-leaning amines accelerate the isocyanate–polyol reaction more strongly, while blowing-selective amines favor the isocyanate–water reaction. In practice, formulators blend both types to control polymer strength and cell structure independently.
How much amine catalyst should I use?
For water-blown flexible foam, total amine loading typically falls around 0.1 to 1.0 pphp, but exact dosage depends on density, mold temperature, index, and any tin co-catalyst. Start low, hold temperature constant, and adjust against measured reaction times rather than appearance alone.
Do amine catalysts cause foam odor?
Volatile tertiary amines can contribute to odor and fogging, particularly in automotive interiors. Reactive amines with a hydroxyl group, or heat-activated packages, reduce the free volatile amine content and associated emissions.
What does a delayed-action amine catalyst do?
A delayed-action or acid-blocked amine remains largely inactive at low temperature and releases active amine once the mold reaches the target temperature. This widens the filling window for large or complex molds so the mixture can flow before foaming accelerates.
How do I know if catalyst imbalance is causing shrinkage?
Look at the timing before the density. If gel time has moved earlier while rise time stays roughly the same, the gelling reaction often leads; reducing the gelling amine share and verifying mold temperature usually brings it back into balance.
Do amine catalysts affect equipment cleaning?
Yes, indirectly. Faster systems shorten the working life of residual mixed material, so flush cycles and mixing head cleaning intervals may need to follow the reaction profile. Equipment with automatic circulation and air-purge cleaning keeps the shot chamber from curing between cycles.
References
[1] G. Oertel, Ed., Polyurethane Handbook, 2nd ed. Munich, Germany: Hanser Publishers, 1994.
[2] M. Szycher, Szycher’s Handbook of Polyurethanes, 2nd ed. Boca Raton, FL, USA: CRC Press, 2012.
[3] M. Ionescu, Chemistry and Technology of Polyols for Polyurethanes, 2nd ed. Shrewsbury, U.K.: Smithers Rapra, 2016.
[4] Standard Test Methods for Flexible Cellular Materials—Slab, Bonded, and Molded Urethane Foams, ASTM D3574-17, ASTM International, West Conshohocken, PA, USA, 2017.
[5] G. Woods, The ICI Polyurethanes Book, 2nd ed. Chichester, U.K.: John Wiley & Sons, 1990.
If you’re interested, check out these related articles:
Causes Of Shrinkage In Polyurethane Foam How To Control It
What Is Spray Polyurethane Foam Composition And Application
Shore A Vs Shore D Hardness In Polyurethane
Measuring Polyurethane Foam Resilience A Practical Test Guide





