
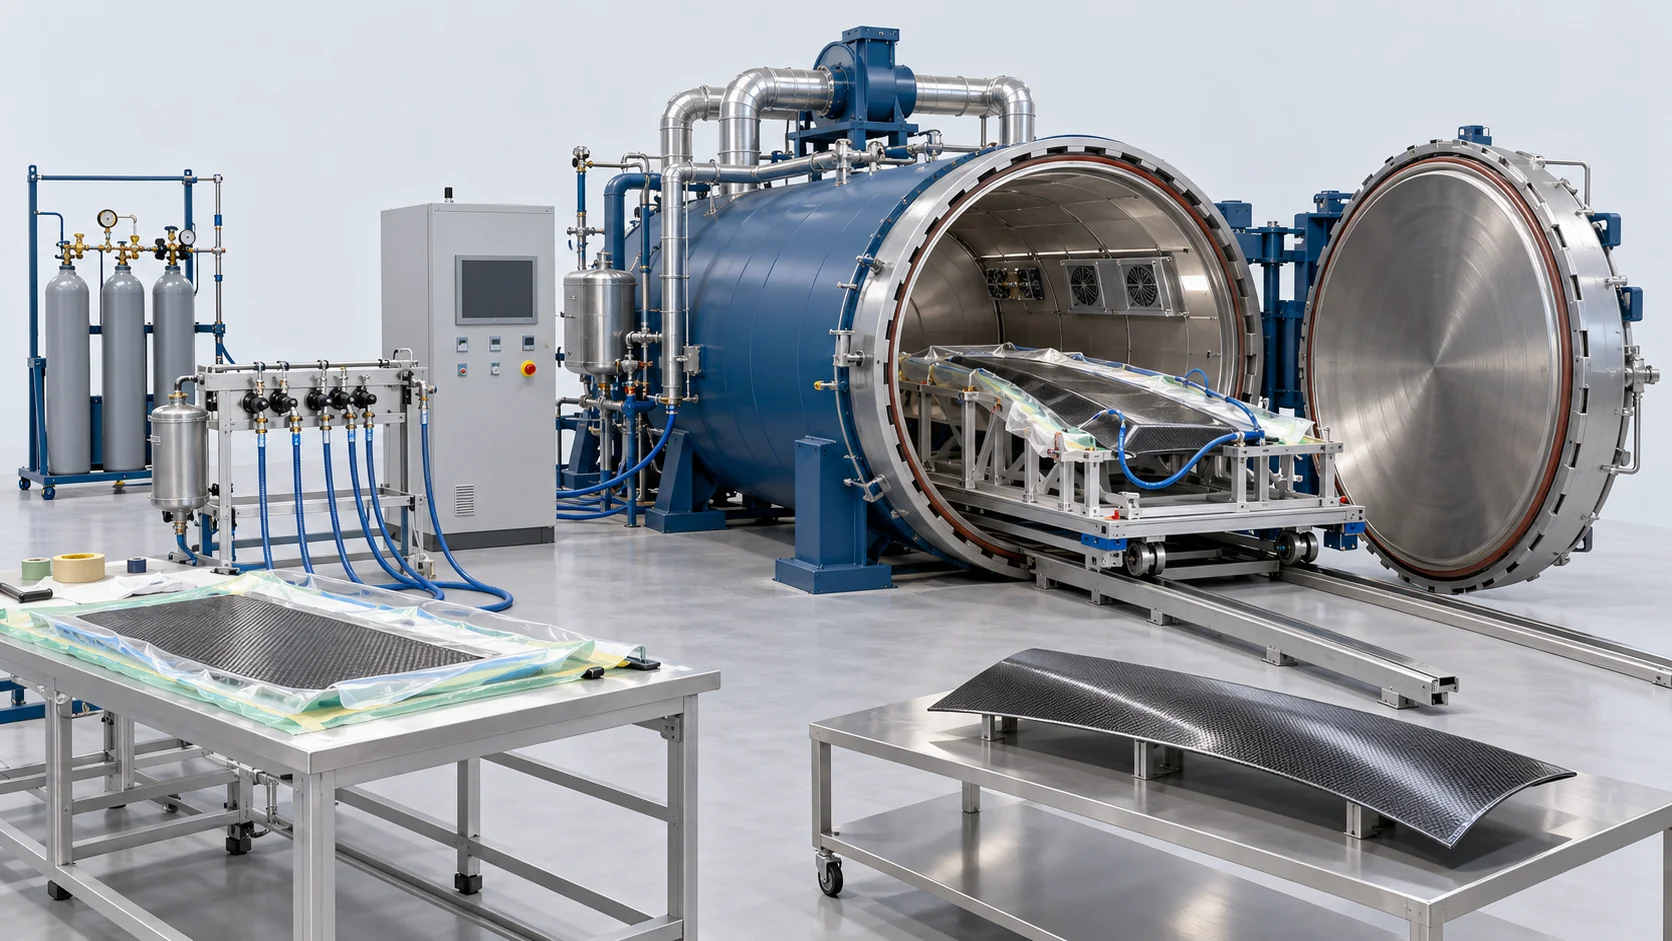
Aerospace Composite Autoclave Solution
A monitored pressure-vessel curing package with zoned heating, gas pressurization and independent tooling vacuum circuits.
Controlled Consolidation for Primary Aerostructures
A monitored pressure-vessel curing package with zoned heating, gas pressurization and independent tooling vacuum circuits.
Equipment and process scope
Specified vessel/door, heating/circulation, pressurization, vacuum circuits and controls. Tooling, prepreg, gas supply, facility design and applicable pressure-vessel documentation are separately agreed.
Validation and production planning
The 3.5 m × 12 m clear working envelope and approximately 130 m³ total vessel volume describe different geometry. Ultrasonic inspection coverage and quantitative laminate porosity are separate acceptance tasks. Equipment capability does not by itself establish aerospace qualification.
The 3.5 m × 12 m clear working envelope and approximately 130 m³ total vessel volume describe different geometry. Ultrasonic inspection coverage and quantitative laminate porosity are separate acceptance tasks. Equipment capability does not by itself establish aerospace qualification.
Turnkey Aerospace Autoclave Consolidation Workflow
The sequence describes the supplied configuration. Final settings, cycle boundaries and acceptance are defined for the selected material and tooling. The 3.5 m × 12 m clear working envelope and approximately 130 m³ total vessel volume describe different geometry. Ultrasonic inspection coverage and quantitative laminate porosity are separate acceptance tasks. Equipment capability does not by itself establish aerospace qualification.
Prepreg Bagging & Multi-Port Vacuum Leak Check
Supplied process reference: Prepreg layups on Invar tools are sealed in vacuum bags, shuttled into the vessel, and checked across 48 lines (leak rate < 0.05 kPa/min).
Door Breech-Locking & Nitrogen Pressurization
Supplied process reference: The breech-lock door locks under triple mechanical interlocks; pure nitrogen gas pressurizes the vessel up to 1.0–1.5 MPa.
Multi-Zone Convective Heating (1.5°C/min)
Supplied process reference: Symmetrical annular air ducts and finned electric heaters raise temperatures at 1.5°C/min to 180°C, holding zone drift within ±1.5°C.
Reference Solution Engineering Envelope
Supplied configuration and validation references; material/component results are separate from equipment ratings.
| Parameter | Value / Unit | Applicable Configuration / Conditions |
|---|---|---|
| Effective Working Dimensions | Ø 3,500 mm Diameter x 12,000 mm Length | Accommodates 11m monolithic wingbox panels and spars; configuration-specific reference or part acceptance target |
| Maximum Vessel Operating Pressure | 0.1 to 1.5 MPa (15 bar) | High-purity dry nitrogen gas pressurization; configuration-specific reference or part acceptance target |
| Operating Temperature Range | Ambient up to 250°C | Multi-zone electric finned circulation heaters; configuration-specific reference or part acceptance target |
| Thermal Field Uniformity | Within ±1.5°C across working zone | 24-point survey conforming to AMS 2750F pyrometry; configuration-specific reference or part acceptance target |
| Ultrasonic Inspection Pass Rate | Specified part acceptance target; original records required | Ultrasonic coverage, acceptance criteria and quantitative porosity measurement are separate; review the part-specific original method and report |
| Cured Laminate Porosity Level | Specified part acceptance target; original records required | Ultrasonic coverage, acceptance criteria and quantitative porosity measurement are separate; review the part-specific original method and report |
Core Equipment for This Solution
Specified vessel/door, heating/circulation, pressurization, vacuum circuits and controls. Tooling, prepreg, gas supply, facility design and applicable pressure-vessel documentation are separately agreed.
Core Advantages of Haifeng Autoclave Systems
Configured equipment functions and interfaces for the selected material and tooling.
±1.5°C Precise Thermal Field
The supplied ±1.5°C working-zone uniformity reference is assessed under the specified loaded survey conditions; part thermal response is evaluated for the selected laminate and tool.
Defined Laminate Acceptance
Nitrogen pressure and tooling vacuum support consolidation. The supplied below-0.2% porosity target requires its own quantitative method; neither pressure nor C-scan coverage guarantees a 100% pass rate.
Monolithic 12m Wingbox Capacity
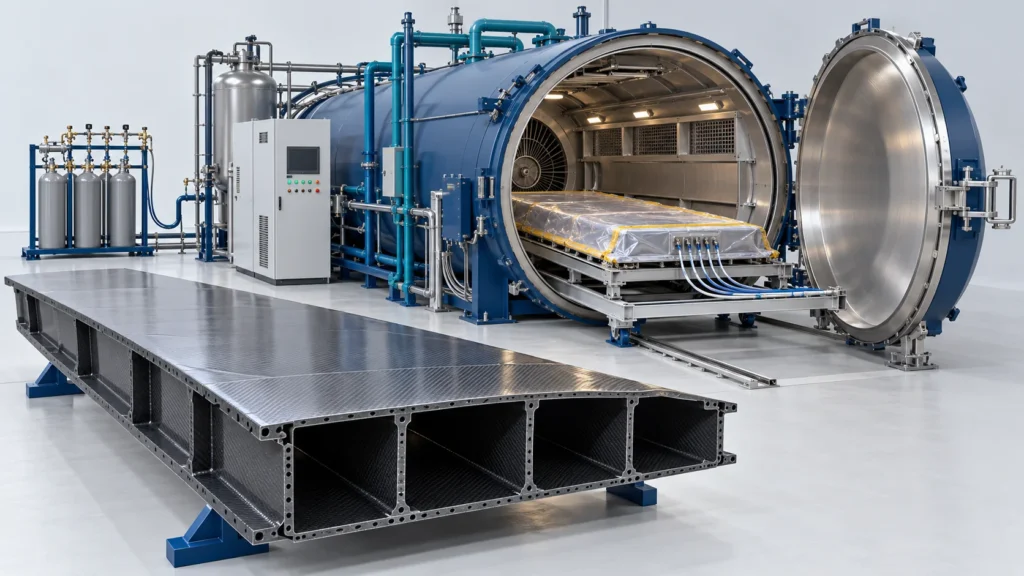
The supplied 12 m envelope accommodates the selected large-tool configuration. The reported 85 kg fastener comparison concerns the particular aircraft structure, not general equipment performance.
48-Channel Vacuum Security
The supplied 48 independent vacuum channels monitor tool-bag vacuum and leak alarms during the defined cure schedule; bag integrity and acceptance remain project-specific.
Related Project Draft
The related wingbox brief describes a specific tool, laminate, cure and inspected project population; its reported outcomes do not establish universal aerospace qualification.
Frequently Asked Questions
How is thick-laminate thermal response controlled?
How is the pressurizing gas selected?
What does the 48-channel vacuum system monitor?
Does an ultrasonic C-scan prove porosity or aerospace qualification?
Discuss Your Production Goals
Share your product or drawing, material system, target output, automation needs and factory utilities so the equipment and interfaces can be configured.


