
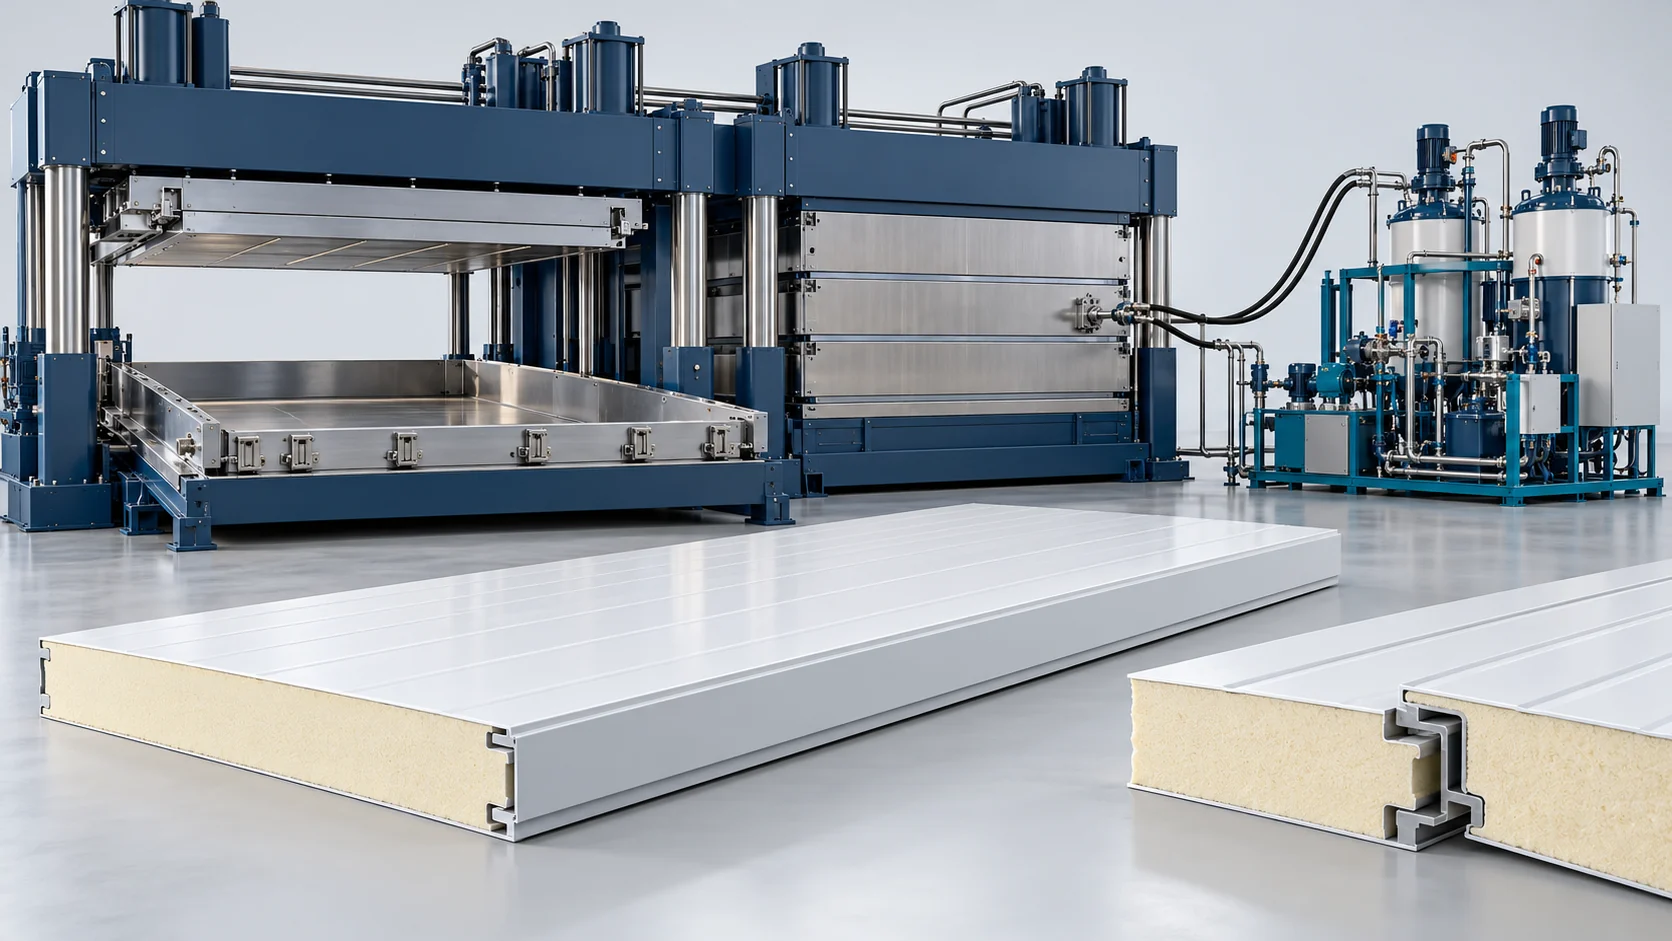
Решение для формования прерывистых сэндвич-панелей ППУ
Flexible hydraulic press foaming systems engineered for customized cold room panels, freezer doors, and modular walk-in coolers. Concept illustration — not a photograph of delivered equipment or a customer installation.
Highly Flexible Discontinuous PU Panel Molding Solutions
While continuous lines excel at massive standard volumes, regional cold room builders, refrigerated display manufacturers, and specialty vehicle upfitters need versatility to produce custom dimensions, variable thicknesses (50–250mm), and panels with embedded eccentric cam-locks. Haifeng’s discontinuous sandwich panel solution utilizes high-pressure injection machines synchronized with multi-daylight 2+2 hydraulic presses, allowing independent loading, injection, curing, and unloading cycles with separate loading, curing and changeover allowances.
2+2 Alternating Daylight Productivity
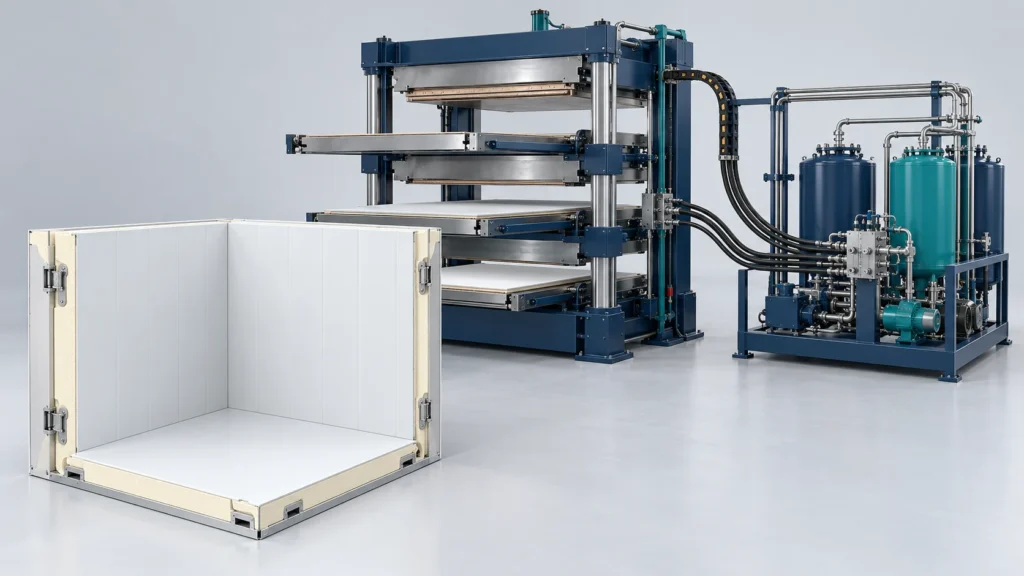
While one set of platens undergoes pressurized curing, operators load sheet boxes and cam-locks on the opposite platens, maximizing press cycle utilization.
Precision Embedded Cam-Lock Integration
Magnetic positioning side bars hold eccentric male and female cam-locks securely inside the mold, producing walk-in cold room panels ready for instant site latching.
Сравнение смежных производственных маршрутов
Balance box assembly, injection, heated cure and unloading across the selected alternating press arrangement. Embedded locks, door components and PIR materials need their own tooling and material review rather than being inferred from platen dimensions.
Discontinuous Hydraulic Panel Pressing Workflow
A synchronized four-stage workflow delivering custom-dimension insulated panels with high density uniformity.
Sheet Box Loading & Cam-Lock Positioning
Pre-cut metal sheet boxes are placed onto the open platen; perimeter boundary bars embedded with magnetic cam-lock locators are clamped securely around the edges.
High-Pressure Multi-Port Foam Injection
A high-pressure PU dosing unit injects a metered chemical shot through side-edge injection holes; the liquid formulation spreads evenly across the closed, tilted cavity.
Hydraulic Clamping & Heated Oil Curing
The configured hydraulic press confines the expanding foam while platen circuits control temperature. The supplied reference is 50–60°C; bond quality and cure require material and panel validation.
Технические характеристики
Review the equipment and process parameters for Discontinuous PU Sandwich Panel Molding Line. Final values depend on the material, tooling, production target and agreed configuration.
| Технический параметр | Стандартная спецификация / Значение | Инженерный контекст и проверка |
|---|---|---|
| Целевое применение | Walk-in Cold Rooms, Freezer Doors, Specialty Vehicles | Custom-sized insulated panels with cam-locks |
| Изоляционный материал сердечника | Polyurethane (PUR) / PIR Rigid Foam | In-situ pressurized cavity injection |
| Press Bed Dimensions | 6.5m / 8.5m / 12.0m (Length) × 1.3m – 1.5m (Width) | Accommodates oversized walk-in panels |
| Диапазон толщины панели | 50 mm – 250 mm (Adjustable boundary bars) | Quick manual or motorized gap changeover |
| Press Daylight Configuration | 2+2 Daylights (Optional 3+3 Daylights) | Alternating load/cure work cycle |
| Clamping Force | 150 – 300 Tons (Hydraulic cylinder network) | Resists internal high foaming expansion pressure |
| Диапазон плотности пеноматериала | 40 – 45 кг/м³ | High structural core density |
Оборудование для этого решения
The related project describes a 2+2, 6.5 m workcell and a 15 min reference cadence for two 100 mm panels. Linked product 910 lists a separate 3–10 min single-mold reference and 20–300 mm range; those figures are not the acceptance specification of this project. Core material, mold volume, shot flow and cure must be matched. The batch-panel line and high-pressure metering unit have different functions. Select the actual platen/daylight and material-delivery package together.
Линия периодического производства сэндвич-панелей ПУ | Панели на заказ
Система периодического действия для жёсткого пенополиуретана, предназначенная для изготовления сэндвич-панелей на заказ и панелей особой формы, с гидравлическим прижимом формы, диапазоном толщины 20–1300 мм и очисткой продувкой воздухом без растворителей.
Высоконапорная пенополиуретановая заливочная машина | Сэндвич-панели
Высоконапорная система непрерывного вспенивания для строительных изоляционных сэндвич-панелей с точным смешиванием при большом расходе
Key Discontinuous Engineering Advantages
For Discontinuous PU Sandwich Panel Molding Line, assess material compatibility, process control, equipment interfaces and changeover needs against your production brief.
Configured Dimensions
Length, width and thickness depend on platens and tooling; the reference range is 50–250 mm.
Cam-Lock Positioning
Fixtures locate locks; inspect engagement and keep foam out of mechanisms.
Layout Planning
The related project uses a 450 m² workcell reference; allow site-specific maintenance and handling space.
Batch Shot Control
Metered shots support variable orders; startup, rejects and changeovers remain part of production planning.
Связанные проекты
The related cold-room panel case provides its own workcell and panel references; its floor area and cycle are not universal planning values.
Часто задаваемые вопросы
Сравните производственные маршруты, требования к материалам, конфигурации оборудования и исходные данные проекта.
When is a batch route useful?
How does the alternating press work?
What cycle time is reported?
Can freezer doors be produced?
Can a batch configuration process PIR?
Какие исходные данные нужны для этой конфигурации?
How should the alternating-press production sequence be specified?
Опишите свои производственные задачи
Share the following for this application: Panel/door drawings, thickness and lock mix, formulation, shot mass, mold population, shifts, layout and inspection needs. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


