
حل PU-LFI لمظلات أسطح المركبات الترفيهية كبيرة الحجم
Configure robotic LFI deposition, compression molding and handling for large RV roof and canopy panels.
Automated PU-LFI Solutions for Seamless RV Roof Canopies
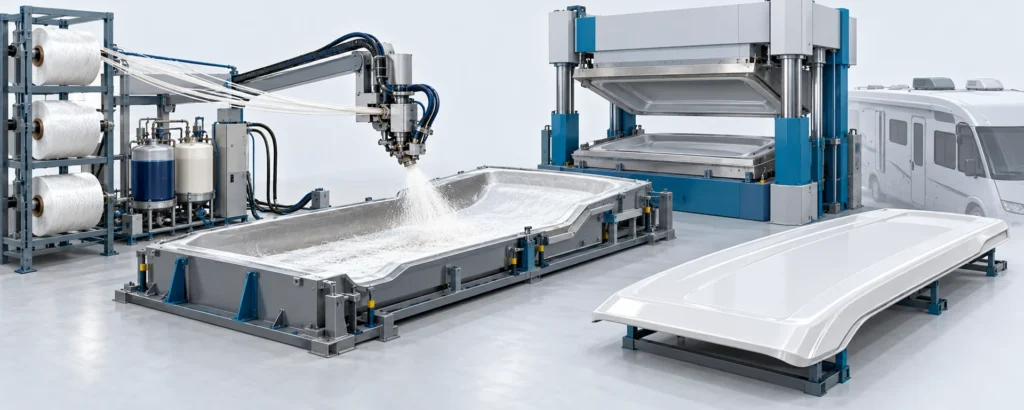
Large LFI panels require coordinated polyurethane delivery, fiber chopping, robotic deposition, mold closing and part handling. The selected reinforcement distribution and tool design govern filling and consolidation. Component weight, dimensional response and water sealing require evidence for the actual panel assembly.
نطاق توريد محدد
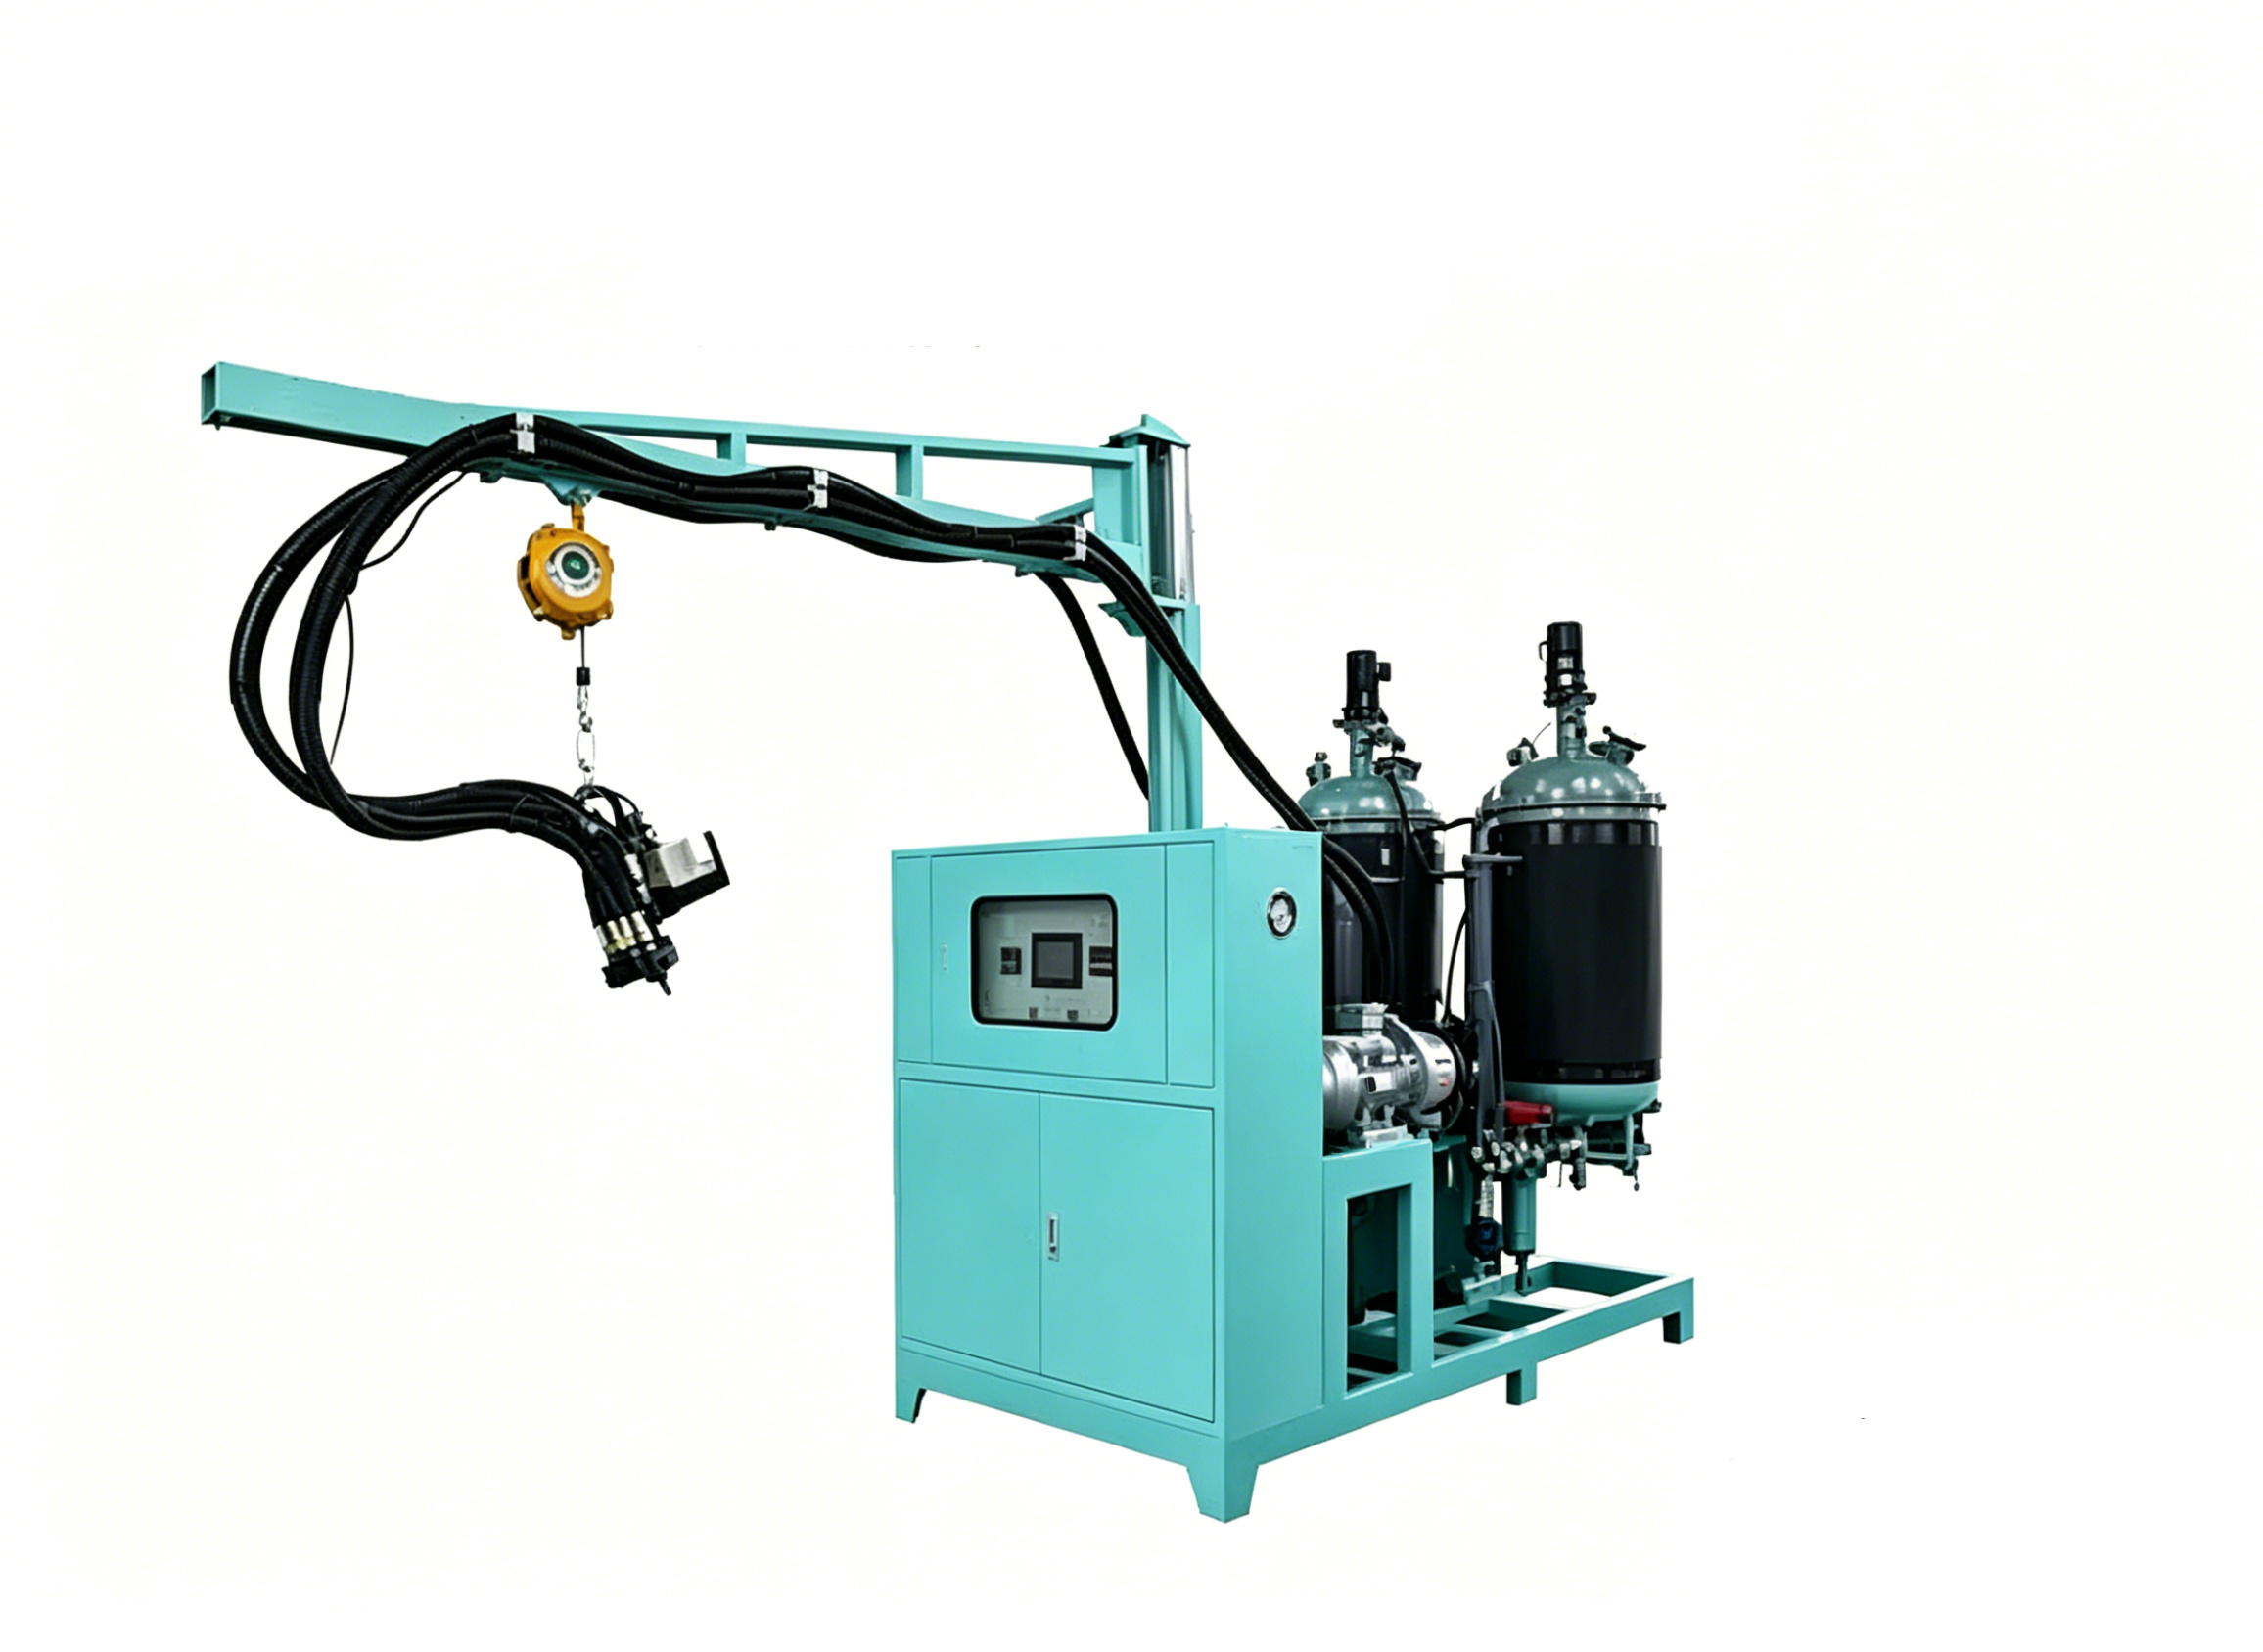
Define the robot/chopper, resin supply, press, tooling, lifting and finishing as separate package items. Panel sealing and vehicle integration are not established by the metering system alone.
المدخلات لاختيار العملية
Panel CAD, fiber and resin data, content basis, mold/press envelope, lifting plan and assembly sealing requirements.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Define the robot/chopper, resin supply, press, tooling, lifting and finishing as separate package items. Panel sealing and vehicle integration are not established by the metering system alone.
Large-Scale RV Roof Canopy PU-LFI Workflow
Define the panel construction → Prepare and deposit the material → Close, consolidate and cure → Handle and qualify the panel. Define preparation, filling, cure and output timing separately for the selected configuration.
Define the panel construction
Review geometry, reinforcement, inserts and interfaces with the RV body.
Prepare and deposit the material
Coordinate resin delivery and chopped fiber with the programmed deposition pattern.
الإغلاق والدمج والمعالجة
Validate transfer time, mold motion and the material-specific thermal sequence.
المواصفات الهندسية والطاقة الإنتاجية
مراجع التكوين الحالي والاختبار. تُعد إعدادات المعدات ونتائج المواد ونتائج التجميع النهائي منفصلة؛ ويُطبَّق كل قيمة فقط على التكوين والظروف الموثقة الخاصة بها.
| المعلمة الفنية | المواصفة القياسية / القيمة | السياق الهندسي & التحقق |
|---|---|---|
| التطبيق المستهدف | Large RV Roof Canopies, Commercial Vehicle Panels | Oversized structural exterior body components |
| مصفوفة المواد | Polyurethane Thermoset Resin + Chopped Glass Roving | High-stiffness isotropic composite system |
| Fiber Chopping Length | 12.5 mm – 100 mm (Programmable) | Continuous roving in-line cutter |
| Fiber Volume Fraction (FVF) | Up to 50% | High-density reinforcement capabilities |
| قدرة إخراج قياس الجرعات | 30 – 80 كغ/دقيقة (قابلة للتخصيص) | مضخات مكبسية محورية بمحرك سيرفو مع قفل النسبة |
| نطاق درجة حرارة القالب | 65°C – 85°C | Multi-zone dynamic water/oil TCU regulation |
| زمن دورة نزع القالب | 200 – 280 seconds (Standard 240 s) | Slashes manual lay-up times from 45+ minutes |
| Coefficient of Thermal Expansion | ~25×10⁻⁶ /K | Prevents buckling under outdoor thermal swings |
| نطاق التوريد | Turnkey (LFI Dosing Skid, Robot, TCU + Optional Press/Tooling) | Complete workcell delivery or retrofit to existing press |
تُختار مراجع المعدات وفق عمليتها الموثّقة. القياس الرئيسي للجرعات والإمداد المساعد والمسارات البديلة ليست حزمة قياسية واحدة.
ضوابط العملية وفحوص التطبيق
قيّم هذه الوظائف باستخدام المادة والتجهيزات القالبية الموجزة الإنتاجية المختارة. تتطلب نتائج الأجزاء النهائية أدلة قبول خاصة بها.
Large-panel coordination
Match deposition reach, press opening and handling clearances to the actual mold.
Defined reinforcement basis
Specify fiber length and whether content is stated by mass or volume.
Assembly-specific comparison
Evaluate weight and weather sealing against a stated panel design and baseline.
مشاريع ذات صلة
هذه مراجع تطبيقية ذات صلة. قارن المادة الفعلية والعملية والوحدات المسلّمة؛ فأرقام المشاريع المبلَّغ عنها ليست نتائج قبول لخط آخر.
الأسئلة الشائعة
أسئلة هندسية وشرائية حول مسار إنتاج البولي يوريثان هذا.
Does an LFI process eliminate water leakage?
Can the quoted weight and cycle apply to another roof design?
ما المعلومات المطلوبة لإعداد تكوين أولي؟
أرسل أهداف إنتاجك
Share the following with your production brief: Panel CAD, fiber and resin data, content basis, mold/press envelope, lifting plan and assembly sealing requirements. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


