La mayoría de los fallos en suelas de doble densidad no se originan en un sistema de poliuretano defectuoso. Se originan en una línea que trata dos perfiles de reacción diferentes como si fueran uno solo. Una suela exterior densa y resistente a la abrasión y una entresuela microcelular amortiguadora tienen viscosidades, velocidades de crecimiento y ventanas de desmoldeo diferentes. Procesar ambas en la misma máquina ahorra espacio en la planta, pero también significa que una pequeña deriva en la dosificación puede hacer que la línea pase de una pieza limpia de dos capas a una pieza que supera la inspección visual pero falla tras el montaje final.
Este artículo recorre la lógica de producción: qué significa doble densidad, cómo funciona la secuencia de vertido, los controles que mantienen distintas las dos capas y las comprobaciones que detectan la deslaminación o la deriva de dureza antes de que la primera pieza llegue al cliente.
Qué significa «doble densidad» en una suela de poliuretano
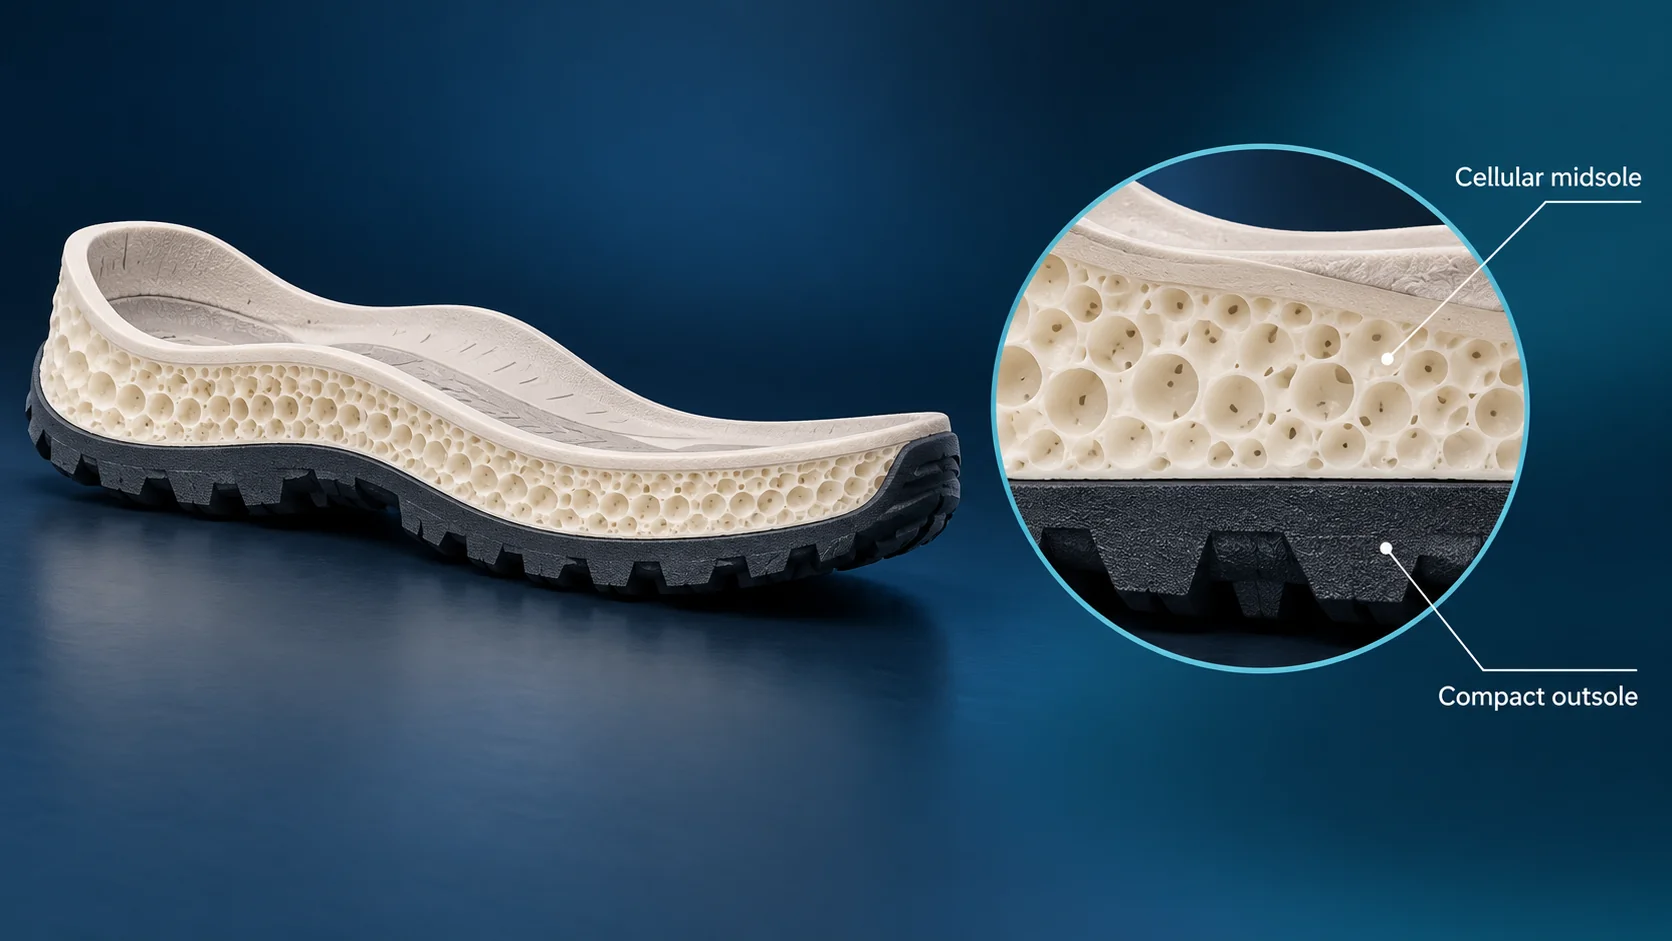
Dual-density is not two colors or two hardnesses applied as an afterthought. It is two polyurethane formulations poured in sequence into the same mold cycle. The outsole is normally a compact or low-foam elastomer with a higher Shore value, while the midsole is a microcellular foam with lower apparent density and greater energy absorption. The difference comes from chain extender selection, blowing agent concentration, and component ratio, not from a simple pigment change.
The functional split is measured with two separate methods. Hardness is determined by durometer testing according to ISO 868 [1], while apparent density is determined according to ISO 845 [2]. A useful specification therefore records both values for each layer: a harder, denser outsole and a softer, lower-density midsole. When only hardness is specified, density can drift and still produce a part that feels correct in the hand.
The functional split is a hardness and density decision, not just a mold-design decision. Dureza Shore A frente a Shore D en poliuretano covers when Shore A and Shore D values matter for layered polyurethane parts that work hard on the surface and absorb energy underneath.
El diseño de dos capas que hace posible la doble densidad
The outsole layer earns its place through cut resistance, slip resistance, and abrasion performance. In rubbery polyurethane, abrasion resistance is often evaluated using ISO 4649 [3], and the result depends on both formulation and cure. The midsole layer earns its place through cushioning and fatigue resistance. If the midsole is too dense, the shoe becomes stiff; if it is too soft, the part collapses under repeated load.
Because the two layers must bond during the pour, the interface design matters as much as the formulation. A wet-on-wet sequence gives a better bond than dry assembly, but it also requires the first layer to reach the right gel state before the second shot arrives. Too early, and the layers mix; too late, and they form a weak boundary.
Cómo se vierte la suela, paso a paso
The pour sequence depends on whether the line is direct-on-upper or sole-only, but the core logic is the same.
- Mold preparation — The mold is preheated and a release agent is applied. Shanks, inserts, or pre-molded components are loaded if the design calls for them.
- First shot — The first formulation is metered into the cavity. Shot weight is calculated from cavity volume and target density, not from a fixed timer.
- Second shot and mold movement — A rotary or slide table moves the mold to the second head, or the same head switches to the second formulation after a purge cycle.
- Cure y desmolde — The part cures under heat, then releases cleanly enough to hold dimension without deformation.
A wrong shot weight changes density before any other process variable can compensate. If the first shot is light, the midsole may be too soft; if it is heavy, the outsole may become thicker and heavier than the specification.
A wrong shot weight changes density before any other process variable can compensate. Cómo calcular el peso de dosificación en poliuretano covers the cavity-volume-to-shot-mass calculation that keeps dual-density soles from ending up too heavy or too soft.
Controles de proceso que determinan la consistencia
Proporción de componentes y dosificación
The component ratio is not a coarse setting. A one-percentage-point drift changes more than shot mass; it changes stoichiometry, leaving unreacted isocyanate or polyol and shifting hardness, density, and cure together. Servo metering systems can hold within ±0.3% over their full dynamic range, but the actual performance also depends on pump selection, material temperature, and recirculation pressure.
Equilibrio entre el crecimiento y la gelificación
The midsole depends on a balance between the blowing reaction and the gelling reaction. If the formulation gels too quickly, it cannot fill the cavity. If it gels too slowly, the foam may rise and then collapse before the polymer network is strong enough to hold the cells. The correct balance changes with mold temperature, line speed, and the density of the layer.
Tiempo de desmoldeo y control dimensional
Demold too early and the part may distort after ejection. Demold too late and the line loses productivity for no property gain. The correct demold window is a function of peak exotherm, mold temperature, and the part’s thickest cross-section.
One commissioning case involving functional dual-density insoles shows what happens when these controls line up: moving to dual-density metering modules raised daily output from 3,000 to 12,000 pairs per line, reduced waste from 8% to 1.5%, and brought defects below 1%. The improvement came from metering repeatability and a stored-formula changeover, not from an increase in nominal machine speed.
If you are balancing two viscosities through the same manifold, record the midsole and outsole ratios, the worst-case shot variance, and the two material temperatures. If the numbers do not close, send the midsole and outsole specifications to info@chinahaifeng.com or WhatsApp 86 13566296633 and ask for a balanced-head review before committing to a configuration.
Controles de calidad antes de la primera pieza
A production sample should not be judged by feel alone. The first article needs to answer four questions.
- Is the hardness split correct? Measure the outsole and midsole separately with the appropriate durometer method [1].
- Is the density split correct? Cut the part and measure a specimen from each layer [2].
- Does the outsole meet the required abrasion or safety criteria? For safety footwear, the applicable standard such as ISO 20345 [4] defines the minimum protective performance. Outsole abrasion is evaluated by methods such as ISO 4649 [3].
- Does the layered structure survive flexing and conditioning? ISO 20344 [5] provides test methods for footwear components and whole shoes, including procedures that expose poor interlayer bonding.
Dimensional checks catch what durometer cannot: a midsole that shrank after cure. If the first layer shrinks before the second shot, the mold cavity no longer matches the design and the next shot may overfill or leave voids.
Dimensional checks catch what durometer cannot: a midsole that shrank after cure. Causas de la contracción en la espuma de poliuretano y cómo controlarla covers why microcellular soles lose dimension and the control points that keep the second shot from being thrown off.
Del ensayo a la línea de producción
Before you shortlist a dual-density line, narrow three inputs.
- the Shore A split and density split for the two layers,
- expected daily pairs and cavity count,
- whether the line is direct-on-upper or sole-only.
Send those specifications to info@chinahaifeng.com or WhatsApp 86 13566296633. A metering and mold-flow review is easier to correct during planning than after the first production batch.
Preguntas frecuentes
¿Cuál es la diferencia entre las suelas de doble densidad y las suelas de dos componentes?
Dual-density refers to two polyurethane formulations poured in the same mold cycle. Two-part soles can also be made by bonding a separately molded outsole and midsole. The difference matters because wet-on-wet dual-density production does not rely on a later adhesive bond.
¿Qué poliuretano se utiliza para la suela exterior y la entresuela?
The outsole is usually a compact or low-foam elastomer with higher hardness and better abrasion resistance. The midsole is usually a microcellular foam with lower apparent density and greater cushioning. Both formulations can be adjusted with chain extenders, blowing agents, and polyol selection.
¿Puede una sola máquina verter ambas densidades?
Yes. The machine needs either two independent metering and mixing circuits or a validated purge and switch sequence between shots. The main risk is not the machine capability itself, but repeatability across the changeover and at the boundary between the two layers.
¿Por qué se deslaminan las suelas de doble densidad?
Delamination usually comes from poor interface timing. If the first layer is too wet, the second shot can mix into it; if the first layer is too advanced, the second layer may not bond. Contaminated mold surfaces, incorrect mold temperature, and ratio drift can also contribute.
¿Cómo se controla la densidad en la entresuela?
Density is controlled by shot weight, blowing agent concentration, mold fill ratio, and material temperature. The practical control point is metering accuracy and shot-weight consistency, because the mold cavity volume is fixed once the tool is cut.
Referencias
[1] ISO 868:2003, Plásticos y ebonita — Determinación de la dureza por indentación mediante un durómetro (dureza Shore), Organización Internacional de Normalización, Ginebra, Suiza, 2003.
[2] ISO 845:2006, Plásticos y cauchos celulares — Determinación de la densidad aparente, Organización Internacional de Normalización, Ginebra, Suiza, 2006.
[3] ISO 4649:2021, Caucho, vulcanizado o termoplástico — Determinación de la resistencia a la abrasión mediante un dispositivo de tambor cilíndrico giratorio, International Organization for Standardization, Geneva, Switzerland, 2021.
[4] ISO 20345:2022, Personal protective equipment — Safety footwear, International Organization for Standardization, Geneva, Switzerland, 2022.
[5] ISO 20344:2021, Personal protective equipment — Test methods for footwear, International Organization for Standardization, Geneva, Switzerland, 2021.
Si te interesa, echa un vistazo a estos artículos relacionados:
SRIM explicado: fundamentos del moldeo por inyección reactiva estructural
Medición de la resiliencia de la espuma de poliuretano: guía práctica de ensayo
El papel del tiempo de subida en el espumado de poliuretano
¿Qué es la espuma de poliuretano proyectada? Composición y aplicación
Causas de la contracción en la espuma de poliuretano y cómo controlarla