

إذا كنت تصنع بكرات أو عجلات أو حشوات sealing أو غرابيل تعدين أو وسائد سكك حديدية، فمن المحتمل أنك رأيت أجزاءً توصف بأنها بولي يوريثان مصبوب أو CPU أو إلاستومر مصبوب — وأحيانًا كما لو كانت هذه المصطلحات الثلاثة تعني الشيء نفسه. فهي متقاربة، لكن التمييز بينها مهم عند اختيار عملية إنتاج.
البولي يوريثان المصبوب هو نظام إلاستومر حراري (thermoset) يُصبّ سائلًا. يُخلط بريبوليمر يحتوي على مجموعات أيزوسيانات مع مُصلّب قصير السلسلة، ويُسكب في قالب مفتوح أو مغلق، ويُعالَج بالمعالجة الحرارية عبر تفاعل كيميائي يبني شبكة متشابكة. وبعد المعالجة، لا يمكن إعادة صهر الجزء أو بثقه كما هو الحال مع المواد الحرارية اللدنة.
تشرح هذه المقالة ما هو CPU على مستوى التركيبة، وكيف تعمل عملية الصب فعليًا، وأين تكمن مخاطر الجودة.
ما الذي يعنيه البولي يوريثان المصبوب (CPU) فعليًا
ينتمي CPU إلى عائلة إلاستومرات البولي يوريثان، لكنه يُعرَّف بالكيمياء بقدر ما يُعرَّف بطريقة معالجته. يبدأ النظام الخام سائلًا، ويُصبّ في قالب، ويتصلب عبر التفاعل.
في المسار الأكثر شيوعًا للصب الساخن، تبدأ العملية ببريبوليمر منتهٍ بمجموعات أيزوسيانات. يتفاعل بوليول — غالبًا PTMEG أو PPG أو بوليول بوليستر — مع فائض من TDI أو MDI أو NDI. والنتيجة وسيط قابل للسكب بمحتوى NCO مضبوط.
ثم يُمدَّد ذلك البريبوليمر بسلسلة باستخدام ديول أو ديامين قصير. والخياران الأكثر شيوعًا هما:
- BDO (1,4-بوتانديول) — يُستخدم عادةً في الدرجات المرنة المقاومة للتحلل المائي ذات انتقال الصلابة المنخفض.
- MOCA (4,4′-ميثيلين-بيس(2-كلوروأنيلين) — يُستخدم حيث تكون هناك حاجة إلى صلابة عالية وقوة ومقاومة للتآكل، لكنه يتطلب درجات حرارة معالجة أعلى لأن MOCA صلب في درجة حرارة الغرفة.
تُحدَّد الخصائص النهائية بنسبة المقاطع الصلبة إلى المقاطع اللينة، وكثافة التشابك، ومدى اكتمال الخلط قبل أن تملأ المادة القالب.
ولأن المكونات سائلة عند نقطة الخلط، يمكن صب CPU في مقاطع سميكة، وحول قوالب معدنية، وفي أدوات قد يكون استخدامها غير عملي في القولبة بالحقن. وهذا الحرية في المعالجة هي السبب الرئيسي الذي يجعل المصنّعين يقبلون أوقات الدوران الأطول للصب.
كيف يختلف CPU عن TPU واليوريثان القابل للطحن وRIM
كثيرًا ما يُخلَط بين CPU وTPU، لكن الفرق جوهري.
TPU is a thermoplastic polyurethane. It is supplied as pellets, melted, and processed by injection molding or extrusion. It can be reprocessed, but certain very soft or very hard wear-resistant grades are difficult to make with pellet-based equipment.
CPU is a thermoset. It starts as two liquid components, reacts in the mold, and cannot be remelted. This allows formulation ranges and thick-wall parts that are difficult to achieve with TPU.
Millable polyurethane (MPU) is a rubber-like gum processed on conventional rubber equipment. It is useful, but it does not offer the same pourable, low-pressure mold-filling behavior as CPU.
RIM, meanwhile, is a high-pressure impingement-mixing process. RIM injects reactive liquid into a closed mold at high pressure and is often selected for fast cycle times on moderate-modulus parts. Cast polyurethane typically operates at lower mixing pressure, uses open or lightly closed molds, and tolerates longer gel times. That makes CPU better suited to very thick parts, high-hardness abrasion grades, and large rollers or pads.
عملية الصب خطوة بخطوة
Most CPU quality failures are not caused by bad chemistry. They are caused by temperature, metering, or degassing errors that occur before the material reaches the mold.
1. تحضير البريبوليمر وإزالة الغازات
The prepolymer is heated to a workable viscosity, usually in the range of 30–80°C depending on the system. If the polyol or prepolymer contains dissolved moisture or entrained air, the result is bubbles, pinholing, or inconsistent hardness.
Vacuum degassing is the standard correction. On casting machines used for rollers, seals, and industrial components, degassing capacity commonly reaches -0.095 MPa or lower. Without this step, dissolved gas expands during the exotherm and creates internal pores that cannot be removed after cure.
2. صهر المُعالِج (المصلّب) والتحكم في درجة الحرارة
حدِّد درجات حرارة صهر MOCA وحفظه وتسخين خطوطه وفق صحيفة البيانات الفنية (TDS) / صحيفة بيانات السلامة (SDS) الخاصة بالدرجة الفعلية ووصفة البوليمر الأولي المعتمدة. وتأكد من أن التوصيل يبقى سائلاً بالكامل على امتداد مسار المادة. فنطاق ضبط الآلة الاسمي 90–115°C لا يثبت أن كل درجة من MOCA منصهرة على امتداد هذا النطاق. واضبط BDO والعوامل المصلّدة الأخرى وفق متطلبات موادها الخاصة، في حدود تصنيف المعدات.
This is why separate temperature-controlled tanks matter. A system that controls prepolymer temperature but not curative temperature can still produce batch-to-batch hardness drift.
3. قياس الجرعات والخلط
CPU production uses either 1A1B systems or 2A2B systems. The extra components in 2A2B equipment allow separate feed of two prepolymers or inclusion of color paste and additive tanks.
The critical parameter is dynamic metering accuracy. A deviation of even one percentage point in the prepolymer-to-curative ratio changes stoichiometry, hardness, and residual curative concentration. Modern precision casting equipment targets ±0.3% or better across the rated pouring range.
Mixing head speed is also important. High-shear mixing in the 6,000–12,000 rpm range is typical, but the right speed depends on viscosity and pot life. Too little shear leaves unmixed curative. Too much shear adds heat and shortens the casting window.
4. الصب وملء القوالب
The mixed material is poured into a mold, often with a controlled pouring rate from tens to more than a thousand grams per second depending on part size. For rollers, centrifugal casting may be used to force the material against a rotating shell and build a void-free layer.
Shot weight must match the mold volume precisely. Underfill leaves a short part. Overfill creates flash, seal failures, or mold pressure that moves a core.
Shot weight is the number that connects metering accuracy to mold quality. كيفية حساب وزن القذفة في البولي يوريثان covers the calculation method and the practical corrections for fill volume, gel time, and part weight.
5. الهلام والمعالجة والمعالجة اللاحقة
After pouring, the material gels, then develops strength. Demolding happens when the part has enough green strength to hold its shape.
Post-curing is often required to complete crosslinking and stabilize properties. Without it, hardness, compression set, and heat resistance may look acceptable at demold but drift later in service.
عوامل التحكم في الخصائص: الصلابة والتآكل وقدرة تحمل الأحمال
Cast polyurethane covers a broad durometer range depending on formulation and curative ratio [6]. The same base chemistry can produce a soft cushioning pad or a hard roller, which is why a single vague spec such as “hard polyurethane” is not a purchasing specification.
The table below shows the core properties processors usually test.
| الخاصية | مرجع الاختبار الشائع | Why it matters in CPU selection |
|---|---|---|
| الصلابة | ISO 868 / ASTM D2240 | Part fit, load distribution, wear behavior [1] |
| Tensile strength and elongation | ISO 37 | Resistance to tearing or cracking under tension [2] |
| مقاومة التمزق | ISO 34-1 | Edge splitting in seals, screens, and thin sections [3] |
| فقدان بالمادة بسبب التآكل | ISO 4649 / DIN 53516 | Roller life, mining screens, wheels, and linings [4] |
| التشوه الانضغاطي المتبقي | ISO 815-1 | Sealing force retention and sustained-load behavior [5] |
Hardness is the most misused number in CPU specifications. Shore A and Shore D are different scales using different indenters. A 70 Shore A part is far softer than a 70 Shore D part.
If the durometer scale is assumed rather than specified, the entire application question changes. صلابة Shore A مقابل Shore D في البولي يوريثان covers scale choice, test method, and how hardness relates to abrasion and load-bearing behavior.
Hardness alone also does not guarantee service life. Two compounds can share the same durometer while differing in tear strength, abrasion loss, or compression set. Applications such as mining screens and railway pads require tear and abrasion data, not only a hardness reading.
قرارات المعدات التي تحدد جودة CPU
At line level, CPU quality is less about the nominal output of the machine and more about how tightly the machine controls four things:
- Temperature on both prepolymer and curative sides
- Vacuum degassing before metering
- Dynamic metering accuracy during pour
- Cleaning behavior between shots and color changes
For example, a 2A2B elastomer casting machine may include MOCA/BDO switching, independent temperature control, vacuum degassing to -0.095 MPa, and automatic circulation plus air-purge cleaning. In roller production, the same machine may run a wear-resistant additive tank and pour rates from under 100 g/s to more than 1,000 g/s depending on mold size.
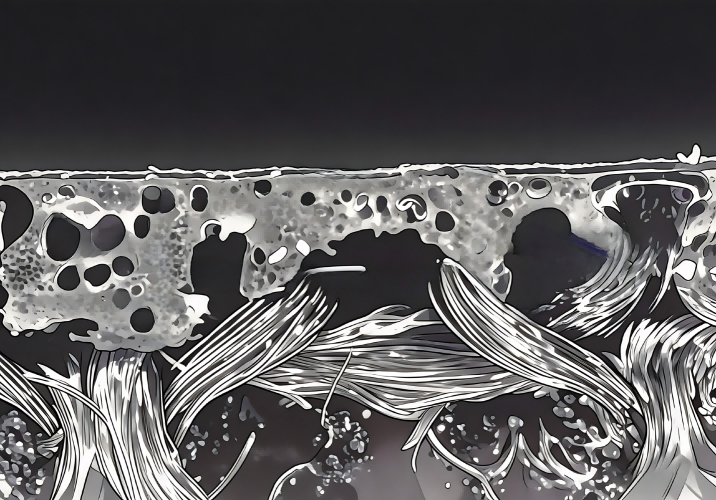
The cleaning system is easy to overlook when buying equipment, but it strongly affects uptime. A mixing head that cannot be purged reliably will build reacted material on internal surfaces, changing backpressure, ratio, and eventually part quality.
Equipment selection should be driven by the actual shot size, cycle time, viscosity, and fill geometry. Large-flow output is useful only if the metering system remains accurate within the operating window.
Equipment selection note: If you are comparing 1A1B and 2A2B casting systems, send the part weight, target hardness, mold volume, and required cycle time to info@chinahaifeng.com or WhatsApp 86 13566296633. The evaluation should focus on ratio tolerance, degassing capacity, and temperature control, not on maximum output printed in a brochure.
تطبيقات يتفوق فيها البولي يوريثان المصبوب
CPU is selected where abrasion, tear strength, load bearing, and thick-section molding matter more than fast cycle time.
Typical applications include:
- Industrial rollers for printing, steel processing, and material conveying
- العجلات والبكرات الصغيرة for high-load floor and warehouse equipment
- Mining screen plates and hydrocyclone linings exposed to wet abrasive slurry
- Hydraulic seals and oil seals requiring elasticity and fluid resistance
- Automotive suspension stops and ball-socket boots
- Railway pads and track components needing outdoor dimensional stability
- Pipe linings for corrosive and high-wear service
Roller casting is the clearest demonstration of how liquid casting, degassing, and controlled gel time combine. The material must wet a bond layer on the core, release air at the surface, gel uniformly, and then cure without shrinkage separation.
Roller production shows the same metering and degassing rules under rotation and core adhesion. كيف تُصنع بكرات البولي يوريثان من الصب حتى المعالجة covers the casting-to-cure sequence and where porosity and adhesion failures come from.
قائمة تحقق عملية للاختيار قبل تحديد مواصفات CPU
Start with the application, not the material.
- Load and deflection: What hardness and modulus does the part actually need?
- Wear mechanism: Sliding, impact, wet abrasive, or cutting wear?
- Temperature: What is the peak operating temperature, including heat from hysteresis?
- Chemical exposure: Oils, water, solvents, or hydrolysis-prone environments?
- Thick sections and metal cores: Does the part require low-pressure mold filling?
- Quality records: Do you need batch traceability, ratio logging, and repeatable demold data?
If the answers point toward thick parts, high abrasion, or tight hardness control, CPU is often the right comparison against TPU, rubber, or RIM.
الانتقال من مواصفات المادة إلى خط صب يلبيها
The weak point in most CPU projects is not the theoretical formula. It is the gap between the datasheet and the casting process.
Before you buy equipment, define the shot weight, the gel time, the degassing requirement, and the temperature tolerance for both components. Then compare machines on those numbers, not on peak output.
Haifeng Polyurethane Machinery supplies metering and casting systems for CPU elastomers, rollers, seals, screen plates, and railway parts. For process scoping, send your part drawing, target hardness, shot weight, and cycle time to:
البريد الإلكتروني: info@chinahaifeng.com
WhatsApp: 86 13566296633
الأسئلة الشائعة
هل البولي يوريثان المصبوب هو نفسه البولي يوريثان الحراري؟
No. Cast polyurethane is a liquid-cast thermoset that cures by chemical crosslinking. Thermoplastic polyurethane is pellet-based, melted, and processed by injection or extrusion. CPU cannot be remelted after cure; TPU can be reprocessed.
ماذا يعني «الصب الساخن» في البولي يوريثان المصبوب؟
Hot-cast usually refers to prepolymer systems processed at elevated temperature, often with a MOCA or diol curative held above room temperature. The term separates these systems from room-temperature-curing “cold-cast” formulations.
ما نطاق الصلابة المتاح في البولي يوريثان المصبوب؟
The range depends on prepolymer type, NCO content, and curative ratio. Cast polyurethane can be formulated from very soft pads to hard engineering grades, so hardness must be specified with the Shore A or Shore D scale, not as a single number.
لماذا يُعدّ إزالة الغازات بالتفريغ مهمًا في صب CPU؟
Dissolved gas, moisture, and entrained air expand during the curing exotherm. Vacuum degassing before metering reduces bubbles, pinholes, and internal porosity that cannot be corrected after the part gels.
كيف ينبغي لي أن أختار بين صب CPU وRIM؟
Use CPU casting when the part is thick, needs very high abrasion resistance, includes metal cores, or requires open-mold pouring and longer gel time. Consider RIM when cycle speed and closed-mold high-pressure injection are more important than extreme hardness or thick-section freedom.
المراجع
[1] ISO 868:2003, اللدائن والمطاط القاسي — تحديد صلابة الانغراز بواسطة مقياس الصلابة (صلابة شور).
[2] ISO 37:2017, Rubber, vulcanized or thermoplastic — Determination of tensile stress-strain properties.
[3] ISO 34-1:2015, المطاط المبركن أو اللدائن الحرارية — تحديد مقاومة التمزق — الجزء 1: عينات الاختبار على شكل بنطال وزاوية وهلال.
[4] ISO 4649:2017, المطاط المبركن أو اللدائن الحرارية — تحديد مقاومة التآكل باستخدام جهاز أسطوانة دوارة.
[5] ISO 815-1:2019, المطاط المبركن أو اللدائن الحرارية — تحديد التشوه الانضغاطي المتبقي — الجزء 1: عند درجات الحرارة المحيطة أو المرتفعة.
[6] Oertel, G., ed., Polyurethane Handbook، الطبعة الثانية، Hanser Publishers، 1994.
إذا كنت مهتمًا، فاطّلع على هذه المقالات ذات الصلة:
صلابة Shore A مقابل Shore D في البولي يوريثان
ما هي رغوة البولي يوريثان شبه الصلبة
Specify PU casting equipment around the part and its working time
PU casting uses a metered reactive mixture to produce a cast polyurethane part. A polyurethane casting machine may deliver a hot-cast or another supplier-approved system through an open pour or into tooling designed for that product. In a quote for a urethane molding machine, specify whether the equipment scope includes degassing, component conditioning, tool heating, mold handling and a post-cure stage. Cast PU rollers and thick seals, for example, may have different fill paths and handling requirements even if they use the same metering principle.
For a PU casting machine trial, use the production grade, smallest and largest pours, and the most demanding tooling. Record ratio and mass, complete fill, cure and surface voids, then test the finished part against its service requirements. Compare roller casting from pouring to cure و three-component PU casting equipment before agreeing the supply boundary.





