

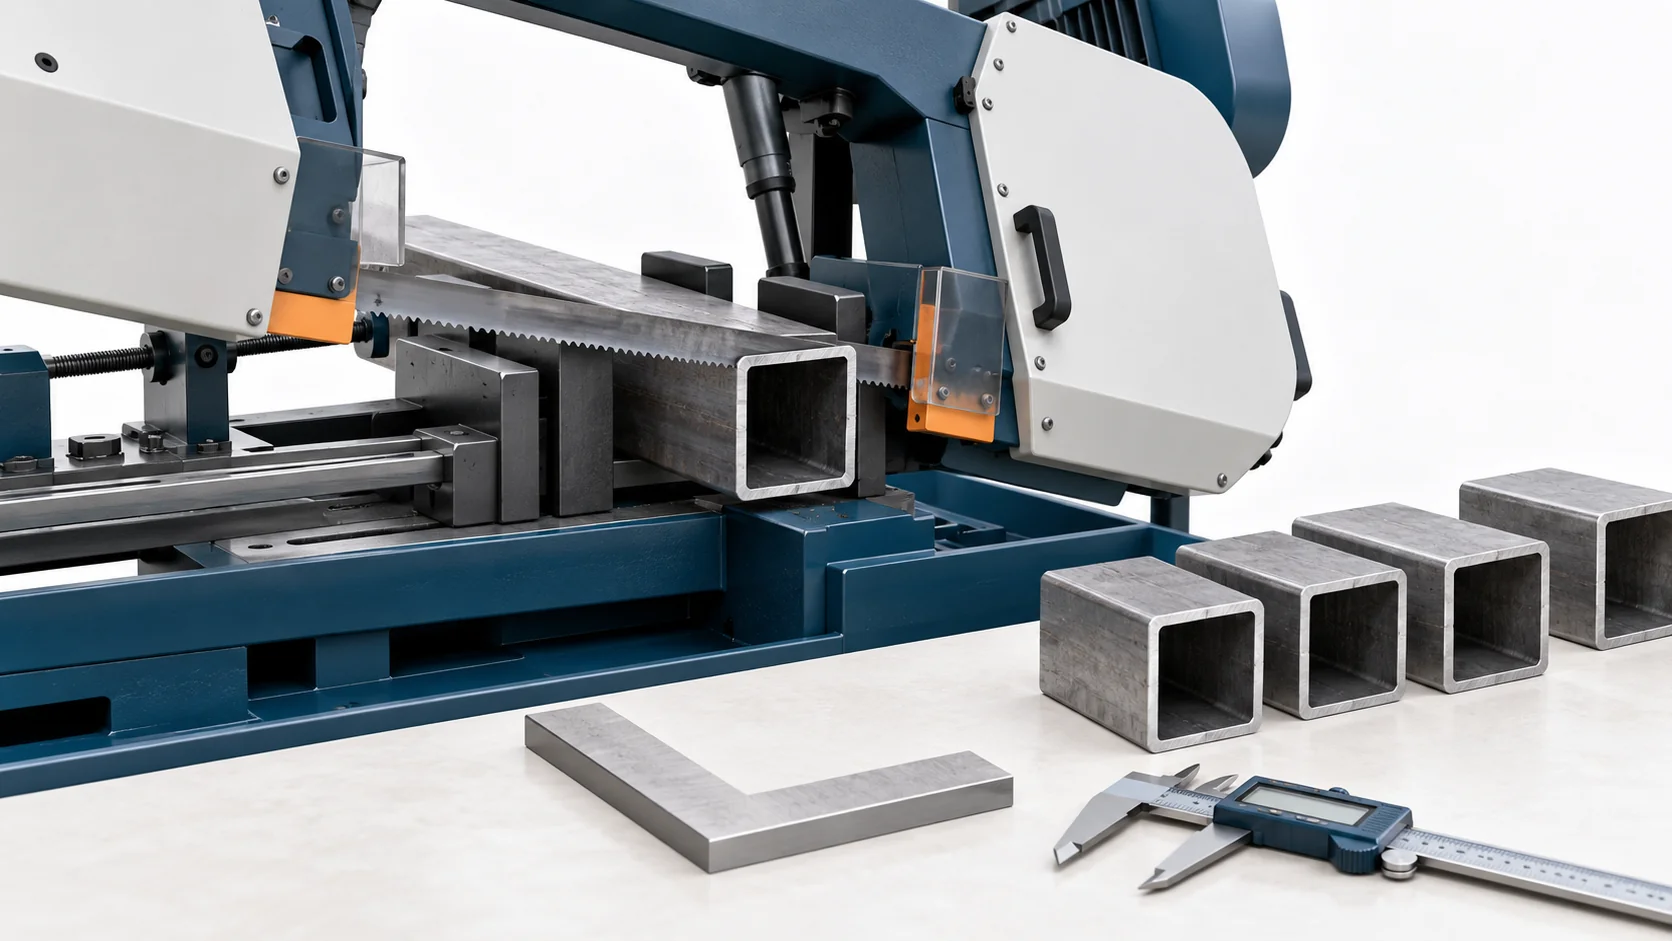
Точность подгонки под сварку полиуретанового оборудования Haifeng закладывается уже на этапе резки заготовок на ленточной пиле. Каждое отклонение перпендикулярности поверхности реза на 0,5°/100 мм может увеличить неравномерность зазора при подгонке под сварку более чем на 0,3 мм и повысить сварочные деформации на 20%–30%, что в итоге выводит плоскостность монтажного основания серводвигательного дозирующего насоса за допуск при финальной сборке. Если перпендикулярность торцов заготовок опор трубопроводов или фланцев превышает 0,2 мм/100 мм, уплотнительные поверхности фланцев после сварки могут перекоситься и снизить долю успешных испытаний резервуара на герметичность (требование Haifeng: отсутствие утечек при 0,02 МПа в течение 30 мин).
Ключевые технологические параметры — краткий обзор:
| Параметр | Стандарт Haifeng | Отраслевой ориентир | Связанный показатель точности |
| Допуск на длину заготовки (L <3000 мм) | ±1,0 мм | ±1,0 мм | Зазор при подгонке под сварку ≤0,5 мм |
| Допуск на длину заготовки (L ≥3000 мм) | ±0,5 мм | ±0,5 мм | Одинаковая длина труб рамы |
| Перпендикулярность поверхности реза (высота ≤200 мм) | ≤0,2 мм/100 мм | ≤0,5° | Контакт при подгонке под сварку |
| Перпендикулярность поверхности реза (высота >200 мм) | ≤0,15 мм/100 мм | ≤0,3° | Совмещение шва обечайки после вальцовки |
| Шероховатость пропиленной поверхности | Ra ≤12,5 мкм | Ra ≤12,5 мкм | Поверхность под сварку без масляных загрязнений |
| Высота заусенца на торце реза | ≤0,1 мм на поверхности под сварку | ≤0,5 мм | Контроль пористости шва/непровара |
| Радиальное биение пильного колеса | ≤0,15 мм | 0,12–0,20 мм | Прямолинейность пропиленной поверхности ≤0,3 мм/м |
| Торцевое биение пильного колеса | ≤0,15 мм | 0,12–0,20 мм | Плоскостность пропиленной поверхности |
| Точность хода направляющих полотна по горизонтали | ≤0,10 мм/100 мм | ≤0,15 мм/100 мм | Перпендикулярность реза ≤0,2 мм/100 мм |
| Точность позиционирования подающей системы | ≤±0,10 мм/500 мм | ≤±0,20 мм/500 мм | Коэффициент вариации длины в партии CV ≤0,3% |
| Повторяемость позиционирования системы подачи | ≤±0,05 мм | ≤±0,10 мм | Стабильные размеры заготовок в партии |
| Натяжение полотна (сталь) | 20–25 Н/мм² | 15–30 Н/мм² | Отклонение полотна ≤0,1 мм/м |
| Скорость резания (углеродистая сталь Q235B/Q345B) | 60–100 м/мин | 50–120 м/мин | Баланс качества реза и производительности |
| Скорость резания (нержавеющая сталь 304/316L) | 30–50 м/мин | 30–60 м/мин | Контроль наклёпа и стойкости инструмента |
| Скорость резания (алюминий 6061/7075) | 200–400 м/мин | 200–500 m/min | Control burrs |
| Feed per tooth (carbon steel) | 0.04–0.08 mm/tooth | 0.04–0.16 mm/tooth | Balance chip shape and cutting force |
| Coolant concentration | 8%–12% emulsion | 5%–15% | Blade life ≥3000 cuts |
| Blanking ambient temperature | 10–40°C | — | Thermal expansion effect ≤0.01 mm/m |
1. Область применения
1.1 Применимые операции
This SOP applies to bandsaw blanking of the following Haifeng polyurethane-equipment components:
| Part to cut | Типичный материал | Typical size | Показатель соответствующего оборудования |
| Frame square tube/rectangular tube | Q235B/Q345B | 40×40–120×120 mm | Frame weld-fit-up gap ≤0.5 mm |
| Tank-shell plate blank | 304/316L | 3–8 mm thick | Tank-shell seam accuracy after rolling |
| Pipeline-support sections | Q235B/304 | Angle/channel/flat bar | Accurate pipeline fixing-point position |
| Round-bar flange blanks | 304/316L/45# | Φ50–Φ300 mm | Flange sealing-face flatness ≤0.02 mm |
| Pouring-platform frame sections | Q235B/Q345B | Square/rectangular tube | Pouring-path repeatability ±0.05 mm |
| Electrical-cabinet brackets | Q235B/cold-rolled sheet | Angle/flat bar | Alignment of cabinet mounting holes |
| Mixing-head mounting-base blanks | Alloy steel/45# | Φ80–Φ200 mm | Mixing-head alignment ≤0.03 mm |
2. Подготовка к работе и проверка точности станка
2.1 Проверка технической документации и материала
| № | Пункт | Требование к точности | Критерий приёмки |
| 1 | Blanking list | Material, size, quantity, and cut length specified | Matches BOM |
| 2 | Сертификат на материал | Марка соответствует чертежу | Chemical-composition and mechanical-property reports included |
| 3 | Visual material inspection | No bending, twisting, or rust | Bend ≤2 mm/m; twist ≤1°/m |
| 4 | Actual material dimensions | Section-size deviation ≤±0.5 mm | Measure with vernier caliper and record |
| 5 | Blanking process card | Saw parameters, clamping plan, and inspection requirements | Includes weld-shrinkage allowance |
2.2 Проверка точности станка
Calibrate the bandsaw regularly under the machine calibration procedure; calibration error for critical parameters must be ≤0.05 mm. Perform accuracy inspection according to JB/T 15187.1-2025, “CNC Horizontal Bandsawing Machines—Part 1: Accuracy Inspection,” and JB/T 4318.1-2026, “Horizontal Bandsawing Machines—Part 1: Accuracy Inspection.”
| Параметр калибровки | Стандарт Haifeng | Периодичность | Средство контроля |
| Radial runout of drive/idler saw wheels | ≤0,15 мм | Ежеквартально | Dial indicator and magnetic base |
| Face runout of drive/idler saw wheels | ≤0,15 мм | Ежеквартально | Индикатор часового типа |
| Плоскостность рабочего стола | ≤0.10 mm/500 mm | Ежеквартально | Precision level/straightedge and feeler gauge |
| Точность хода направляющих полотна по горизонтали | ≤0,10 мм/100 мм | Ежемесячно | Dial indicator and master test piece |
| Blade-position error from combined guide errors | ≤0,15 мм | Ежемесячно | Indicator |
| Точность позиционирования подающей системы | ≤±0,10 мм/500 мм | Ежемесячно | Laser distance meter/master gauge block |
| Повторяемость позиционирования системы подачи | ≤±0,05 мм | Ежемесячно | Dial indicator and master test piece |
| Saw-frame travel parallelism to guideway | ≤0.10 mm/1000 mm | Каждые 6 месяцев | Dial indicator and straightedge |
| Blade perpendicularity to worktable | ≤0.1 mm/100 mm | Ежемесячно | Square and feeler gauge |
2.3 Проверка точности полотна и оснастки
| Tool/component | Требование к точности | Периодичность | Средство контроля |
| Blade tooth pitch | Match workpiece section size | Each blade batch | Tooth-pitch gauge |
| Blade tooth set | Symmetric left/right; deviation ≤0.05 mm | Each blade batch | Caliper |
| Blade wear | Tooth-tip wear ≤0.10 mm | Каждую смену | Magnifier/touch |
| Blade tension | 20–25 N/mm² (steel) | Каждую смену | Tension tester |
| Guide-block clearance | 0.05–0.10 mm | Weekly | Feeler gauge |
| Guide-wheel wear | ≤0.10 mm | Ежемесячно | Индикатор часового типа |
| Feed-vise jaw parallelism | ≤0.05 mm/100 mm | Ежемесячно | Индикатор часового типа |
3. Структурированный рабочий процесс отрезки заготовок ленточной пилой
3.1 Подготовка перед сменой и прогрев
3.1.1 Проверка состояния станка
Switch on the main power, then start the saw and CNC system. After the self-check completes without alarms, home the saw frame. Check the following:
1. Blade tension meets the set value (20–25 N/mm² for steel; reduce as appropriate for aluminum).
2. Coolant level and concentration are correct (8%–12% for stainless; 5%–8% for carbon steel).
3. Hydraulic pressure is stable within machine requirements (typically 4–6 MPa).
4. Feed-vise and clamping-vise jaws are clean and within wear limits.
3.1.2 Bandsaw no-load warm-up
Warm up the saw unloaded before precision blanking (such as flange blanks and mixing-head mounting-base blanks):
| Blanking type | Warm-up time | Способ |
| General accuracy (length tolerance ±1.0 mm) | ≥5 min | Run blade unloaded and cycle saw frame up/down |
| Precision (length tolerance ±0.5 mm) | ≥10 мин | Run blade at cutting speed and traverse feed system full stroke |
| High accuracy (length tolerance ±0.3 mm) | ≥15 min | Simulate cutting conditions and monitor hydraulic-oil temperature |
3.2 Зажим заготовки и установление баз
3.2.1 Control clamping accuracy
Secure clamping directly determines blank length and end-face perpendicularity. Before clamping, clean vise jaws and workpiece locating faces and remove burrs and oil.
| Clamping method | Suitable workpiece | Locating accuracy | Notes |
| Hydraulic vise (standard jaws) | Square/round bar, rectangular tube | ≤0.10 mm | Jaws must be perpendicular to blade |
| Dedicated V-jaws | Round bar, pipe | ≤0,05 мм | V face must be perpendicular to blade |
| Multi-part fixture | Small sections in batch | ≤0.10 mm | Use spacers to locate each piece |
| Dedicated locating fixture | Flange blanks, mixing-head mounting bases | ≤0,05 мм | Check locating-pin wear regularly |
3.2.2 Set and locate blank length
| Locating method | Accuracy | Применение |
| Manual stop | ±0,5 мм | Single pieces/small batches |
| Digital scale | ±0.1 mm | Batch blanking |
| Servo feed system | ±0.05 mm | High-accuracy batch work (flange blanks) |
| Laser positioning | ±0.03 mm | Precision blanks (mixing-head mounting base) |
3.3 Параметры резки и контроль точности
3.3.1 Material groups and sawing parameters
Materials cut for Haifeng equipment mainly include carbon steel (Q235B/Q345B), stainless steel (304/316L), aluminum alloy (6061/7075), and alloy steel (45#/40Cr).
Recommended parameters for Q235B/Q345B carbon steel:
| Workpiece section (mm) | Cutting speed Vc (m/min) | Feed per tooth (mm/tooth) | Blade pitch (mm) | Blade tension (N/mm²) |
| ≤50 | 80–100 | 0.06–0.08 | 4–6 | 20–25 |
| 50–100 | 70–90 | 0.05–0.07 | 6–8 | 20–25 |
| 100–200 | 60–80 | 0.04–0.06 | 8–10 | 22–25 |
| >200 | 50–70 | 0.04–0.05 | 10–12 | 22–25 |
Recommended parameters for 304/316L stainless steel:
| Workpiece section (mm) | Cutting speed Vc (m/min) | Feed per tooth (mm/tooth) | Blade pitch (mm) | Blade tension (N/mm²) |
| ≤50 | 40–50 | 0.04–0.06 | 4–6 | 22–25 |
| 50–100 | 35–45 | 0.03–0.05 | 6–8 | 22–25 |
| 100–200 | 30–40 | 0.03–0.04 | 8–10 | 25–28 |
| >200 | 30–35 | 0.02–0.03 | 10–12 | 25–28 |
Austenitic stainless steel (304/316L) work-hardens strongly, so its cutting speed must be substantially lower than for carbon steel. Because molybdenum makes 316L more prone to work hardening than 304, reduce speed further and increase tension as appropriate to prevent blade deflection. Chip shape and color indicate whether speed and feed are suitable: white, curled chips are generally desirable; short, hard blue chips indicate low speed and high feed; thin, loose or powdery white chips indicate excessive speed.
Recommended parameters for 6061/7075 aluminum alloy:
| Workpiece section (mm) | Cutting speed Vc (m/min) | Feed per tooth (mm/tooth) | Blade pitch (mm) | Blade tension (N/mm²) |
| ≤50 | 300–400 | 0.08–0.12 | 3–5 | 15–20 |
| 50–100 | 250–350 | 0.06–0.10 | 5–7 | 15–20 |
| 100–200 | 200–300 | 0.05–0.08 | 7–9 | 18–22 |
3.3.2 Inspect sawing accuracy
| Inspection item | Стандарт Haifeng | Средство контроля | Периодичность |
| Blank length deviation (L <3000 mm) | ±1,0 мм | Tape measure/caliper | 100% inspection |
| Blank length deviation (L ≥3000 mm) | ±0,5 мм | Tape measure | 100% inspection |
| End-face perpendicularity (height ≤200 mm) | ≤0,2 мм/100 мм | Square and feeler gauge | First article and sampling |
| End-face perpendicularity (height >200 mm) | ≤0,15 мм/100 мм | Square and feeler gauge | First article and sampling |
| Sawn-face straightness | ≤0.3 mm/m | Straightedge and feeler gauge | First article each batch |
| Surface roughness | Ra ≤12,5 мкм | Roughness tester/comparator coupon | Sampling |
| Burr height on weld-fit-up face | ≤0.1 mm | Magnifier/touch | 100% inspection |
3.4 Удаление заусенцев и обработка торцов
3.4.1 Deburring requirements
Burrs on sheet-metal mating faces and weld-fit-up faces must be ≤0.1 mm. After deburring, use a chamfering tool or belt sander to create a 0.1–0.3 mm × 45° chamfer.
3.4.2 Maintain accuracy after end-face finishing
Recheck end-face perpendicularity after deburring to confirm that finishing did not introduce deviation. For precision blanks (flange blanks and mixing-head mounting-base blanks), recheck perpendicularity with a CMM or precision square.
4. Ключевые параметры точности отрезки заготовок ленточной пилой
| № | Category | Параметр | Стандарт Haifeng | Средство контроля | Периодичность |
| 1 | Machine accuracy | Радиальное биение пильного колеса | ≤0,15 мм | Индикатор часового типа | Ежеквартально |
| 2 | Machine accuracy | Торцевое биение пильного колеса | ≤0,15 мм | Индикатор часового типа | Ежеквартально |
| 3 | Machine accuracy | Плоскостность рабочего стола | ≤0.10 mm/500 mm | Precision level | Ежеквартально |
| 4 | Machine accuracy | Точность хода направляющих полотна по горизонтали | ≤0,10 мм/100 мм | Dial indicator/master test piece | Ежемесячно |
| 5 | Machine accuracy | Feed positioning accuracy | ≤±0,10 мм/500 мм | Laser distance meter | Ежемесячно |
| 6 | Machine accuracy | Feed repeat positioning | ≤±0,05 мм | Dial indicator/master test piece | Ежемесячно |
| 7 | Cutting parameter | Натяжение полотна (сталь) | 20–25 Н/мм² | Tension tester | Каждую смену |
| 8 | Cutting parameter | Carbon-steel cutting speed | 60–100 м/мин | Tachometer | Каждую смену |
| 9 | Cutting parameter | Скорость резания 316L | 30–50 м/мин | Tachometer | Каждую смену |
| 10 | Blank accuracy | Length deviation (L <3000 mm) | ±1,0 мм | Tape measure/caliper | 100% inspection |
| 11 | Blank accuracy | Length deviation (L ≥3000 mm) | ±0,5 мм | Tape measure | 100% inspection |
| 12 | Blank accuracy | End-face perpendicularity (height ≤200 mm) | ≤0,2 мм/100 мм | Square/feeler gauge | First article + sampling |
| 13 | Blank accuracy | End-face perpendicularity (height >200 mm) | ≤0,15 мм/100 мм | Square/feeler gauge | First article + sampling |
| 14 | Blank accuracy | Sawn-face straightness | ≤0.3 mm/m | Straightedge/feeler gauge | First article |
| 15 | Surface quality | Surface roughness | Ra ≤12,5 мкм | Roughness tester/coupon | Sampling |
| 16 | Surface quality | Burr height on weld-fit-up face | ≤0.1 mm | Magnifier | 100% inspection |
| 17 | Process allowance | Transverse weld-shrinkage allowance | 0.5 mm per seam | Review blanking list | 100% inspection |
| 18 | Process allowance | Longitudinal weld-shrinkage allowance | 2–3 mm/m | Review blanking list | 100% inspection |
| 19 | Environment | Blanking temperature | 10–40°C | Temperature/humidity logger | Continuous |
5. Типичные проблемы и технологические ошибки
5.1 Отклонение полотна вызывает чрезмерную погрешность перпендикулярности торца
Symptom: Cut-face perpendicularity to the workpiece axis exceeds 0.2 mm/100 mm; weld-fit-up gaps are uneven and the frame bends after welding.
Root cause: Blade deflection is the main cause of excessive end-face perpendicularity error. Causes include insufficient blade tension (below 80% of set value), excessive guide-block clearance (above 0.10 mm), worn guide wheels or bearing movement, excessive feed, and a blade tooth pitch that does not suit the section. The guide-angle assembly may also hold the blade out of perpendicular to the worktable.
Corrective actions:
1. Measure blade tension every shift; keep it at 20–25 N/mm².
2. Check guide-block clearance weekly; replace blocks if clearance is outside 0.05–0.10 mm.
3. Check guide-wheel wear monthly; replace wheels if wear exceeds 0.10 mm.
4. After blade installation, adjust guide-angle bolts until the blade is square to the table; verify with a square.
5. Select blade pitch to match the workpiece section (approximately 1/10–1/15 of section size).
5.2 Разрыв полотна прерывает резку и создаёт риск для безопасности
Symptom: The blade suddenly breaks during cutting, leaves a mark on the workpiece, and requires reclamping and recutting.
Root cause: Causes include excessive tension (above 120% of set value), excessive cutting speed and overheating, excessive feed that overloads teeth, incorrect tooth pitch, or inadequate coolant/lubrication that causes chips to adhere to teeth. Frequent blade breakage, angled cut faces, excessive burrs, and rapid blade wear are common shop-floor problems.
Corrective actions:
1. Follow the blade-tension standard strictly (20–25 N/mm² for steel); keep deviation within ±5% of the set value.
2. Select cutting speed by material (carbon steel 60–100 m/min; 316L 30–50 m/min).
3. Adjust feed in real time based on chip shape; white curled chips indicate a desirable condition.
4. Keep coolant concentration and flow within limits, and direct coolant accurately at the kerf.
5. Before use, inspect tooth-tip wear (≤0.10 mm) and tooth-set symmetry.
5.3 Накопленное отклонение длины заготовки затрудняет подгонку под сварку
Symptom: Length variation in batch-cut square stock increases, lengths do not match during fit-up, and extensive rework is needed.
Root cause: Feed positioning accuracy or repeatability has deteriorated. Worn feed-vise jaws, a worn feed screw, or encoder-signal interference can cause positioning error. Changing friction between the workpiece and support rack can also make actual feed length differ from the set value.
Corrective actions:
1. Check feed positioning monthly with a laser distance meter; maintain ≤±0.10 mm/500 mm.
2. Check repeat positioning monthly; maintain ≤±0.05 mm.
3. Replace feed-vise jaws if wear exceeds 0.05 mm.
4. Remove chips and debris from support racks before feeding to keep resistance stable.
5. For batch work, sample-check length every 20 pieces and recalibrate immediately if a drift trend appears.
5.4 Наклёп при резке заготовок из нержавеющей стали вызывает аномальный износ полотна
Symptom: Blade life when cutting 316L drops sharply (below 500 cuts), cutting force rises, and a hardened layer and burrs appear on the cut face.
Root cause: Austenitic stainless steel (304/316L) work-hardens strongly; surface hardness during sawing can increase from HB 150 to above HB 300. Excessive speed or insufficient feed makes blade teeth repeatedly cut the hardened layer and accelerates wear. Molybdenum makes 316L more prone to work hardening than 304.
Corrective actions:
1. Keep 316L cutting speed at 30–50 m/min; do not use carbon-steel speeds.
2. Use a “high-feed, low-speed” strategy so teeth always cut below the hardened layer.
3. Increase blade tension as appropriate (25–28 N/mm²) to resist deflection.
4. Use an M42 bi-metal blade or carbide-tipped blade for better wear resistance.
5. Ensure coolant fully covers the kerf to prevent heat buildup from worsening work hardening.
5.5 Неправильная концентрация СОЖ вызывает налипание стружки и шероховатость поверхностей реза
Symptom: Chips adhere to the cut face, burrs increase, roughness exceeds Ra 12.5 μm, and chip spaces between teeth become blocked.
Root cause: Coolant concentration is outside the recommended range. Stainless-steel machining requires adequate lubrication and cooling. Emulsion below 8% provides insufficient lubrication and encourages chip adhesion; above 15%, cooling declines, foam increases, and chip evacuation worsens. Incorrect concentration is a common cause of chip adhesion and rough sawn faces.
Corrective actions:
1. Use 8%–12% emulsion for stainless steel and 5%–8% for carbon steel.
2. Measure and record coolant concentration with a refractometer every shift.
3. Regularly remove chips and floating oil from the coolant tank to prevent bacterial growth.
4. Aim coolant nozzles at the kerf for effective cooling and chip flushing.
5.6 Износ направляющих блоков постепенно ухудшает перпендикулярность реза
Symptom: After the saw has been used for a period, end-face perpendicularity gradually moves out of tolerance and the cut becomes angled.
Root cause: Guide blocks maintain blade-position accuracy. Wear increases clearance between the blocks and blade, allowing cutting forces to push the blade sideways and tilt the cut face. Guide-block wear is one of the most common causes of bandsaw accuracy loss. Radial movement in saw-wheel bearings and worn guide-wheel grooves can also affect perpendicularity.
Corrective actions:
1. Check guide-block clearance weekly; replace blocks if it is outside 0.05–0.10 mm.
2. Use wear-resistant alloy guide blocks; do not substitute ordinary carbon steel.
3. Check saw-wheel bearing movement monthly; replace bearings if movement exceeds 0.05 mm.
4. Check guide-wheel grooves monthly; replace a wheel if a pronounced groove has formed.
5. Keep a guide-block replacement log with service intervals and sawing-accuracy measurements.





