
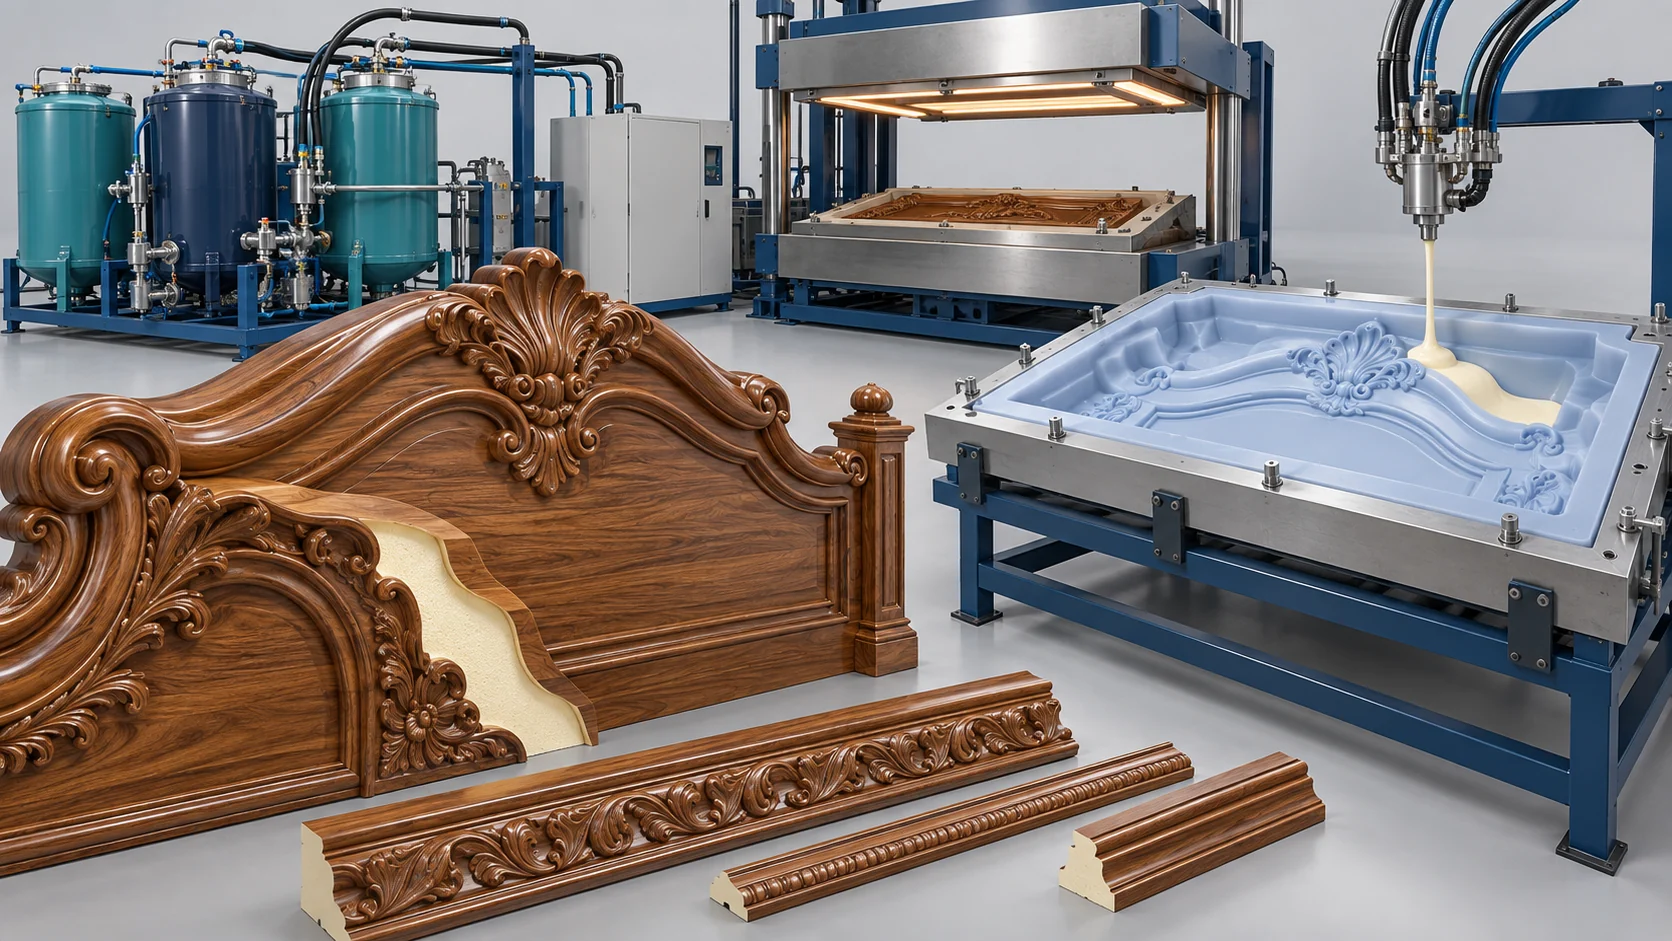
Solución de moldeo de imitación de madera de PU rígido
Plan rigid PU imitation-wood moldings around the master pattern, mold, finish and fastening requirements.
Structural Rigid PU Solutions for Intricate Imitation Wood Carvings
Imitation-wood molding reproduces a selected master pattern through material delivery, expansion and cure in a suitable mold. Part density and surface finish are chosen for the design; they do not reproduce every structural property of a named wood species. Moisture response, cracking and fastener holding must be assessed on the molded part.
Alcance de suministro definido
Specify material delivery, mold type, release, cure and finishing interfaces. A carved-part project does not establish a fixed labor saving or universal woodworking compatibility.
Insumos para la selección del proceso
Master pattern/CAD, relief and undercuts, part thickness, finish, fastener locations, batch mix and output.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Specify material delivery, mold type, release, cure and finishing interfaces. A carved-part project does not establish a fixed labor saving or universal woodworking compatibility.
Rigid PU Imitation Wood Molding Workflow
Review the pattern and finish → Prepare material and mold → Fill and cure → Finish and inspect. Define preparation, filling, cure and output timing separately for the selected configuration.
Review the pattern and finish
Identify fine relief, undercuts, parting lines and the coating or stain system.
Prepare material and mold
Confirm the formulation, mold construction and release procedure.
Rellenar y curar
Validate the shot and thermal sequence against the section thickness.
Especificaciones técnicas
Configuración existente y referencias de ensayo. Los ajustes del equipo, los resultados del material y los resultados del conjunto terminado son independientes; aplique cada valor solo a su configuración y condiciones documentadas.
| Parámetro técnico | Especificación estándar / Valor | Contexto de ingeniería y verificación |
|---|---|---|
| Aplicación objetivo | Bed Headboard Carvings, Ornate Wall Panels, Mirror Frames | High-density architectural furniture millwork |
| Matriz del material | High-Density Structural Rigid Polyurethane Foam | Fast-curing microcellular imitation wood |
| Part Density Range | 250 – 600 kg/m³ (Customizable per wood species) | Replicates pine, oak, mahogany, or teak |
| Screw/Nail Holding Force | Confirm against the selected fastener and specimen | Specify the fastener withdrawal method and source report |
| Capacidad de dosificación | 30 – 80 kg/min (Customizable) | High-volume fast shot injection |
| Tiempo de ciclo de desmoldeo | 4 – 8 minutes (Thickness dependent) | Rapid curing for heavy-section castings |
| Moisture Absorption | <0.5% (24-hour water immersion) | Verify dimensional stability and moisture response for the intended conditions |
Controles de proceso y verificaciones de aplicación
Evalúe estas funciones con el material, los moldes y el resumen de producción seleccionados. Los resultados de las piezas acabadas requieren su propia evidencia de aceptación.
Pattern-to-tool planning
Select mold materials and release strategy for the actual carving and undercuts.
Part-level stability checks
Evaluate moisture, dimensional response and cracking under the intended conditions.
Defined finishing and fastening
Test the coating and fastener arrangement on representative moldings.
Proyectos relacionados
Estas son referencias de aplicación relacionadas. Compare el material, el proceso y los módulos entregados reales; las cifras de proyecto reportadas no son resultados de aceptación para otra línea.
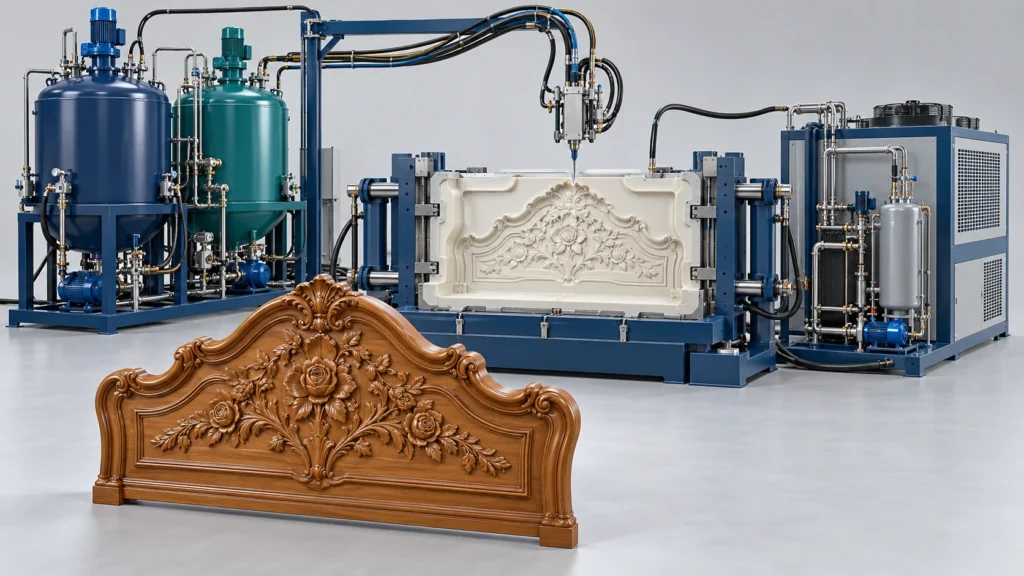
Proyecto de línea de cabeceros de PU rígido con imitación de madera en Arabia Saudita
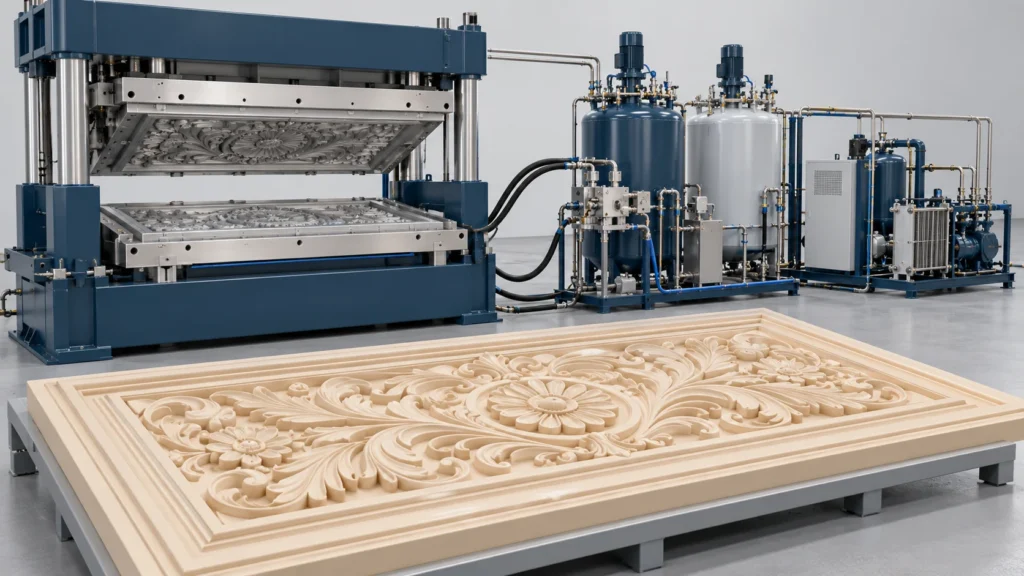
Proyecto de línea de moldeo de PU rígido para paneles decorativos tallados en China
Preguntas frecuentes
Respuestas sobre la selección del proceso, la integración de equipos y el soporte en la entrega.
Can density alone make a PU molding equivalent to solid wood?
How should carving labor savings be evaluated?
¿Qué información se necesita para una configuración preliminar?
Hablemos de su proyecto de producción de muebles
Share the following with your production brief: Master pattern/CAD, relief and undercuts, part thickness, finish, fastener locations, batch mix and output. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


