
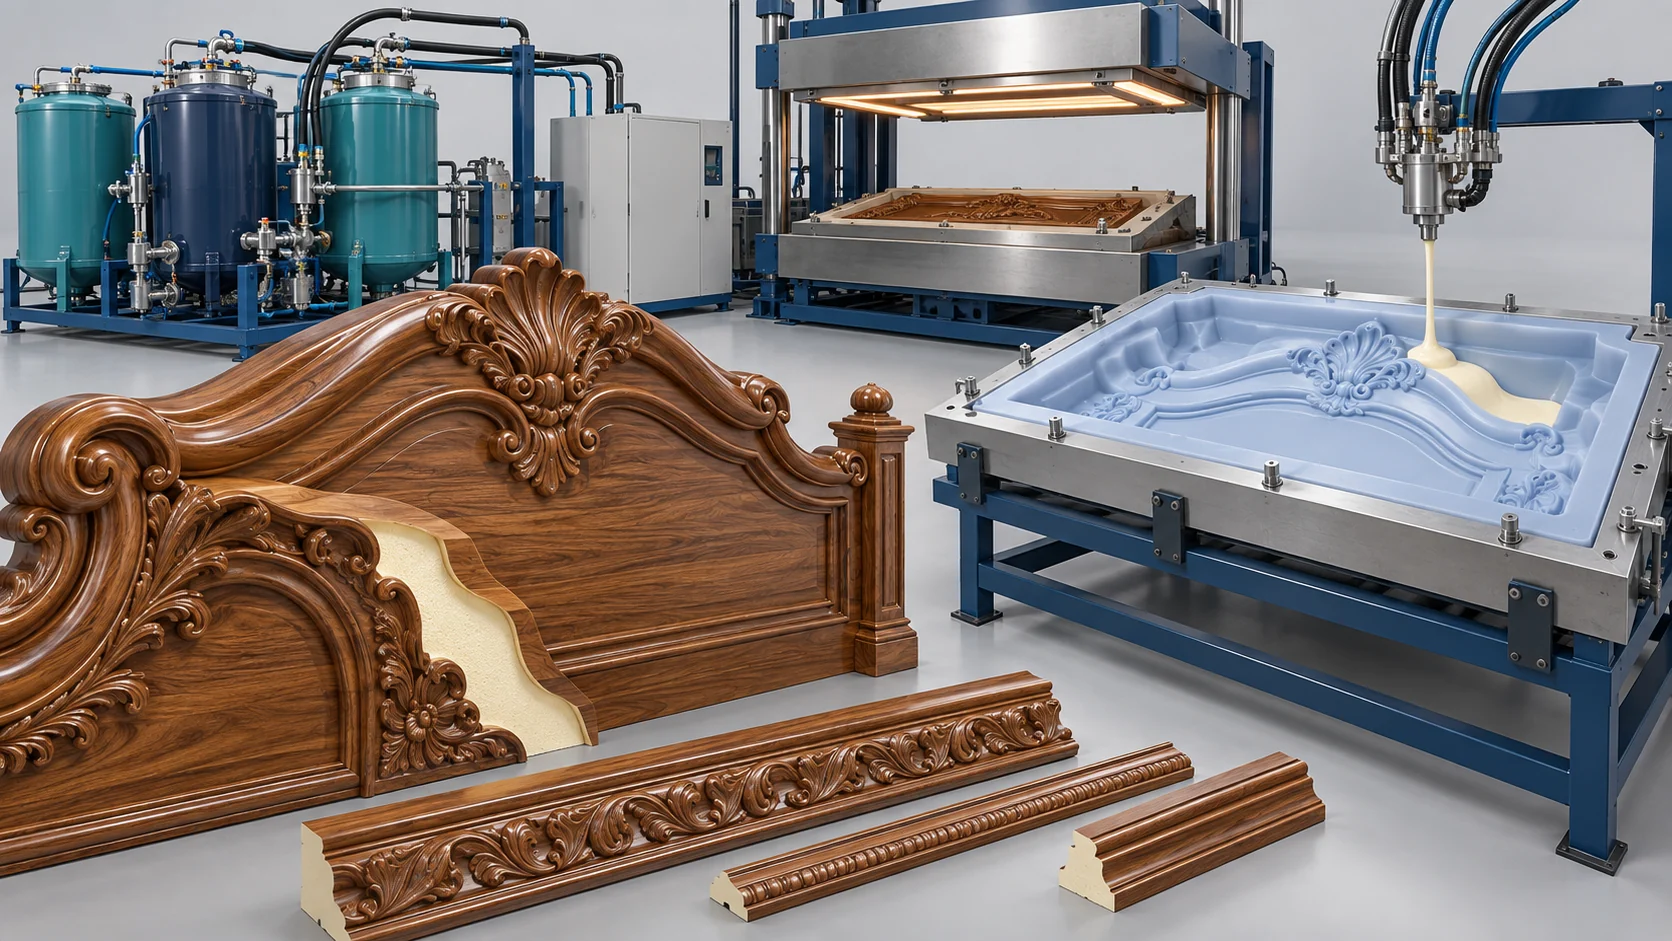
حل قولبة البولي يوريثان الصلب المشابه للخشب
Plan rigid PU imitation-wood moldings around the master pattern, mold, finish and fastening requirements.
Structural Rigid PU Solutions for Intricate Imitation Wood Carvings
Imitation-wood molding reproduces a selected master pattern through material delivery, expansion and cure in a suitable mold. Part density and surface finish are chosen for the design; they do not reproduce every structural property of a named wood species. Moisture response, cracking and fastener holding must be assessed on the molded part.
نطاق توريد محدد
Specify material delivery, mold type, release, cure and finishing interfaces. A carved-part project does not establish a fixed labor saving or universal woodworking compatibility.
المدخلات لاختيار العملية
Master pattern/CAD, relief and undercuts, part thickness, finish, fastener locations, batch mix and output.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Specify material delivery, mold type, release, cure and finishing interfaces. A carved-part project does not establish a fixed labor saving or universal woodworking compatibility.
Rigid PU Imitation Wood Molding Workflow
Review the pattern and finish → Prepare material and mold → Fill and cure → Finish and inspect. Define preparation, filling, cure and output timing separately for the selected configuration.
Review the pattern and finish
Identify fine relief, undercuts, parting lines and the coating or stain system.
Prepare material and mold
Confirm the formulation, mold construction and release procedure.
املأ وعالِج
Validate the shot and thermal sequence against the section thickness.
المواصفات الفنية
مراجع التكوين الحالي والاختبار. تُعد إعدادات المعدات ونتائج المواد ونتائج التجميع النهائي منفصلة؛ ويُطبَّق كل قيمة فقط على التكوين والظروف الموثقة الخاصة بها.
| المعلمة الفنية | المواصفة القياسية / القيمة | السياق الهندسي & التحقق |
|---|---|---|
| التطبيق المستهدف | Bed Headboard Carvings, Ornate Wall Panels, Mirror Frames | High-density architectural furniture millwork |
| مصفوفة المواد | High-Density Structural Rigid Polyurethane Foam | Fast-curing microcellular imitation wood |
| Part Density Range | 250 – 600 kg/m³ (Customizable per wood species) | Replicates pine, oak, mahogany, or teak |
| Screw/Nail Holding Force | Confirm against the selected fastener and specimen | Specify the fastener withdrawal method and source report |
| قدرة إخراج قياس الجرعات | 30 – 80 كغ/دقيقة (قابلة للتخصيص) | High-volume fast shot injection |
| زمن دورة نزع القالب | 4 – 8 minutes (Thickness dependent) | Rapid curing for heavy-section castings |
| Moisture Absorption | <0.5% (24-hour water immersion) | Verify dimensional stability and moisture response for the intended conditions |
ضوابط العملية وفحوص التطبيق
قيّم هذه الوظائف باستخدام المادة والتجهيزات القالبية الموجزة الإنتاجية المختارة. تتطلب نتائج الأجزاء النهائية أدلة قبول خاصة بها.
Pattern-to-tool planning
Select mold materials and release strategy for the actual carving and undercuts.
Part-level stability checks
Evaluate moisture, dimensional response and cracking under the intended conditions.
Defined finishing and fastening
Test the coating and fastener arrangement on representative moldings.
مشاريع ذات صلة
هذه مراجع تطبيقية ذات صلة. قارن المادة الفعلية والعملية والوحدات المسلّمة؛ فأرقام المشاريع المبلَّغ عنها ليست نتائج قبول لخط آخر.
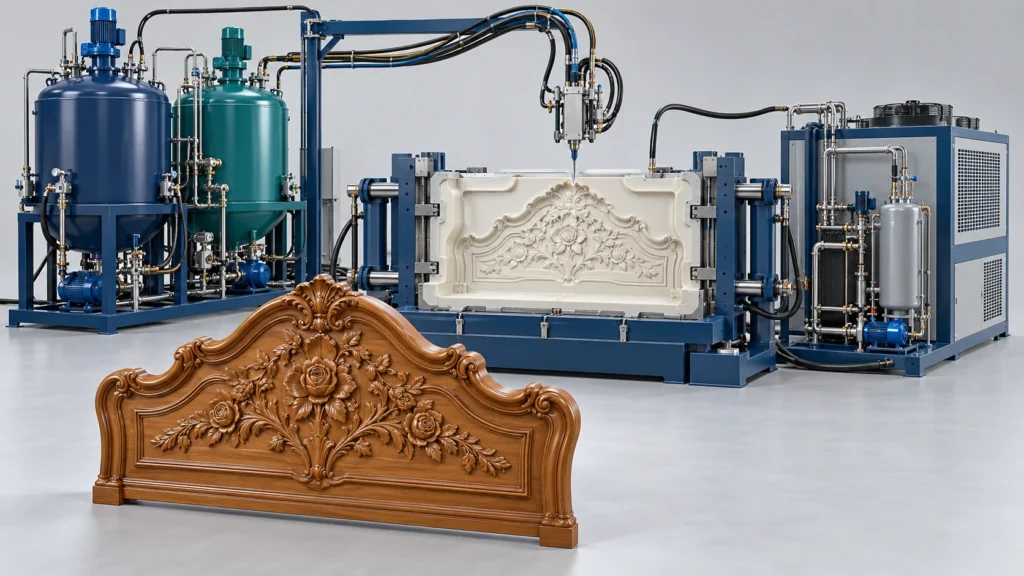
مشروع خط تشكيل البولي يوريثان الصلب للوحات رأس السرير بمظهر الخشب في السعودية
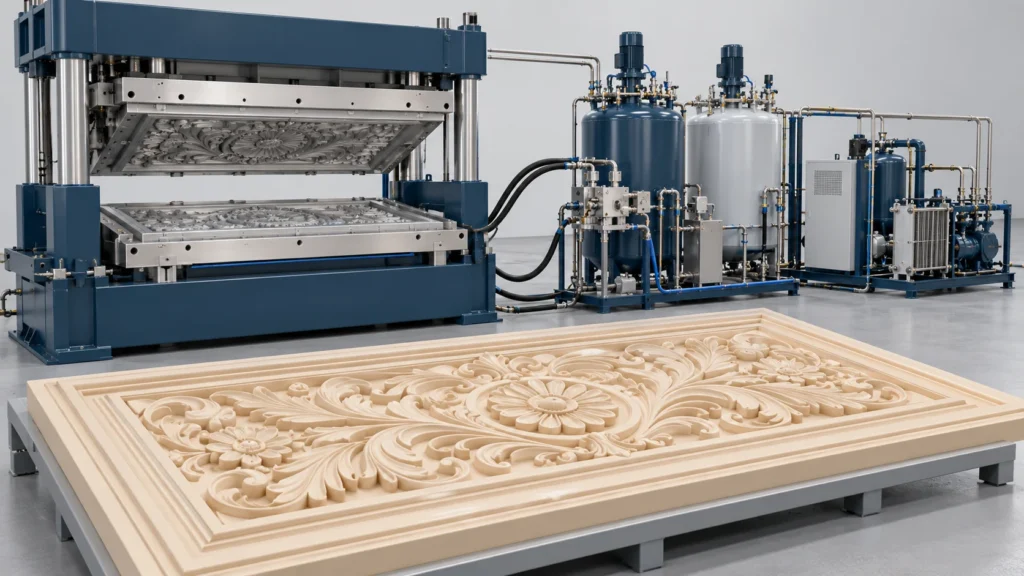
مشروع خط تشكيل البولي يوريثان الصلب للألواح الزخرفية المنقوشة في الصين
الأسئلة الشائعة
إجابات حول اختيار العملية وتكامل المعدات ودعم التسليم.
Can density alone make a PU molding equivalent to solid wood?
How should carving labor savings be evaluated?
ما المعلومات المطلوبة لإعداد تكوين أولي؟
ناقش مشروع إنتاج الأثاث الخاص بك
Share the following with your production brief: Master pattern/CAD, relief and undercuts, part thickness, finish, fastener locations, batch mix and output. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


