
Solución de inyección directa para marcos fotovoltaicos de material compuesto
Coordinate closed-box PU injection and continuous pultrusion for the selected composite PV frame profile.
Engineered Composite Framing for Next-Generation Solar Modules
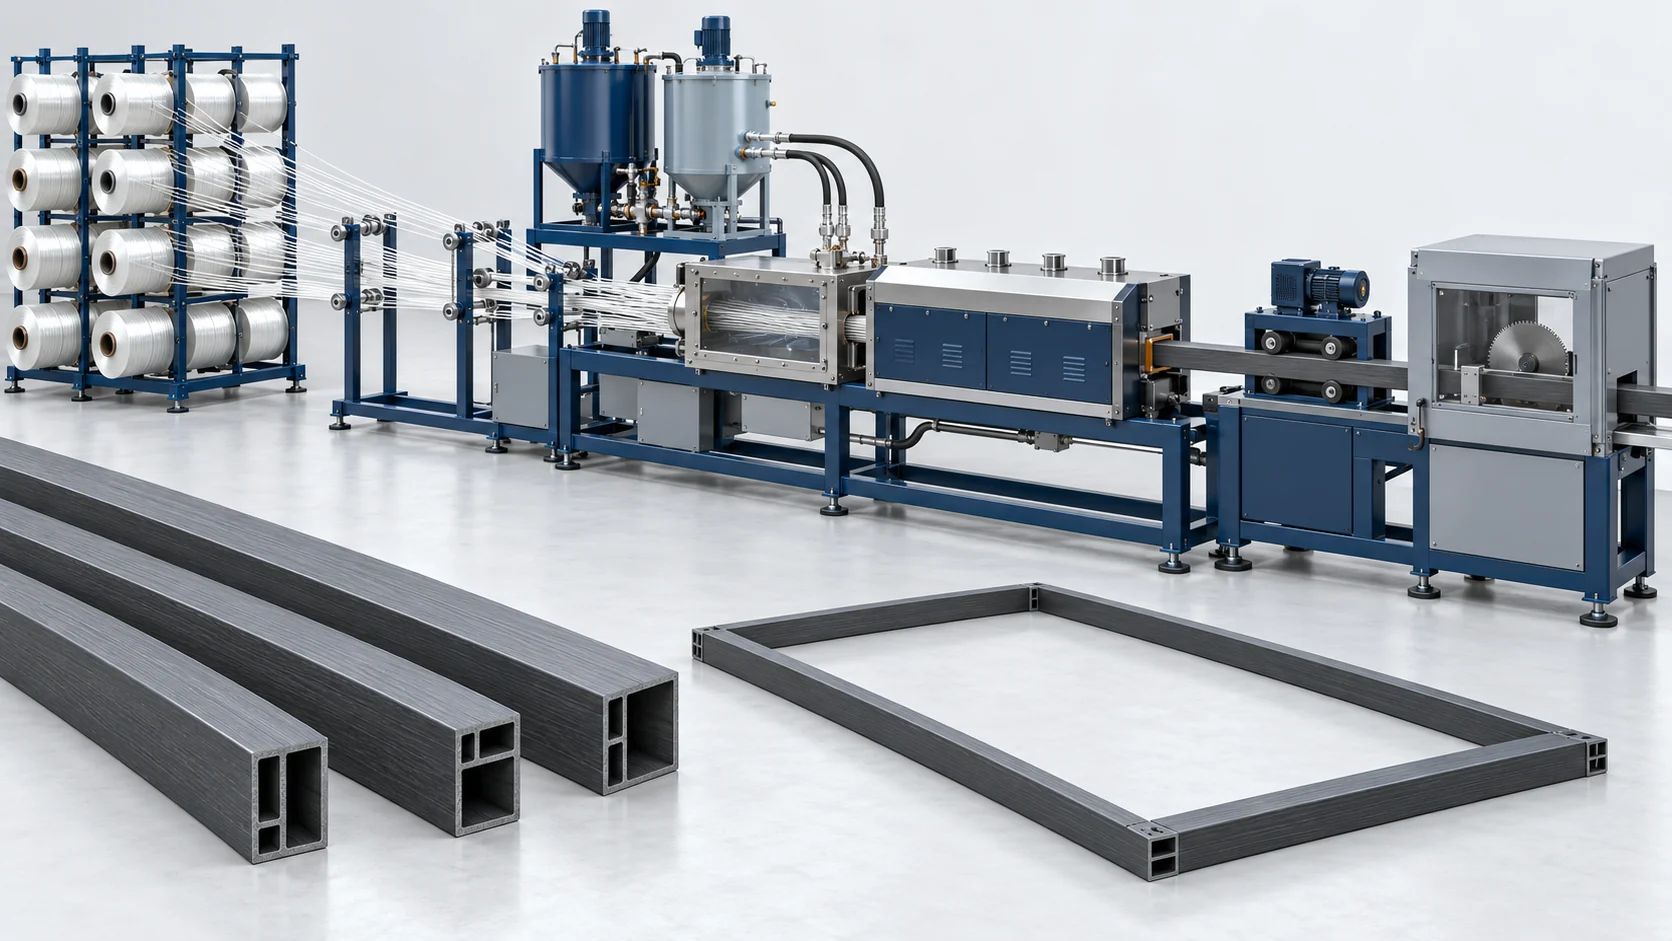
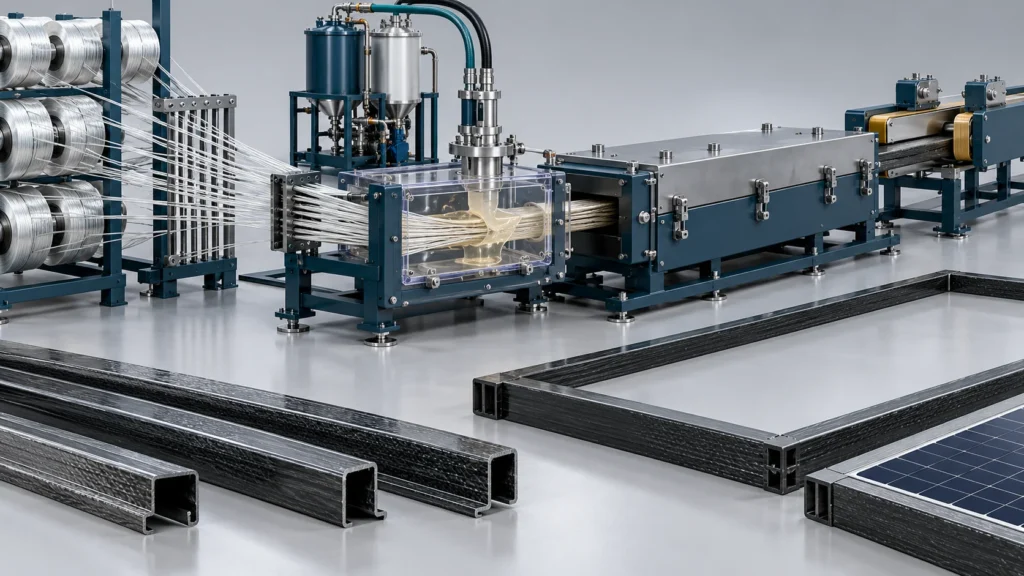
Continuous frame pultrusion feeds reinforcement through the configured injection box and heated die before pulling and cutting. Resin delivery, reinforcement wet-out, die temperature and pull speed must be matched. This is distinct from molding separate frames in a closed tool or dispensing adhesive around a module.
Alcance de suministro definido
Define resin conditioning, metering, mixing and injection-box interfaces, then identify pulling, heating and cutting equipment. Frame and module performance require their own structural, environmental and electrical evaluation.
Insumos para la selección del proceso
Profile section, fiber form/sizing, resin data, fiber-content basis, die length, puller interfaces and module tests.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Define resin conditioning, metering, mixing and injection-box interfaces, then identify pulling, heating and cutting equipment. Frame and module performance require their own structural, environmental and electrical evaluation.
Composite PV Frame Direct Injection Workflow
Prepare reinforcement and profile → Condition and meter resin → Impregnate, heat and pull → Cut and qualify. Define preparation, filling, cure and output timing separately for the selected configuration.
Prepare reinforcement and profile
Confirm fiber form, sizing, content basis and the profile/die design.
Condition and meter resin
Establish resin handling, ratio and the injection-box interface.
Impregnate, heat and pull
Validate wet-out and cure along the actual die and line-speed window.
Standard Engineering Parameters for Solar Pultrusion
Configuración existente y referencias de ensayo. Los ajustes del equipo, los resultados del material y los resultados del conjunto terminado son independientes; aplique cada valor solo a su configuración y condiciones documentadas.
| Parámetro | Valor / Unidad | Configuración / Condiciones aplicables |
|---|---|---|
| Resin Dosing Output | 0.8 to 8.0 kg/min (Custom up to 15 kg/min) | Servo-driven continuous high-pressure piston pumps |
| Presión de mezcla | 10.0 to 15.0 MPa | High-pressure impingement mixing without dynamic rotor |
| Stoichiometric Precision | Tolerancia de proporción dentro de ±0,3 % | Dynamic closed-loop encoder tracking across pull speeds |
| Pultrusion Line Speed Range | 0.5 to 1.5 m/min (Standard) | Matched to polyurethane resin gelation and die length |
| Supported Fiber Content | Up to 82% (Fiber volume fraction) | High-pressure closed injection box with roving pre-seal |
| Frame Profile Tensile Modulus | Greater than 45 GPa | ASTM D638 testing on cured glass/polyurethane matrix |
Equipos principales de esta solución
Las referencias de equipos se seleccionan según su proceso documentado. La dosificación principal, el suministro auxiliar y las rutas alternativas no constituyen un único paquete estándar.
Controles de proceso y verificaciones de aplicación
Evalúe estas funciones con el material, los moldes y el resumen de producción seleccionados. Los resultados de las piezas acabadas requieren su propia evidencia de aceptación.
Line-linked delivery
Coordinate resin demand with profile geometry and pulling speed.
Separate pressure references
Distinguish mixing pressure, injection delivery and box backpressure.
Verified reinforcement basis
Confirm fiber mass or volume content and use actual wet-out and laminate evidence.
Proyectos relacionados
Estas son referencias de aplicación relacionadas. Compare el material, el proceso y los módulos entregados reales; las cifras de proyecto reportadas no son resultados de aceptación para otra línea.
Preguntas frecuentes
Find answers about Composite PV Frame Direct Injection Solution, including material selection, equipment configuration and the information needed to plan a production line.
Is direct injection here a batch closed-mold process?
Does the stated fiber percentage establish laminate quality?
¿Qué información se necesita para una configuración preliminar?
Request a Composite Solar Frame Equipment Proposal
Share the following with your production brief: Profile section, fiber form/sizing, resin data, fiber-content basis, die length, puller interfaces and module tests. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


