Los problemas de dureza del poliuretano rara vez se anuncian en el laboratorio. Aparecen como la queja de un cliente sobre una suela que se siente demasiado rígida, un rodillo que marca la lámina o un lote de sellos que no asienta correctamente. Para cuando una muestra llega al durómetro, la verdadera pregunta suele haber pasado de “¿esta pieza cumple la especificación?” a “¿por qué este lote es diferente del anterior?”. Medir la dureza del poliuretano es sencillo. Medirla con la fiabilidad suficiente para controlar la producción es una habilidad distinta, y la mayor parte del error en los datos de dureza proviene de cómo se realiza la medición, no del durómetro en sí.
Qué mide realmente la dureza del poliuretano
Un durómetro Shore no mide cuán rígida es una pieza bajo carga, qué tan bien devuelve la energía ni cuánto se desgastará. Mide cuánto penetra en la superficie un indentador cargado por resorte de una geometría específica bajo una fuerza definida. El poliuretano es viscoelástico, por lo que esa penetración depende de la temperatura, el tiempo de contacto y la presencia de cualquier superficie dura de respaldo: tres variables que causan más disputas de control de calidad que la propia formulación.
En la escala Shore, el resultado es un número adimensional de 0 a 100, donde un número mayor significa que el material resiste más la indentación. Un material Shore 0 deja que el indentador se hunda por completo; Shore 100 no ofrece prácticamente ninguna penetración bajo la fuerza del resorte de la escala. El cero y el cien son límites del instrumento, no descripciones del material como “blando” y “duro”.
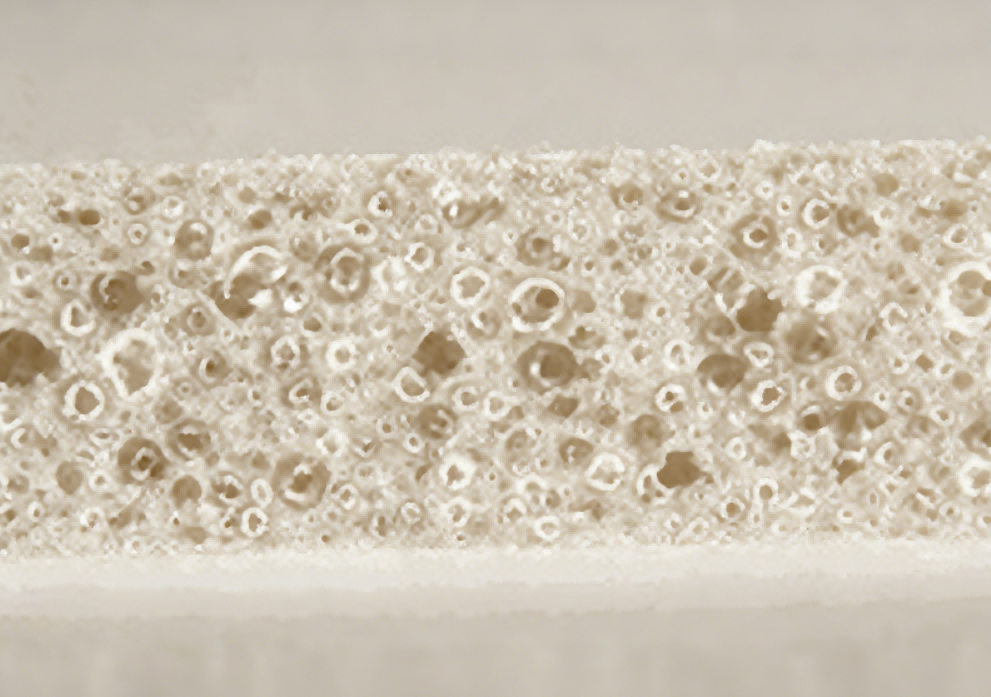
Como la medición es una indentación y no una propiedad volumétrica, se comporta de manera distinta de la resistencia a la tracción o el módulo. Dos poliuretanos pueden dar la misma lectura Shore A 60 y aun así diferir en resiliencia, deformación permanente por compresión y resistencia al desgarro. La dureza debe tratarse como una verificación superficial rápida y comparativa, no como un sustituto de un análisis más completo de propiedades.
Shore A, Shore D y Shore 00: cómo elegir la escala correcta
The letter after “Shore” matters as much as the number. Shore A uses a truncated cone indentor and a moderate spring force for soft-to-medium elastomers and flexible foams — in practice, most cast polyurethane parts land between roughly 20 and 95 Shore A. Shore D uses a sharper cone and a heavier spring for hard elastomers, rigid foams, and tough plastics. Shore 00, with a broad blunt indentor and a lighter spring, is reserved for very soft foams, gels, and low-density materials where even Shore A compresses the sample too far.
The common source of confusion sits in the low-90s of Shore A and the 20s to 40s of Shore D. A 95 Shore A elastomer and a 45 Shore D elastomer can feel similar under the thumb, but they are different materials with different heat builds, recovery behavior, and machining characteristics. In most shops the working rule is to switch from Shore A to Shore D above about 90 Shore A. Do not average or convert between the scales as if they were units of the same quantity.
Shore A and Shore D overlap in the 90s, but they are not interchangeable — a Shore 95A part and a Shore 50D part are engineered for different service conditions. Dureza Shore A frente a Shore D en poliuretano covers how to read the overlap, when to switch scales, and why the choice affects material and process decisions.
If you are switching a part from Shore A to Shore D on an existing drawing, do not remap the old number one-to-one. Send the current hardness, the target hardness, and the part’s real service load to info@chinahaifeng.com, and we can help you judge whether the specification, the material, or the metering setup is the actual constraint.
El procedimiento de ensayo estándar según ASTM D2240 e ISO 868
Hardness readings are only comparable when the procedure is fixed. ASTM D2240 governs durometer hardness for rubber and rubber-like materials, and it is the reference most polyurethane shops default to [1]. ISO 868 covers the same Shore method for plastics and ebonite [2]. ISO 7619-1 addresses vulcanized and thermoplastic rubbers [3]. The documents share the same physical logic but differ on details such as minimum thickness and conditioning times, so a specification should state which standard it follows.
The procedure itself is deceptively short. Press the presser foot flat against the sample so the indentor penetrates perpendicular to the surface, then read the scale after a fixed dwell time. For elastic materials that relax under load, the reading falls over the first several seconds, which is why a one-second reading and a fifteen-second reading of the same part can differ by several points. Record the dwell time alongside the value; without it, the number cannot be compared across shifts or suppliers.
Take five readings at points spaced well away from each other and from the part edge — commonly 10 mm or more — and report the average or the median per the governing standard. A single reading on a molded part is best treated as a spot check, not as the part’s hardness value.
Handheld durometers with a presser foot give serviceable field data only if the operator applies the device the same way every time. For inbound inspection and lot acceptance, a stand-mounted durometer with a controlled approach and a constant applied force removes the largest operator variable. If the durometer is fitted with a mass, use it; thumb pressure is not a calibrated method.
Hardness is only one entry in a practical QC program for foams and elastomers. Medición de la resiliencia de la espuma de poliuretano: guía práctica de ensayo covers the companion resilience test and explains why padding, seating, and cushioning specifications often call out hardness and resilience together.
Reglas de preparación y acondicionamiento de muestras que importan más que el medidor
The most common cause of an artificially high reading is a sample that is too thin. If the indentor senses the steel bench or the mold surface beneath the part, it reports the backing rather than the polymer. ASTM D2240-class measurements generally require a minimum thickness around 6 mm [1], while ISO 868 sits near 4 mm for many materials [2]. When in doubt, stack flat sheets or machine a dedicated test button rather than testing the finished edge.
Surfaces must be flat, parallel to the presser foot, and free of flash, release agent, and dust. Measuring on a curved crown, a gate scar, or a parting seam pushes the indentor at an angle and corrupts the result. For parts that are inherently curved — rollers, wheels, bump stops — take the reading on a machined flat or on a witness button cured in the same shot, and record that the value is a witness-button reading rather than an in-situ part reading.
Temperature is the hidden multiplier. Polyurethane hardens measurably as it cools, and a part pulled warm from the mold will read differently from the same part conditioned overnight. Standard conditioning is around 23 ± 2 °C and 50 ± 5 % relative humidity, and repeat comparison tests should always be run at the same part temperature after the part has fully cooled. A hardness number without a temperature is a number without context.
Errores comunes que distorsionan las lecturas del durómetro
Most bad hardness data follows a short list of patterns:
- Testing a sample thinner than the standard minimum, so the indentor reads the support.
- Testing a rounded, textured, or flash-bearing surface instead of a flat, parallel face.
- Taking the reading immediately at impact rather than after a fixed dwell time.
- Not recording the durometer scale, or mixing Shore A and Shore D values from different instruments.
- Testing parts at different temperatures — warm from demolding versus cold from storage.
- Using a durometer that has not been checked against certified reference blocks.
Each of these errors moves the result in a predictable direction. A thin or back-supported sample reads artificially hard. A soft, warm part reads artificially soft. An impulse reading on a viscoelastic material is closer to its short-term stiffness than to its relaxed hardness. These errors move the number without telling you anything about whether the formulation or the machine changed — which is the question production actually needs answered.
A reliable hardness number is only useful if you can reproduce it. If a QC chart with the same formulation swings more than a few points across a shift, message WhatsApp +86 13566296633 or email info@chinahaifeng.com with the before-and-after readings and the machine’s current ratio settings. In our experience the cause usually traces back to metering drift or mold temperature, not to the durometer.
La consistencia de la dureza y el papel de la precisión de dosificación
On the production floor, hardness is not really a measurement problem; it is a formulation and mixing problem. Shore hardness for a given polyurethane system is set by hard-segment content, isocyanate index, chain-extender ratio, and cure history. Density plays an indirect role — two foams with the same density can still read differently if their polymer structure differs, so density should not be used as a hardness proxy.
That is why the equipment-level variables matter. If the metering pumps drift on the A or B side, the isocyanate index drifts with them, and the cured part walks up or down the Shore scale across a shift. Dynamic metering accuracy on a precision casting or high-pressure line in the range of ±0.3 % of full scale is the practical target for keeping ratio-driven hardness scatter small — along with disciplined tank and hose temperature control so the viscosities, and therefore the pump fills, stay stable.
Mold temperature is the second control. A mold running 10 °C cold changes the cure profile and can freeze a higher short-term hardness into the skin while the core cures differently later. When hardness varies between cavities on the same machine, check mold temperature balance and venting before adjusting the formula. The formulation may not have changed; the heat history did.
Once a hardness approval is tied to a specific A/B ratio, the practical question becomes dosing repeatability shot to shot. Cómo calcular el peso de dosificación en poliuretano covers shot weight calculation and how consistent metered output feeds part-to-part property control.
Revise su especificación de dureza con un ingeniero de equipos
Hardness scatter rarely improves by buying a better durometer. It improves by tracing the target number back through the material ratio, the metering repeatability, and the mold thermal balance.
If you are setting a new hardness spec or chasing an existing one across shifts, prepare four things before you contact us:
- The Shore scale, target value, and tolerance from the part drawing.
- The material system — prepolymer type, polyol, and chain extender.
- The shot weight, cycle time, and current A/B ratio settings.
- A short note on where the scatter appears: between shifts, between cavities, or after a supplier change.
Email info@chinahaifeng.com or message us on WhatsApp at +86 13566296633. We will review the logic of the spec, not just the durometer reading.
Preguntas frecuentes
¿Cuál es la diferencia entre Shore A y Shore D?
Shore A uses a truncated cone indentor and a lighter spring for soft-to-medium elastomers and flexible foams. Shore D uses a sharper cone and a heavier spring for harder materials. They are not convertible units; a specification should name the scale, not just the number.
¿Puedo medir la dureza directamente en una pieza terminada?
Only if the measured area is flat, parallel to the presser foot, and thick enough that the indentor is not reading the backing. Curved parts such as wheels and rollers are better checked on a flat witness button cured in the same shot, with the method recorded.
¿Qué espesor de muestra se requiere?
A common minimum is about 6 mm for ASTM D2240-class testing and about 4 mm under ISO 868 guidance for many materials. If the part is thinner, stack flat pieces or cut a dedicated test button. A reading taken on a thin section over a hard support will read artificially high.
¿Cuántas lecturas debo tomar?
Take five readings at spaced locations and report the average or median according to the governing standard. A single reading on a molded part is a spot check, not a hardness value, because molded surfaces vary point to point.
¿Por qué el mismo material da lecturas distintas en días diferentes?
Temperature and dwell time are usually the answer. Polyurethane is viscoelastic and temperature-sensitive, so a warm part reads softer than a conditioned one, and a short dwell reads differently from a standard dwell. Keep part temperature around 23 ± 2 °C and record the dwell time with every value.
¿La densidad de la espuma determina la dureza?
Not directly. Density and hardness often move together in practical foam families, but two foams at the same density can have different hardness because hardness is set by polymer structure, hard-segment content, and index — not by density alone.
Referencias
[1] ASTM International. ASTM D2240, Standard Test Method for Rubber Property—Durometer Hardness. West Conshohocken, PA: ASTM International.
[2] International Organization for Standardization. ISO 868, Plastics and ebonite — Determination of indentation hardness by means of a durometer (Shore hardness). Geneva: ISO.
[3] International Organization for Standardization. ISO 7619-1, Rubber, vulcanized or thermoplastic — Determination of indentation hardness — Part 1: Durometer method (Shore hardness). Geneva: ISO.
Si te interesa, echa un vistazo a estos artículos relacionados:
Qué es la espuma de poliuretano semirrígida
¿Qué es la espuma de poliuretano proyectada? Composición y aplicación
RRIM frente a RIM: qué proceso se adapta mejor a tu pieza estructural
Causas de la contracción en la espuma de poliuretano y cómo controlarla
Medición de la resiliencia de la espuma de poliuretano: guía práctica de ensayo