

¿Qué es el moldeo por inyección reactiva (RIM)?
El moldeo por inyección reactiva (RIM) es un proceso de poliuretano en molde cerrado que dosifica dos o más líquidos reactivos de baja viscosidad en una cabeza de mezcla de alta presión, los mezcla por impacto e inyecta el líquido en reacción en un molde donde se completa la polimerización. La diferencia esencial respecto del moldeo por inyección de termoplásticos es que no se funde ningún polímero sólido: el poliuretano se forma durante el proceso [1], [2].
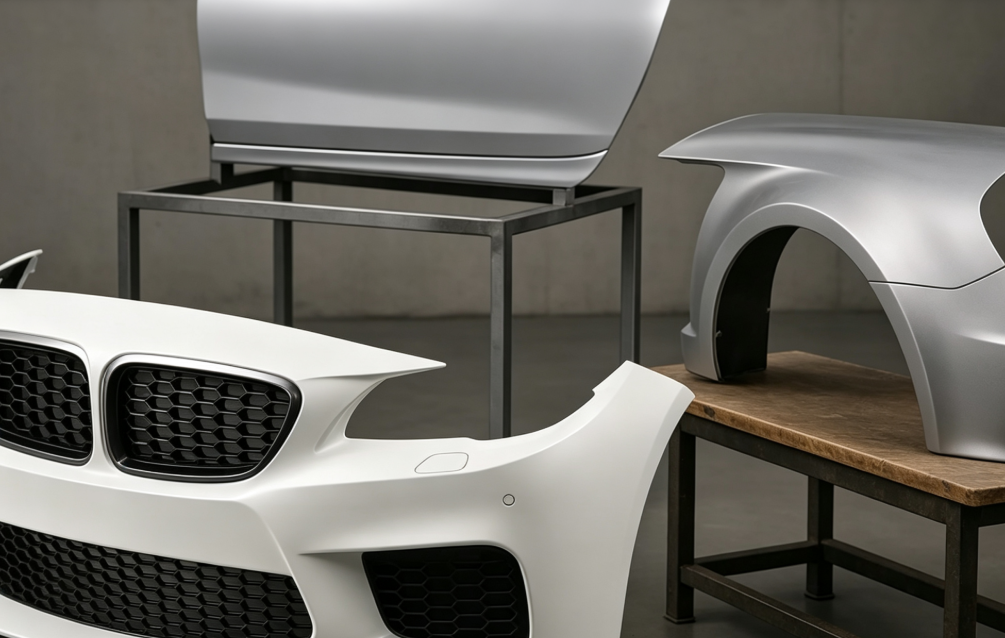
That distinction drives most downstream decisions. Because the liquid enters the mold at low viscosity, it can fill thin walls and complex contours with lower clamping force than a similar thermoplastic part would require. Because cure is a chemical reaction, cycle time depends on formulation, part mass, wall thickness, and mold temperature—not simply on cooling time [3], [4].
Operators who come from low-pressure casting often underestimate two things: first, impingement mixing needs consistent high pressure to generate a homogeneous blend; second, any metering drift shows up directly as hardness, density, or surface-quality variation. A deviation of one percentage point in the component ratio can shift part properties enough to fail a customer specification.
Cómo funciona el proceso RIM paso a paso
1. Material conditioning. The polyol side and isocyanate side are held at controlled temperature—commonly in the 25–45°C range on production equipment—and recirculated to keep viscosity stable before the shot.
2. High-pressure metering. Each stream is delivered by opposing pumps or cylinders that maintain the selected A:B ratio. Dynamic metering accuracy of ≤±0.3% is the practical target on modern RIM machines because ratio error translates directly into property drift.
3. Impingement mixing. The two streams collide at high velocity inside a small mixing chamber. The rapid energy exchange blends the components without the long-residence mechanical mixers used in many low-pressure casting systems.
4. Mold filling and cure. The mixed liquid flows through the runner into a closed mold. Polymerization raises molecular weight and releases exotherm; the part usually demolds once it has enough green strength to hold its shape without distortion.
5. Demold and post-mold handling. Parts are released, deflashed or trimmed, and in some cases post-cured to complete property development.
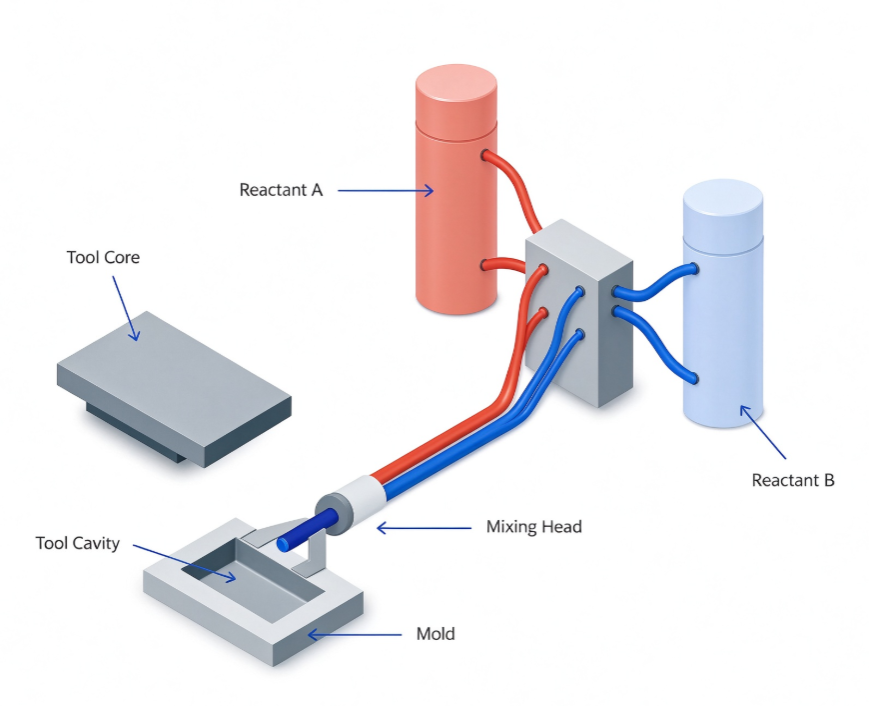
Shot weight is the first value to lock down after the CAD model is fixed. If it is calculated from a volume estimate instead of a mass balance, the result is usually an oversized or undersized metering unit.
If you are setting up a new mold, shot weight is one of the first variables to lock down. Cómo calcular el peso de dosificación en poliuretano covers the calculation so you do not oversize or undersize the metering unit.
RIM, RRIM y SRIM: dónde están los límites
In practice, people use “RIM” loosely to describe several polyurethane molding processes. The differences matter because they change viscosity, mixing conditions, and tool wear.
Unfilled RIM uses two reactive streams with no solid filler. It suits parts that need a fine surface, controlled density, and moderate structural performance. Once short fibers are added to the liquid stream, the process becomes RRIM; the slurry is more abrasive and more viscous, so pump, mixing head, and metering decisions change. When a continuous fiber mat or preform is placed in the mold and the liquid fills around it, the process is SRIM.
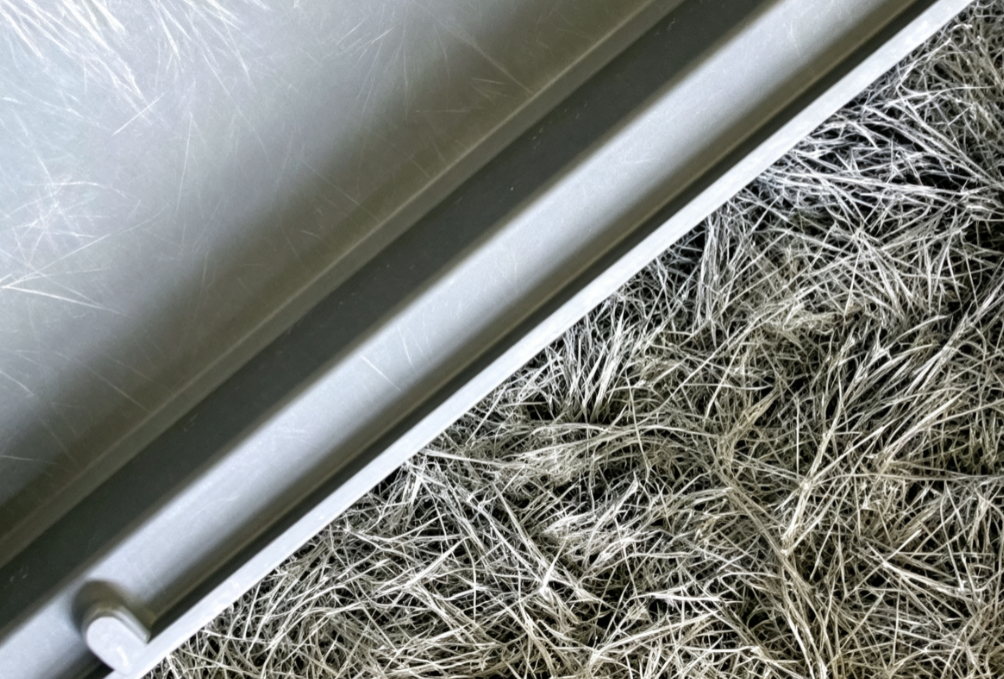
Unfilled RIM works well for large, detailed surfaces, but once long fibers or continuous mats enter the system, viscosity and mixing behavior change. RRIM frente a RIM: qué proceso se adapta mejor a tu pieza estructural covers when reinforced RIM is the better fit.
When the part uses a structural preform instead of liquid-carried reinforcement, the process becomes SRIM rather than RIM. SRIM explicado: fundamentos del moldeo por inyección reactiva estructural covers how dosing and tooling change for structural parts.
Parámetros del equipo que determinan la calidad de la pieza
Most RIM quality problems can be traced to four machine-level variables.
Metering accuracy. If the A:B ratio drifts during a shift, the part hardness, density, or cure state drifts with it. Closed-loop servo control and mass-flow verification are more useful than a catalog throughput number.
Mixing pressure. Impingement mixing requires enough pressure to break the streams into fine, uniformly distributed domains. On the RIM systems we build, the mixing head operates at 150–200 bar. Lower pressure can still produce a part, but it often produces streaks, soft zones, or unreacted pockets.
Material temperature control. Viscosity changes with temperature, and viscosity changes the mixing result. A stable recirculation loop holds the material at processing temperature and prevents cold-shot variation.
Mold temperature and clamp. The mold controls surface finish, cure rate, and demold behavior. The clamp must hold the tool closed against cavity pressure, but RIM clamp forces are modest compared with thermoplastic injection molding of the same projected area [4].
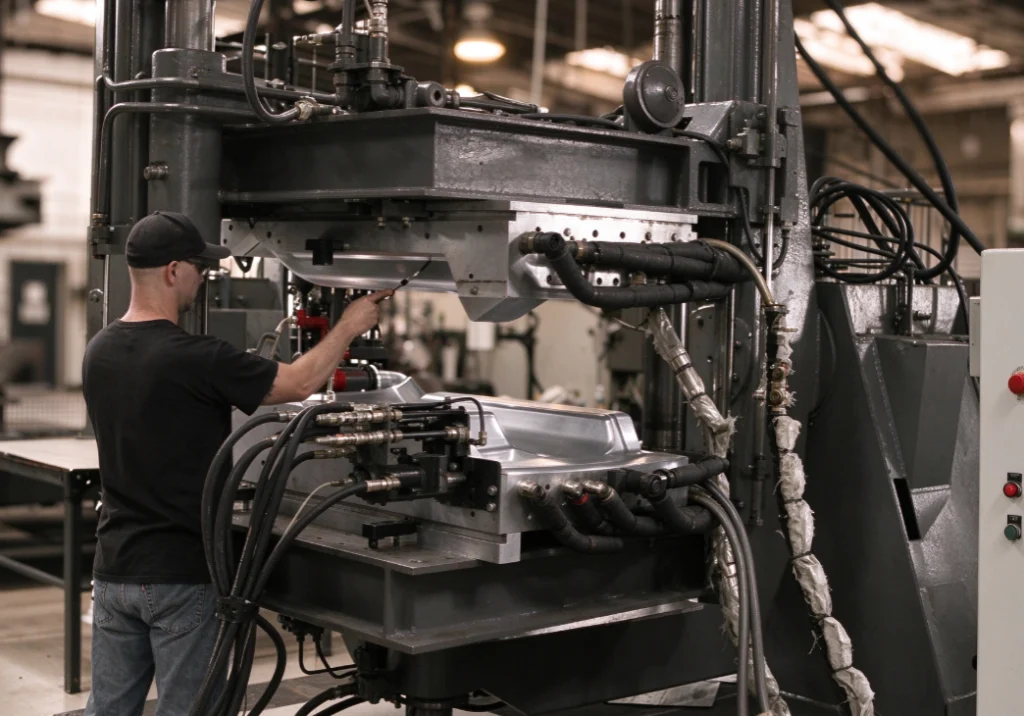
A useful way to diagnose a RIM problem is to treat the machine as the controlled variable, not the source of last resort. If the metering unit produces a correct ratio under no pressure but not during a shot, the issue is often a worn pump, air entrainment, or a bad recirculation valve—not the formulation.
Equipment selection checkpoint. If you are comparing a low-pressure casting machine with a true high-pressure RIM cell, collect these numbers first: part shot weight, mold volume, target cycle time, material viscosity at processing temperature, and whether any filler or fiber is present. Send them with your part drawing to info@chinahaifeng.com or WhatsApp +86 13566296633, and ask for a metering-range and mixing-head recommendation rather than a generic quote.
Del prototipo a la producción en serie: dimensionamiento de una celda RIM
A prototype mold can hide machine limitations. The real test is whether the cell can repeat the shot over hundreds of cycles without drifting.
Three numbers matter when sizing a production RIM machine: shot weight, pouring rate, and available mixing pressure. Small interior parts may need only 50–100 g/s, while a large structural panel can require 1,000–2,000 g/s. If the machine is run near its maximum pour rate all day, the operator has no margin when the formulation changes or the mold fills harder than predicted.
Cycle structure is the next decision. A RIM cell usually includes material conditioning, metering, mixing, mold clamping, and demold. The bottleneck is rarely the mixing head alone; it is often the mold-change or trimming step. Automation pays back only when the metering system can deliver the same shot at the same ratio across the entire production window.
Hable con un ingeniero de equipos RIM
Before you commit to a pour rate or clamp size, verify that the machine can hold your ratio window across an entire shift.
Send these five items to info@chinahaifeng.com or WhatsApp +86 13566296633:
- Part material and target Shore hardness
- Shot weight or part volume
- Required cycle time
- Mold dimensions and number of cavities
- Filler or fiber loading, if any
The RIM team at Haifeng Polyurethane Machinery will use them to recommend a metering range, mixing head, and recirculation setup—not just the largest machine in the catalog.
Preguntas frecuentes
¿Cuál es la diferencia entre el RIM y el moldeo por inyección tradicional?
Traditional injection molding melts a solid thermoplastic and cools it under high clamp force. RIM pumps low-viscosity reactive liquids into a mold and forms the polymer by chemical reaction inside the cavity. RIM typically requires less clamp force for a similar part, and it is especially useful for large, thin-walled polyurethane components [1], [4].
¿Qué materiales se utilizan en el RIM?
Most RIM systems use a two-component polyurethane chemistry: a polyol side and an isocyanate side. Additives control foaming, cell structure, flame retardancy, release, and color. Reinforced systems add short fibers or mats, which moves the process toward RRIM or SRIM.
¿Qué precisión tiene la proporción de mezcla en el RIM?
Production RIM machines should hold dynamic metering accuracy near ±0.3% across the operating range. Ratio drift is one of the most common causes of hardness and density variation in finished parts.
¿Es el RIM adecuado para piezas reforzadas con fibra?
Yes, but the equipment must be specified for the additional viscosity and abrasiveness. Unfilled RIM equipment can be damaged by reinforced slurry or mat processes; RRIM and SRIM require different pump, mixing-head, and seal selections.
¿Qué tamaño de inyección puede manejar una máquina de RIM?
It depends on the platform. General-purpose RIM machines may cover 50–2,000 g/s, while specialized systems narrow that range for small precision parts or large building panels. The correct machine is matched to shot weight and cycle time, not simply to maximum output.
Referencias
[1] C. W. Macosko, RIM: Fundamentals of Reaction Injection Molding. Munich, Germany: Hanser Publishers, 1989.
[2] D. Randall and S. Lee, The Polyurethanes Book. New York, NY, USA: John Wiley & Sons, 2002.
[3] G. Oertel, Polyurethane Handbook, 2nd ed. Munich, Germany: Hanser Publishers, 1994.
[4] “Reaction injection molding,” in Encyclopedia of Polymer Science and Technology, 4th ed. Hoboken, NJ, USA: Wiley, 2014.
Si te interesa, echa un vistazo a estos artículos relacionados:
RRIM frente a RIM: qué proceso se adapta mejor a tu pieza estructural
Cómo calcular el peso de dosificación en poliuretano





