[مرجع سريع لمعايير عمليات Haifeng]
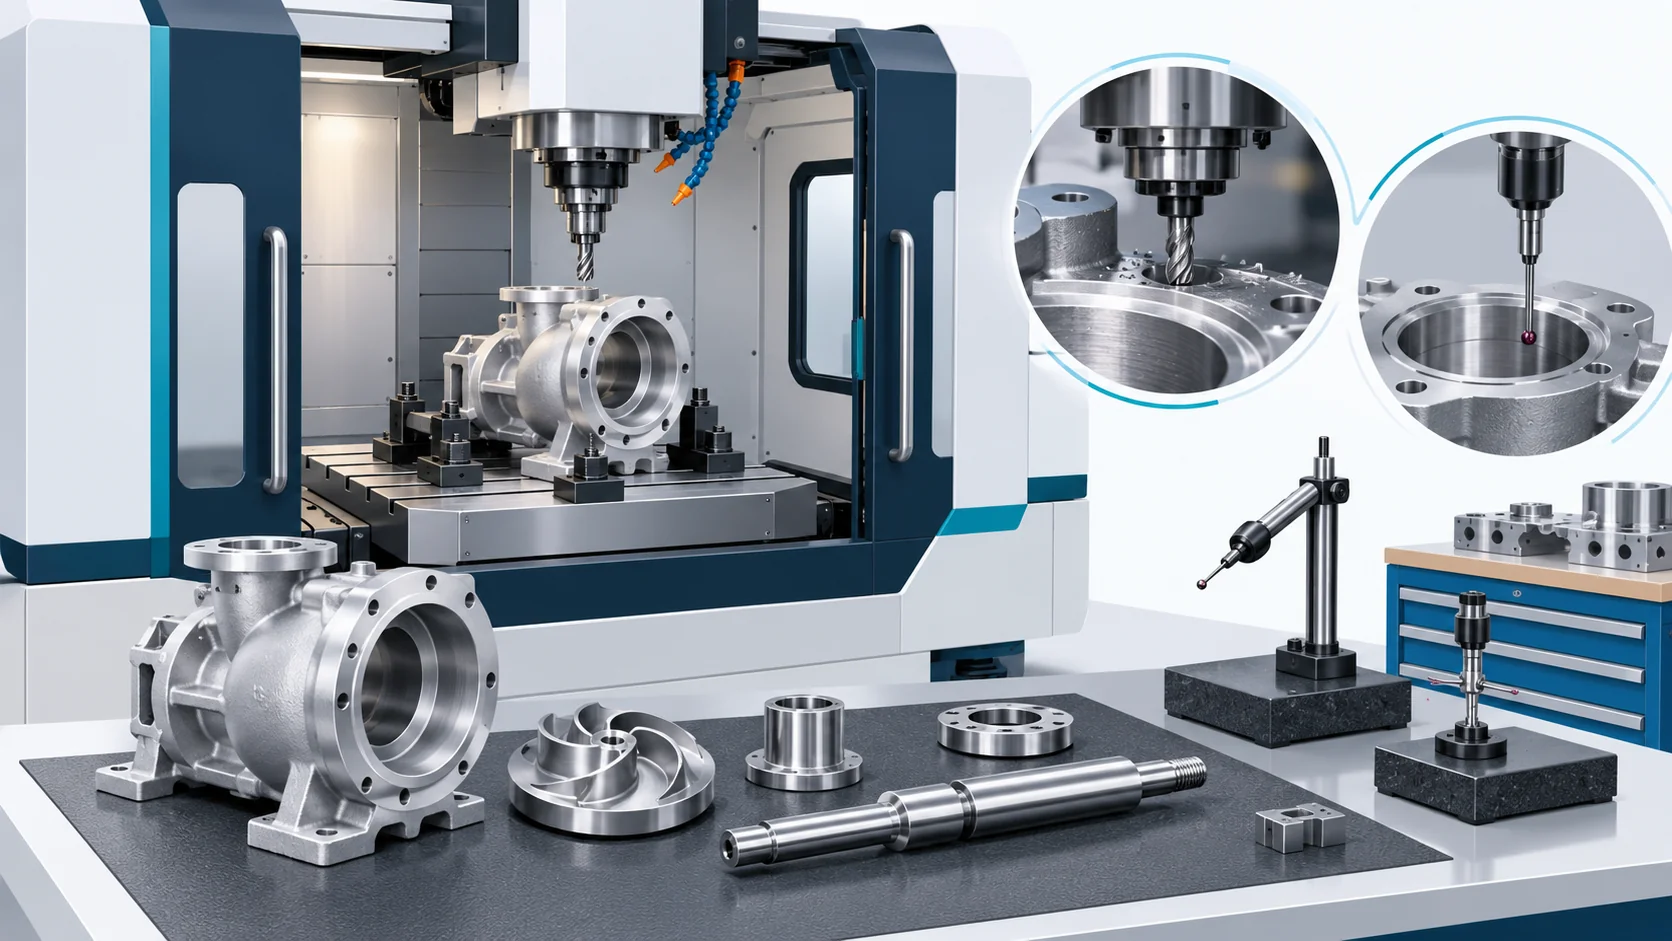
تعتمد دقة قياس الجرعات في معدات البولي يوريثان من Haifeng اعتمادًا كبيرًا على دقة التصنيع باستخدام الحاسب الآلي لمكوناتها الحرجة. فالخلوص من جهة واحدة بين ترس مضخة القياس وتجويفه لا يزيد عن 0.005 بوصة (نحو 0.127 مم). وتحدد دقة أسنان الترس والتلاؤم بين الترس والعلبة الكفاءة الحجمية تحديدًا مباشرًا؛ وأي انحراف في التصنيع يمكن أن يخفض دقة قياس الجرعات من ±0.3% إلى أكثر من ±0.5%. أثناء عمليات التصنيع باستخدام الحاسب الآلي، حافظ على دقة التموضع ضمن ±0.01 مم والتكرارية ضمن ±0.005 مم، بحيث تدعم جودة المكونات المتسقة دقة الماكينة الكاملة.
المعايير الرئيسية للعملية في لمحة:
| المعامل | معيار Haifeng | المرجع الصناعي | مؤشر دقة المعدات ذات الصلة |
| دقة التموضع لمركز التصنيع | ≤±0.01 مم | ≤±0.015 mm | أداء قياس الجرعات للآلة: يُتحقق منه بشكل منفصل في ظروف اختبار متفق عليها |
| دقة تكرار تحديد الموضع | ≤±0.005 mm | ≤±0.008 mm | معامل الاختلاف (CV) لاتساق أبعاد أجزاء الدفعة ≤0.5% |
| الخلوص العكسي | ≤0.002 mm | ≤0.005 مم | دقة تصنيع الكونتور |
| الانحراف الشعاعي للمغزل | ≤0.003 mm | ≤0.005 مم | خشونة سطح سن الترس Ra ≤0.4 ميكرومتر |
| الانحراف الشعاعي للأداة (مقطع تفريز طرفي من الكربيد الصلب) | ≤0.01 مم | ≤0.01 مم | تفاوت التجويف IT6–IT7 |
| خلوص سن ترس مضخة قياس الجرعات مع التجويف | 0.005 بوصة (0.127 مم) لكل جانب | — | الكفاءة الحجمية ≥95%؛ دقة قياس الجرعات ±0.3% |
| خشونة سن ترس مضخة قياس الجرعات | Ra ≤0.4 μm | Ra ≤0.8 ميكرومتر | معدل تآكل السن ≤0.001 مم/1000 ساعة |
| خشونة سطح التلامس بين قلب الصمام ورأس الخلط | Ra ≤0.2 μm | Ra ≤0.4 μm | زمن تبديل العكس ≤0.3 ثانية |
| سرعة القطع للفولاذ المقاوم للصدأ 316L | 100–140 م/دقيقة | 100–150 م/دقيقة | عمر الأداة ≥60 دقيقة |
| سرعة القطع لسبيكة الألومنيوم | 200–250 م/دقيقة | 180–250 م/دقيقة | دقة الأبعاد IT6–IT7 |
| درجة تفاوت التشغيل للفولاذ المقاوم للصدأ | IT6–IT7 | IT7–IT9 | قابلية التبادل لأسطح التلامس الحرجة |
| تفاوت موضع الثقب | ≤0.02 مم | ≥0.05 mm | دقة تجميع المكونات متعددة الثقوب |
| درجة الحرارة المحيطة أثناء التشغيل | 20±2°م | 20±5°م | خطأ التشوه الحراري ≤5 ميكرومتر |
| دقة التكرار لمجس التلامس داخل الماكينة | ≤0.002 mm | ≤0.005 مم | حلقة مغلقة تدمج التشغيل والفحص |
تُحدَّد تفاوتات المكوّنات المعنية وفق رسومات المشروع المعتمدة وإجراء الفحص. أما دقة قياس الجرعات للماكينة فتُحدَّد وتُختبر بشكل منفصل بالنسبة للتكوين المختار وحالة المادة ودرجة الحرارة والتدفق وأساس القياس؛ ولا تكفي أهداف الأبعاد للمكوّنات وحدها لإثباتها.
1. النطاق
1.1 العمليات المنطبقة
ينطبق إجراء التشغيل القياسي (SOP) هذا على التشغيل الآلي بنظام التحكم الرقمي (CNC) للأجزاء الدقيقة التالية الخاصة بمعدات Haifeng للبولي يوريثان:
| الجزء | المادة النموذجية | متطلب الدقة الرئيسي | مؤشر أداء المعدات ذات الصلة |
| ترس مضخة قياس الجرعات | فولاذ أدوات سبائكي/فولاذ سريع القطع | خشونة سطح الأسنان Ra ≤0.4 ميكرومتر؛ مقطع سنّي بدرجة DIN 5 | الكفاءة الحجمية ≥95%؛ دقة قياس الجرعات ±0.3% |
| جسم/تجويف مضخة قياس الجرعات | فولاذ أدوات سبائكي/9Cr18MoV | تفاوت التجويف IT6؛ استدارة أسطوانية ≤0.005 مم | يضمن دقة خلوص الترس مع التجويف |
| قلب/جلبة صمام رأس الخلط | 17-4PH/316L | خشونة السطح المتزاوج Ra ≤0.2 ميكرومتر؛ استدارة أسطوانية ≤0.003 مم | زمن العكس ≤0.3 ثانية؛ لا تسرب داخلي |
| شفة تركيب محرك السيرفو | سبيكة ألومنيوم 6061/7075 | استواء سطح التركيب ≤0.01 مم | محاذاة القارنة ≤0.03 مم |
| قاعدة تركيب الدليل الخطي | سبيكة ألومنيوم/فولاذ كربوني | استواء سطح التركيب ≤0.01 مم/500 مم | توازي الدليل ≤0.02 مم/م |
| دعامة اللولب الكروي | فولاذ سبائكي | تفاوت تجويف المحمل IT6؛ التماثل المحوري ≤0.01 مم | الحركة المحورية للولب ≤0.005 مم |
| شفة أنبوب نقل المواد | 316L | استواء سطح الإحكام ≤0.02 مم؛ Ra ≤0.8 ميكرومتر | لا يوجد تسرب عند 0.02 ميجاباسكال في اختبار إحكام الهواء |
| صفيحة فوهة رأس الخلط | كربيد أسمنتي/فولاذ أدوات | تفاوت قطر الثقب ±0.005 مم؛ Ra لجدار التجويف ≤0.2 ميكرومتر | جودة الخلط واتساق التدفق |
2. التحضير قبل العمل والتحقق من دقة الماكينة
2.1 مراجعة الوثائق الفنية
| الرقم | البند المطلوب فحصه | متطلب الدقة | معيار القبول |
| 1 | برنامج CNC | يطابق أحدث رسم | مراجعة البرنامج تطابق بطاقة العملية |
| 2 | قائمة الأدوات | يشمل طراز الأداة وهندستها وسجل عمر الخدمة | تم قياس انحراف الأداة وتسجيله |
| 3 | رسم التثبيت | تحديد مراجع التموضع وخطة التثبيت | دقة التحديد ≤0.005 مم |
| 4 | خطة الفحص | يشمل الأبعاد الحرجة والتفاوتات والأدوات | متوافق مع ISO 2768-1 أو متطلبات الرسم |
| 5 | شهادة المادة | درجة المادة مطابقة للرسم | يتضمن تقارير الصلابة والتركيب |
2.2 التحقق من دقة الماكينة
عاير مركز التشغيل بانتظام وفقًا لإجراء المعايرة الخاص به. يجب أن يكون خطأ المعايرة للمعايير الحرجة (انحراف دوران المغزل ودقة تحديد الموضع) ≤0.005 مم.
| بند المعايرة | معيار Haifeng | الفترة | أداة الفحص |
| الانحراف الشعاعي للمغزل | ≤0.003 mm | كل ثلاثة أشهر | مؤشر قرصي ومغزل معياري |
| الحركة المحورية للمغزل | ≤0.002 mm | كل ثلاثة أشهر | مؤشر قرصي |
| دقة تحديد الموضع لمحاور X/Y/Z | ≤±0.01 مم | كل ثلاثة أشهر | مقياس تداخل ليزري |
| دقة تحديد الموضع المتكرر لمحاور X/Y/Z | ≤±0.005 mm | كل ثلاثة أشهر | مقياس تداخل ليزري |
| الخلوص العكسي | ≤0.002 mm | كل ثلاثة أشهر | مقياس تداخل ليزري |
| استواء طاولة العمل | ≤0.01 مم/500 مم | كل 6 أشهر | ميزان تسوية دقيق/مسطرة استقامة |
| نظافة مخروط المغزل | لا توجد رقائق متبقية أو مواد غريبة | كل وردية | فحص بصري وباللمس |
2.3 التحقق من دقة الأداة
تؤثر هندسة الأداة تأثيرًا مباشرًا في الدقة الأبعادية وجودة السطح. يجب أن يكون الانحراف الشعاعي ≤0.01 مم لقواطع التفريز الطرفية المصنوعة من الكربيد الصلب و≤0.03 مم للأدوات ذات الإدخالات القابلة للتبديل. وتتطلب أدوات التشغيل الدقيق عمومًا انحرافًا أقل من 3 ميكرومتر عند سرعات التفريز العالية، مع انحراف أقل من 3 ميكرومتر على طول حد القطع بالكامل.
| نوع الأداة | حد الانحراف الشعاعي | أداة الفحص | تكرار الفحص |
| قاطعة تفريز طرفية من الكربيد الصلب | ≤0.01 مم | مقياس اتصال (مسند على كتلة V) | قبل تحميل كل دفعة |
| رأس تفريز وجهي بإدخالات قابلة للتبديل | ≥0.03 mm | مؤشر قرصي | عند كل تغيير أداة |
| Drill/reamer | ≤0.01 مم | مؤشر قرصي | عند كل تغيير أداة |
| Precision boring tool | ≤0.005 مم | Dial indicator and master ring gauge | عند كل تغيير أداة |
| Shrink-fit holder | ≤0.003 mm | مؤشر قرصي ومغزل معياري | Every tool loading |
3. سير عمل منظم للتصنيع باستخدام الحاسب الآلي
3.1 التحضير قبل الوردية وتسخين الماكينة
3.1.1 التأكد من حالة الماكينة
Switch on the main power, then start the machine and CNC system. After the system completes its self-check with no alarms, return each axis to its reference point (home). The recommended sequence is Z-axis first, followed by X and Y, to establish an accurate machine coordinate system as the datum for tool setting and machining. After homing, run the machine unloaded at low speed to warm it up. This distributes lubricant evenly over the spindle bearings and guide rails and reduces the effect of thermal deformation. A thermal-error compensation study showed that effective compensation reduced positioning error from −2.53–14.83 μm to −1.47–2.71 μm, an 81.66% reduction.
3.1.2 Check cooling and lubrication systems
Confirm that air pressure is stable within the machine’s specified range (typically 0.5–0.7 MPa) and that lubricant and coolant levels are within their normal ranges. For high-speed spindles, pay special attention to taper cleanliness; no chips or foreign matter may remain. Adjust coolant concentration to the material: use 8%–12% emulsion for stainless steel and 5%–8% for aluminum alloy.
3.2 تثبيت قطعة العمل وإنشاء مراجع التحديد
3.2.1 Control clamping accuracy
Secure clamping directly affects machining safety and accuracy. Before clamping, clean the worktable and workpiece locating surfaces and remove burrs and oil. When using a vise or strap clamps, tighten diagonally and use a dial indicator to align the workpiece parallel to the machine axes. Keep error within the process limit (typically ≤0.02 mm). For precision parts such as metering-pump gears and mixing-head valve cores, use dedicated locating fixtures to improve repeatability.
| Clamping method | Suitable workpiece | Locating accuracy | ملاحظات |
| Precision vise | Small and medium regular parts | ≤0.01 مم | Verify jaw parallelism |
| Vacuum chuck | Thin-wall plate parts | ≤0.005 مم | Check uniformity of vacuum force |
| Dedicated locating fixture | Metering-pump body, mixing head | ≤0.005 مم | Check locating-pin wear regularly |
| Four-axis rotary table | Multi-face machining parts | ≤0.008 مم | Verify rotary center |
3.2.2 Control tool-setting accuracy
Tool setting links the program coordinate system to the physical workpiece. Set each tool independently and enter its compensation value. Verify the origin with the “G54 X0 Y0” command to avoid batch scrap caused by tool-setting errors. Haifeng requires tool-setting accuracy within ±0.005 mm. For critical parts such as metering-pump gears and mixing-head valve cores, use a high-accuracy tool presetter or laser tool-setting system.
3.3 التحقق من البرنامج وقطع القطعة الأولى
3.3.1 Program simulation and dry run
Before automatic machining, use the CNC graphical simulation or Dry Run mode to check for abnormal tool retraction, undefined axis movement, or possible collision with fixtures. Pay particular attention to whether the G codes at the beginning and end of the program (such as G90/G91 and G17/G18) match the intended operation.
3.3.2 First-article trial cut
Apply a “verify at low speed” approach to the first trial cut. Set the feed override below 50% and enable Single Block mode. After machining the first feature (such as a hole or milled face), pause the machine and measure critical dimensions with calipers, micrometers, or other suitable gauges. If a dimension is out of tolerance, make a fine adjustment through tool-radius compensation or work-coordinate offset. Resume continuous machining at 100% override only after the part passes inspection.
3.4 معاملات القطع والتحكم في الدقة
3.4.1 Material groups and cutting parameters
CNC machining for Haifeng equipment mainly involves carbon steel, alloy steel, stainless steel (304/316L), aluminum alloy (6061/7075), and cemented carbide. Select optimized parameters from the applicable table for each material.
Recommended milling parameters for stainless steel (304/316L) (with TiAlN-coated carbide tools):
| Operation | Cutting speed Vc (m/min) | Feed per tooth fz (mm/tooth) | Radial depth ae | Axial depth ap |
| Roughing (side milling) | 100–140 | 0.05–0.08 | 0.10D–0.15D | 0.5D–1.0D |
| Semi-finishing | 120–160 | 0.03–0.06 | 0.05D–0.10D | 0.3D–0.5D |
| التشطيب | 140–180 | 0.02–0.04 | 0.02D–0.05D | 0.1D–0.3D |
Recommended milling parameters for aluminum alloy (6061/7075):
| Operation | Cutting speed Vc (m/min) | Feed per tooth fz (mm/tooth) | Radial depth ae | Axial depth ap |
| Roughing | 200–300 | 0.10–0.20 | 0.15D–0.25D | 1.0D–2.0D |
| التشطيب | 250–350 | 0.05–0.10 | 0.05D–0.10D | 0.3D–0.5D |
With stable, consistent machining conditions, aluminum alloys 6061 and 7075 can achieve tolerances of ±0.01 mm or tighter.
3.4.2 Control and compensate for thermal deformation
Thermal-deformation error is a key indicator of machining-center accuracy. Apply the following controls when machining Haifeng equipment components:
1. Warm up before machining: Run the spindle unloaded for 15–30 minutes so that spindle bearings and ball screws reach thermal equilibrium.
2. Control coolant temperature: Maintain cutting-fluid temperature at 20±2°C to prevent heat from cutting from expanding the workpiece and tool.
3. Apply online compensation: For long continuous operations, enable the machine’s thermal-error compensation function and correct motion commands in real time using temperature-sensor data. Software compensation is widely used: a temperature-to-deformation mapping model calculates thermal error from live temperatures and applies corrections to motion-control commands.
4. Control ambient temperature: Maintain the precision-machining area at 20±2°C.
3.4.3 Monitor tool wear
Tool wear directly affects dimensional accuracy and surface roughness. Operators must monitor the following during machining:
| Item monitored | Normal condition | Warning threshold | Response |
| Spindle load | Stable without sharp fluctuation | Fluctuation >10% | Check tool/workpiece condition |
| Cutting sound | Even humming | Shrill squeal or dull impact | Stop immediately and check for chipped tool edges |
| Surface-roughness trend | Stable within standard | Ra increase >20% | Replace tool or adjust parameters |
| Chip shape | Regular C-shaped or short spiral | Powder-like or long tangled chips | Adjust feed/speed |
3.5 الفحص داخل الماكينة والتصنيع بالحلقة المغلقة
For critical precision parts such as metering-pump bodies and mixing-head valve cores, use in-machine inspection to create a closed-loop process integrating machining and inspection. Repeatability of the touch-trigger probe must be ≤0.002 mm.
In-machine inspection procedure:
1. After semi-finishing the part, call the in-machine inspection program.
2. Trigger the probe to contact key measurement points automatically (bore diameter, mating surface, position, etc.).
3. The system compares measured values with tolerance requirements.
4. If a deviation exceeds the warning range, the system automatically corrects the tool compensation value.
5. Perform finishing after correction to ensure the final dimensions pass inspection.
4. المعاملات الرئيسية لدقة التصنيع باستخدام الحاسب الآلي
| الرقم | Accuracy category | المعامل | معيار Haifeng | أداة الفحص | تكرار الفحص |
| 1 | Machine accuracy | دقة تحديد الموضع لمحاور X/Y/Z | ≤±0.01 مم | مقياس تداخل ليزري | كل ثلاثة أشهر |
| 2 | Machine accuracy | دقة تحديد الموضع المتكرر لمحاور X/Y/Z | ≤±0.005 mm | مقياس تداخل ليزري | كل ثلاثة أشهر |
| 3 | Machine accuracy | الخلوص العكسي | ≤0.002 mm | مقياس تداخل ليزري | كل ثلاثة أشهر |
| 4 | Machine accuracy | الانحراف الشعاعي للمغزل | ≤0.003 mm | مؤشر قرصي ومغزل معياري | كل ثلاثة أشهر |
| 5 | Tool accuracy | Solid-carbide end-mill radial runout | ≤0.01 مم | مؤشر قرصي | At each batch tool loading |
| 6 | Tool accuracy | Precision boring-tool radial runout | ≤0.005 مم | Dial indicator and master ring gauge | عند كل تغيير أداة |
| 7 | Machining accuracy | 316L stainless-steel dimensional tolerance | IT6–IT7 | CMM | First article and sampling |
| 8 | Machining accuracy | Aluminum-alloy dimensional tolerance | IT6–IT7 | CMM | First article and sampling |
| 9 | Machining accuracy | تفاوت موضع الثقب | ≤0.02 مم | CMM | First article and sampling |
| 10 | جودة السطح | خشونة سن ترس مضخة قياس الجرعات | Ra ≤0.4 μm | Surface-roughness tester | 100% inspection |
| 11 | جودة السطح | خشونة سطح التلامس بين قلب الصمام ورأس الخلط | Ra ≤0.2 μm | Surface-roughness tester | 100% inspection |
| 12 | جودة السطح | General mating-surface roughness | Ra ≤0.8 ميكرومتر | Surface-roughness tester | Sampling inspection |
| 13 | Critical fit | خلوص سن ترس مضخة قياس الجرعات مع التجويف | 0.127 mm per side (0.005 in) | Pneumatic gauge/plug gauge | 100% inspection |
| 14 | Critical fit | Mixing-head valve-core-to-sleeve clearance | 0.005–0.015 mm | Pneumatic gauge | 100% inspection |
| 15 | Environmental control | درجة الحرارة المحيطة أثناء التشغيل | 20±2°م | Temperature/humidity logger | Continuous monitoring |
| 16 | In-machine inspection | Touch-trigger probe repeatability | ≤0.002 mm | Master-ball calibration | كل وردية |
5. المشكلات الشائعة ومزالق العمليات
5.1 الانحراف المفرط للأداة يزعزع دقة التجاويف
Symptom: Bore dimensions vary within tolerance but the CV exceeds 0.5%, or chatter marks appear on the bore wall.
Root cause: Tool radial runout exceeds the standard. When a solid-carbide end mill has runout above 0.01 mm, the effective diameter of its cutting edges exceeds the nominal diameter and the edges carry uneven cutting loads, resulting in oversized bores and poorer surface quality. In reaming and boring, every 0.01 mm increase in tool runout can cause a bore-diameter deviation of 0.015–0.02 mm.
Corrective actions:
1. Before loading each batch, measure runout with a dial indicator: ≤0.01 mm for solid-carbide end mills and ≤0.005 mm for precision boring tools.
2. Check holder-taper cleanliness and wear; replace the holder if needed.
3. Replace collet holders with shrink-fit holders to reduce runout to below 0.003 mm.
4. For precision bores, separate boring and reaming into distinct operations: rough-bore first, then finish with an adjustable reamer.
5.2 التصلد الانفعالي أثناء تصنيع الفولاذ المقاوم للصدأ يسبب تآكلًا غير طبيعي للأداة
Symptom: Tool life when machining 316L falls sharply (below 30 minutes), cutting force increases, and surface quality deteriorates.
Root cause: Austenitic stainless steel (304/316L) has a strong tendency to work-harden. During cutting, surface hardness can rise from HB 150 to above HB 300. Incorrect cutting parameters, such as insufficient depth of cut or feed, make the tool repeatedly cut the hardened layer and accelerate wear. The molybdenum content of 316L makes it more prone to work hardening than 304.
Corrective actions:
1. Use a high-feed, shallow-cut strategy so the cutting edge always engages material below the hardened layer.
2. Use trochoidal milling for 316L. Reference parameters: Vc=196 m/min, fz=0.08 mm/tooth, ae=1 mm, ap=24 mm.
3. Select TiAlN- or AlTiN-coated carbide tools to improve resistance to crater wear.
4. Apply sufficient coolant to prevent heat buildup from worsening work hardening.
5.3 التشوه الحراري يسبب انحراف دقة الأجزاء الدقيقة
Symptom: Parts that pass in the morning show systematic dimensional shift in the afternoon (typically 0.01–0.03 mm), or dimensions drift gradually during continuous machining.
Root cause: Cutting and friction heat expand the machining-center spindle, ball screws, and workpiece. Spindle axial thermal growth can reach 0.02–0.05 mm, and ball-screw growth can reach 0.05–0.10 mm over a 3 m travel. For precision parts in Haifeng equipment with tolerances as tight as ±0.005 mm, thermal deformation is a primary cause of batch accuracy drift.
Corrective actions:
1. Run the spindle unloaded for 15–30 minutes before machining; begin only after thermal equilibrium is reached.
2. Enable thermal-error compensation during long continuous runs. Test data indicate that compensation can keep thermal error within 8 μm.
3. Schedule finishing operations during the stable period after the machine reaches thermal equilibrium.
4. For precision parts, use a staged process: rough machining, natural cooling, then finish machining.
5.4 تشوه التثبيت يُخرج الأجزاء رقيقة الجدران عن حدود التفاوت
Symptom: Thin-wall parts such as metering-pump bodies become oval or out of tolerance after machining, and spring back when the fixture is released.
Root cause: Excessive clamping force or poorly distributed clamping points elastically deform the part while it is held. The tool cuts material from this deformed state; once unclamped, the part springs back and its actual dimensions shift.
Corrective actions:
1. Use a vacuum chuck or dedicated soft jaws instead of hard-jaw clamping to distribute clamping force.
2. For precision thin-wall parts, use axial clamping with auxiliary radial support.
3. After roughing, release the fixture and allow the part to cool naturally; then finish with lower clamping force.
4. Reduce finishing feed as appropriate to limit cutting-force deformation.
5.5 التركيز غير الصحيح لسائل التبريد يسبب تفاوتًا في جودة السطح
Symptom: Stainless-steel parts made with the same program show inconsistent roughness, with some batches exceeding Ra 0.8 μm.
Root cause: Cutting-fluid concentration is outside the recommended range. Stainless-steel machining needs sufficient lubrication and cooling. Emulsion below 8% provides insufficient lubrication and accelerates tool wear; above 15%, cooling performance declines, foam increases, and chip evacuation worsens.
Corrective actions:
1. Use 8%–12% emulsion for stainless steel and 5%–8% for aluminum alloy.
2. Measure and record coolant concentration with a refractometer every shift.
3. Regularly remove chips and floating oil from the coolant tank to prevent bacterial growth.
4. For precision machining of 316L stainless steel, use high-pressure through-tool coolant (pressure ≥70 bar) to aid chip removal and cooling.
5.6 الإعداد غير الصحيح لإحداثيات البرنامج يسبب خردة في الدفعة
Symptom: The first article passes, but after several consecutive parts a systematic dimensional shift appears, equal to a fixed offset.
Root cause: The work coordinate system (G54/G55) or tool-length compensation value is set incorrectly. In multi-operation machining, failure to switch work coordinates or the correct tool-compensation number makes the tool move from the wrong datum.
Corrective actions:
1. Follow the “tool setting–verification–trial cut” process strictly; set each tool independently.
2. Verify the origin with “G54 X0 Y0” and start batch production only after confirming it is correct.
3. Set a safe height (Z-axis safety plane) at the beginning of the program to prevent a coordinate error from causing a tool crash.
4. Before batch machining, dry-run a complete cycle in Single Block mode and confirm the path is correct.