

تبدو مواصفات مقاومة اللهب واضحة على الرسم: مؤشر أكسجين محدد 28، وUL 94 V-0، واجتياز FMVSS 302. لكن واقع الإنتاج أقل انتظامًا. فجزءان يحملان التصنيف نفسه قد يتصرفان بشكل مختلف تبعًا للكثافة، وبنية الخلايا، وتكوّن القشرة، وما إذا كان مثبط اللهب قد وُزّع بالتساوي فعليًا. يشرح هذا المقال ما يقيسه مؤشر الأكسجين المحدد، وموقع هذا المؤشر بين اختبارات الحريق المستخدمة للبولي يوريثان، ولماذا تُعد خيارات المعدات بالغة الأهمية بقدر خيارات التركيبة.
ما الذي يقيسه مؤشر الأكسجين المحدد (LOI) فعليًا
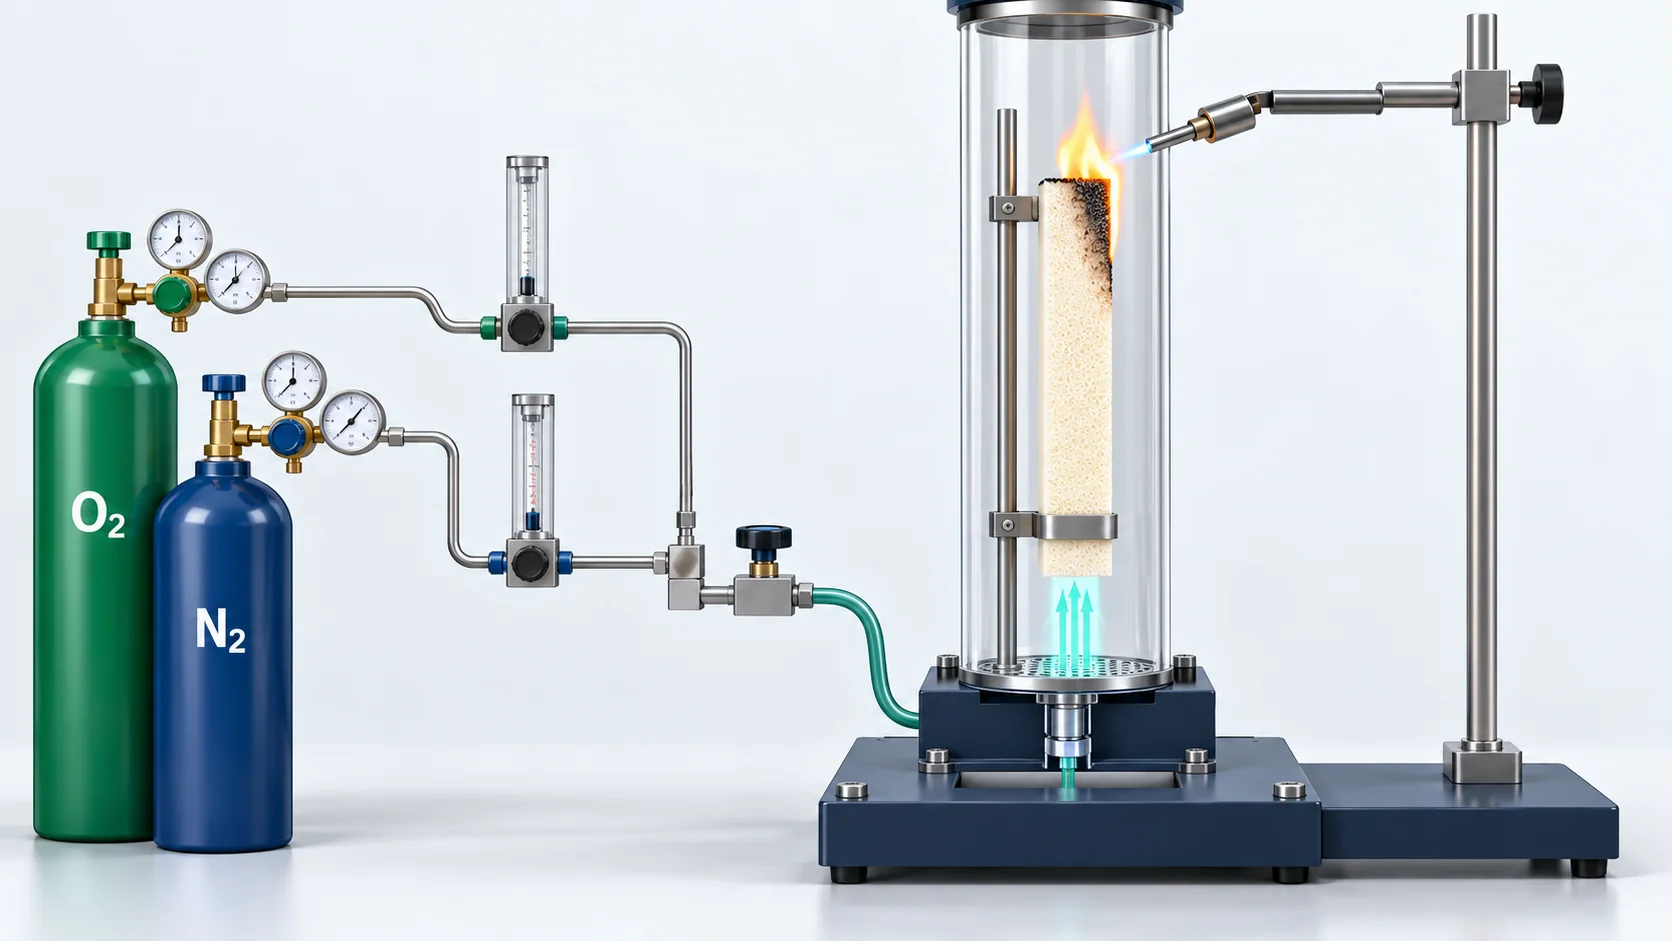
Limiting oxygen index is the minimum oxygen concentration, expressed as a percentage, required to support candle-like combustion of a material in an oxygen-nitrogen mixture under controlled laboratory conditions [1][2]. The test uses a small specimen held vertically in a chimney. An igniter is applied to the top surface, and the operator or instrument determines the lowest oxygen fraction at which burning continues for a defined length or time.
Normal air is about 21% oxygen. A material with an LOI below 21 can continue to burn in air once ignited; a material with an LOI well above 21 needs an oxygen-enriched atmosphere to keep burning. That makes LOI useful as a formulation screening number: higher LOI generally means harder ignition and more rapid self-extinguishing in the bench test. It is not a prediction of full-scale fire behavior.
Two things are worth keeping straight. First, LOI is a material property measured under one ignition geometry, not a product fire rating. Second, LOI results are sensitive to specimen thickness, conditioning, and whether the material drips or chars [1][2]. If a production part has density gradients or a non-uniform flame-retardant distribution, a single laboratory plaque can still be misleading.
كيف يرتبط مؤشر الأكسجين المحدد بمعيار UL 94 وFMVSS 302 وتصنيفات المباني
It is common to see LOI listed next to a UL 94 class, but they are not interchangeable tests.
UL 94 evaluates small-flame ignition and burning of plastic specimens in horizontal or vertical orientation. The familiar vertical classes are V-0, V-1, and V-2; HB is the horizontal burn class. The vertical test applies a 50 W burner flame twice to a bar specimen and records afterflame time, afterglow, and flaming drips [3]. Some flame-retardant polyurethanes are submitted to UL 94, but the rating applies to the tested thickness, grade, and color; a V-0 plaque does not automatically make a molded part V-0.
FMVSS 302 covers automotive interior materials. The test uses a horizontal specimen exposed to a small flame and measures burn rate; a common benchmark is a maximum burn rate of 102 mm/min for materials that do not self-extinguish [4]. Polyurethane seating foam, headliners, and trim foams are often tested as part of the assembled interior, not as isolated foam.
For building insulation, the relevant frame is usually the Euroclass system under EN 13501-1 or the North American surface-burning test ASTM E84. EN 13501-1 assigns reaction-to-fire classes such as B, C, D, or E, with additional smoke and flaming-droplet classifications [5]. ASTM E84 produces Classes A, B, or C based on flame spread and smoke developed index [6]. Rigid spray polyurethane foam and PIR board are often evaluated as a finished system: foam, facing, joint, and installation condition together determine the class.
None of these tests converts cleanly to LOI. A high LOI often helps with vertical ignition tests, but dripping, thickness, and char integrity matter in UL 94 and the building tests. A specification that only says “flame-retardant polyurethane” is therefore incomplete.
Flame-retardant spray foam also changes viscosity, cell structure, and spray pattern. ما هو تركيب رغوة البولي يوريثان بالرش وتطبيقاتها covers how SPF formulation and application conditions shape the finished foam.
كيميائيات مقاومة اللهب وكيف تغيّر المعالجة
Most polyurethane flame retardants work through one of a few mechanisms: gas-phase radical scavenging, endothermic decomposition, char formation, or dilution. Common approaches include:
- Liquid phosphorus-based flame retardants, which can plasticize and lower viscosity at process temperature but may require careful mixing.
- Halogenated flame retardants, often used with antimony synergists where regulatory and environmental limits allow.
- Mineral fillers such as aluminum trihydroxide (ATH) or magnesium hydroxide, which release water and absorb heat during decomposition; these raise viscosity and can settle.
- Melamine and other nitrogen-based additives, often used in flexible foam to limit dripping during small-flame tests.
- Intumescent or char-forming packages, used where a protective carbon layer is more important than gas-phase inhibition.
The same flame retardant can shift a formulation enough to change processing economics. A liquid phosphate may make the polyol side easier to pump but reduce final foam hardness; a high-load ATH package may require continuous tank agitation and larger pump clearances. Because these additives sit in the polyol or blended side, their particle size and settling rate matter throughout the production shift.
In semi-rigid automotive and trim foams, flame-retardant requirements are often specified alongside density, surface quality, and mold-fill behavior. ما هي رغوة البولي يوريثان شبه الصلبة covers where semi-rigid foam is used and what changes to expect in molding.
لماذا لا تضمن التركيبة وحدها الحصول على التصنيف
A fire test specimen is not the same thing as a production part. In a well-mixed laboratory plaque, the flame retardant is evenly distributed and density is controlled. In production, several things can create local weak spots:
- Ratio drift. If the isocyanate index or the polyol-side additive percentage drifts, some parts may foam with a lower flame-retardant concentration than the qualification sample.
- Filler settling. ATH and other solid additives can settle in a static tank, so the last shots of a shift may be richer in particles than the first shots.
- Density variation. Lower-density regions in flexible foam can ignite more easily under small-flame tests and can produce more dripping.
- Incomplete mixing. Flame-retardant packages that are not fully dispersed leave resin-rich or additive-poor domains that a visual inspection may miss.
- Skin and cell structure differences. A thick integral skin or a fine closed-cell surface can delay ignition in a way that a cut foam core cannot.
This is why qualified parts should be tested at the same thickness, density, and surface condition as the production article, and why incoming material lots should be checked against the original qualification. A rating applies to a specific system, not to the word “polyurethane.”
قرارات المعدات التي تؤثر على معالجة المواد المقاومة للهب
When a plant moves from standard polyurethane to a flame-retardant formulation, three equipment choices usually determine whether the line stays stable.
Tank agitation and recirculation. Solid flame retardants must remain suspended. Tank loops without adequate agitation let filler settle, so the ratio changes over time. Recirculation also holds temperature and viscosity within a narrower band.
Metering and pump selection. Liquid phosphate plasticizers can thin one side, while ATH can be abrasive and shear-sensitive. Gear pumps and closed-loop flow measurement need to maintain the A/B ratio even when viscosity changes through the shift. Ratio control matters for fire performance because the flame retardant is almost never an inert extra.
Mixing head design and pressure. High-viscosity, filled systems respond differently in low-pressure mixers than in high-pressure impingement mixing heads. Poor dispersion may not show up as a visible defect; it can appear later as uneven LOI, UL 94 afterflame time, or smoke drip in FMVSS 302.
On Haifeng polyurethane machinery, these requirements are handled at the machine level: recirculating material stations, closed-loop metering, and mixing heads built for filled systems. The same applies to elastomer and rigid foam lines where flame-retardant additives are added on the polyol side. The first step is defining the processing window with the flame-retardant supplier before selecting equipment.
If you are evaluating a foaming machine for a flame-retardant system, send the current formulation viscosity, filler type, target output, and required fire standard. A quick compatibility check can prevent the most expensive mistake: buying a machine that meters well in a clean formulation and drifts once the filler is introduced. Contact info@chinahaifeng.com or WhatsApp +86 13566296633 for a processing review.
قائمة تحقق عملية للمواصفات الخاصة بالبولي يوريثان المقاوم للهب
Use this as a working checklist before locking a part drawing or machine specification:
- Name the fire standard first: UL 94, FMVSS 302, EN 13501-1, ASTM E84, or a customer-specific test. LOI alone is rarely enough.
- Define the tested part geometry, thickness, skin condition, density, and any facing or lamination.
- Ask the flame-retardant supplier for the processing envelope: viscosity at operating temperature, particle size, settling rate, and recommended mixing type.
- Specify ratio tolerance and material temperature range on the production machine, not just in the lab.
- Require retain samples and periodic fire-test verification from production, not only qualification plaques.
- Include tank agitation, recirculation, and wear-resistant pump selection when the formulation contains solid flame retardants.
As with LOI, resilience testing depends on conditioned specimens and a repeatable protocol. قياس مرونة رغوة البولي يوريثان: دليل اختبار عملي covers a structured bench-test approach you can use as a model for in-house fire-test documentation.
هل تحتاج إلى مساعدة في تحديد مواصفات معدات البولي يوريثان المقاوم للهب؟
Haifeng Polyurethane Machinery works with high-pressure and low-pressure foaming lines, elastomer casting systems, and turnkey polyurethane production equipment. If you are dealing with flame-retardant formulations and need to match metering, mixing, and additive handling to the fire test your customer requires, send drawings, target output, and material data.
جهة الاتصال:
- البريد الإلكتروني: info@chinahaifeng.com
- WhatsApp: +86 13566296633
الأسئلة الشائعة
ما الفرق بين مؤشر الأكسجين المحدد ومعيار UL 94؟
LOI measures the minimum oxygen concentration that supports candle-like combustion in a controlled oxygen-nitrogen atmosphere [1][2]. UL 94 measures timed burning, afterflame, and flaming drips under a small flame in horizontal or vertical orientation [3]. A material can have a high LOI and still fail a UL 94 requirement if it drips heavily or supports flame spread, so both values deserve a place in a specification when both matter.
ما قيمة مؤشر الأكسجين المحدد التي تُعد مقاومة للهب في البولي يوريثان؟
There is no universal threshold. A material with an LOI near 21 is on the boundary of air-supported combustion, while values comfortably above 21 indicate greater difficulty sustaining flame in the bench test. Many flame-retardant rigid polyurethane and PIR formulations are developed to reach LOI values in the mid-20s or higher, but the target should be tied to the application standard rather than a fixed number.
هل تجعل الكثافة الأعلى البولي يوريثان أقل قابلية للاشتعال؟
Higher density in the same foam family usually means more mass to heat before sustained burning, so it can improve small-flame performance. But density is not a fire rating. A high-density foam with no flame retardant can still fail a vertical ignition test, and a low-density foam with a good char-forming system may pass its intended bench test. Fire behavior also depends on cell structure, facing, and additives.
هل يمكن لرغوة البولي يوريثان اجتياز اختبار FMVSS 302؟
Yes. Automotive polyurethane foams are routinely tested to FMVSS 302 and can meet the required horizontal burn behavior, especially when flame-retardant additives are combined with the right density and skin formation [4]. The key is to test the production material at the same thickness and in the same assembly condition used in the vehicle.
كيف تؤثر مثبطات اللهب على معدات المعالجة؟
They can increase viscosity, cause filler settling, add shear sensitivity, or change the mixing ratio balance. Equipment with recirculating tanks, closed-loop metering, and wear-resistant pumps handles flame-retardant systems more consistently. Without those features, the production part may pass qualification and drift later in the shift.
هل يكفي مؤشر الأكسجين المحدد للامتثال في عزل المباني؟
No. Building insulation is classified under reaction-to-fire standards such as EN 13501-1 in Europe or ASTM E84 in North America [5][6]. LOI can be used during formulation development, but the finished insulating product—including facing, density, thickness, and installation—must meet the applicable building code classification.
المراجع
[1] ISO 4589-2:2017, Plastics — Determination of burning behaviour by oxygen index — Part 2: Ambient-temperature test, International Organization for Standardization, Geneva, 2017.
[2] ASTM D2863-19, Standard Test Method for Measuring the Minimum Oxygen Concentration to Support Candle-Like Combustion of Plastics (Oxygen Index)، جمعية ASTM الدولية، كونشوهوكين، بنسلفانيا، 2019.
[3] UL 94, Standard for Tests for Flammability of Plastic Materials for Parts in Devices and Appliances, Underwriters Laboratories, Northbrook, IL.
[4] FMVSS 302, Flammability of Interior Materials, U.S. National Highway Traffic Safety Administration, Washington, D.C.
[5] EN 13501-1:2018, Fire classification of construction products and building elements — Part 1: Classification using data from reaction to fire tests, European Committee for Standardization, Brussels, 2018.
[6] ASTM E84-23, Standard Test Method for Surface Burning Characteristics of Building Materials، ASTM International، ويست كونشوهوكن، بنسلفانيا، 2023.
إذا كنت مهتمًا، فاطّلع على هذه المقالات ذات الصلة:
كيف تُصنع بكرات البولي يوريثان من الصب حتى المعالجة
صلابة Shore A مقابل Shore D في البولي يوريثان
RRIM مقابل RIM: أي عملية تناسب الجزء الإنشائي لديك
شرح SRIM: أساسيات القولبة بالحقن التفاعلي الهيكلي
كيفية حساب وزن القذفة في البولي يوريثان





