

Hot pressing uses a heated tool and controlled closing force to form or bond a specified part. In KPU shoe-upper production, a hot press system can form three-dimensional decorative details with matched tooling and a defined heat, pressure and dwell profile. If a request lists only “hot machinery,” replace it with the part, substrate, usable tool area and tested production rate.
Start with the layers and the tool
Send a reference upper, drawings for the trim and relief, and the approved KPU material and substrate. Have the material and tooling suppliers define the workable heating and cooling conditions. Agree which tool surfaces are heated and how the base is located so that alignment and pattern depth are repeatable. Document tolerances at seam interfaces and areas that will be flexed during wear.
Compare press capacity using the planned tool footprint and cavity layout. A nominal force in the brochure gives limited information about the pressure distribution across a large tool. Ask for verification of platen flatness and temperature distribution across the loaded tool. Confirm the loading arrangement, accessible space and tooling change procedure.
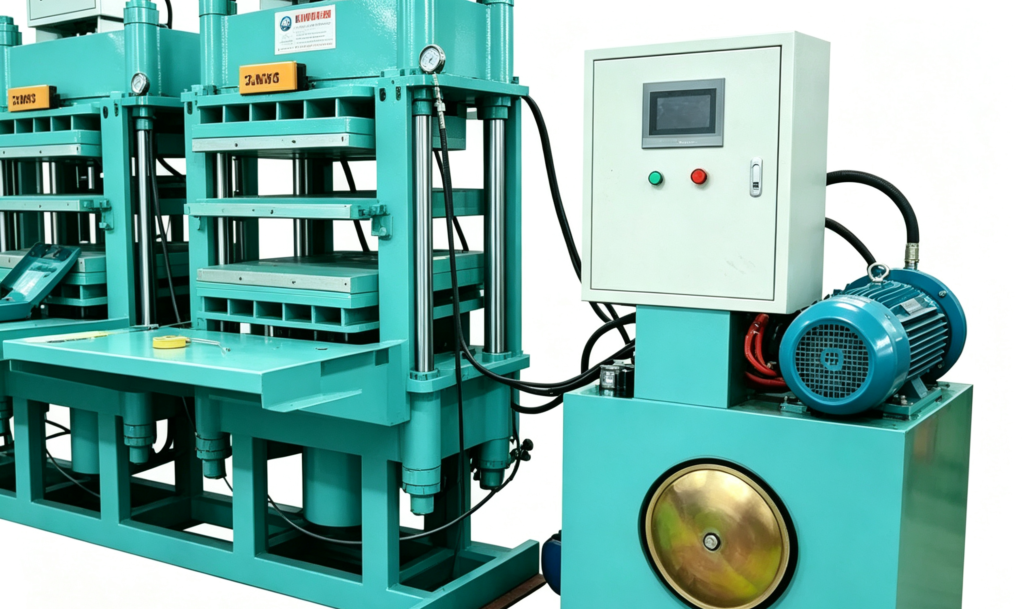
Make the trial match real production
- Run the smallest and largest upper sizes that share the press. Use representative layers, including any difficult-to-position panel or finish.
- Measure surface pattern, adhesion, dimensional appearance and the worst visible transitions. Ask the product development team to specify flex and bond checks for the actual upper.
- Time loading, heating and dwell, unloading, any cooling fixture and inspection. Include a tool change and thermal stabilization before the first accepted part.
- Log recipe settings by tool and size. Check operator access and guarding with the production and safety teams before finalizing the station configuration.
Compare output after testing the whole station
Use accepted pairs per hour, including mixed sizes and color changes. For example, two upper pieces per completed 90-second cycle would yield 80 pieces in an uninterrupted hour before yield and changeover losses. If each pair requires coordinated left and right tooling, check which sizes the station can actually release together. Compare the KPU hot press molding machine with the upstream and downstream operations described in the guide to high-mix footwear production lines. Include which vendor owns the mold tests, process records, spares and training.





