
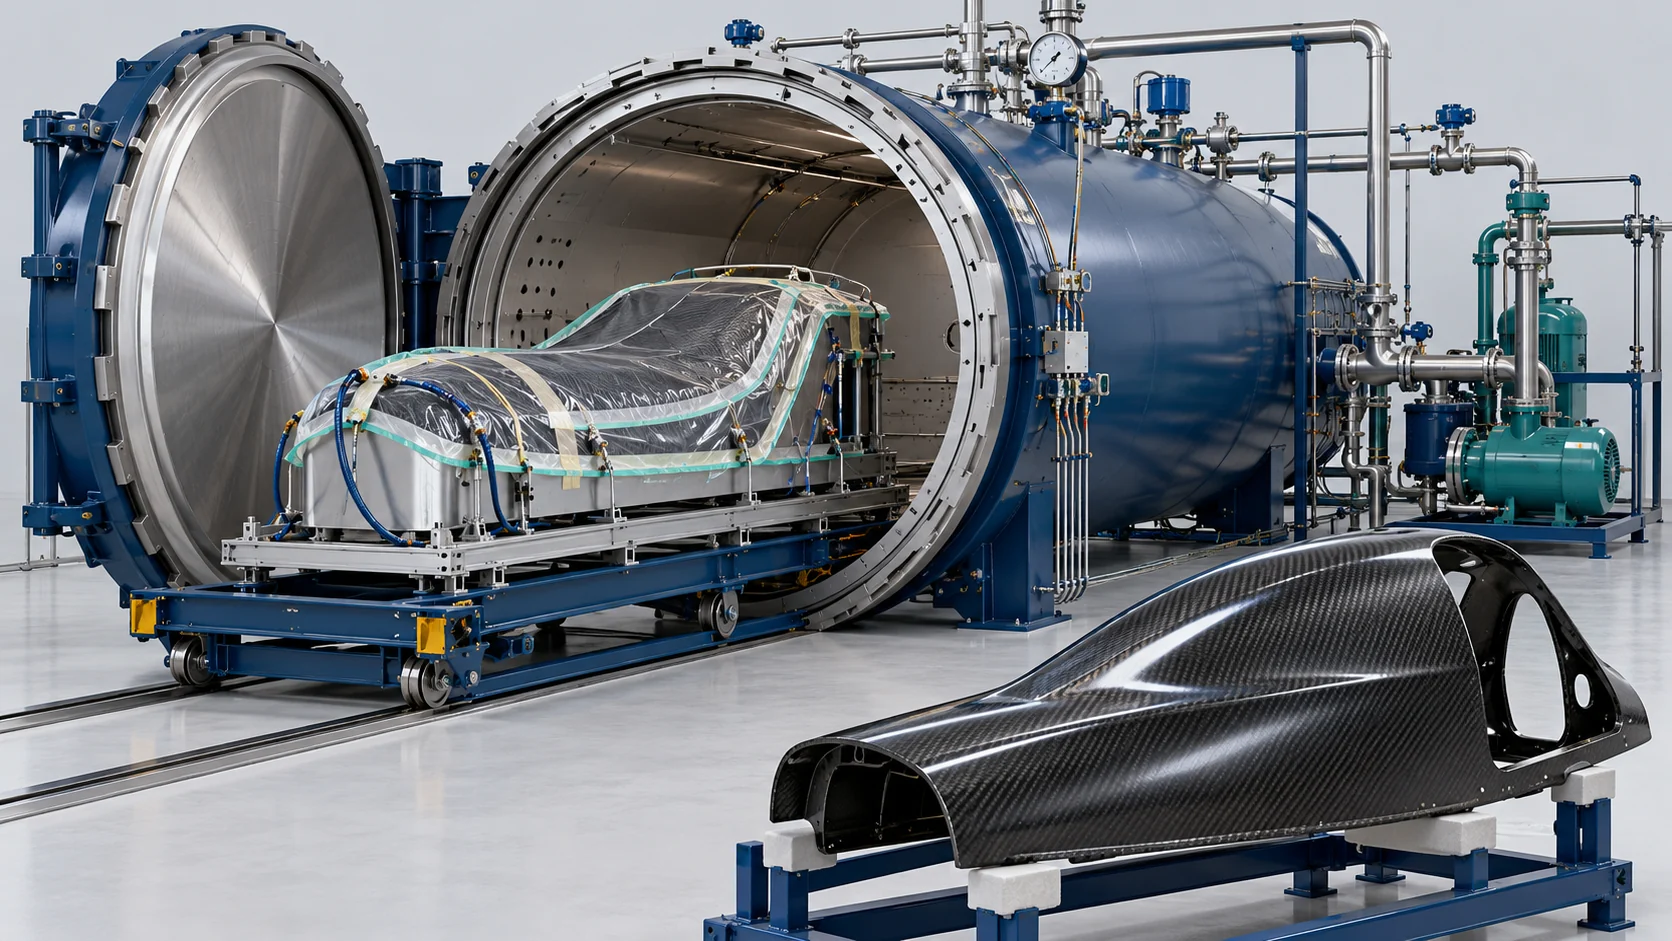
Производственное решение для формования композитов в автоклаве
Coordinate prepreg layup, vacuum bagging and a qualified autoclave pressure/temperature cycle.
Стройте процесс вокруг своего изделия
Coordinate prepreg layup, vacuum bagging and a qualified autoclave pressure/temperature cycle.
Сначала изделие и материал
Начните с чертежа готового изделия, системы материалов и требований к приемке. Технологический маршрут и комплектация оборудования оцениваются совместно.
Производительность по всему процессу
Определяйте выпуск с учетом подготовки, формования/реакции, отверждения, обработки и контроля. Практическую производительность линии определяют самый медленный этап и смены изделий.
Состав оборудования и процесса
Specified vessel/door, heating/circulation, pressurization, vacuum circuits and controls. Tooling, prepreg, gas supply, facility design and applicable pressure-vessel documentation are separately agreed.
Валидация и планирование производства
The 3.5 m × 12 m clear working envelope and approximately 130 m³ total vessel volume describe different geometry. Ultrasonic inspection coverage and quantitative laminate porosity are separate acceptance tasks. Equipment capability does not by itself establish aerospace qualification.
Define usable loaded space, tool mass, vacuum channels and part-temperature monitoring alongside the autoclave cycle. Vessel design/operating limits, thermal uniformity and aerospace component qualification are different requirements with separate records.
От подготовки до годного изделия
Последовательность планирования для указанного маршрута. Окончательные настройки и условия приемки устанавливаются по результатам анализа материала и детали.
Define the laminate
Review prepreg, tool, part dimensions and required qualification.
Control storage and layup
Track material exposure, ply orientation and intermediate compaction.
Bag and instrument
Arrange seals, vacuum connections and part/tool temperature monitoring.
Информация, необходимая для настройки линии
Предоставьте эти данные, чтобы можно было определить состав оборудования, интерфейсы и план валидации.
| Проектные данные | Требуемая информация |
|---|---|
| Part envelope | Tool/part dimensions, mass and laminate thickness |
| Prepreg | Storage/out-time and approved cure instructions |
| Autoclave interface | Vessel capacity, pressure, thermal and vacuum requirements |
| Приёмка | Cure records, dimensional and laminate tests |
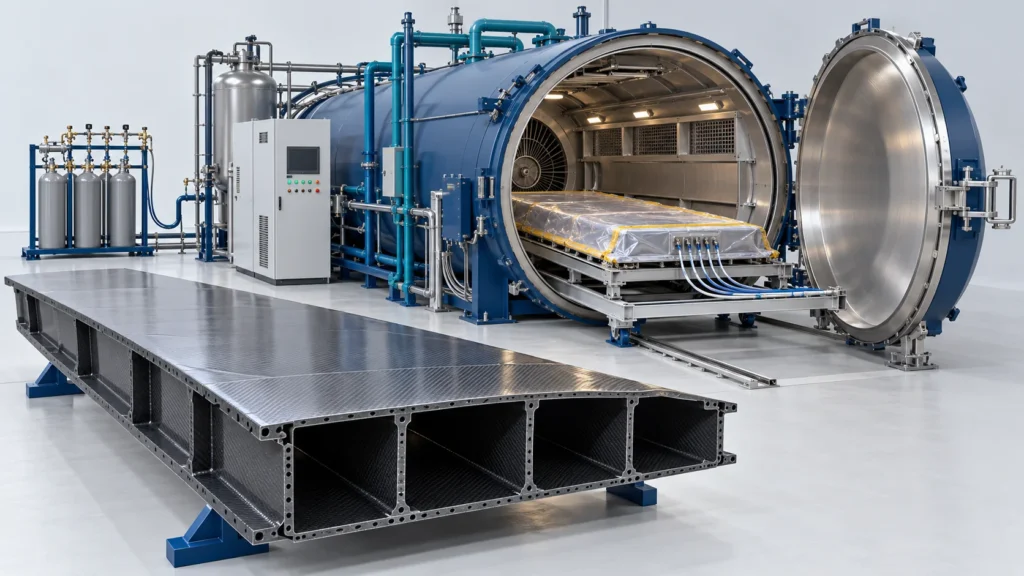
Large Aerospace Composite Application: Configuration Reference
The following supplied configuration illustrates a large-tool curing package. Final pressure-vessel requirements, facility services, approved material cycles and part qualification are agreed separately.
| Параметр | Значение / единица измерения | Применимая конфигурация / условия |
|---|---|---|
| Effective Working Dimensions | Ø 3,500 mm Diameter x 12,000 mm Length | Accommodates 11m monolithic wingbox panels and spars; configuration-specific reference or part acceptance target |
| Maximum Vessel Operating Pressure | 0.1 to 1.5 MPa (15 bar) | High-purity dry nitrogen gas pressurization; configuration-specific reference or part acceptance target |
| Operating Temperature Range | Ambient up to 250°C | Multi-zone electric finned circulation heaters; configuration-specific reference or part acceptance target |
| Thermal Field Uniformity | Within ±1.5°C across working zone | 24-point temperature survey using the agreed method and load conditions; configuration-specific reference or part acceptance target |
| Ultrasonic Inspection Pass Rate | Part acceptance target defined in the technical agreement | Ultrasonic coverage, acceptance criteria and quantitative porosity measurement are separate; use the agreed part-specific method and acceptance criteria |
| Cured Laminate Porosity Level | Part acceptance target defined in the technical agreement | Ultrasonic coverage, acceptance criteria and quantitative porosity measurement are separate; use the agreed part-specific method and acceptance criteria |
Vacuum, Cure Records and Laminate Acceptance
The supplied package includes 48 independent tooling-vacuum channels, bag-leak monitoring, zoned heating, circulation, gas pressurization and controlled cooling. Its process reference uses nitrogen purity of at least 99.9%, a bag-vacuum reference of 0.05 kPa absolute and a leak-rate reference below 0.05 kPa/min. Conditions and measurement boundaries are specified for each tool and bag.
An example cure schedule ramps at 1.5°C/min to 180°C, holds at 1.5 MPa for 120 minutes and cools at 1.8°C/min. The available ramp-rate reference is 0.5–2.5°C/min. Vacuum-line venting follows the approved material procedure; this example is not a universal prepreg cure recipe.
The supplied below-0.2% laminate porosity target and ultrasonic inspection coverage require separate methods and acceptance criteria. An 85 kg fastener comparison applies only to its specified aircraft structure. Equipment capability and a large working envelope do not establish aerospace qualification.
Основное оборудование и интегрированные интерфейсы
The autoclave is one core module; loading, vacuum, tooling, utilities and inspection need a defined delivery boundary.
Согласуйте оборудование с процессом
Оцените повторяемость, обращение с деталями и приёмку на всех этапах рабочего процесса.
Autoclave Cycle Control
Coordinate vessel pressure, vacuum channels, thermal uniformity and part-temperature records for the qualified cure schedule.
Cycle measurements
Record vessel pressure, vacuum channels and actual part temperatures.
Separate qualifications
Keep vessel suitability and finished-laminate evidence as distinct acceptance items.
Independent vacuum monitoring
Configured vacuum channels retain tool-bag vacuum and leak-alarm records alongside the approved cure schedule.
Связанные проекты
The wingbox record is an application reference. Confirm actual supplied modules and qualification documents rather than inferring aviation approval from vessel ratings.
Часто задаваемые вопросы
Определите производственный маршрут до выбора машины.
What does thermal-pressure molding mean here?
Какая информация нужна для определения размеров производственной линии?
Что входит в комплект оборудования?
Фиксированы ли время цикла и характеристики готовой продукции?
What should be verified under the actual autoclave load?
Опишите свои производственные задачи
Share the following for this application: Tool/part envelope and mass, batch loading, prepreg cycle, vacuum channels, thermocouples, site services and inspection. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


